RAPID SILICONE TOOLING · DEGASSING VACUUM CHAMBERS · PRE-SERIES BRIDGE PRODUCTION
Polyurethane Vacuum Casting & Silicone Mold Rapid Tooling
Polyurethane CastingDegassed Bubble-Free Vacuum Chamber10–100 Part Rapid Production RunsABS / PC / PP / Rubber Simulating ResinsFast 7–12 Business Days2.5D Optical VMM & Assembly Fit-Up Verified
Vacuum casting (polyurethane casting) is the gold standard for rapid pre-series manufacturing and high-fidelity functional prototyping. Utilizing precision silicone molds cast from SLA 3D printed or CNC machined master models, our automated vacuum chamber degassing process ensures bubble-free, production-grade polyurethane parts with exquisite surface textures and sub-millimeter detail fidelity. Bridge the gap between 3D printing and costly steel injection tooling with functional prototypes delivered in 7 to 12 business days.
7 – 12 Days
Fast Turnaround
Ex-factory production & inspection turnaround
±0.15 mm
Dimensional Precision
Per 100 mm (±0.0015″/in typical)
15 – 25 Pcs
Mold Cavity Life
Per silicone tool before re-casting
Shore 30A – 88D
Durometer Spectrum
Soft elastomeric rubber to rigid plastics
1. The Vacuum Casting Process: Step-by-Step Rapid Silicone Tooling
Polyurethane vacuum casting replicates the mechanical integrity and cosmetic finish of injection molded parts without expensive steel tooling. The workflow is executed inside our climate-controlled casting shop across four standardized engineering phases:
Standard 4-Step Vacuum Casting Workflow
1
Master Pattern Creation: An ultra-precise master model is fabricated via industrial
SLA 3D printing (high-temperature resin) or high-speed
CNC machining, then hand-sanded, primed, and finished to the required texture (SPI polish or Mold-Tech grain).
2
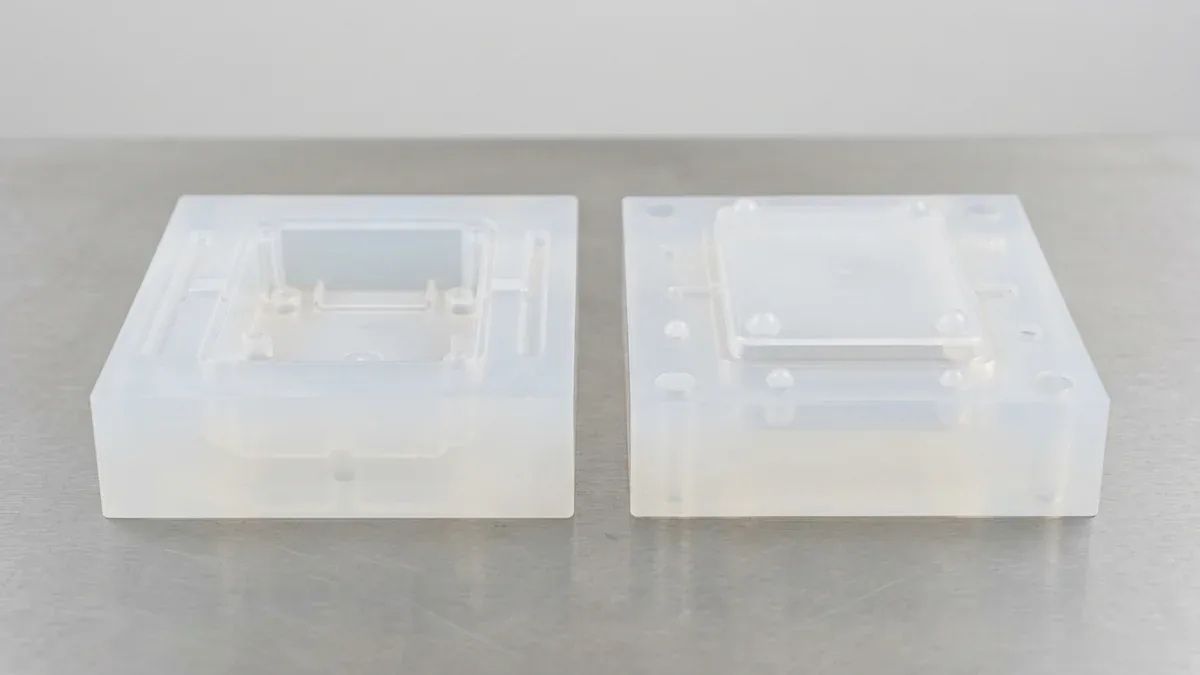
Silicone Mold Fabrication: The master pattern is fitted with gating and vent runners, suspended in a casting flask, and submerged in liquid addition-cure RTV silicone under vacuum to eliminate all micro-air bubbles before controlled thermal curing.
3
Dual-Cup Vacuum Degassing & Gravity Pouring: The parted RTV-2 silicone mold halves are fitted with pre-positioned brass inserts, closed, and tightly bound with high-tensile sealing tape. Inside the dual-chamber vacuum casting unit (–100 kPa / < 1 mbar), Cup A (polyol) and Cup B (isocyanate) undergo 10–15 minutes of primary vacuum degassing before Cup B is automatically tipped into Cup A, homogenized by a rotary mixing paddle, and poured through a conical funnel into the preheated silicone mold cavity.
4
Thermal Demolding & Post-Processing: Parts undergo post-curing in a convection oven at 60°C–70°C. Once demolded, parts receive sprue trimming, custom Pantone color painting, optical mold replication and UV-resistant clear lacquering, or conductive EMI shielding.
2. Engineering Design for Manufacturability (DFM) Guidelines
Designing plastic components for silicone molding offers substantial geometric freedom compared to rigid steel tooling, but respecting polymer shrinkage and fluid dynamics is critical for tight dimensional repeatability:
RULE 01
Nominal Wall Thickness
1.5 – 3.0 mm Optimal
Maintain uniform wall thickness throughout the part. Recommended nominal wall is 1.5 mm to 3.0 mm. Gradual thickness transitions prevent localized exothermic heat buildup and differential shrinkage.
RULE 02
Shrinkage Compensation
0.15% – 0.25% Factor
Account for cumulative volumetric shrinkage between master pattern fabrication, silicone mold curing, and polyurethane cross-linking. Our engineers scale CAD masters by ~0.15% to hit target dimensions.
RULE 03
Draft & Deep Undercuts
Flexible Demolding
Because silicone rubber is elastic and flexible, zero-draft walls, deep internal undercuts, and negative draft angles can be demolded naturally without requiring expensive mechanical side-actions or sliders.
RULE 04
Embossed Features & Inserts
Sub-Millimeter Fidelity
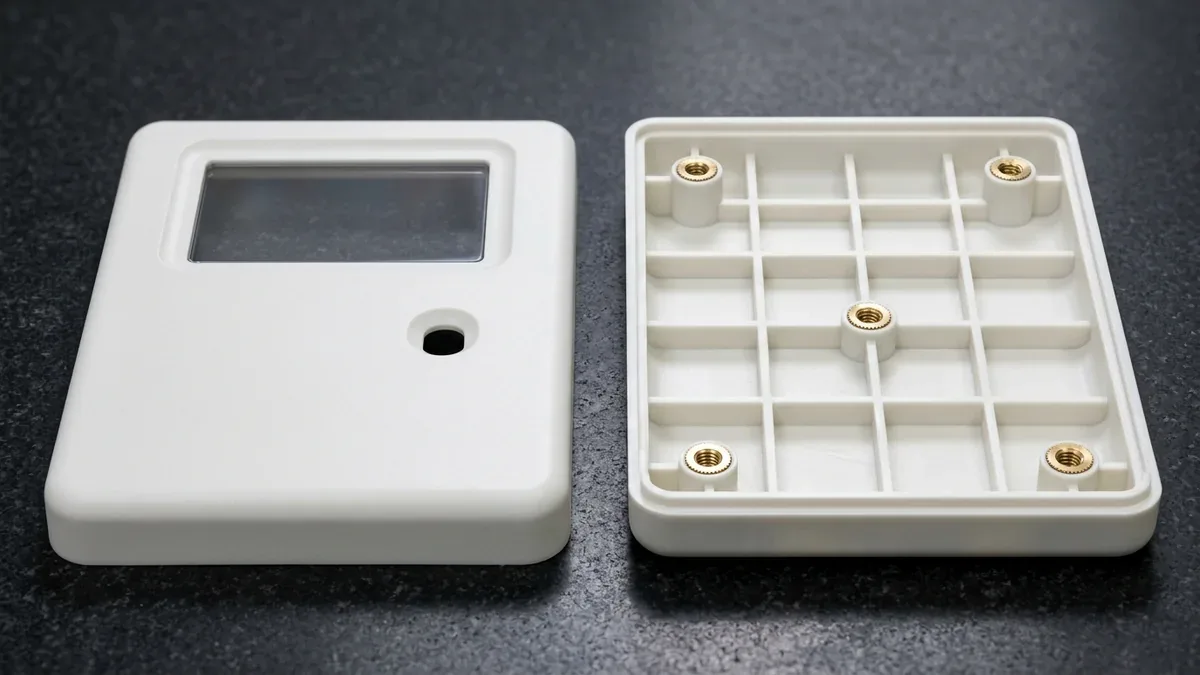
Silicone captures micro-textures, fine engraved text, and leatherette grains down to 10 μm. Threaded brass inserts can be pre-positioned in the mold and encapsulated in situ with superior pull-out resistance.
8-Point Polyurethane Vacuum Casting & RTV-2 Silicone Tooling Design for Manufacturability (DFM) Rules| Vacuum Casting Feature | Recommended Engineering Standard | Silicone Mold Physics & Part Quality Impact |
|---|
| 1. Nominal Wall Thickness | 1.5 mm to 3.0 mm (Minimum 1.0 mm on small localized ribs) | Ensures complete gravity-driven resin fill under vacuum before the 4–6 minute polyurethane pot-life gelation window expires. |
| 2. Cumulative Shrinkage Offset | Apply +0.15% to +0.25% isotropic scaling factor to the SLA / CNC master model | Compensates for addition-cure RTV-2 silicone cross-linking shrinkage and exothermic polyurethane curing contraction. |
| 3. Draft Angles & Undercuts | 0.5°–1.0° recommended on deep vertical bosses; moderate undercuts require 0° draft | Elastic Shore 40A silicone peels over snap-fit hooks and undercuts naturally without mechanical sliders, extending mold life to 20–25 shots. |
| 4. Reinforcing Rib & Boss Geometry | Rib thickness = 0.60 × nominal wall; fillet radii R ≥ 0.5 mm at rib intersections | Prevents exothermic heat concentration and air-pocket trapping at sharp corners during vacuum cavity filling. |
| 5. Co-Cast Metal Threaded Inserts | Use blind-ended knurled brass inserts (M2–M8) supported on steel dowel locator pins | Blind insert ends prevent low-viscosity liquid polyurethane from wicking into internal screw threads during vacuum pouring. |
| 6. Master Pattern Layer Line Removal | Specify hand-sanded 800-grit matte or SPI A-1 diamond buff on SLA/DLP master patterns | Platinum-cure silicone reproduces surface topography down to 2 μm—every master flaw or 3D print layer line will transfer to all 25 castings. |
| 7. Optical Clear Lens & Light Guide Design | Avoid abrupt thickness jumps > 6.0 mm on PMMA/PC-like clear urethane parts | Minimizes internal exothermic yellowing and refractive distortion during the 65–70 °C convection oven post-cure cycle. |
| 8. Quality Verification Method | Non-contact 2.5D Optical Vision (VMM), digital calipers, and mating assembly fit-up checks | Flexible and thin-walled elastomer/urethane castings are verified optically and via functional mating gauges without contact-probe deflection. |
Comprehensive Polyurethane Resin Spectrum & Technical Specifications
Our extensive library of specialized polyurethane formulations accurately emulates the mechanical, thermal, and cosmetic characteristics of end-use production thermoplastics:
Polyurethane Vacuum Casting Resins (ABS-Like, PC-Like, Elastomer) & Mechanical Properties| Simulated Plastic | Polyurethane Resin Grade | Hardness & Strength | Heat Deflection (HDT) | Key Properties & Applications |
|---|
| ABS-Like (Rigid & Impact) | Hei-Cast 8150 / Axson PX 223 | Shore 82–85D | Tensile: 70 MPa | 85°C – 95°C | High impact resistance, easy to paint/texture. Electronic housings, consumer device bezels. |
| PP / PE-Like (Ductile) | Axson PX 100 / Hei-Cast 3050 | Shore 75–80D | Elongation: 25% | 75°C – 85°C | High fatigue resistance, living hinges, snap-fits, fluid tanks, caps, and medical clips. |
| PC / PMMA-Like (Clear) | Axson PX 5210 / BJB TC-880 | Shore 84–87D | >88% Transparency | 90°C – 100°C | Optical water-clear, UV-stable, high-gloss finish via SPI A-1 master mold replication. Light pipes, LED lenses, dial windows. |
| Rubber / Elastomer (TPE) | Hei-Cast 8400 / Axson UP 4000 | Shore 30A – 90A (Adjustable) | Operating Temp: –20°C to 80°C (HDT: N/A for elastomers) | High tear strength, overmolding simulation, flexible keypads, waterproof gaskets, soft grips. |
| Flame-Retardant (UL94-V0) | Axson PX 245 / Sika FR Series | Shore 85–88D | UL94-V0 | 125°C – 140°C | Self-extinguishing under electrical load. Switchgear housings, EV power modules, aerospace. |
3. Surface Finishing & Aesthetic Customization
Polyurethane vacuum casting delivers outstanding aesthetic realism. Surface finishes cloned from the master model can be paired with our in-house secondary surface finishing capabilities:
Full-Body Color
Pantone Color Matching
Liquid resins are custom-pigmented before degassing to match exact Pantone, RAL, or physical customer color chips, delivering scratch-resistant through-body pigmentation.
Texture Clone
Mold-Tech Texture Replication
Silicone replicates the exact texture applied to the master pattern—including high-gloss mirror finishes, fine spark EDM grains, and authentic Mold-Tech leatherette textures (MT-11000).
High Gloss
Optical Polishing & Clear Coats
Water-clear PU resins (PC/PMMA-like) achieve optical clarity via SPI A-1 master mold replication, precision diamond hand-finishing, and UV-resistant protective clear coatings to achieve crystal-clear optical light transmission.
EMI / Graphics
Painting & Pad Printing
We provide soft-touch matte painting, silk screening, precision pad printing for logos/legends, and conductive copper/nickel paints for internal EMI/RFI shielding.
4. Cross-Industry Applications: High-Fidelity Pre-Series Prototypes
Vacuum casting is the preferred manufacturing solution for clinical user trials, pilot testing, marketing focus groups, and bridge production:
Automotive
Automotive & Mobility
Air conditioning ducting, dashboard bezels, interior consoles, lighting lenses, and fluid reservoir prototypes. See our
automotive components solutions.
Medical
Medical Devices & Diagnostics
Handheld surgical tool prototypes, diagnostic console bezels, wearable monitors, and prosthetic test sockets. Explore our
medical device capabilities.
Consumer
Electronics & Appliances
High-gloss smart speaker housings, ruggedized tool enclosures, remote control bezels, and snap-fit assemblies. Explore
electronics enclosures.
Aerospace
Aerospace & Defense
Lightweight ventilation ducts, specialized cockpit control housings, and flame-retardant (UL94-V0) avionics enclosures. Explore
aerospace manufacturing.
5. Process Selection: Vacuum Casting vs. 3D Printing vs. Injection Molding
Choosing the optimal manufacturing technology depends on part quantity, mechanical requirements, surface cosmetic needs, and upfront budget:
1 – 5 Units
3D Printing (SLA / SLS / MJF)
Fast Single Parts
Ideal for 1 to 5 one-off conceptual prototypes with complex internal geometries. Zero tooling investment required, but per-unit cost remains high for multiple copies, and parts exhibit minor layer line textures.
10 – 100 Units
Vacuum Casting (Polyurethane)
The Pre-Series Sweet Spot
The optimal bridge process for 10 to 100 parts. Low silicone tooling investment, rapid 7 to 12 business days ex-factory turnaround, isotropic mechanical performance, and injection-mold quality surface finishes.
500 – 100k+ Units
Plastic Injection Molding
Mass Production Scale
Engineered for high-volume serial production. Requires substantial steel tooling investment and 18–35 business days (about 4–7 weeks) lead time, but delivers the lowest per-part cost for large manufacturing runs.
Engineering Process Comparison: Polyurethane Vacuum Casting vs. 3D Printing vs. Injection Molding| Decision Parameter | 3D Printing (SLA / SLS / MJF) | Polyurethane Vacuum Casting | Rapid Injection Molding |
|---|
| Optimal Production Volume | 1 – 10 pieces | 10 – 100 pieces (Pre-Series Bridge) | 500 – 100,000+ pieces |
| Tooling Medium & Lifespan | Zero Tooling (Direct CAD Build) | RTV-2 Silicone Mold (15 – 25 shots / cavity) | 7075-T6 Al / P20 / H13 Steel (5,000 – 1M+ shots) |
| Upfront Tooling Investment | None | Very Low (Fraction of Metal Tooling) | Moderate to High Capital Investment |
| Ex-Factory Lead Time | 4 – 8 Business Days | 7 – 12 Business Days | 18 – 35 Business Days (T1 Sample) |
| Mechanical Isotropicity & Finish | Anisotropic layer lines (requires sanding) | 100% Isotropic; clones SPI A-1 / MT-11010 | 100% Native Thermoplastic Resins |
6. Frequently Asked Questions (FAQ)
What is the typical lifespan of a silicone mold in vacuum casting?+
A high-quality RTV silicone mold typically yields 15 to 25 parts before the silicone degrades due to chemical attack from aggressive polyurethane resins and thermal curing cycles. For parts molded in abrasive or rigid resins, mold life is approximately 15 to 20 shots, while softer elastomeric resins allow up to 25 shots per cavity.
What dimensional tolerances can be achieved on vacuum cast polyurethane parts?+
Standard vacuum casting tolerances typically maintain ±0.15 mm per 100 mm (or ±0.0015″ per inch), depending on the master pattern and resin shrinkage. Achieving tight tolerances depends heavily on the precision of the master pattern (SLA or CNC machined) and controlled thermal degassing cycles.
How does polyurethane vacuum casting compare to 3D printing in mechanical performance?+
Unlike 3D printed parts which can exhibit anisotropic weakness along layer lines (Z-axis), vacuum cast parts are poured as a continuous liquid under vacuum, yielding 100% isotropic mechanical properties. Polyurethane formulations accurately mirror the tensile strength, impact resistance, and elongation of production thermoplastics like ABS, PP, and PC.
Can threaded inserts or metal hardware be cast directly into urethane parts?+
Yes. Brass knurled threaded inserts, stainless steel dowel pins, electronic bushings, and structural mounting hardware can be accurately positioned over locators inside the silicone mold prior to pouring. The liquid polyurethane encapsulates the insert during the vacuum cycle, creating strong, reusable threads that resist pull-out and torsional stripping.
Need Low-Volume Plastic Prototypes with Production Quality?
Bridge the critical gap between 3D printing and expensive steel injection molds. AS Prototypes delivers polyurethane vacuum casting parts in 7 to 12 business days with custom Pantone colors, high-gloss or Mold-Tech textures, and production-grade resins simulating ABS, PP, PC, and Shore 30A-90A rubber.
• Strict NDA Confidentiality• Bubble-Free Vacuum Degassing• Optical VMM & Mating Fit-Up Verification• 7–12 Day Ex-Factory Turnaround