Precision Manufacturing Facility & Machinery Fleet
AS Prototypes operates a modernized 5,000+ m² precision manufacturing facility in Shenzhen, China, adhering strictly to rigorous quality management standards. Our facility houses multi-axis CNC milling centers, multi-spindle Star Swiss-type screw lathes, Sodick linear wire EDM, Haitian Mars injection molding cells from 50 to 850 tons, and a dedicated 20°C ± 1°C climate-controlled metrology laboratory equipped with a high-precision Zeiss CNC coordinate measuring machine (CMM).
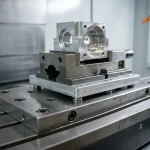
1. Multi-Axis CNC Milling & 5-Axis Simultaneous Machining Centers
Equipped with 3-axis, 4-axis direct-drive rotary tables, and 5-axis simultaneous trunnion centers from Brother, Fanuc, Mazak, and AFMING (Heidenhain CNC controls). We achieve high dynamic positioning and tight angular tolerances across complex aerospace brackets, medical enclosures, impellers, and heat sinks.
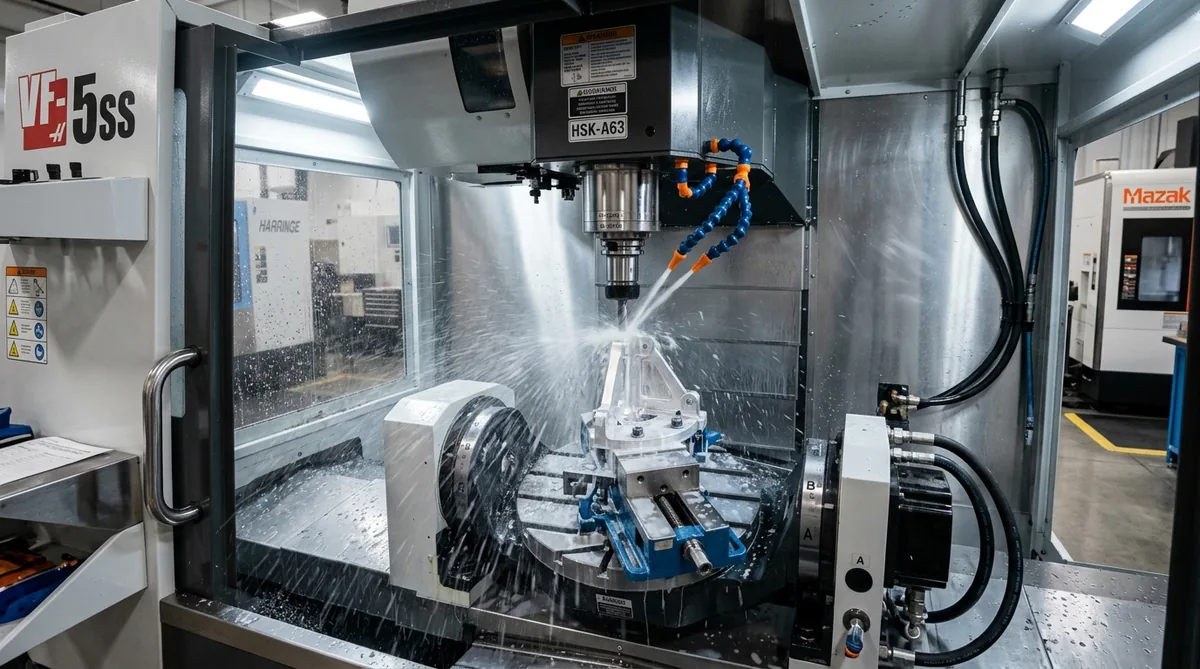
| Equipment Description | Brand / Builder | Model / Series | Working Travel (X / Y / Z) | Spindle & Control | Accuracy | Qty |
|---|---|---|---|---|---|---|
| 5-Axis Simultaneous Machining Center | AFMING / Topstar | GMU-400 | Table: Ø450 mm × 350 mm | 20,000 RPM (HSK-A63) / Heidenhain TNC | ±0.008 mm (Repeatability: ±0.004 mm) | 1 |
| High-Speed CNC Milling Center (BT30) | Brother (Japan) | Speedio W1000Zd2 | 1,000 × 500 × 380 mm | 16,000 RPM / CNC-C00 High Speed | ±0.008 mm | 2 |
| High-Speed CNC Tapping Center | Brother (Japan) | Speedio S700Zd1 | 700 × 400 × 300 mm | 16,000 RPM / 21-Tool ATC | ±0.008 mm | 5 |
| Precision Vertical Machining Center (4-Axis) | Fanuc (Japan) | Robodrill α-D21LiB5 | 700 × 400 × 330 mm | 24,000 RPM / Direct Drive 4th Axis | ±0.008 mm (Repeatability: ±0.004 mm) | 4 |
| Heavy-Duty Vertical Machining Center | Mazak (Japan) | VCN-530C | 1,050 × 530 × 510 mm | 12,000 RPM (CAT40) / Mazatrol SmoothG | ±0.008 mm (Repeatability: ±0.004 mm) | 2 |
2. Precision CNC Turning Centers & Star Swiss Micro-Machining Screw Lathes
Specialized in micro-turning and high-aspect-ratio shaft machining. Multi-axis STAR Swiss machines utilize synchronized sub-spindles, guide bushings, and live tooling stations to complete complex turned-and-milled parts in a single clamping setup with ±0.005 mm repeatability.
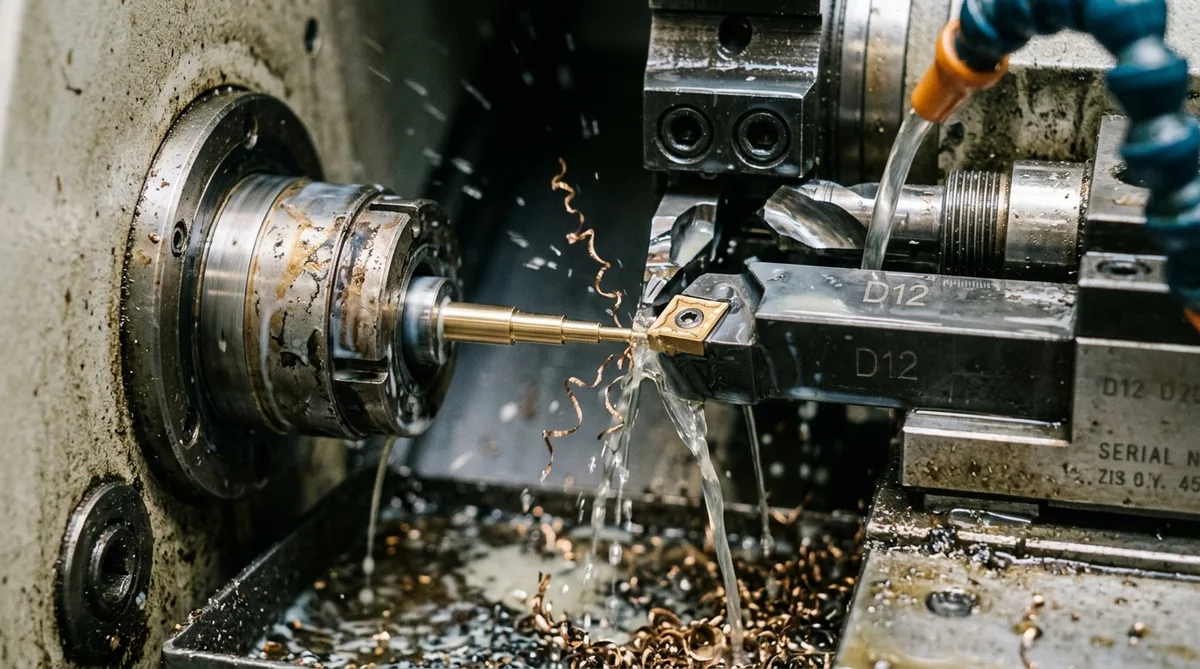
| Equipment Description | Brand / Builder | Model / Series | Bar Capacity / Envelope | Tooling & Sub-Spindle | Accuracy | Qty |
|---|---|---|---|---|---|---|
| Swiss-Type Micro-Turning Center | STAR Micronics (Japan) | BS-12-H | Max Bar: Ø12 mm | Dual Spindle + Live Cross Drill Stations | ±0.008 mm (Repeatability: ±0.004 mm) | 2 |
| Swiss-Type Screw Machine (7-Axis) | STAR Micronics (Japan) | SB-20R Type G | Max Bar: Ø20 mm | 7-Axis Sub-Spindle + Full C-Axis Indexing | ±0.008 mm (Repeatability: ±0.004 mm) | 2 |
| Swiss-Type High-Rigidity Screw Machine | STAR Micronics (Japan) | SB-23R | Max Bar: Ø23 mm | Guide Bushing / Non-Guide Convertible | ±0.008 mm (Repeatability: ±0.004 mm) | 2 |
| Precision CNC Turning Center | SYNTEC | T-46 Slant Bed | Max Turn: Ø300 × 550 mm | 8-Station Hydraulic Tool Turret | ±0.008 mm | 3 |
| High-Precision CNC Lathe | Takisawa (Japan) | TCC-2000 | Max Swing: Ø350 × 400 mm | Hydraulic Collet Chuck + Tailstock | ±0.008 mm (Repeatability: ±0.004 mm) | 2 |
3. Electrical Discharge Machining (EDM) & Ultra-Precision Grinding
Dedicated to hardened tool steels (HRC 55–65), tungsten carbide inserts, delicate keyways, and mirror surface finishes. Sodick linear motor wire EDM eliminates mechanical backlash, achieving Ra 0.2 μm finishes and sharp inside corners impossible with rotary tooling.
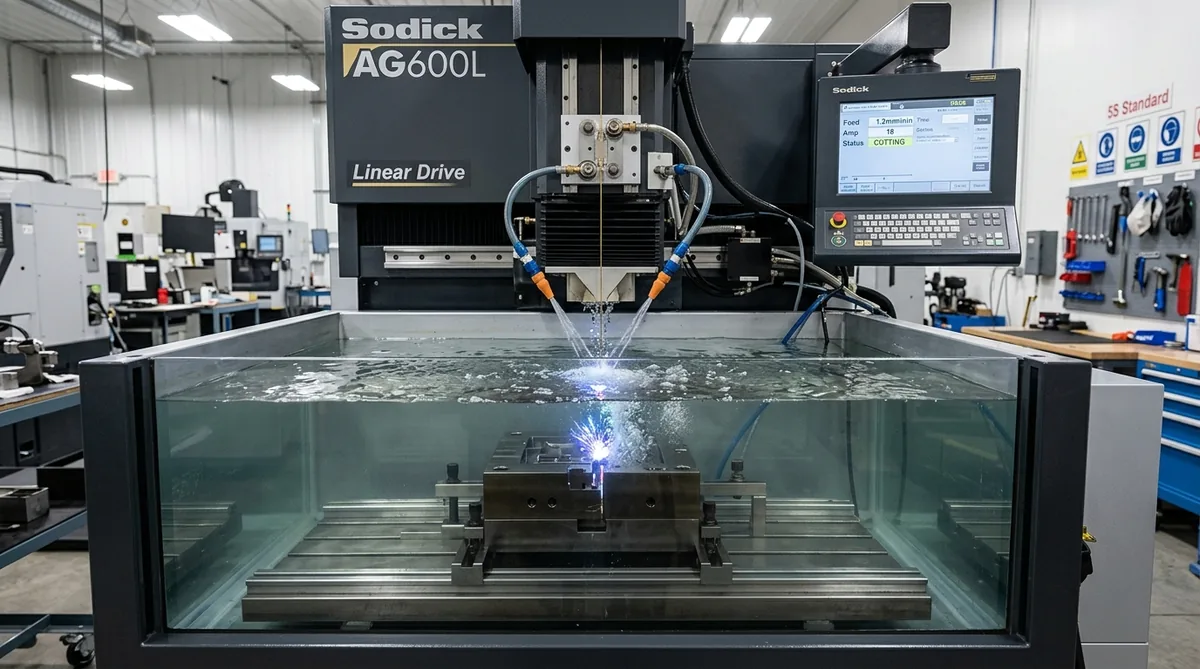
| Process / Equipment Type | Brand / Builder | Model / Series | Working Travel (X / Y / Z) | Technology & Wire | Accuracy / Finish | Qty |
|---|---|---|---|---|---|---|
| Linear Motor Wire Cut EDM | Sodick (Japan) | ALN400Qs | 400 × 300 × 250 mm | 0.10 – 0.25 mm Brass / Tungsten Wire | ±0.003 mm (Ra 0.2 μm) | 3 |
| High-Speed CNC Sinker EDM | Makino (Japan) | MGC3 / EDGE2 | 800 × 500 × 350 mm | High-Density Copper / Graphite Electrodes | ±0.005 mm (Ra 0.4 μm) | 1 |
| Ultra-Precision Surface Grinder | Okamoto (Japan) | AR-618S | 600 × 300 × 250 mm | Digital Micro-Downfeed 0.001 mm | ±0.005 mm (Ra 0.2 μm) | 2 |
| Precision Cylindrical Grinder | Palmary | ODC-3250 | Max Dia: Ø320 × 500 mm | Dead / Live Center Precision Grinding | ±0.005 mm (Cylindricity 2 μm) | 1 |
4. Rapid Tooling, Injection Molding Machines & Polyurethane Vacuum Casting
Comprehensive plastics fabrication ranging from silicone vacuum casting (10–50 units) to high-tonnage production injection molding. Haitian Mars servo-hydraulic presses cover a 50-ton to 850-ton clamping force fleet for precision consumer electronics, industrial housings, and automotive enclosures.
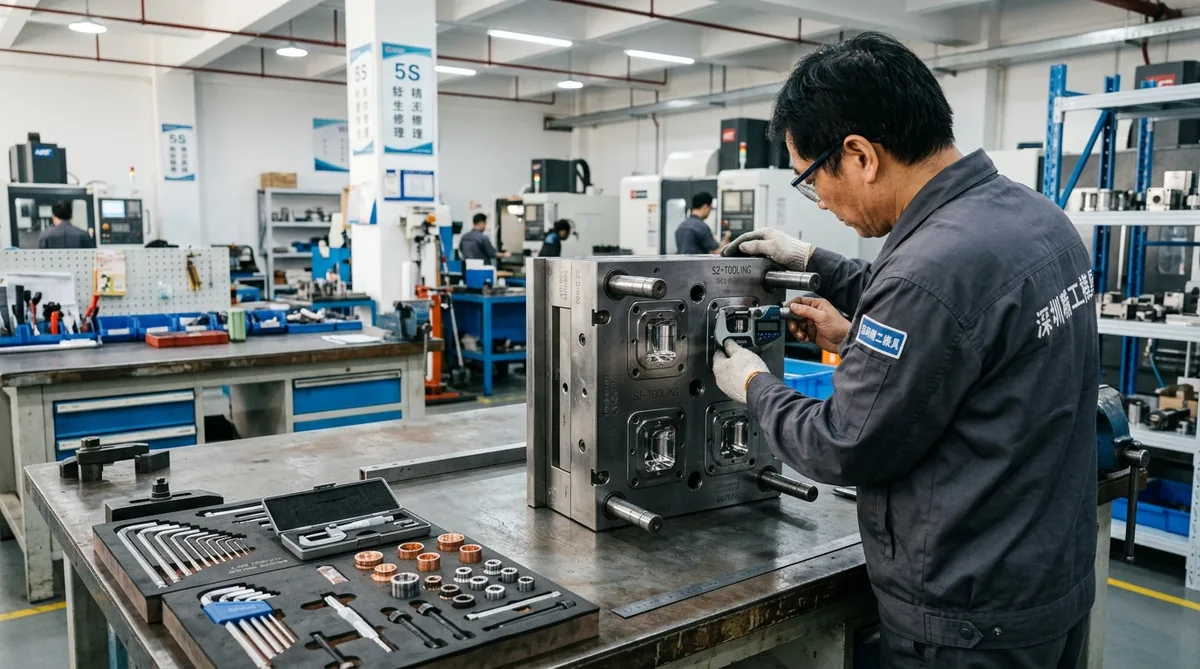
| Equipment Description | Brand / Builder | Model / Series | Clamping Force / Chamber Size | Shot Capacity / Thermal Control | Target Materials | Qty |
|---|---|---|---|---|---|---|
| Servo Hydraulic Injection Molding Machines | Haitian Plastics Machinery | Mars Series (High-Rigidity) | 50 Ton – 850 Ton Range | Shot Weight: 20g – 2,800g | ABS, PC, PA66, POM, PEEK, TPU | 10 |
| High-Temperature Mold Water Heaters | Shini (信易) | STM High-Temp Mold Water Controller | Dual Loop Temperature Module | PID Precision Heating up to 160°C | Tooling Temperature Stability | 1 |
| Industrial Water-Cooled Chillers | Shini (信易) | SIC Air/Water Industrial Chiller | Continuous Circulation Loop | Flow: 250 L/min at 7°C – 15°C | Cycle Time Optimization | 1 |
| Industrial Polyurethane Vacuum Casting System | AS Engineering Tech | VC-1500 Pro | Chamber: 1,500 × 800 × 800 mm | 0.5 mbar Dual High-Vacuum Degassing | PU Resins (ABS-, PC-, Rubber-Like) | 2 |
| Forced-Air Thermal Post-Curing Ovens | AS Thermal Systems | TO-1200 | Internal: 1,200 × 1,000 × 1,200 mm | Ambient to 200°C Uniform Airflow | Silicone Molds & PU Degassing | 2 |
5. Precision Sheet Metal Fabrication, Laser Cutting & CNC Bending Fleet
End-to-end sheet metal prototyping and enclosure fabrication. High-wattage 12kW fiber laser delivers clean dross-free edge profiles, paired with 160-ton CNC press brakes featuring hydraulic dynamic crowning for precision angle repeatability within ±0.1°.
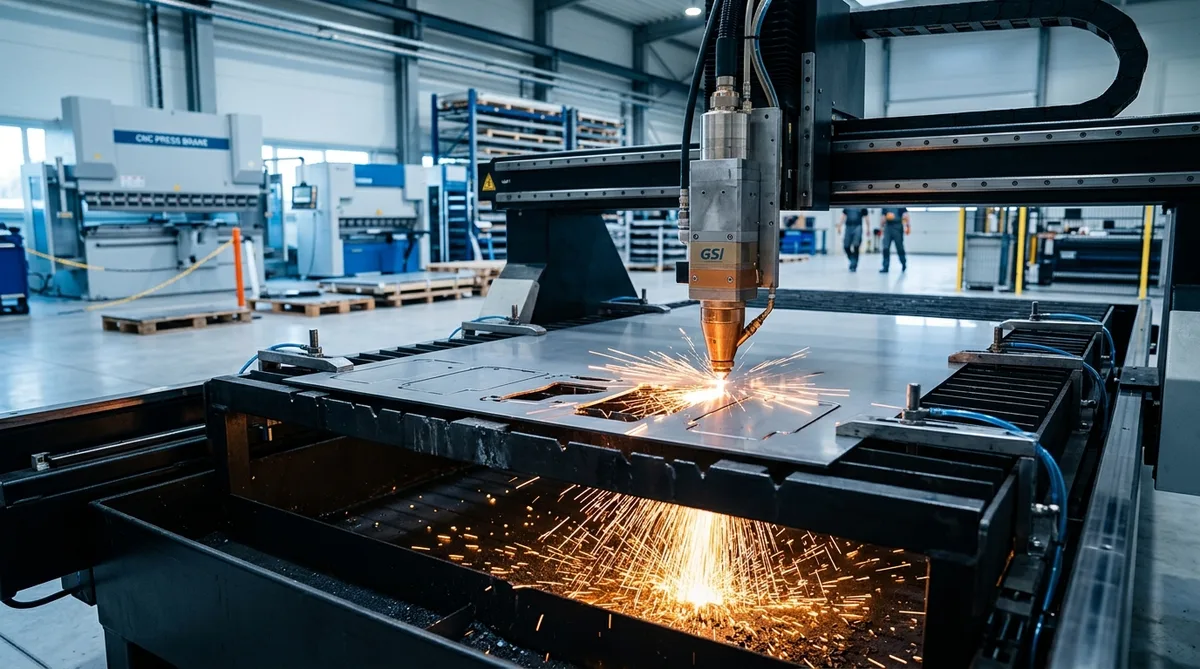
| Process / Equipment | Brand / Builder | Model / Specifications | Working Bed / Tonnage | Thickness Capacity | Accuracy | Qty |
|---|---|---|---|---|---|---|
| High-Power CNC Fiber Laser Cutter | Bodor / Han’s Laser | 12,000W / 6,000W Dual Shuttle | 3,000 × 1,500 mm | Steel: 25 mm, SS: 20 mm, Al: 16 mm | ±0.03 mm | 1 |
| CNC Electro-Hydraulic Press Brake | Amada Type / Delem CNC | 160-Ton Multi-Axis CNC | Max Bending Length: 3,200 mm | Dynamic CNC Crowning Compensation | Angle: ±0.1° | 2 |
| Hydraulic Guillotine Shearing Machine | Yangli | QC12Y Heavy Duty | Max Cut: 3,200 mm Width | Max Sheet Thickness: 6.0 mm | ±0.10 mm | 1 |
| Automatic Deburring & Edge Rounding | Timesavers Type | Dual Wide Belt + Rotary Brushes | Passage Width: 1,000 mm | Consistent Slag Removal & Edge Break | Uniform R0.5 – R1.5 | 2 |
6. Industrial Additive Manufacturing (SLA Resins, SLS Nylon, HP MJF & DMLS Metal 3D Printing)
Direct additive manufacturing for rapid concept proof, airflow manifolds, and conformal-cooled metal tooling. Large-frame SLA printers build master visual models, HP Multi Jet Fusion (MJF) and SLS systems produce dense functional nylon parts, paired with automated chemical vapor smoothing for injection-grade surface sealing, while dual-laser DMLS machines sinter dense aerospace titanium, nickel alloys, and stainless steels.
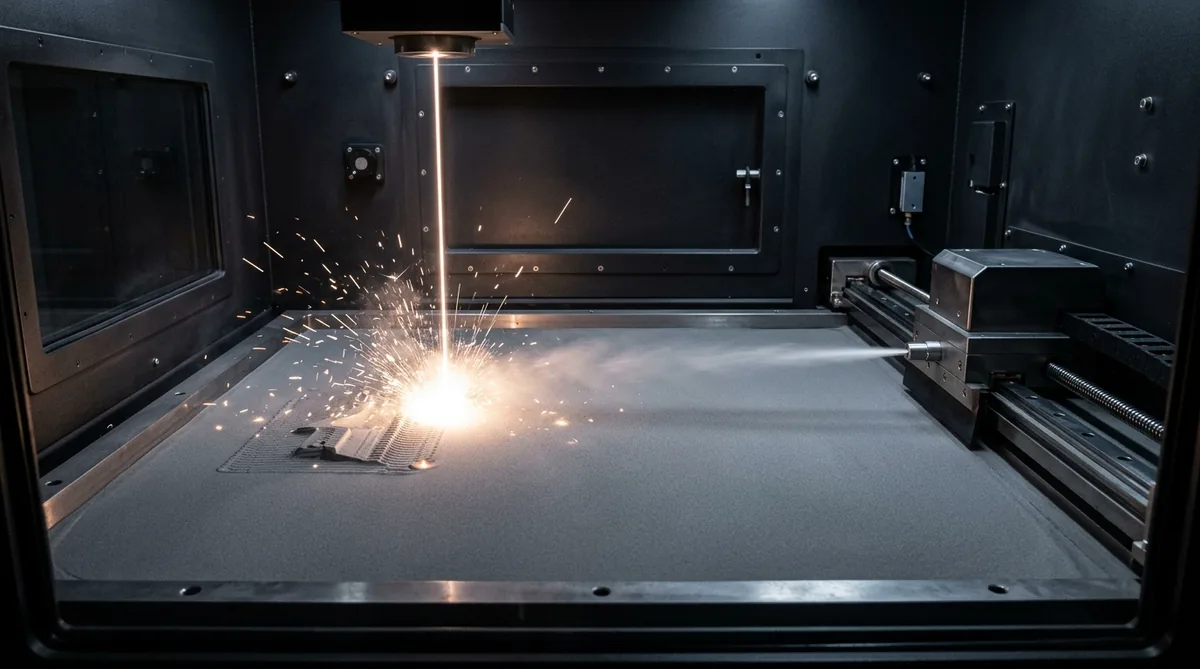
| Additive Technology | Brand / Builder | Model / Series | Build Volume (X / Y / Z) | Layer Pitch / Resolution | Compatible Materials | Qty |
|---|---|---|---|---|---|---|
| Industrial Stereolithography (SLA) | Kings / UnionTech | SLA-800 Pro | 800 × 800 × 550 mm | 0.05 mm – 0.10 mm | Tough White Resin, Clear Transparent Resin, High-Temp Resin | 4 |
| HP Multi Jet Fusion (MJF) | HP (Hewlett-Packard) | MJF 5200 / 4200 | 380 × 284 × 380 mm | 0.08 mm (80 μm) | PA12 Nylon, PA11, Flexible TPU Elastomer | 2 |
| Selective Laser Sintering (SLS) | TPM3D / Farsoon | SLS-400 P Series | 400 × 400 × 450 mm | 0.08 mm – 0.12 mm | PA12 (Nylon 12), PA12-GF (Glass-Filled), Flexible TPU | 2 |
| Direct Metal Laser Sintering (DMLS / SLM) | Eplus3D / HBD | SLM-280 Dual Laser | 280 × 280 × 365 mm | 0.02 mm – 0.05 mm | Titanium Ti6Al4V, Stainless 316L, AlSi10Mg, Inconel 718 | 1 |
| Automated Chemical Vapor Smoothing | AMT / PostPro | Vapor Smoothing Cell | Chamber: 600 × 400 × 400 mm | Closed-Loop Solvent Flow | PA12, TPU, ABS Sealing & Injection-Grade Finish | 1 |
| Stratasys / Intamsys | Industrial FDM / FFF (Fortus 450mc / FUNMAT PRO 410) | 406 × 355 × 406 mm | ±0.127 mm (or ±0.0015 mm/mm) | ABS-M30, PC-10, ASA, PA-CF, ULTEM 9085 | 2 Units |
7. Quality Assurance & Metrology Inspection Laboratory (20°C ± 1°C Cleanroom)
Our dedicated metrology cleanroom operates under 24/7 positive pressure and 20°C ± 1°C thermal regulation. Utilizing Zeiss CNC coordinate measuring machines, optical comparators, and calibrated electronic height gauges, we provide comprehensive dimensional verification and Comprehensive First Article Inspection (FAI) reports.
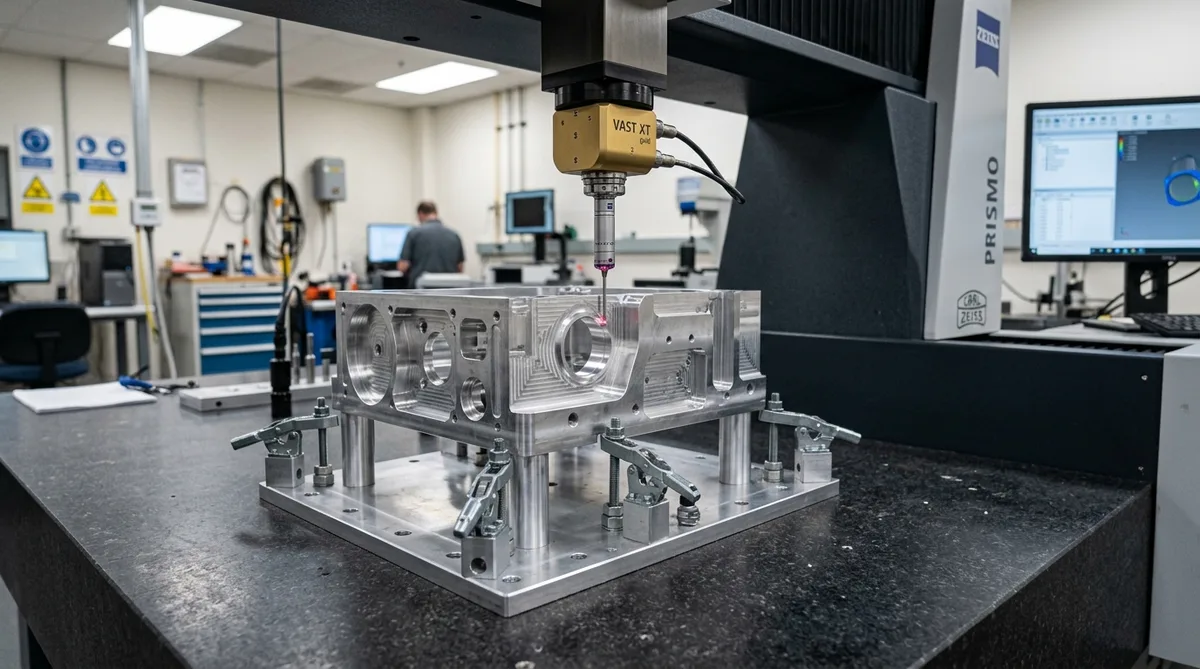
| Inspection Instrument | Brand / Builder | Model / Series | Measuring Range | Resolution & Accuracy | Inspection Scope | Qty |
|---|---|---|---|---|---|---|
| 3D CNC Coordinate Measuring Machine (CMM) | Zeiss (Germany) | Contura / PRISMO | 800 × 1,000 × 600 mm | E0 = 1.5 + L/350 μm (±0.0015 mm) | Full 3D GD&T, true position, CAD model comparison | 1 |
| 2.5D Optical Video Measuring System (VMS) | VMS Metrology | 4060 / 4030F Sensor | 400 × 650 mm Glass Stage | ±0.003 mm Optical Resolution | Micro-hole pitch, small stamping profiles, non-contact 2D | 2 |
| Precision Profile Projector / Optical Comparator | ESSON Optics | EP-1 System | 200 × 100 mm Screen View | ±0.005 mm Screen Magnification | Thread root radius, gear teeth profiles, chamfer verification | 2 |
| High-Precision Electronic Height Gauge | TESA (Switzerland) | Micro-Hite 700 | Max Height: 700 mm | ±0.002 mm Heidenhain Glass Scale | Step height, bore centerline, flatness reference checking | 1 |
| Digital Display Height Gauge | Mitutoyo (Japan) | HDS-H30C Digimatic | Max Height: 180 / 300 mm | ±0.005 mm Digital Readout | Granite plate workshop inspection and machine set-up | 1 |
| Digital Rockwell Hardness Tester | Qicheng Instruments | A016 Digital Indenter | HRA, HRB, HRC up to 80 HRC | ±0.5 HRC Diamond Cone | Heat treat quenching, tempering, and case hardening validation | 1 |
| Portable Surface Roughness Tester | Mitutoyo (Japan) | Surftest SJ-210 | Ra, Rz, Rq down to 0.01 μm | Diamond Tip Stylus (2 μm radius) | Machined, ground, polished, and bead blasted finish verification | 2 |
Shopfloor 5S Discipline & Metrology Calibration Protocols
Dimensional accuracy and toolpath repeatability rely on disciplined shopfloor climate management, scheduled instrument calibration, and standardized first-article inspection procedures across every single production batch.
Cleanroom Metrology Environment
Our dedicated CMM inspection lab is isolated with pneumatic vibration dampers, positive air pressure, and constant thermal regulation at 20°C ± 1°C (45–60% RH) to eliminate thermal expansion measurement discrepancies.
Scheduled Calibration Rigor
All granite surface plates, digital micrometers, bore gauges, optical scales, and CMM ruby styli undergo semi-annual independent calibration traceable to CNAS and NIST national metrology benchmarks.
First Article Inspection (FAI)
Every production run requires senior QC sign-off on the first off-tool component before batch release. Full ballooned engineering drawings and Dimensional FAI inspection reports are available upon request.
Raw Material Traceability
Raw metal ingots, bar stock, and sheet plates are verified against authentic Mill Test Reports (MTR) with chemical composition and mechanical tensile verification to prevent material substitution.
Frequently Asked Questions Regarding Factory Capacity & Machinery
Technical specifications, facility auditing options, and lead times for prototype and production manufacturing.
Can prospective clients or independent inspectors audit the AS Prototypes facility?
Yes, absolutely. We welcome on-site client audits and independent inspection agencies (SGS, TÜV, Bureau Veritas) at our Shenzhen facility. We also provide real-time video facility walkthroughs and live CMM inspection demonstrations for overseas procurement teams.
What are the maximum and minimum part dimensions your equipment can fabricate?
Our multi-spindle Star Swiss screw machines fabricate micro-components as small as Ø0.5 mm in diameter, while our large-bed CNC milling centers and laser cutters handle plate components up to 3,000 × 1,500 mm. Injection molded components are supported by our 50-ton to 850-ton clamping press fleet.
How do you prevent machine drift and maintain tight tolerances during 24/7 continuous operation?
All critical machines feature optical linear glass scales and thermal spindle compensation. Machinists use Renishaw in-situ touch probes to re-datum fixtures and check tool wear regularly, ensuring sustained ±0.005 mm repeatability across multi-day runs.
How fast can AS Prototypes set up tooling and machine expedited prototype parts?
We reserve dedicated high-speed machining centers and Swiss lathes for agile prototyping. Following engineering CAD review and DFM feedback within 24 hours, rapid prototype parts are machined and inspected within 4 to 8 business days, then dispatched via international express air courier (DHL/FedEx/UPS, 3–5 business days transit).
Put Our Advanced Machinery Fleet to Work on Your Next Precision Project
Upload your 3D CAD models (STEP, IGES, X_T, SLDPRT) and 2D engineering drawings. Our senior tooling and machining engineers will evaluate toolpaths, clamping setups, and provide an itemized quotation with actionable DFM feedback within 12–24 hours.