Metal 3D Printing Services: Precision DMLS & SLM Components
At AS Prototypes, our metal 3D printing services combine dual-laser Direct Metal Laser Sintering (DMLS) and Selective Laser Melting (SLM) under inert argon with vacuum stress relief. Integrating conformal cooling channels and cellular lattice structures with in-house Computer Numerical Control (CNC) machining and Wire Electrical Discharge Machining (EDM), we deliver flight-ready metal hardware.
DMLS & SLM Metal 3D Printing Working Principle
Direct Metal Laser Sintering (DMLS) and Selective Laser Melting (SLM) are Laser Powder Bed Fusion (PBF-LB/M) processes where high-power ytterbium fiber lasers scan 20–50 μm (0.0008″–0.0020″) cross-sections into pre-alloyed metal powder, melting particles into a >99.7% dense crystal lattice.
- Inert Argon Atmospheric Control: Oxygen levels in the build chamber are maintained below 100 ppm using continuous argon purge, preventing reactive oxidation and preserving metallurgical purity for titanium and nickel superalloys.
- Full Metallurgical Melting (>99.7% Density): Complete liquid-phase laser melting delivers tensile, yield, and fatigue strength comparable to forged and wrought alloys. Note on Directional Anisotropy: Layer-by-layer epitaxial solidification produces directional anisotropy, with Z-axis tensile elongation typically 10–15% below the XY build plane. Our engineering team aligns primary tensile loads along XY during Design for Additive Manufacturing (DfAM) slicing and offers vacuum solution aging or optional Hot Isostatic Pressing (HIP) for isotropic fatigue resistance.
- Topology Optimization & Generative Design: Build organic weight-reduced structures, internal fluid passages, and curved conformal cooling cores free of cutter-reach or fixture constraints.
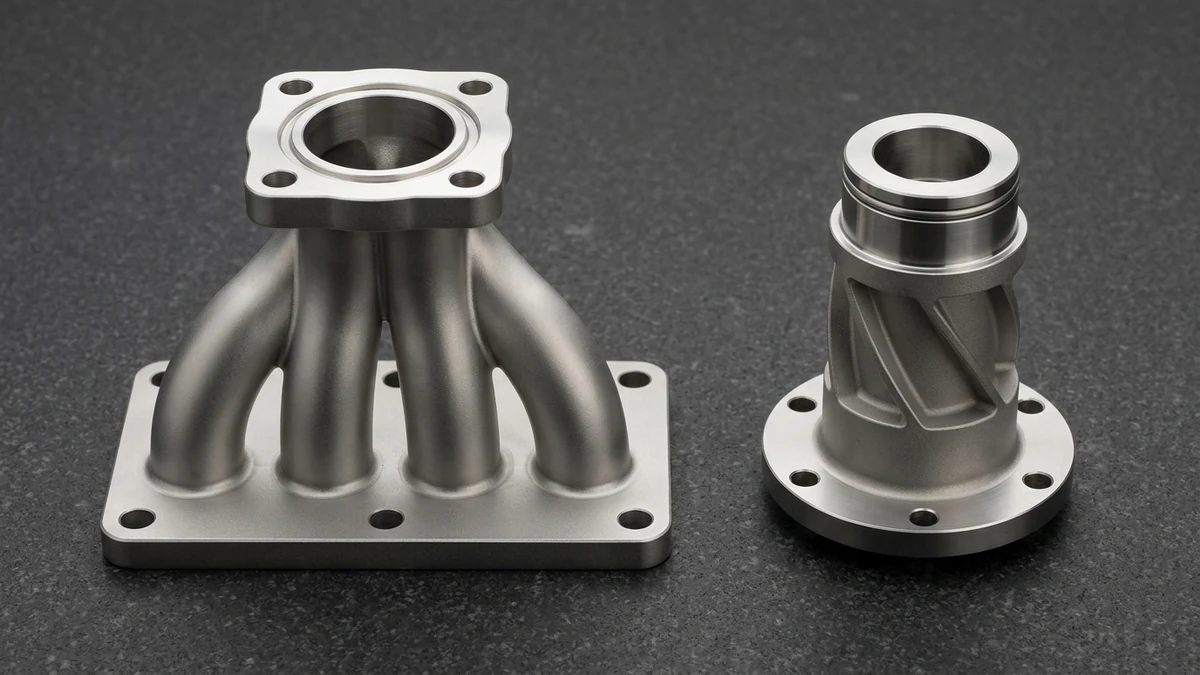
- Component Consolidation: Merge 10–30 sub-components, braze joints, and fasteners into one monolithic body—as shown on the DMLS 316L stainless 4-into-1 collector manifold and Inconel 718 helical swirl injector nozzle alongside—eliminating fluid leak paths.
DMLS / SLM Metal 3D Printing Alloys & Mechanical Specifications
| Metal Alloy | Standard & Spec | Tensile & Yield (MPa / ksi) | Hardness & Density | Thermal & Chemical | Recommended Application |
|---|---|---|---|---|---|
| Titanium Ti-6Al-4V (Gr 5 / Gr 23) | ASTM F2924 / F3001 | Tensile: 1,150 MPa (167 ksi) Yield: 1,000 MPa (145 ksi) | 36 HRC >99.7% Density | Biocompatible, corrosion-resistant up to 400°C | Aerospace structural brackets, orthopedic bone plates, motorsport suspension links |
| Aluminum AlSi10Mg | ASTM F3318 / EN AC-43000 | Tensile: 400 MPa (58 ksi) Yield: 260 MPa (38 ksi) | 110 HBW >99.6% Density | High thermal conductivity (130–150 W/m·K), 2.67 g/cm³ | Conformal heat sinks, cold plates, lightweight drone arms, automotive intake manifolds |
| Stainless Steel 316L | ASTM F3184 / A276 | Tensile: 650 MPa (94 ksi) Yield: 500 MPa (73 ksi) | 220 HV >99.8% Density | High acid & chloride resistance, cryogenic stability | Marine fluid manifolds, food & pharmaceutical nozzles, subsea chemical valve bodies |
| Precipitation Hardening 17-4PH | ASTM F3049 / A564 (H900) | Tensile: 1,250 MPa (181 ksi) Yield: 1,100 MPa (160 ksi) | 38–44 HRC >99.7% Density | High fatigue endurance, magnetic, precipitation hardenable | Aerospace structural fittings, surgical cutters, high-pressure pump shafts, splined hubs |
| Nickel Superalloy Inconel 718 | ASTM F3055 / AMS 5662 (Aged) | Tensile: 1,380 MPa (200 ksi) Yield: 1,100 MPa (160 ksi) | 42–47 HRC >99.6% Density | Oxidation & creep resistant up to 700°C (1,290°F) | Rocket engine combustion chambers, turbine exhaust rings, swirl injectors, downhole tools |
| Maraging Tool Steel MS1 (1.2709) | DIN 1.2709 (18Ni-300, Aged) | Tensile: 1,950 MPa (283 ksi) Yield: 1,850 MPa (268 ksi) | 50–54 HRC >99.8% Density | Polishable to SPI A-2 (Ra ≤ 0.05 μm), superior thermal fatigue resistance | Plastic injection mold cores with curved conformal cooling channels, zinc die-casting inserts |
| Integrated Post-CNC Finishing | As-printed layer thickness spans 20–50 μm with stress-relieved linear accuracy of ±0.10 mm (±0.004″) or ±0.2% (whichever is greater). In-house 3-axis and 4-axis CNC milling, simultaneous 5-axis contour machining, and Sodick wire EDM finish critical sealing faces and bores to ±0.010 mm (±0.0004″) (±0.005 mm / ±0.0002″ on wire EDM and ground features; ISO 2768-mK general machined features) with Ra 0.8–1.6 μm milled finish (Ra 0.2–0.4 μm on EDM/ground faces) and ISO 6H gauge-verified tapped threads. | ||||
Technology Comparison: DMLS/SLM vs. Metal Binder Jetting
Direct Metal Laser Sintering (DMLS / SLM)
High Performance
Complete laser-induced melting inside an inert argon chamber delivers full metallurgical density (>99.7%) and immediate structural load-bearing performance.
- Mechanical Density: >99.7% (matches wrought metallurgical integrity).
- Ideal Materials: Ti-6Al-4V, Inconel 718, AlSi10Mg, 316L, 17-4PH, MS1 Tool Steel.
- Best For: High-stress aerospace brackets, conformal-cooled mold cores, orthopedic implants, and turbomachinery.
- Shrinkage Control: Zero furnace sintering shrinkage; dimensions are locked during laser fusion.
- When to Avoid DMLS: Simple 2.5D prismatic blocks, flat plates, or solid shafts without internal channels are faster and more economical via direct billet CNC machining.
Metal Binder Jetting & Sintering
Batch Economics
A liquid bonding agent is jetted into loose metal powder to form green-state parts that are subsequently debound and furnace-sintered or bronze-infiltrated.
- Mechanical Density: 95%–97% sintered density (or bronze-infiltrated composite matrix).
- Ideal Materials: 420 stainless steel infiltrated with bronze, 316L, tungsten heavy alloys.
- Best For: Medium-to-high volume runs of small non-flight hardware, decorative fixtures, and light-duty wear parts.
- Shrinkage Factor: Undergoes 15%–20% linear shrinkage (~40%–50% volumetric) during furnace sintering, causing slumping on unsupported spans.
In-House Post-Processing & Secondary CNC Precision Machining
Laser fusion is only half the workflow. In our in-house manufacturing facility, metal 3D-printed blanks move directly into thermal stabilization, subtractive datum finishing, and metrology verification:
- Vacuum Stress-Relief Heat Treatment: While still fused to the steel or titanium build plate, builds undergo controlled vacuum furnace annealing to relieve internal thermal tension and prevent springback distortion.
- Sodick Wire EDM Cut-Off: Linear-motor wire EDM cleanly severs stress-relieved parts from the sacrificial build platform without inducing mechanical clamping distortion.
- Secondary CNC Datum Machining: Mating flanges, bearing bores, and dowel holes are finished to ±0.010 mm (±0.0004″) and threads rigid-tapped to ISO 6H on Brother, Fanuc, and Mazak 3-axis/4-axis vertical machining centers (VMCs), with AFMING GMU-400 5-axis machining reserved for multi-angle contours and wire EDM holding ±0.005 mm.
- Surface Refinement & Media Blasting: Ceramic micro-bead blasting (Ra 6.0–9.0 μm), centrifugal vibro-tumbling (Ra 2.5–4.0 μm), and ASTM B912 electropolishing (Ra 0.8–1.6 μm) refine printed textures. Explore our metal surface finishing solutions.
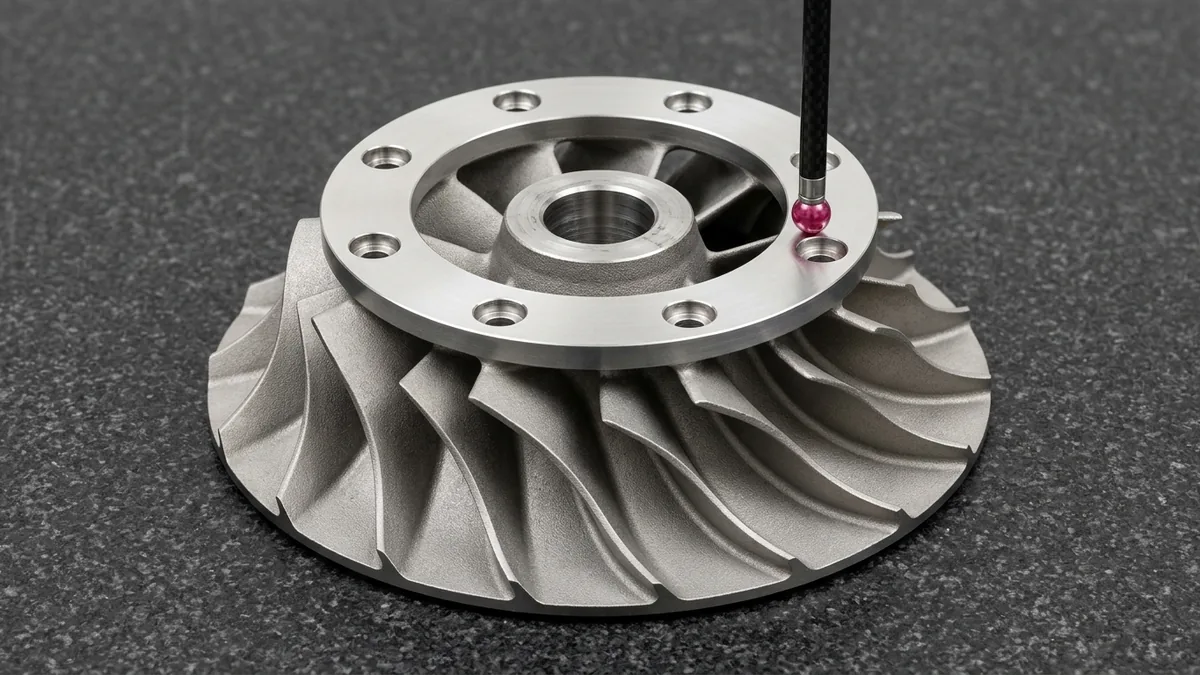
- 20°C Zeiss CMM Inspection (Upon Request): Our 20°C ± 1°C metrology laboratory performs tactile Zeiss Coordinate Measuring Machine (CMM) Geometric Dimensioning and Tolerancing (GD&T) verification and First Article Inspection (FAI) reporting on CNC-machined datum features—such as the Ti-6Al-4V radial impeller datum ring shown alongside.
Target Industry Solutions & Mission-Critical Applications
Rocket engine combustion chambers, turbopump impellers, satellite optical brackets, and conformal fuel manifolds in Inconel 718 and Ti-6Al-4V. Explore our aerospace manufacturing solutions.
Patient-matched titanium cranial plates, trabecular spinal cages with controlled osseointegration porous lattices, and ergonomic surgical cutters. See our medical device capabilities.
Custom titanium exhaust collectors, topology-optimized upright knuckles, high-efficiency brake calipers, and lightweight EV motor cooling sleeves. Review our automotive parts service.
Maraging tool steel mold core inserts featuring curved conformal cooling passages that track complex mold contours, cutting injection molding cycle times by 20%–40%. Learn about our injection mold tooling.
Design for Additive Manufacturing (DfAM): 8-Point DMLS/SLM Metal Rules
Designing specifically for laser powder bed fusion melt-pool metallurgy prevents recoater blade collisions, minimizes sacrificial metal support removal, and establishes rigid datum surfaces for secondary CNC finish milling:
| Metallurgical & CAD Feature | Minimum Threshold | Preferred CAD Target | Melt-Pool Thermal Physics & Hybrid CNC Strategy |
|---|---|---|---|
| 1. Self-Supporting Overhang Angle | ≥ 45° from Build Plate | 45° – 60° Self-Supporting Slopes | Downward-facing metal surfaces below 45° require dense metal anchor supports to conduct laser heat into the build plate and prevent dross curling. |
| 2. Internal Conformal Channels | ≥ Ø1.5 mm Circular | Teardrop or Diamond Profile > Ø3.0 mm | Horizontal circular passages above Ø6.0 mm sag at the top crown; converting cross-sections to self-supporting 45° teardrop crowns eliminates internal supports. |
| 3. Minimum Structural Wall & Fins | ≥ 0.50 mm (0.020″) | 1.00 – 2.50 mm (Aspect Ratio ≤ 8:1) | Tall, thin heat-exchanger fins under 0.6 mm can deflect under residual thermal tension and trigger steel or ceramic recoater blade crashes. |
| 4. Unmelted Powder Escape Ports | ≥ 2 Holes × Ø3.0 mm | ≥ 2 Holes × Ø5.0 mm (Line-of-Sight) | Ensure smooth internal fillet radii and opposing flush ports so dense atomized titanium, Inconel, or steel powder can be vibrated and vacuumed out. |
| 5. Secondary CNC Machining Stock | +0.50 mm per Face | +0.80 to +1.20 mm on Datum Faces/Bores | Add machining stock to all O-ring grooves, bearing journals, and flange faces destined for ±0.010 mm 3/4/5-axis CNC finish milling. |
| 6. CNC Workholding Datum Lugs | 3 Coplanar Clamping Pads | Sacrificial Parallel Dovetail / Vise Tabs | Organic topology-optimized brackets cannot be gripped in a standard precision machine vise; adding sacrificial parallel clamping tabs simplifies 3-axis/4-axis CNC setup. |
| 7. Root Fillets & Section Transitions | R ≥ 1.0 mm Internal Fillets | R ≥ 1.5 – 3.0 mm Gradual Transitions | Abrupt transitions from thin lattice struts to heavy solid bosses create steep thermal gradients that can crack during rapid laser solidification. |
| 8. Threaded Holes & Precision Bores | Print Pilot Bore Only | Ream & Rigid-Tap Post-Print (ISO 6H) | Never rely on as-printed DMLS threads for structural bolts; print undersized pilot holes and rigid-tap or thread-mill after vacuum stress relief. |
4-Level DMLS Metal Finishing Grades & Ex-Factory Lead Time Schedule
Specify your finishing tier during Request for Quotation (RFQ) review. All schedules below represent Ex-Factory Production & Inspection Turnaround (excluding 3–5 days international air transit via DHL/FedEx/UPS):
| RFQ Finishing Tier | Post-Processing & Machining Scope | Surface Roughness (Ra) | Feature Tolerance | Ex-Factory Lead Time |
|---|---|---|---|---|
| Level 1: Stress-Relieved & Media-Blasted | Vacuum stress relief + Sodick wire EDM plate cut-off + support removal + ceramic micro-bead blasting | Ra 6.0 – 9.0 μm (240–350 μin) | ±0.10 mm (±0.004″) or ±0.2% | 5 – 8 Business Days |
| Level 2: Vibro-Tumbled Isotropic | Level 1 + high-energy centrifugal/rotary ceramic media tumbling for uniform edge radiusing and smoother flow surfaces | Ra 2.5 – 4.0 μm (100–160 μin) | ±0.10 mm (±0.004″) or ±0.2% | 7 – 10 Business Days |
| Level 3: Hybrid Additive + CNC Datums | Level 1/2 + precision 3/4/5-axis CNC finish milling of sealing flanges, bearing bores, and ISO 6H tapped threads + Zeiss CMM report | Ra 0.8 – 1.6 μm (Machined Faces) | ±0.010 mm (±0.0004″) (CNC Datums) | 7 – 12 Business Days |
| Level 4: Ground & Mold-Polished Core | Maraging steel MS1 age-hardening (50–54 HRC) + wire EDM / Okamoto grinding + fine stone/abrasive cavity polish (optional SPI A-2 diamond buff, Ra ≤ 0.05 μm) | Ra 0.1 – 0.4 μm (SPI B-2 to C-2) | ±0.005 mm (±0.0002″) (EDM / Ground) | 10 – 15 Business Days |
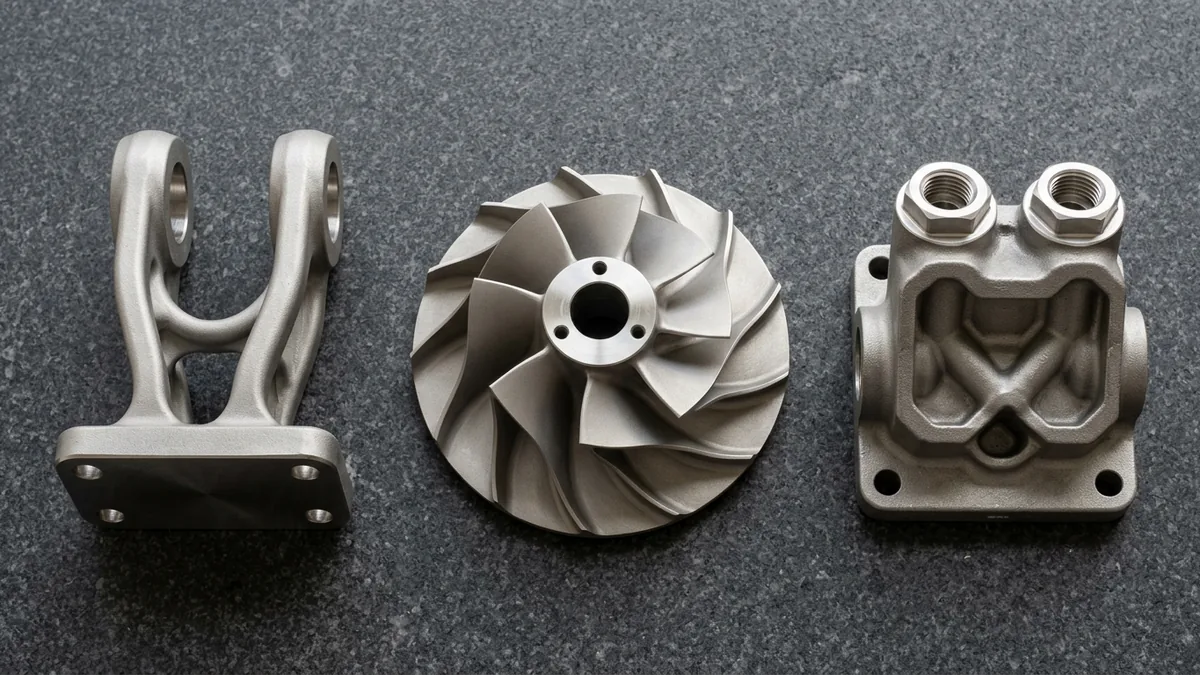
Level 3 hybrid finishing pairs matte bead-blasted organic struts with bright CNC-milled mounting datums, precision-reamed shaft bores, and threaded hex-collar fluid ports—as demonstrated on the Ti-6Al-4V clevis bracket, Inconel 718 turbine impeller, and 316L stainless hydraulic manifold below.
Frequently Asked Questions (FAQ)
Q1: How does DMLS metal 3D printing compare to CNC machining?
Q2: Are metal 3D printed parts as strong as billet or cast metal parts?
Q3: Why is post-print stress-relief heat treatment necessary for DMLS parts?
Q4: What surface roughness can be achieved on metal 3D printed parts?
Ready to Build Production-Grade Metal 3D Printed Parts?
Upload your 3D CAD models (STEP / IGES) and 2D tolerance drawings for a complimentary Design for Additive Manufacturing (DfAM) review, build-orientation analysis, and hybrid CNC datum-locking quotation from our in-house engineering team.