Electronic Appliance CNC Machining & Device Enclosures
Our in-house electronic appliance CNC machining facility fabricates custom 6061-T6 unibody enclosures, skived C11000 copper heatsinks, Electromagnetic Interference (EMI) shields, and overmolded housings. Using Computer Numerical Control (CNC) milling, Star Swiss turning, and bridge tooling, we scale hardware through Engineering, Design, and Production Verification Testing (EVT, DVT, and PVT).
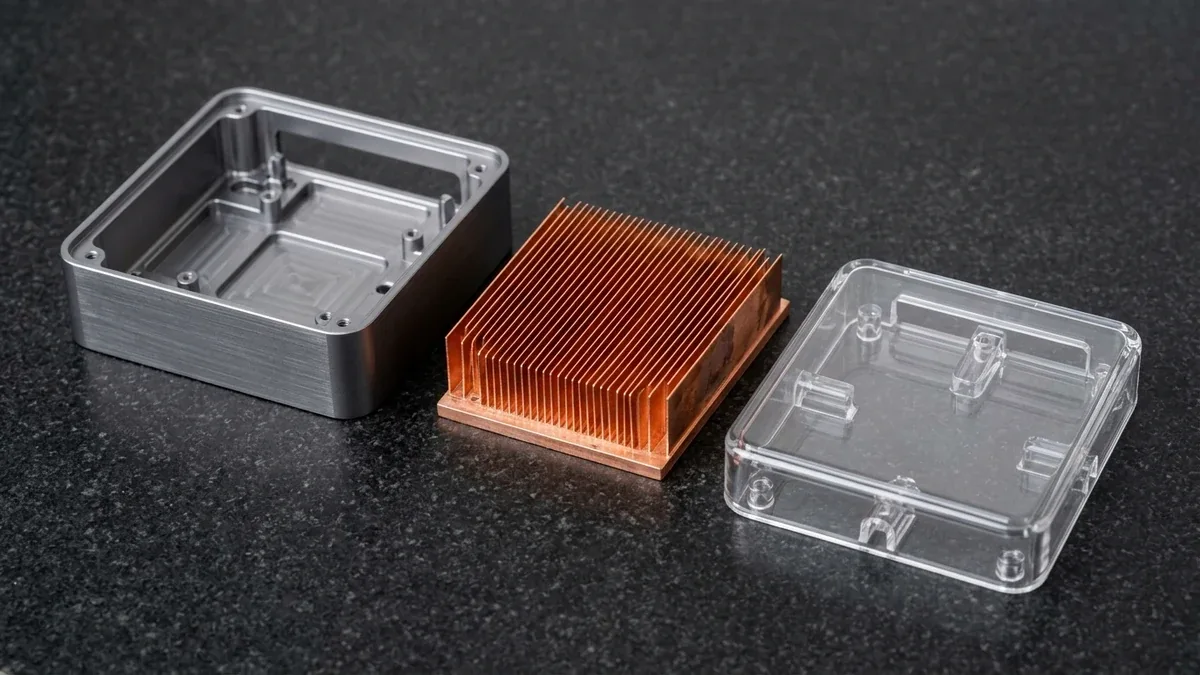
4-Stage Electronics EVT, DVT & PVT Prototyping Lifecycle
A phase-gate manufacturing workflow engineered to eliminate PCB fitment interference, thermal throttling, and cosmetic defects. All turnaround windows denote ex-factory production and inspection completion, strictly separate from 3–5 business days DHL, FedEx, or UPS international air transit.
CAD Tolerance & Thermal DFM Audit
Response: Within 24 HoursLine-item evaluation of thin-wall enclosure deflection, PCB standoff alignment, snap-fit undercut shut-offs, and selective EMI masking boundaries before cutting metal.
- ✓ Root-Sum-Square (RSS) tolerance stack-up
- ✓ Thin-wall vacuum chuck fixture planning
- ✓ Moldflow & parting-line gate analysis
Engineering Verification Prototypes
Ex-Factory: 4 – 8 Business DaysRapid 3-axis CNC milling of uncoated 6061-T6 housings, C11000 electrolytic copper heatsinks, and Stereolithography (SLA) or Multi Jet Fusion (MJF) enclosures for Printed Circuit Board Assembly (PCBA) bring-up.
- ✓ 1 to 20 functional EVT sub-assemblies
- ✓ PCBA boss & I/O port fitment check
- ✓ Verified Raw Material Test Reports (MTR)
Design Verification & Cosmetic Builds
Ex-Factory: 7 – 12 Business DaysPre-production batches (20–100 units) finished with #120/#180 glass-bead blasting, MIL-A-8625 Type II color anodizing, diamond-cut chamfers, and stamped EMI shielding cans.
- ✓ Drop-test & IP67 gasket compression check
- ✓ Conductive SurTec 650 EMI pad masking
- ✓ Diamond-buffed optical PMMA light pipes
Bridge Tooling & Mass Production
Ex-Factory: 12 – 35 Business DaysRapid aluminum molds (12–18 business days T1) and P20/H13 steel production tooling (18–35 business days) alongside multi-fixture CNC runs for 100 to 10,000+ units.
- ✓ T1 molded samples & Cpk capability data
- ✓ Molded-in knurled C3604 brass inserts
- ✓ Zeiss Coordinate Measuring Machine (CMM) QC
Precision Electronics & Smart Appliance Component Showcase
Core electronics hardware fabricated on dedicated shop-floor platforms—pairing cost-efficient ISO 2768-mK baseline profiles with micron-level critical interface fits (shown in the six studio macro showcases below).
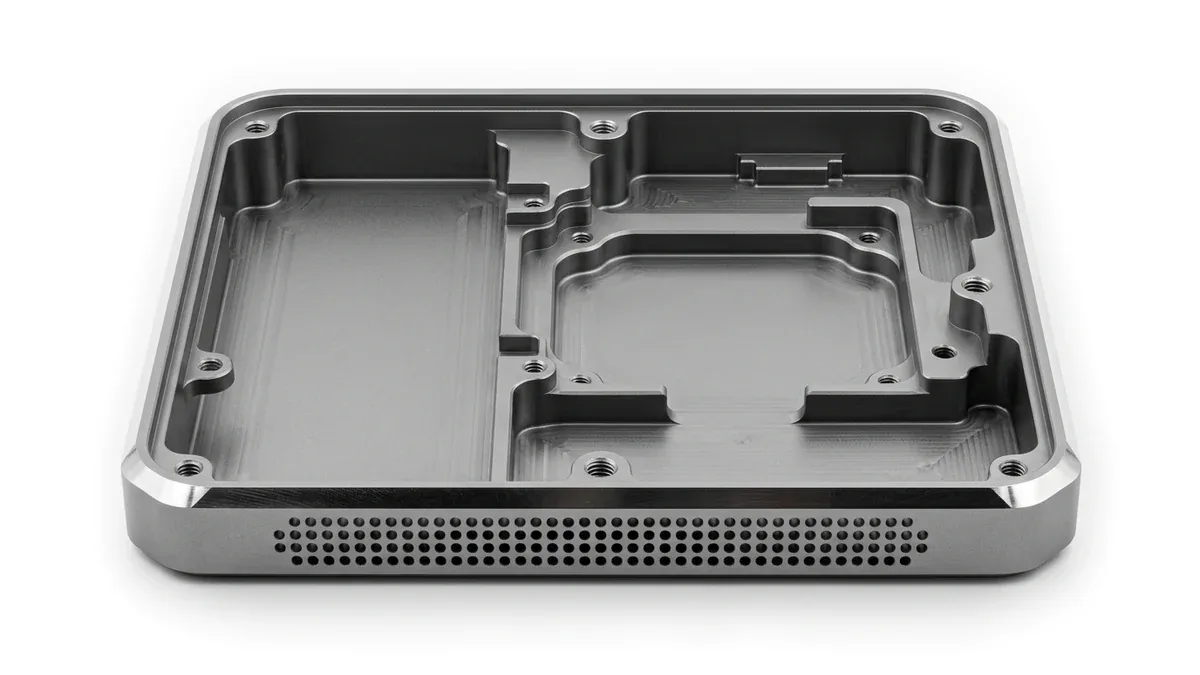 3-Axis CNC Milling
Aluminum Unibody Smart-Device Enclosures
Monolithic 6061-T651 housings milled on high-speed 3-axis vertical machining centers featuring compartmentalized battery and logic-board pockets, micro-drilled acoustic speaker grilles, and #150 bead-blasted grey anodizing accented by 45° diamond-cut chamfers.
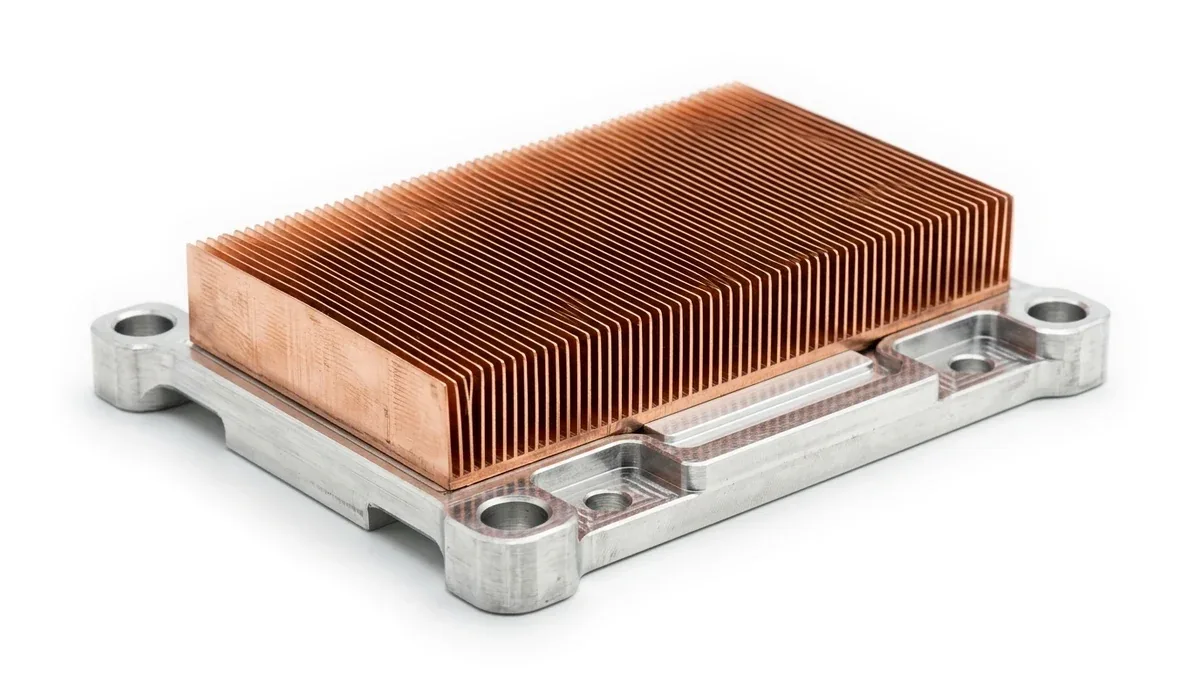 Thermal CNC & Skiving
Skived Copper Heatsinks & Thermal Cold Plates
High-density C11000 Electrolytic Tough Pitch (ETP) copper parallel-fin heatsinks mounted on CNC-milled 6063-T5 aluminum baseplates (C10100/C10200 oxygen-free copper available for vacuum-brazed cold plates), with open airflow channels and fly-cut die pedestals.
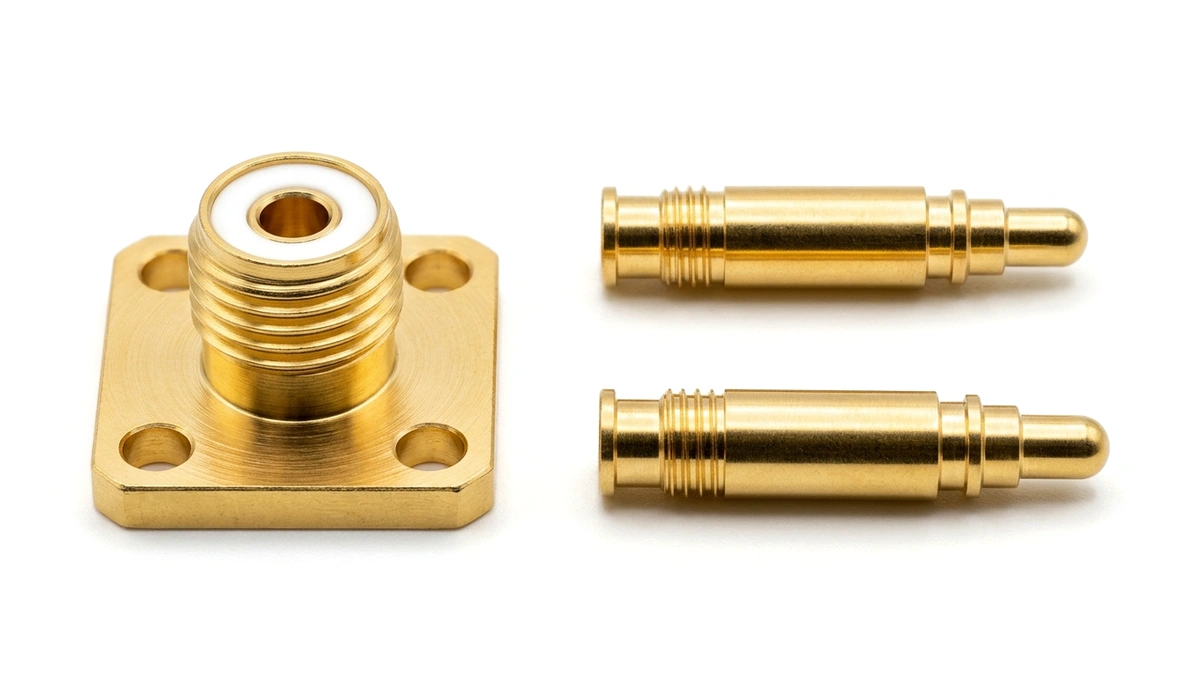 Star Swiss Turning
Swiss-Turned RF Coaxial Connectors & Contacts
Hard-gold-plated C3604 brass 4-hole square-flange RF coaxial receptacles housing concentric virgin polytetrafluoroethylene (PTFE) dielectric sleeves, paired with multi-stepped male contact pins featuring hemispherical tips and retention grooves turned on Star Swiss lathes.
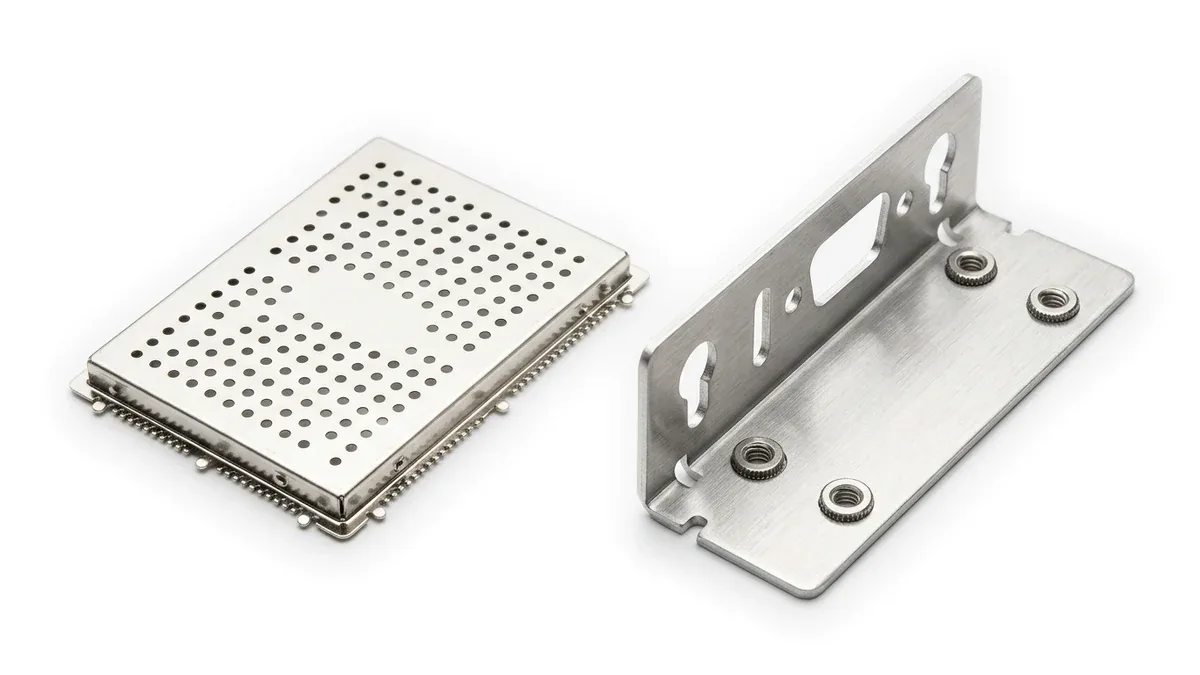 Sheet Metal & Stamping
Board-Level EMI Shield Cans & I/O Brackets
Thin 0.2 mm C7521-1/2H nickel-silver stamped PCB RF shielding cans with serrated grounding tabs and Surface-Mount Technology (SMT) solder feet, alongside fiber-laser-cut and CNC-bent 1.2 mm 5052-H32 aluminum I/O brackets with self-clinching nuts.
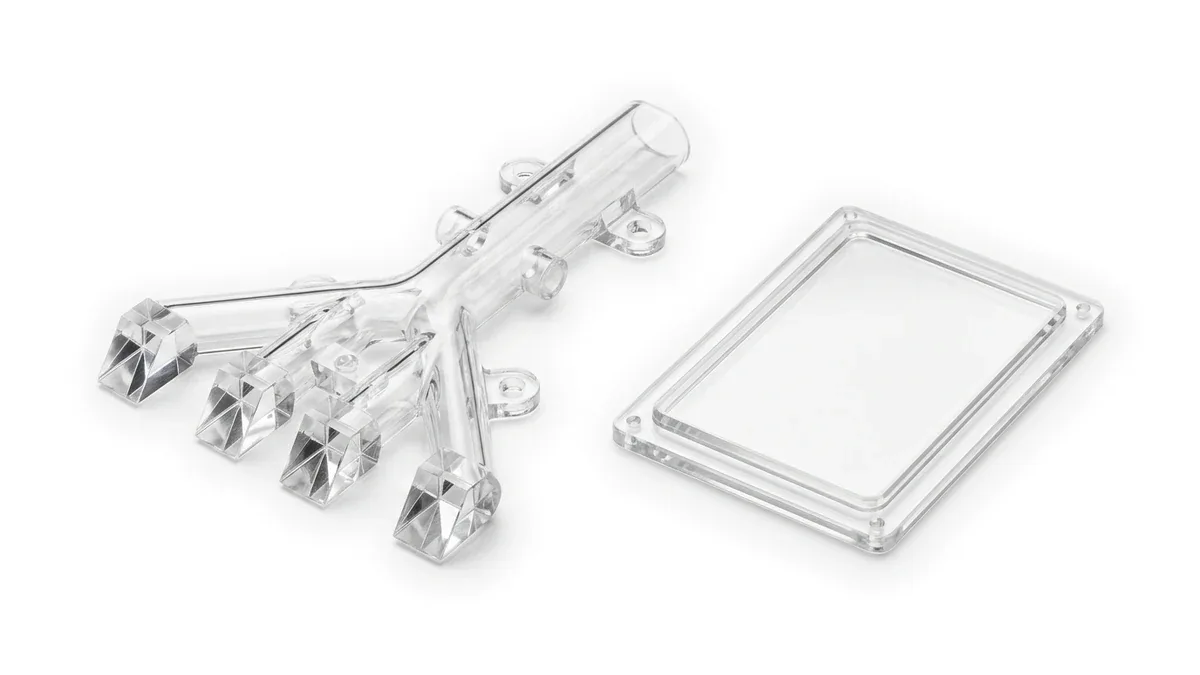 Optical Diamond Milling
Optical PMMA Light Guides & Sensor Windows
Optical polymethyl methacrylate (PMMA) multi-branch light pipes with 45° Total Internal Reflection (TIR) prisms finished via 70–80 °C annealing and Single-Point Diamond Turning (SPDT), paired with 110–120 °C annealed and dichloromethane (DCM) vapor-polished polycarbonate (PC) windows.
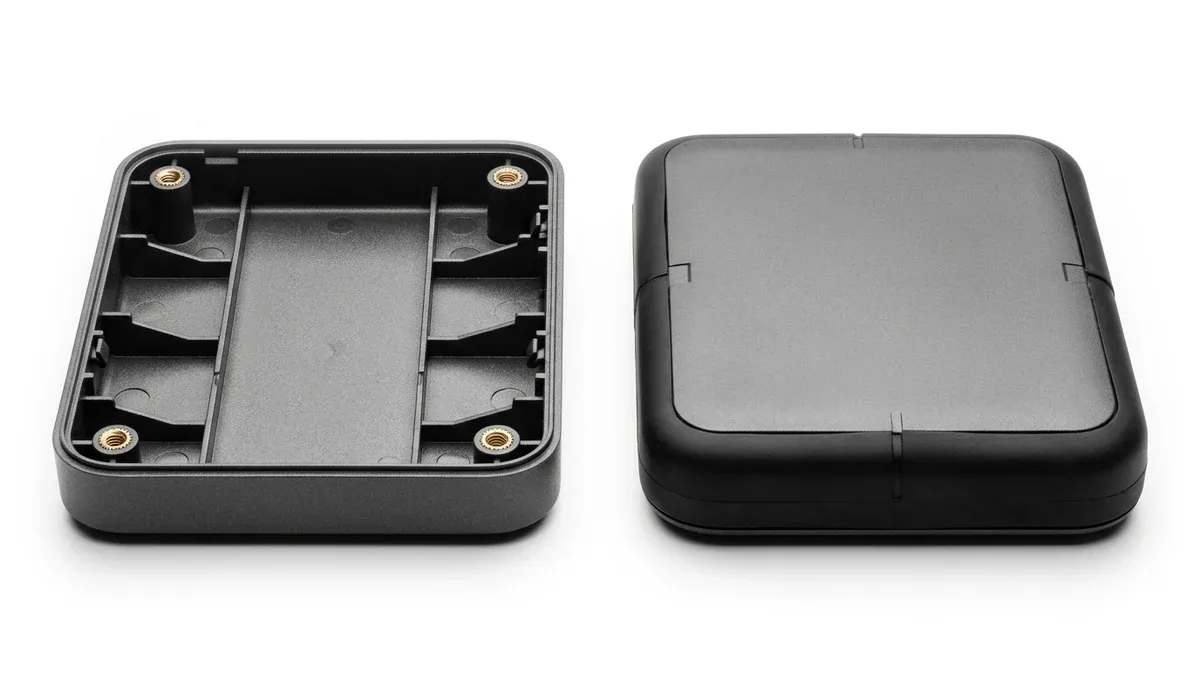 Injection & Overmolding
PC/ABS Enclosures & TPE Soft-Grip Overmolding
Flame-retardant UL94 V-0 PC/ABS housings molded with uniform 1.8 mm walls, 0.9 mm (0.50× nominal wall) anti-sink internal ribs, molded-in knurled C3604 brass threaded inserts, and seamless Shore 60A thermoplastic elastomer (TPE) perimeter overmolding.
Integrated Electronics Hardware Manufacturing Ecosystem
Consolidating CNC metal chassis, thermal modules, and molded polymer housings inside one Shenzhen shop floor eliminates multi-vendor datum drift across mated consumer assemblies.
High-Speed 3/4-Axis & Star Swiss CNC
In our in-house CNC machining facility practice, Brother Speedio and 24,000 RPM Fanuc Robodrill centers finish 6061-T651 shells (Vc = 280–400 m/min, fz = 0.06–0.12 mm/tooth) alongside Star sliding-headstock Swiss lathes (Ø0.5–32.0 mm bar capacity).
24,000 RPM Spindles & Star Guide-Bushing LathesSheet Metal & EMI/RFI Shielding
12 kW fiber laser blanking, 160-ton CNC press-brake forming (DIN 6935 flat-pattern K-factor development), and progressive stamping produce 0.2 mm C7521 Radio Frequency Interference (RFI) board shields, 5052-H32 I/O brackets, and conductive SurTec 650 grounding paths.
0.05 mm SMT Coplanarity & Flush Clinch HardwareRapid Tooling, Optics & Overmolding
Seamless scaling from SLA, Selective Laser Sintering (SLS), MJF, and urethane vacuum casting to P20 (28–34 HRC) and H13 (48–52 HRC) bridge molds with two-shot TPE overmolding.
50T–850T Presses & SPI A-1 Optical PolishingWhy Do Electronics Teams Choose Our In-House Facility Over Quoting Networks?
Direct single-roof manufacturing guarantees matched anodize dye lots, physical multi-part assembly fit-ups before dispatch, and closed-network CAD confidentiality that distributed quoting marketplaces cannot enforce.
| Manufacturing Control Vector | Distributed Quoting Networks | AS Prototypes (In-House Direct Facility) |
|---|---|---|
| Cosmetic Anodize Consistency | Split across separate anodizing job shops, causing visible shade shifts between mated upper and lower shells. | Single-Bath Rack Control: Mated 6061-T6 enclosures are bead-blasted and anodized together on one titanium rack under D65 master-sample inspection. |
| Multi-Process Device BOM | CNC housings, stamped EMI shields, and molded bezels routed to uncoordinated subcontractors without trial assembly. | Pre-Shipment Fit-Up Verification: Aluminum chassis, copper heatsinks, PMMA light guides, and PC/ABS covers are dry-fitted before dispatch. |
| EMI/RFI Grounding Masking | Unmasked immersion anodizing creates an insulating oxide barrier over PCB grounding bosses and gasket tracks. | Precision Selective Masking: Die-cut silicone plugs and CNC laser ablation preserve low-resistance SurTec 650 grounding pads. |
| Thin-Wall Enclosure Flatness | Standard jaw clamping bows 0.8–1.2 mm aluminum sidewalls inward, binding against PCBA edges during assembly. | Vacuum Chuck & Symmetric Milling: Alternating residual-stress relief roughing holds 0.020 mm (0.0008″) datum flatness. |
| Intellectual Property (IP) | Unreleased consumer product CAD assemblies circulated across open external supplier bidding pools. | Direct Bilateral NDA: Closed-network CAM programming and restricted shop-floor access safeguard confidential hardware launches. |
| Commercial Cost Structure | Opaque algorithmic platform markups stacked onto cosmetic bead-blasting and tight-tolerance callouts. | Custom Quoted per CAD DFM: Transparent engineering evaluation driven directly by spindle cycle time, resin weight, and fixture setup. |
Electronics Material Selection & Precision Tolerances Matrix
Verified mechanical, thermal, and optical properties paired with achievable shop-floor tolerances and objective design trade-offs across core electronics alloys and polymers.
| Material & Grade | Process & Standard | Strength & Thermal (MPa · W/m·K) | Finish & Functional Trait | Achievable Tolerance (mm / in) | Recommended Application / When to Choose |
|---|---|---|---|---|---|
| Aluminum 6061-T6 / T651 Pre-Stretched Cosmetic Plate | 3/4-Axis CNC Milling · ISO 2768-mK | 310 MPa (45.0 ksi) · k = 167 W/m·K | #120/#180 Bead Blast + MIL-A-8625 Type II + SurTec 650 Masking | ±0.010 mm (±0.0004″) | Best for cosmetic unibody chassis and RF enclosures; avoid tight cold sheet bends (< 3.0t cracks outer grains—use 5052-H32). |
| Copper C11000 (ETP) C10100/C10200 for Vacuum Braze | Skiving & CNC Milling · ASTM B152 | 220–250 MPa (32–36 ksi) · k = 388 W/m·K | 100–101% IACS · Electroless Nickel (ENP) or Anti-Tarnish | ±0.015 mm (±0.0006″) | Best for high-heat-flux CPU/SoC skived heatsinks; avoid C11000 in reducing-gas brazing (specify oxygen-free C10100/C10200). |
| Brass C3604 Free-Cutting Swiss-Turn Bar | Star Swiss Turning · JIS H3250 | 380–440 MPa (55–64 ksi) · k = 115 W/m·K | Hard Gold (0.5–1.27 µm) over Sulfamate Nickel Barrier | ±0.005 mm (±0.0002″) | Best for 5G RF coaxial bodies, pogo-pin contacts, and knurled inserts (RoHS 6c alloy; specify lead-free C6801 if < 0.1% Pb required). |
| Nickel-Silver C7521 Cu-18Ni-20Zn Strip (0.2 mm) | Stamping & Laser · JIS H3100 | 490–590 MPa (71–86 ksi, 1/2H) · 620–740 MPa (SH) | Direct Reflow SMT Solderability (Zero Post-Plating) | ±0.10 mm (±0.004″) | Best for board-level PCB EMI/RFI shield cans (1/2H) and clip-on frames (SH); avoid for primary heat spreading (k = 33 W/m·K). |
| Optical PMMA & PC Acrylic (n=1.49) · PC (n=1.58) | SPDT & Optical CNC · ISO 2768-mK | 80 MPa (PMMA) / 65 MPa (PC) · Ra ≤ 0.02 µm | PMMA: ~92% Transmittance (70–80 °C Anneal + Buff) · PC: ~89% (110–120 °C + DCM) | ±0.020 mm (±0.0008″) | PMMA best for crisp TIR LED light pipes (never DCM vapor or flame polish); choose PC for drop-resistant LiDAR/IR windows. |
| PC/ABS + TPE Overmold UL94 V-0 Resin + Shore 60A Grip | Two-Shot / Insert Molding · ISO 20457 | 2.4 GPa (348 ksi) Flexural Modulus | VDI 24 (1.5°–2.0° Draft) / SPI B-1 + 1.2 mm TPE Seal | ±0.08–0.15 mm (TG 4–5) | Best for handheld smart-appliance shells (100–10,000+ units); keep internal ribs ≤ 0.50–0.60× wall thickness to prevent sink marks. |
Empirical Quality Verification & Electronics DFM Physics
Cosmetic uniformity, thermal contact flatness, optical clarity, and RF grounding continuity are verified through shop-floor process controls inside our 20 °C ± 1 °C metrology lab.
Eliminating Anodize Witness Lines
Symptom: faint cutter halos visible after Type II anodizing. Root cause: thermal spindle Z-drift altering grain reflectivity. Corrective action: laser tool-offset calibration, fine skimming before #150 glass-bead blasting, and single-rack dye-lot control.
- ✓ Zero step-over witness marks on Class-A faces
- ✓ Monocrystalline diamond-cut 45° bevels
- ✓ ISO 4287 roughness check (Mitutoyo SJ-210)
Pedestal Flatness & Air-Decay Leak QC
Fly-cutting C11000 copper pedestals to 0.030 mm / 100 mm flatness minimizes Thermal Interface Material (TIM) bond-line resistance, while gasketed outdoor housings undergo pressure-decay verification.
- ✓ Ra 0.4 µm (16 µin) die contact pedestals
- ✓ Low-impedance SurTec 650 Faraday continuity
- ✓ 3.5–6.0 bar pressure-decay & bubble leak test
Split-Track PMMA & PC Finishing
Optical PMMA undergoes 70–80 °C annealing plus #800–#5000 progressive diamond buffing or SPDT (never DCM vapor or flame, preventing fogging), whereas machined PC requires 110–120 °C annealing before DCM vapor polishing.
- ✓ Zero solvent crazing or prism edge roll-off
- ✓ Crisp diamond-turned 45° TIR facets
- ✓ ~92% PMMA / ~89% PC transmittance preserved
Zeiss CMM & 2.5D Optical VMS
Machined PCB standoffs and I/O cutouts are probed on our Zeiss Contura CMM, while delicate 0.2 mm SMT shield cans and elastomer seals are measured non-contact via 2.5D Optical Video Measuring Systems (VMS).
- ✓ Ballooned First Article Inspection (FAI) reports
- ✓ 0.05 mm SMT foot coplanarity via 2.5D VMS
- ✓ Calibrated thread plug & pin gauge checks
Frequently Asked Questions: Electronic Appliance CNC Machining
Direct engineering answers on thin-wall 6061-T651 flatness control, selective EMI grounding, thermal heatsink finish, and ex-factory EVT/DVT/PVT lead times.
Thin-wall 6061-T6 enclosures (0.8–1.2 mm walls) warp when asymmetric pocketing releases internal rolling stresses, so we machine pre-stretched 6061-T651 plate using alternating double-sided roughing passes. Final finishing runs on custom vacuum fixtures after a 150–165 °C stress-relief cycle, holding 0.020 mm (0.0008 in) datum flatness.
Sulfuric acid anodizing per MIL-A-8625 Type II grows a 10–25 µm insulating oxide layer that blocks Faraday cage electromagnetic shielding. We apply silicone plug masking or laser ablation over PCB grounding pads and gasket tracks, treating exposed aluminum contacts with conductive trivalent SurTec 650 conversion.
High-heat-flux processors require low-roughness, flat pedestals to minimize thermal interface material bond-line thickness and air-gap resistance. Our shop fly-cuts C11000 electrolytic copper and 6063-T5 aluminum pedestals to Ra 0.4–0.8 µm (16–32 µin) per ISO 4287 while holding 0.030 mm (0.0012 in) flatness per 100 mm.
After 24-hour engineering DFM review, uncoated EVT CNC and 3D printed prototypes finish in 4–8 business days ex-factory, while anodized or plated DVT batches require 7–12 business days. Rapid bridge injection tooling takes 12–35 business days ex-factory, strictly separate from 3–5 business days international air transit.
Ready to Prototype or Scale Your Electronics Hardware?
Upload your 3D CAD assembly models (STEP, IGES, or SolidWorks) and 2D Geometric Dimensioning and Tolerancing (GD&T) drawings for a comprehensive manufacturability review, datum-locking strategy, and custom production quotation.