Aerospace CNC Machining Services & Multi-Axis Flight Hardware
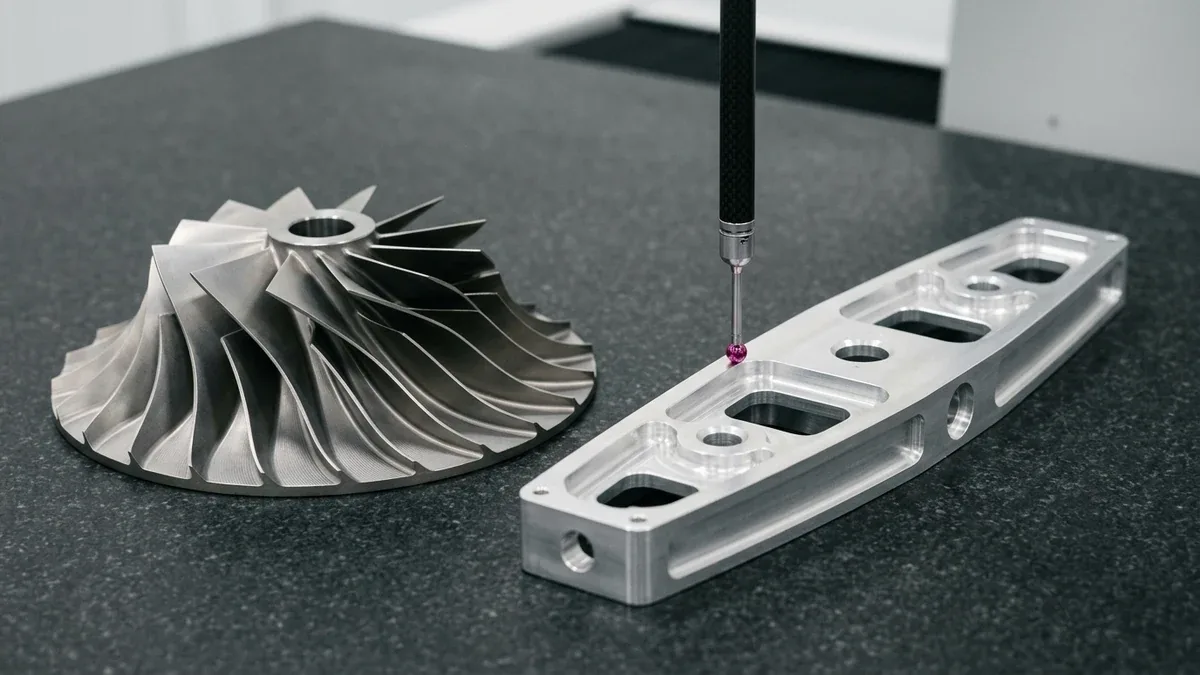
AS Prototypes delivers direct in-house aerospace CNC machining services across high-speed 3/4-axis Computer Numerical Control (CNC) milling, simultaneous 5-axis contouring, Direct Metal Laser Sintering (DMLS), cylindrical grinding, and submerged Electrical Discharge Machining (EDM). From monolithic 6061-T651 avionics chassis to Ti-6Al-4V blisks and Invar 36 flexures, every flight build includes Coordinate Measuring Machine (CMM) verification.
4-Stage Aerospace & Avionics Hardware Execution Lifecycle
A phase-gate manufacturing protocol eliminating thin-rib chatter, residual billet distortion, and datum shift. All schedules denote ex-factory production and inspection turnaround, separate from 3–5 business days international air transit (DHL/FedEx/UPS).
Toolpath & GD&T Feasibility Review
Response: 24 – 48 HoursDuring Design for Manufacturability (DFM) review, senior Computer-Aided Manufacturing (CAM) engineers evaluate Geometric Dimensioning and Tolerancing (GD&T) datums, pocket aspect ratios, 5-axis tilt clearance, and MIL-A-8625 hole-masking zones.
- ✓ Full 5-axis kinematic collision simulation
- ✓ Thin-wall rib step-down deflection check
- ✓ Datum A-B-C soft-jaw & fixture locking
Engineering Development Units
Ex-Factory: 4 – 8 Business DaysRapid as-machined 3/4-axis Vertical Machining Center (VMC) milling of 6061-T651 avionics housings, 7075-T7351 structural ribs, and high-temperature polyetherimide (PEI) ducts for bench fit-up and vibration testing.
- ✓ 1 to 10 functional prototype assemblies
- ✓ Traceable heat-lot Mill Test Reports (MTR)
- ✓ 20°C ± 1°C Zeiss CMM critical-fit check
Finished & Hybrid Additive Builds
Ex-Factory: 7 – 12 Business DaysQualification hardware integrating DMLS Ti-6Al-4V sintering with 5-axis post-machining, cylindrical valve-spool grinding, MIL-A-8625 Type II/III anodizing, conductive SurTec 650 conversion, and ASTM A967 passivation.
- ✓ Ballooned First Article Inspection (FAI)
- ✓ Silicone plug masking on H7 bores & threads
- ✓ CMM coaxiality, runout & ISO 4287 Ra reports
Low-Volume Series Production
Ex-Factory: 7 – 30 Business DaysRepeatable batch manufacturing (10 to 1,000+ units; 7–12 days standard 3/4-axis runs, 15–30 days complex 5-axis or multi-finish assemblies) using locked numerical control (NC) programs and in-spindle probing.
- ✓ Locked CAM toolpaths & serialized billet lots
- ✓ Renishaw in-situ work-offset probing
- ✓ Custom shock-absorbing export packaging
Precision Aerospace & Avionics Component Showcase
Flight, propulsion, fluid-control, and orbital payload hardware matched to the most economical shop-floor platform—combining high-speed 3/4-axis VMCs with strategic 5-axis, grinding, DMLS, and Wire EDM cells.
Ruggedized Avionics & RF Filter Chassis
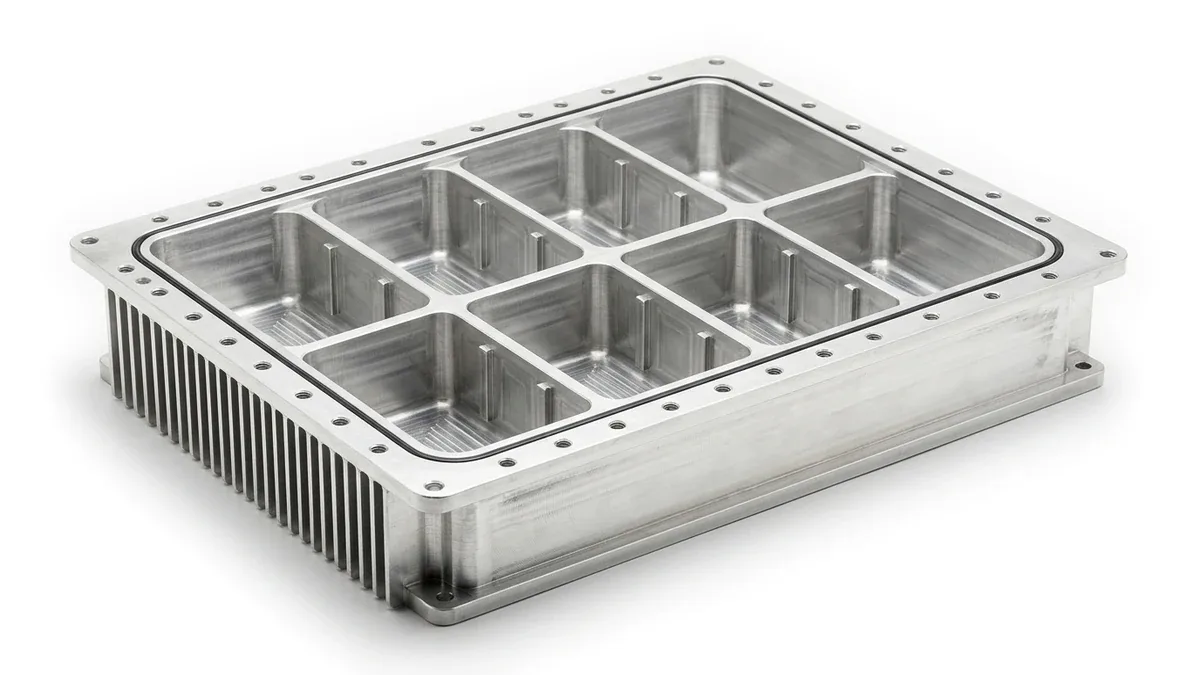
Monolithic 6061-T651 billet-hogged avionics enclosures milled on high-speed Brother and Mazak 3-axis VMCs with multi-cavity radio-frequency (RF) and electromagnetic interference (EMI) isolation bays, external cooling fins, and a continuous closed-loop O-ring groove inside the bolt circle.
5-Axis Titanium Impellers & Blisks
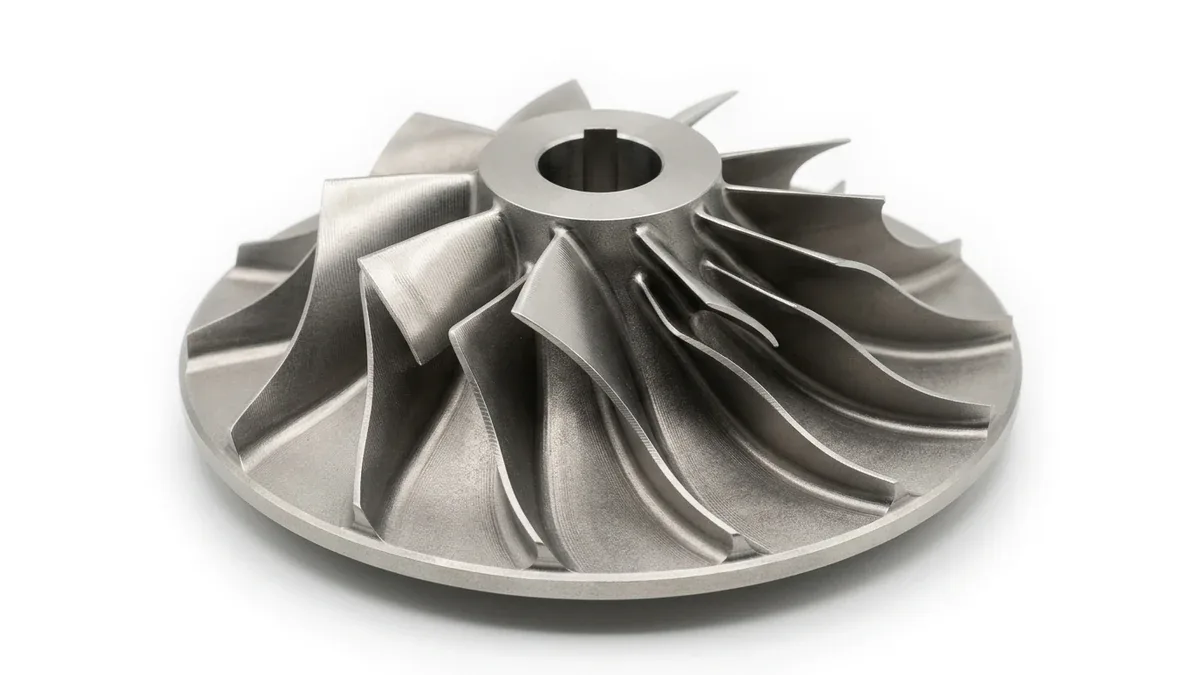
Simultaneous 5-axis Ti-6Al-4V (Grade 5) and Inconel 718 centrifugal impellers machined on our AFMING GMU-400 trunnion center (Ø450 × 350 mm) with 3D twisted aerodynamic splitter blades, tangential root fillets, and concentric keyed rotor bores.
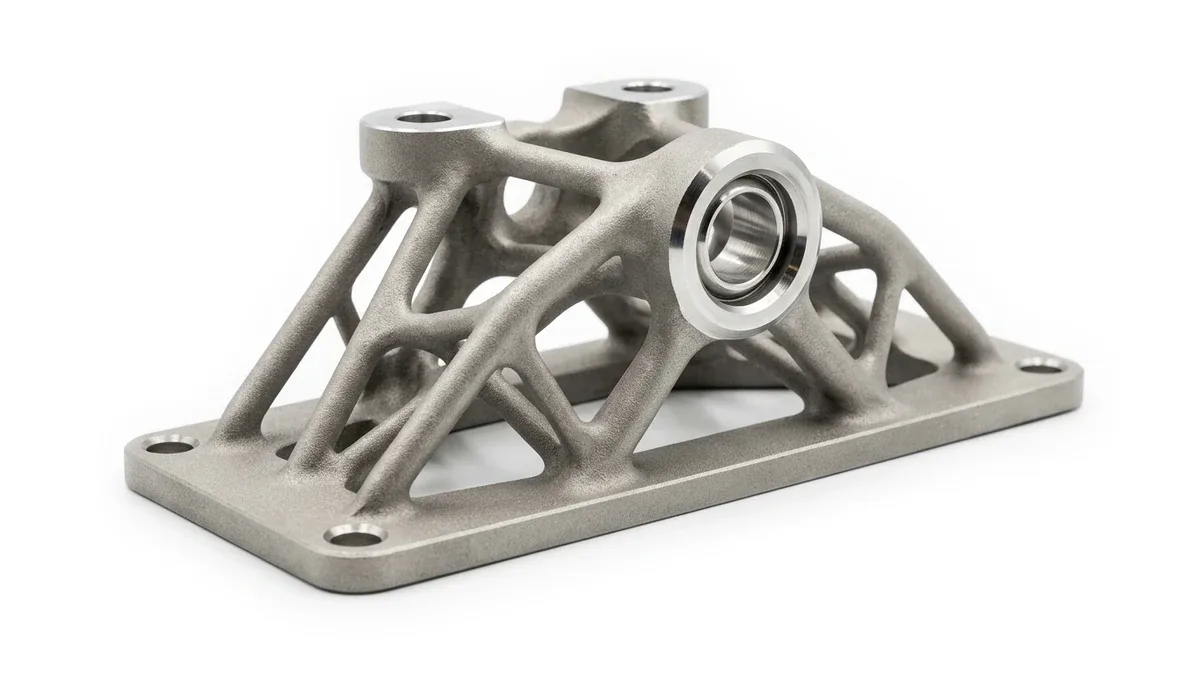
DMLS Topology-Optimized Airframe Brackets
Generative Ti-6Al-4V and AlSi10Mg load-bearing brackets laser-sintered inside our 280 × 280 × 365 mm dual-laser DMLS chamber, vacuum stress-relieved, and 5-axis post-machined across mounting pads and spherical bearing clevis bores.
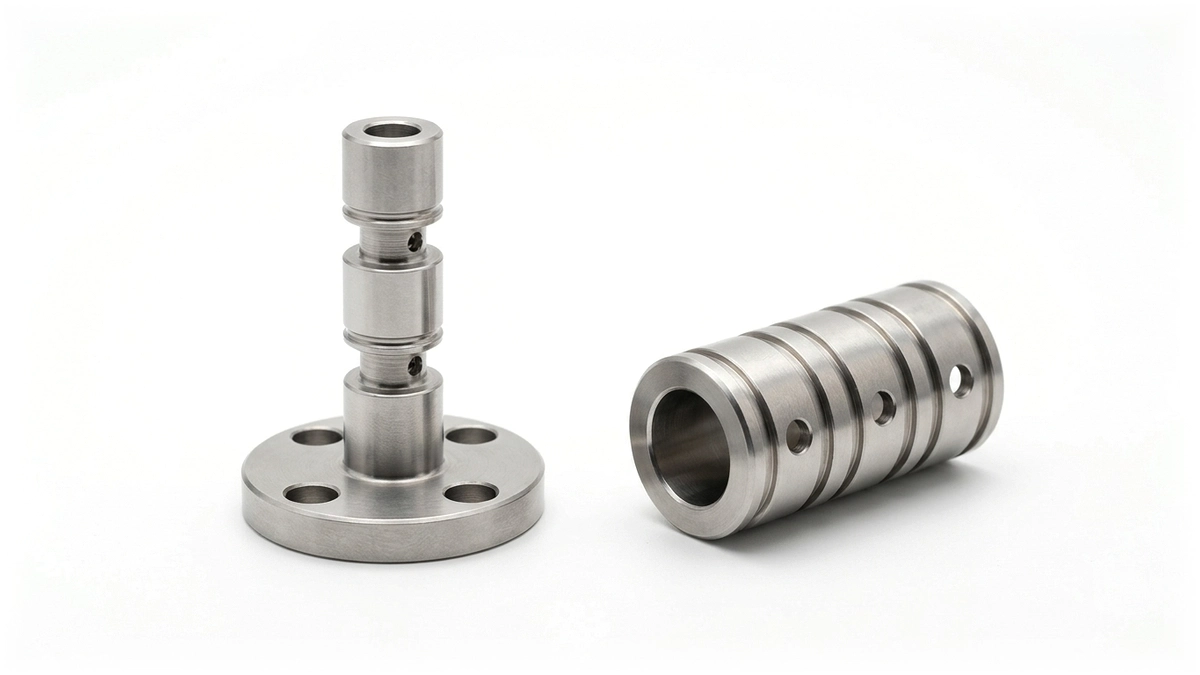
Hydraulic Actuator Valve Spools & Sleeves
Precipitation-hardened 17-4PH (Condition H900) flight-control hydraulic flanged valve spools featuring cylindrical-ground metering lands, pressure-balancing micro-grooves, and cross-drilled fluid orifices paired with match-honed cartridge sleeves with radial metering ports.
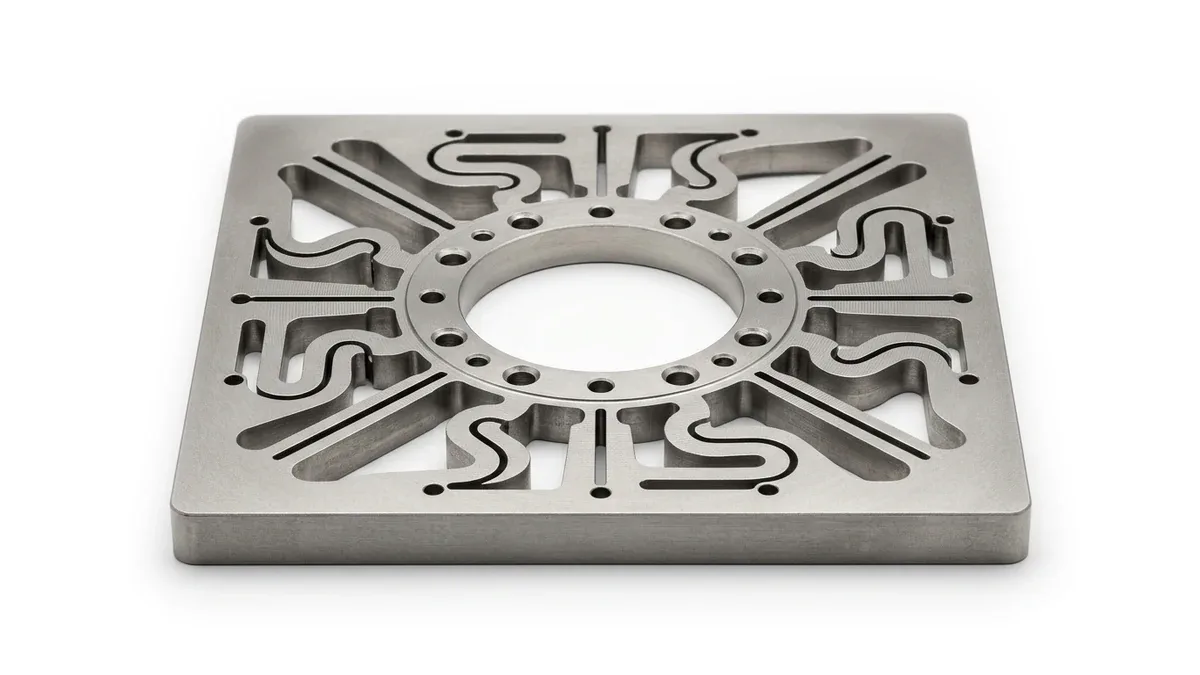
Invar 36 Satellite Optical Payload Flexures
Ultra-low thermal expansion Invar 36 (FeNi36) orbital mirror mounts cut via submerged Sodick linear-motor Wire EDM using one rough cut plus three to four skim passes (≤ 1–2 µm recast white layer) to isolate optics from launch stress.
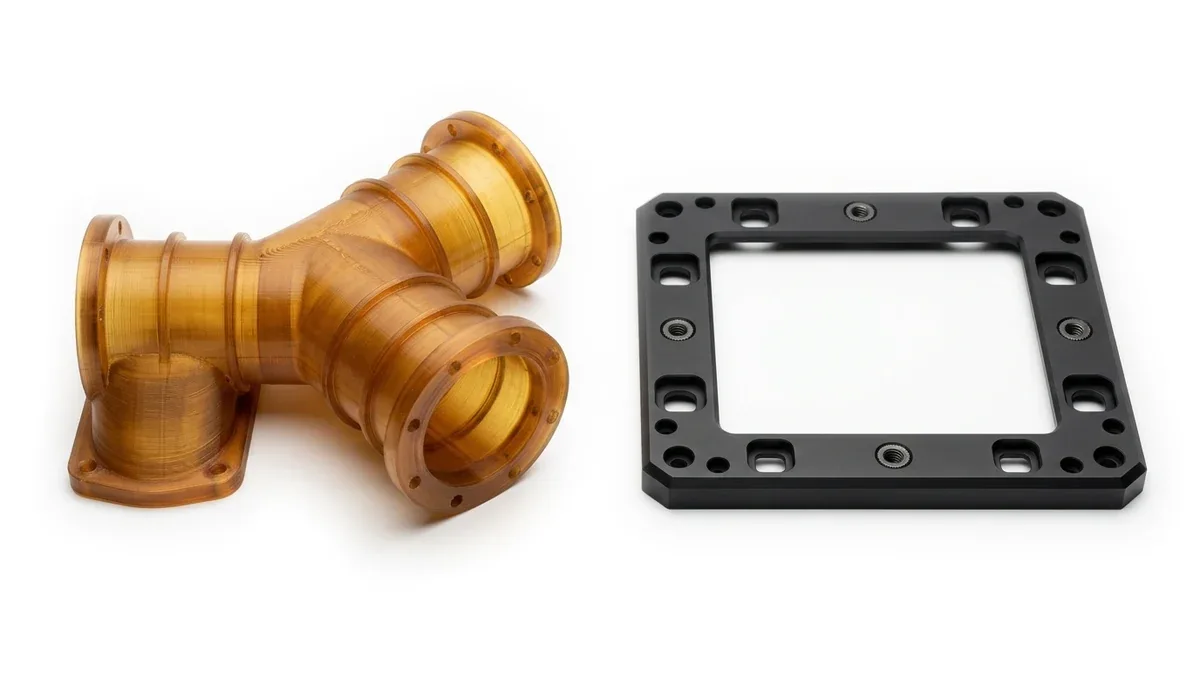
Polyetherimide ECS Ducts & 5052-H32 Bezels
Flame-retardant polyetherimide (ULTEM 9085 / 1010, UL94 V-0) bifurcated environmental control system (ECS) Y-ducts printed via heated-chamber Fused Deposition Modeling (FDM), paired with laser-cut matte-black anodized 5052-H32 sheet metal cockpit bezels with self-clinching nuts.
Unified Multi-Axis CNC, DMLS & Wire-EDM Aerospace Cell
Consolidating high-speed 3/4-axis milling, simultaneous 5-axis contouring, DMLS sintering, and submerged Wire EDM under one roof eliminates inter-vendor datum transfer stack-up on multi-process flight assemblies.
Economical 3/4-Axis & Strategic 5-Axis
Prismatic avionics housings, mounting plates, and cold plates route to our 13 Brother, Fanuc, and Mazak 3/4-axis VMCs (up to 1,050 × 530 × 510 mm) at Vc = 280–400 m/min in 7075-T7351, reserving simultaneous 5-axis machine hours strictly for compound-angle manifolds and Ti-6Al-4V blisks (Vc = 45–65 m/min).
HSK-A63 Shrink-Fit Holders & Through-Spindle Coolant (TSC)DMLS Sintering + 5-Axis Datum Milling
In our in-house hybrid cell practice, we sinter Ti-6Al-4V and Inconel 718 topology brackets on steel build plates, perform vacuum stress-relief annealing, and transfer the plate directly onto our 5-axis trunnion to bore H7 clevises before Wire-EDM cutoff.
Unified Build-Plate Datum & Zero Re-Clamping ShiftStar Swiss, Grinding & Sodick EDM
Slender aerospace pins and sensor stems (Ø0.5–32 mm) turn on 6 Star sliding-headstock Swiss lathes, while 17-4PH valve spools and Invar 36 flexures finish on our Palmary ODC-3250 cylindrical grinder and Sodick ALN400Qs submerged Wire EDM.
±0.005 mm (±0.0002″) Precision & Ra 0.2 µm LandsShop-Floor Aerospace Material Limitations & When NOT to Specify
- Avoid Fusion Welding 7075 Aluminum or Using Peak-Aged 7075-T6 in Thick Marine/Humid Airframes: High-zinc 7075 suffers severe hot-cracking during tungsten inert gas (TIG)/laser welding and short-transverse stress-corrosion cracking (SCC); specify mechanically fastened over-aged 7075-T7351 for thick bulkheads or weldable 6061-T651 / 5052-H32 for brazed/welded enclosures.
- Avoid Cold-Bending 6061-T6 Sheet Below 3.0t–6.0t Inside Radii: Solution-heat-treated 6061-T6 fractures along outer bend grains on tight avionics flanges; specify ductile 5052-H32 (minimum inside bend radius R ≥ 1.0t–1.5t per DIN 6935) for formed chassis and clinched bezels.
- Avoid Unmasked MIL-A-8625 Type III Hardcoat on H7 Bores & Fine Threads: A 50 µm Type III oxide layer penetrates 25 µm inward and grows 25 µm outward per surface (shrinking bore diameters by ~0.05 mm at 450–550 HV0.05 hardness); always specify silicone plug masking or post-anodize wire thread inserts.
Direct In-House Aerospace Cell vs. Online Order-Routing Platforms
Why propulsion, avionics, and orbital payload engineering teams partner directly with our integrated Shenzhen machine shop rather than decentralized online subcontracting platforms.
| Engineering Criterion | Decentralized Online Platforms | AS Prototypes (Direct In-House Facility) | Recommended Aerospace Application / When to Choose |
|---|---|---|---|
| DMLS + 5-Axis Hybrid Datum | Metal 3D printing and CNC post-milling split across separate shops, losing datum alignment after support removal. | Unified Build-Plate Reference: DMLS titanium sintering and 5-axis H7 bore finishing share the same build-plate datum in-house. | Best for topology-optimized airframe brackets and conformal manifolds requiring ±0.015 mm true-position interfaces. |
| 90% Billet Hog-Out Stability | Aggressive single-sided roughing releases internal rolling stresses, twisting thin-wall ribs after vise unclamping. | Pre-Stretched T651/T7351 & Balanced Roughing: Alternating flip-milling and controlled thermal stress relief hold flatness ⏥ 0.025 mm (0.0010″). | Best for monolithic wing ribs, optical baseplates, and multi-cavity RF avionics housings with 0.8–1.5 mm walls. |
| Hardcoat Bore & Thread Fit | Unmasked MIL-A-8625 Type III anodizing (25 µm/side outward growth) seizes fine aerospace screws and shrinks bearing bores. | Silicone Plug Masking & Wire Inserts: Dedicated masking of H7 bores and post-anodize 304 stainless wire thread inserts preserve 6H/3B assembly fit. | Best for wear-resistant actuator housings and EMI-grounded chassis combining Type III exterior with Alodine lands. |
| Material Lot Traceability | Fragmented raw-stock paperwork across anonymous sub-tier suppliers with unverified heat-treatment states. | Heat-Lot MTR & ASTM E18 Verification: Every billet is matched to its original Mill Test Report and checked via digital Rockwell hardness testing. | Best for flight-test EDU builds, 17-4PH H900 hydraulic spools, and Ti-6Al-4V propulsion rotors. |
| Spindle Cost Optimization | Automated quoting engines apply blanket 5-axis surcharges to simple 2.5D prismatic housings and brackets. | 3/4-Axis + 5-Axis Partitioning: High-speed 3-axis VMCs rough prismatic stock before targeted 5-axis finishing, Custom Quoted per CAD DFM. | Best for multi-part bill-of-materials (BOM) packages mixing simple structural mounts with complex 5-axis impellers. |
Aerospace Material Selection & Achievable Tolerances Matrix
Benchmarked tensile properties, thermal limits, and repeatable in-house shop-floor tolerances across flight-critical alloys, sheet metals, and high-temperature polymers.
| Material & Temper | Tensile / Yield Strength (MPa / ksi) | Density (g/cm³) & Thermal / Physical Trait | Critical Tolerance (mm / in) | Recommended Application / When to Choose |
|---|---|---|---|---|
| Titanium Ti-6Al-4V Grade 5 / Grade 23 Extra-Low Interstitial (ELI) Billet & DMLS | 950 / 880 MPa (138 / 128 ksi) | 4.43 g/cm³ · k = 6.7 W/m·K · 400°C Max Service | ±0.010 mm (±0.0004″) | Choose for 5-axis centrifugal blisks, DMLS topology airframe brackets, and high-fatigue engine clevises. |
| Aluminum 7075-T651 / T7351 Pre-Stretched Structural Plate | 572 / 503 MPa (83.0 / 73.0 ksi) [T651] 505 / 435 MPa (73.2 / 63.1 ksi) [T7351] | 2.81 g/cm³ · High SCC Resistance in T7351 Temper | ±0.010 mm (±0.0004″) | Choose T7351 for thick monolithic wing ribs and bulkheads exposed to stress-corrosion environments (non-weldable). |
| Aluminum 6061-T651 Stress-Relieved Avionics Billet | 310 / 276 MPa (45.0 / 40.0 ksi) | 2.70 g/cm³ · k = 167 W/m·K · Vacuum-Brazeable | ±0.010 mm (±0.0004″) | Choose for 3-axis milled Air Transport Rack (ATR) avionics enclosures, RF filter cavities, and vacuum-brazed cold plates. |
| Aluminum 5052-H32 Ductile Aerospace Sheet Metal | 228 / 193 MPa (33.1 / 28.0 ksi) | 2.68 g/cm³ · Cold Bend Radius R ≥ 1.0t–1.5t (DIN 6935) | Cut ±0.10–0.20 mm · Bend ±0.20–0.40 mm | Choose for laser-cut, CNC-bent avionics brackets, battery trays, and self-clinched cockpit instrument bezels. |
| Stainless Steel 17-4PH Condition H900 / H1025 Bar | 1,310 / 1,170 MPa (190 / 170 ksi) [H900] | 7.78 g/cm³ · 40–44 HRC (ASTM E18) · ASTM A967 Passivated | ±0.005 mm (±0.0002″) Ground | Choose for cylindrical-ground hydraulic actuator valve spools, honed cartridge sleeves, and latch pins. |
| Invar 36 (FeNi36) Annealed Low-Expansion Alloy | 490 / 280 MPa (71.1 / 40.6 ksi) | 8.05 g/cm³ · CTE ≤ 1.2 × 10⁻⁶ /K (20–100°C) | ±0.005 mm (±0.0002″) Wire EDM | Choose for submerged Wire-EDM satellite optical payload flexures, laser bench mounts, and carbon-fiber-reinforced polymer (CFRP) layup tooling. |
| Inconel 718 & ULTEM PEI Superalloy / FDM PEI 1010 & 9085 | 1,275 MPa (Inconel) · 69–81 MPa (FDM XY PEI) | 700°C Max (Inconel) · Tg 217°C (PEI 1010) / 186°C (9085), UL94 V-0 | ±0.015 mm (CNC) / ±0.20 mm (FDM) | Choose Inconel 718 for hot-section propulsion manifolds and industrial FDM PEI for lightweight cabin ECS air ducts. |
Climate-Controlled Metrology & Aerospace Quality Protocols
Every flight, hydraulic, and orbital payload component undergoes deterministic stress-relief stabilization, calibrated surface finishing, and multi-instrument inspection inside our Shenzhen metrology lab.
Zeiss CMM & 2.5D Optical VMS
Machined blisks, coaxial clevis bores, and sealing glands are verified on our Zeiss Contura/PRISMO CMM (800 × 1,000 × 600 mm, MPEE = 1.5 + L/350 µm) at 20°C ± 1°C, while thin 5052-H32 bezels undergo non-contact 2.5D Optical Video Measuring System (VMS) checks (±0.003 mm).
- ✓ Ballooned First Article Inspection (FAI)
- ✓ Tactile ruby-probe CAD surface verification
- ✓ 3.5–6.0 bar pressure-decay housing leak test
90% Billet Hog-Out Stabilization
Thin-wall bulkheads removing over 90% of billet mass undergo symmetric double-sided roughing and intermediate thermal aging—150–165°C for 6061-T651, and strictly ≤ 100–110°C for 7075 alloys to prevent T6/T73 over-aging softening.
- ✓ Pre-stretched T651 / T7351 plate stock
- ✓ Custom contoured vacuum & soft-jaw fixtures
- ✓ Flatness ⏥ 0.025 mm across thin mounting webs
MIL-A-8625 & ASTM A967 Finishing
We execute MIL-A-8625 Type II and Type III hard anodizing (50 µm coat at 450–550 HV0.05), RoHS-compliant conductive chromate conversion (Alodine 1200S / SurTec 650) for EMI grounding, and zero-growth ASTM A967 passivation (~0.002 µm).
- ✓ ASTM B117 neutral salt-spray validation
- ✓ Selective dual-finish masking (Type III + SurTec)
- ✓ 304 stainless wire thread insert installation
Heat-Lot MTRs & Hardness QC
Incoming Ti-6Al-4V, 7075-T7351, 17-4PH, and Invar 36 stock is verified against authentic mill-heat Mill Test Reports (MTR), cross-checked via ASTM E18 Rockwell hardness testing (±0.5 HRC) and ISO 4287 stylus roughness profilometry.
- ✓ Heat-number Mill Test Reports (MTR)
- ✓ ASTM E18 Rockwell hardness verification
- ✓ Mitutoyo SJ-210 Ra / Rz surface reports
Technical Engineering FAQ: Aerospace & Avionics Manufacturing
Concise shop-floor answers on 5-axis titanium machining, hybrid DMLS post-milling, submerged Wire-EDM flexures, and ex-factory production turnaround schedules.
Simultaneous 5-axis trochoidal milling with high-pressure through-spindle coolant evacuates heat before Ti-6Al-4V’s low 6.7 W/m·K conductivity causes work hardening. Rigid HSK-A63 shrink-fit holders and tapered ball-nose cutters maintain ±0.015 mm (±0.0006″) blade contour accuracy and Ra 0.4 µm (16 µin) surface finish.
As-sintered DMLS Ti-6Al-4V brackets exhibit ±0.15 mm (±0.006″) thermal shrinkage and Ra 6–10 µm roughness across organic struts. We add 0.8–1.0 mm CAD machining stock to mating interfaces, perform vacuum stress-relief annealing, and 5-axis post-machine clevis bores to ISO 286 H7 (+0.018/0 mm for Ø10–18 mm).
Rotary end mills impart lateral cutting forces that deflect thin 0.30 mm compliant flexure blades and induce residual stress drift in Invar 36. Submerged Sodick Wire EDM executes one rough cut plus three to four skim passes, holding ±0.005 mm (±0.0002″) slits and Ra 0.2–0.4 µm finishes.
Following engineering DFM review within 24–48 hours, rapid CNC prototype brackets ship in 4–8 business days ex-factory, while anodized, ground, or DMLS parts complete in 7–12 business days. Batch runs require 7–30 business days ex-factory, excluding 3–5 days DHL, FedEx, or UPS air transit.
Ready to Prototype or Scale Your Aerospace Hardware?
Upload your 3D CAD models (STEP, IGES, or Parasolid) and 2D GD&T drawings for a comprehensive manufacturability review, datum-fixturing strategy, and custom production quotation from our in-house CNC, DMLS, and Wire-EDM engineering team.