In-House Precision Surface Finishing Lines · Turnkey Surface Engineering
Precision Metal & Plastic Surface Finishing Services
Enhance mechanical wear endurance, environmental corrosion resistance, and cosmetic surface elegance for prototypes and production parts. AS Prototypes delivers comprehensive, mil-spec compliant metal and plastic surface finishing with strict pre- and post-treatment dimensional tolerance control (critical registers masked or ground to ±0.005–0.010 mm / ±0.0002″–±0.0004″), precision thread masking, and Coordinate Measuring Machine (CMM) verification (available upon request). From rugged hard anodized robotic components to mirror-polished optical mold cavities, our in-house finishing division guarantees flawless batch-to-batch consistency.
1. Metal & Plastic Surface Finishing Specifications Matrix
Comparative engineering benchmarks across layer thickness, surface roughness (Ra / µin standards), dimensional tolerances, salt fog corrosion endurance, and recommended substrate pairings:
| Finishing Process | Compatible Substrates | Coating Thickness | Surface Roughness (Ra) | Corrosion & Hardness | Key Engineering Applications |
|---|---|---|---|---|---|
| Anodizing Type II (Sulfuric) | Aluminum (6061, 7075, 5052) | 5 – 25 μm (0.2–1.0 mil) (50% in / 50% out) | Ra 0.8 – 1.6 μm (32–63 μin) | 336+ hrs Salt Spray (ASTM B117) | Consumer electronics enclosures, robotics brackets, colored architectural trims. |
| Hard Anodizing Type III (Hardcoat) | Aluminum (6061-T6, 7075-T651) | 25 – 50 μm (1.0–2.0 mil) (Heavy wear layer) | Ra 1.2 – 2.4 μm (48–95 μin) | 450–550 HV0.05 (ASTM E384), 1000+ hrs Salt Spray | Aerospace hydraulic manifolds, sliding wear tracks, military-grade rugged enclosures. |
| Electroless Nickel Plating (ENP) | Steel, Stainless Steel, Copper, Aluminum | 5 – 30 μm (0.2–1.2 mil) (Uniform internal bores) | Ra 0.4 – 0.8 μm (16–32 μin) | HV 900–1000 (after bake), 1000+ hrs | Precision valve spools, pump shafts, semiconductor fittings, fluidic manifolds. |
| Electrostatic Powder Coating | Carbon Steel, Sheet Metal, Aluminum | 40 – 120 μm (1.6–4.7 mil) (Thermoset film) | Ra 2.0 – 4.5 μm (Smooth/Textured) | Extreme impact, chip & UV endurance | Precision sheet metal enclosures, telecom server racks, machine chassis. |
| Abrasive Bead Blasting | Aluminum, Stainless Steel, Titanium, Brass | 0 μm (Subtractive micro-texture) | Ra 1.2 – 3.2 μm (48–125 μin, #80–#150) | Uniform satin matte, anti-glare | Tooling cutter mark removal, optical instrument housings, medical device chassis. |
| Chemical Passivation (ASTM A967) | Stainless Steel (303, 304, 316L, 17-4PH) | 0 μm (Atomic Cr2O3 passive film) | Preserves baseline Ra | Eliminates free iron, ASTM B117 tested | Surgical medical instruments, food machinery, cleanroom hardware. |
| Black Oxide (MIL-DTL-13924) | Carbon Steel, Alloy Steel, Stainless Steel (Class 4) | < 1 μm (True zero dimensional change) | Preserves ground Ra | Anti-reflective, oil-retentive | Optical lens barrels, CNC fixtures, spline shafts, precision gears, fasteners. |
| Precision Zinc Plating & Galvanizing | Carbon Steel, Alloy Steel, Sheet Metal | 5 – 25 μm (Electro) / 45 – 85 μm (HDG) | Ra 1.6 – 3.5 μm | Cathodic sacrificial zinc barrier | Outdoor structural brackets, chassis frames, heavy machinery mounting plates. |
| Optical Mirror Polishing (SPI A-1) | Hardened Mold Steels (S136), Acrylic, PC | 0 μm (Subtractive diamond lapping) | Ra 0.012 – 0.025 μm (0.5–1.0 μin) (SPI A-1 Mirror) | Ultra-high reflectivity & mold release | Injection mold tool cavities, optical reflectors, clear light pipes. |
| Hard Chrome Plating (AMS 2460) | 40Cr, 4140, Tool Steels, Cast Iron | 20 – 100 μm (Industrial thick layer) | Ra 0.2 μm (Precision ground OD) | Rockwell C 65–70 (HV 850–1050) | Hydraulic cylinder piston rods, severe sliding pins, wear bushings, roll shafts. |
| Chemical Vapor Smoothing (3D Nylon) | HP MJF & SLS PA12, PA11, TPU | 0 μm (Surface remelt levelling) | Ra drops from 8.0 to < 1.5 μm | 100% Water & Gas Impermeable | Automotive ducts, fluidic manifolds, functional wearable orthotics, enclosures. |
| Chemical Vapor Polishing (PC & ABS) | Polycarbonate (PC), ABS | 0 μm (Controlled vapor smoothing) | Ra < 0.05 μm (Water-clear clarity) | Annealed (60–80°C Constant-Temp for PC) | Microfluidic analytical chips, transparent fluid manifolds, medical sight glasses. |
2. In-House Surface Finishing Capabilities & Texture Gallery
Inspect macro surface textures, layer thicknesses, and specific engineering applications across our comprehensive in-house and validated chemical processing lines:
Precision Anodizing (Type II & Type III Hardcoat)
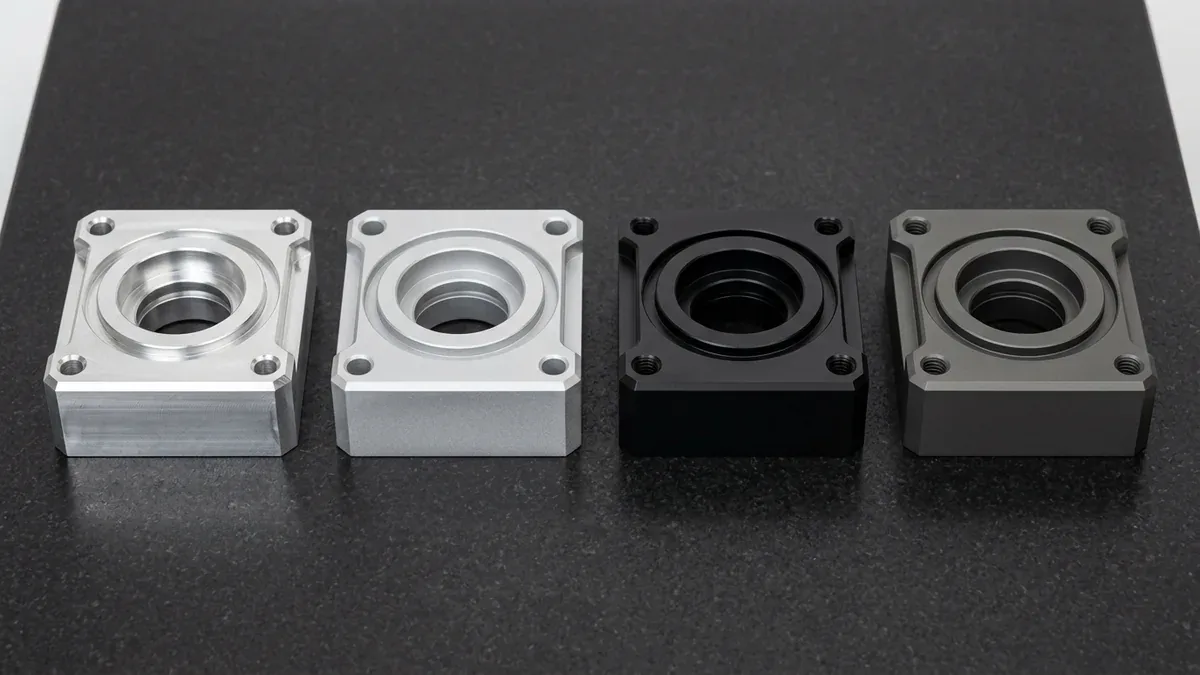
Electrochemical conversion creating a durable aluminum oxide barrier. Type II Sulfuric (5–25 μm) provides vibrant cosmetic color dyeing and 336h salt spray protection. Type III Hardcoat (25–50 μm) delivers extreme abrasive wear resistance reaching 400–550 HV.
High-Phosphorus Electroless Nickel Plating (ENP)
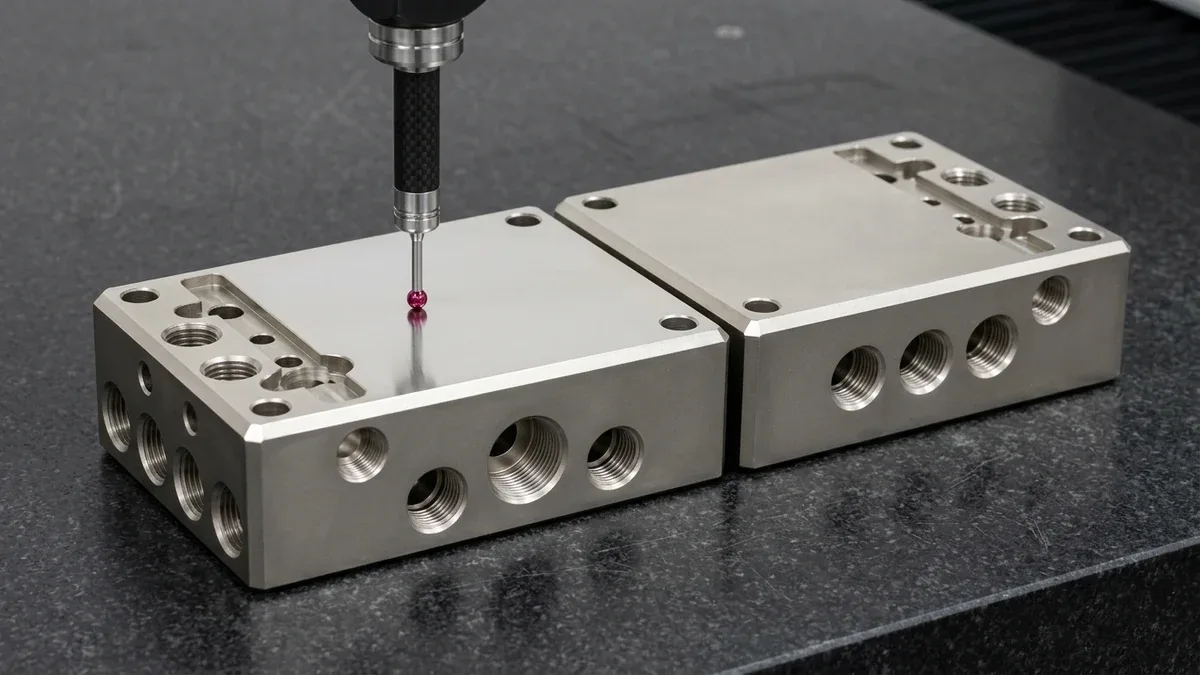
Autocatalytic chemical reduction depositing 100% uniform layer thickness across internal cross-drilled channels, deep blind bores (aspect ratio 1:4), and precision threads without edge buildup. High-phosphorus (10–13% P) is non-magnetic with 1,000h+ salt spray endurance.
Electrostatic Powder Coating Services
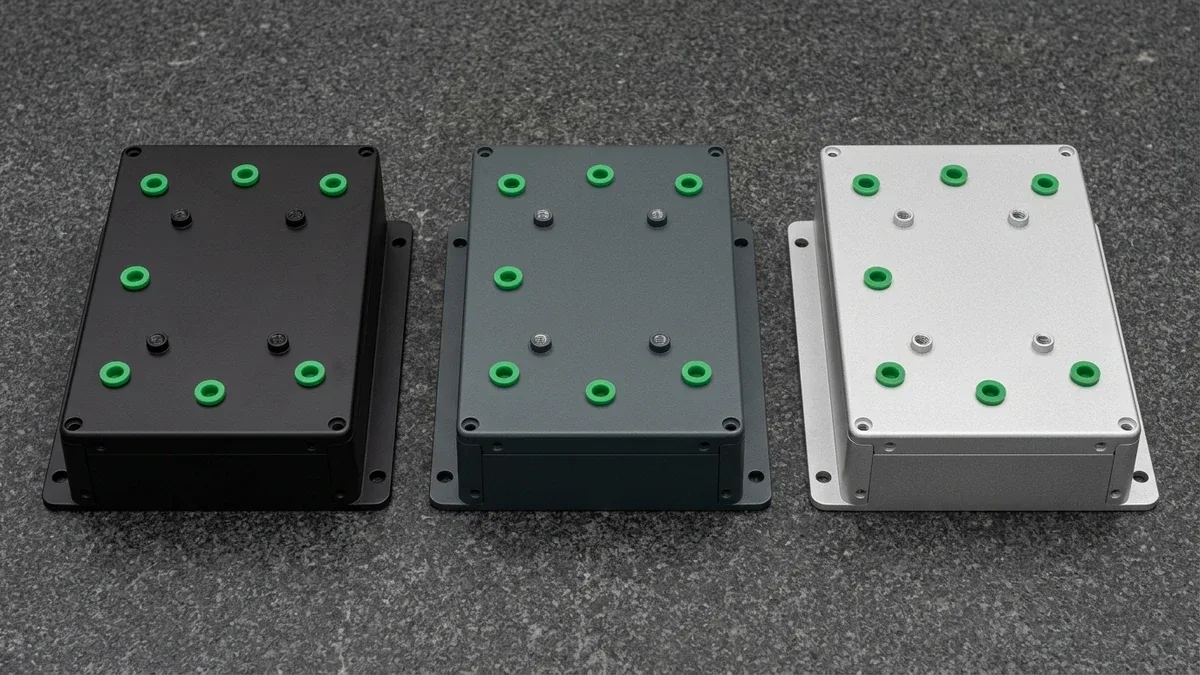
Finely atomized thermoset polymers cured under 200°C heat. Superior impact resistance, chip resistance, and UV stability for sheet metal enclosures, brackets, and robot chassis. Available in fine texture, sand grain, smooth satin, and heavy wrinkle.
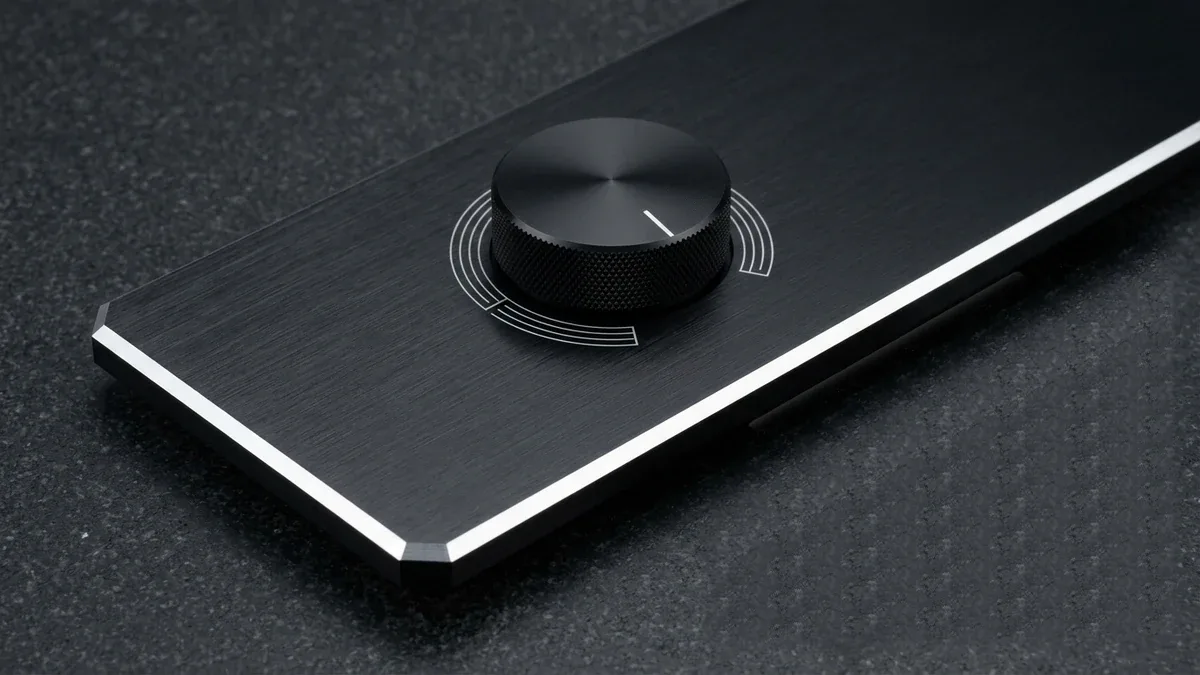
Mechanical Bead Blasting & Hairline Brushing
Calibrated #80 to #150 glass and ceramic beads eliminate CNC cutter marks, micro-deburr sharp edges, and produce a uniform satin matte finish. Precision linear and circular brushing (#180 to #400 grit) creates distinctive directional hairline graining for front bezels.
Precision Silk Screen, Pad Print & Laser Engraving
High-definition graphics, regulatory CE/FCC legends, dial graduations, and traceability barcodes. Industrial 2-component epoxy inks withstand chemical wipes (ASTM D3359 5B). Fiber laser ablation generates crisp white high-contrast legends and permanent serialized codes.
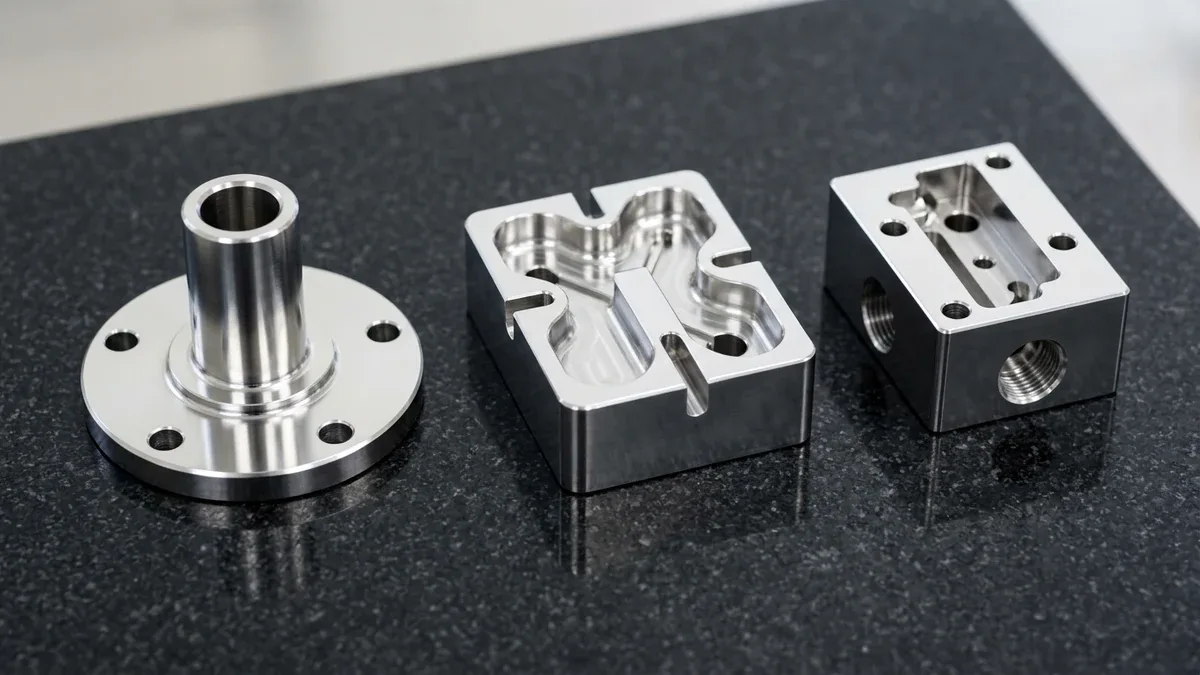
Chemical Passivation & Electropolishing
Nitric or citric acid decontamination selectively removes exogenous free iron from machined stainless steel, accelerating the formation of a dense, corrosion-resistant chromium oxide film (Cr2O3) for medical device hardware with zero dimensional shift.
Precision Black Oxide Conversion Coating
Hot alkaline conversion coating transforming surface iron into black magnetite (Fe3O4). Delivers deep non-reflective optical absorption with anti-galling lubrication retention for spline shafts, drive gears, tooling fixtures, and optical mounts with zero dimensional growth.
Precision Zinc Plating & Galvanizing Services
Sacrificial zinc coatings offering robust outdoor atmospheric rust defense. Electro-galvanizing (5–25 μm blue-white, yellow, or black zinc) preserves fine thread engagement, while hot-dip galvanizing (45–85 μm) provides decades of outdoor structural barrier protection.
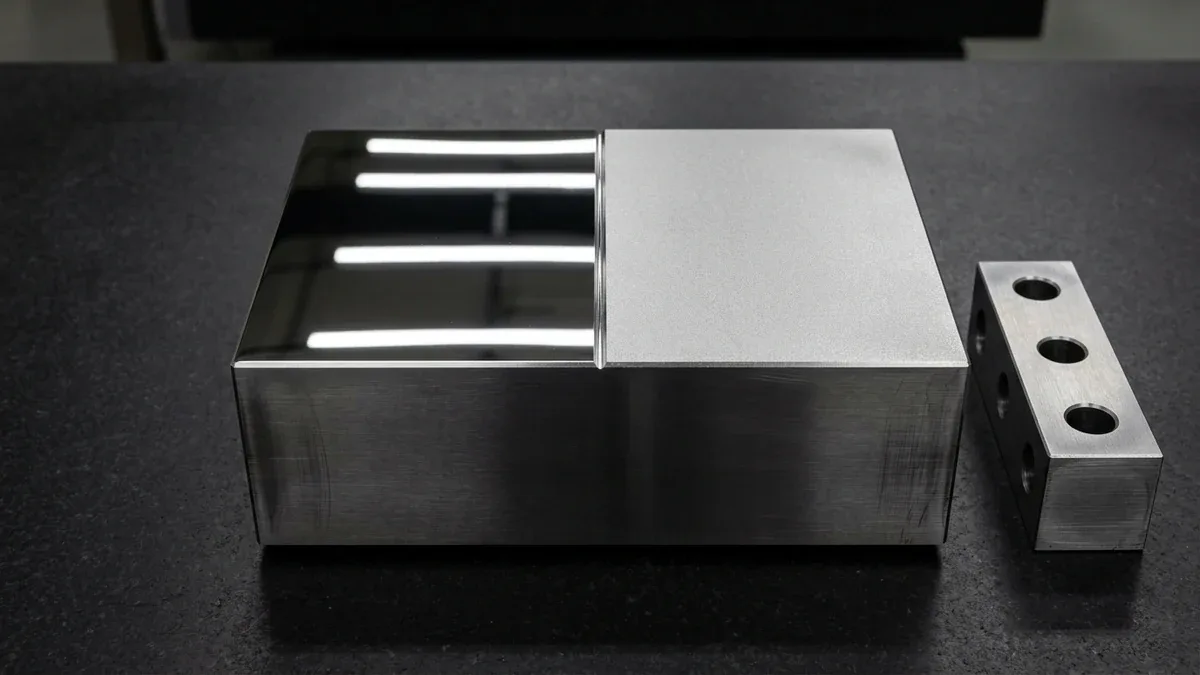
Optical Mirror Polishing (SPI A-1 / A-2)
Multi-stage diamond paste hand-lapping eliminating microscopic tool marks and EDM recast layers down to Ra 0.012 – 0.025 μm (SPI A-1). Engineered for injection mold tooling cores, acrylic light pipes, and laser mirror surfaces with zero orange peel.
Heavy-Duty Industrial Hard Chrome Plating
Functional hard chrome electrodeposition depositing a dense, micro-cracked chromium structure. Offers extreme surface hardness (65–70 HRC), low coefficient of sliding friction (0.12), and exceptional galling resistance for hydraulic piston rods and pins.
Industrial 3D Printing Chemical Vapor Smoothing
Automated vapor chamber processing that selectively liquefies and reshapes polymer micro-pores. Transforms rough, powdery HP MJF and SLS nylon components into smooth, semi-gloss, injection-molded quality parts that are 100% airtight and watertight (rated 2–3 bar).
Optical Diamond Flycutting (PMMA) & Solvent Vapor Polishing (PC)
Specialized optical finishing combining ultra-precision diamond flycutting for PMMA with controlled solvent vapor smoothing for PC and ABS. PMMA (Acrylic) is machined using Single-Point Diamond Flycutting (SPDT) and multi-stage diamond buffing to achieve SPI A-1 optical clarity without chemical solvents. Polycarbonate (PC) and ABS undergo controlled solvent vapor smoothing (DCM/acetone vapor reflow) for complex internal cross-drilled channels, followed by mandatory 60–80°C constant-temperature stress-relief annealing to eliminate micro-crazing.
3. Surface Finishing DFM & Dimensional Tolerance Compensation
Achieving post-finishing dimensional perfection requires exact coordination between CAM cutter toolpaths and chemical bath buildup characteristics:
Type III Hardcoat (CAM Pre-Compensation)
Type III hardcoat builds up 50% on the exterior surface and penetrates 50% into the aluminum substrate. A 50 μm total coating adds 25 μm outward per surface (+50 μm on outer diameter, -50 μm on inner bore diameter).
Real-World Engineering Practice: Because chemical bath coating tolerances (±5–10 μm) and blind bore Faraday cage effects exceed ultra-tight bearing tolerances, critical bearing journals tighter than ±0.010 mm (e.g., Φ 20.000 +0.010/0 mm) are masked with custom silicone plugs during anodizing or precision diamond reamed/ground post-coating to ensure exact nominal press fits.
Custom Silicone Thread & Bore Masking
Because 60° thread flank geometry displaces radially by 2t (1/sin 30°), diametral pitch diameter clearance reduces by 4t (4× additive coating thickness). For 100% additive plating (such as 25 μm ENP), pitch diameter shrinks by ~100 μm, locking standard fasteners unless masked or tapped with 6G/6e clearance taps.
Protection Standards: We utilize tapered high-temperature silicone plugs (M2 to M24), pull-through cords, and precision die-cut Kapton tape dots to shield blind threaded holes, reamed dowel pin registers, and electrical grounding pads. Threads remain 100% clean, paint-free, and pass Go/No-Go thread gauge inspection immediately.
True Zero-Growth Chemical Finishes (< 1 μm)
When ultra-precise mating tolerances (±0.005 mm) cannot accommodate additive coating thickness, zero-growth chemical conversion processes are ideal.
Available Processes: Chemical Passivation (ASTM A967, < 0.1 μm), Black Oxide (MIL-DTL-13924, < 1 μm), and Chromate Conversion (SurTec 650 / Alodine 1200S, < 0.8 μm) convert surface metallurgy without adding measurable dimensional shift, ensuring zero interference in tight assembly stacks.
| Surface Finish / Coating | Total Film Thickness | Net Outward Growth per Surface | Impact on External OD / Internal Bore ID | Mandatory CAM & Masking DFM Protocol |
|---|---|---|---|---|
| 1. Type II Sulfuric Anodizing (MIL-A-8625) | 8 – 20 μm | +4 to +10 μm per side (50% in / 50% out) | OD grows +8–20 μm; Bore ID shrinks –8–20 μm | Plug H7 bearing bores and M2–M6 fine threads with tapered silicone plugs; pre-bead-blast (#120) to hide milling cutter marks. |
| 2. Type III Hardcoat Anodizing (MIL-A-8625) | 25 – 50 μm | +12.5 to +25 μm per side (50% in / 50% out) | OD grows +25–50 μm; Bore ID shrinks –25–50 μm | Apply CAM pre-machining offset or mask tight registers (≤ ±0.010 mm); radius sharp external edges (R ≥ 0.2–0.5 mm) to prevent corner flaking. |
| 3. Electroless Nickel Plating (ASTM B733) | 5 – 30 μm | 100% additive buildup (+5 to +30 μm/side) | OD grows +10–60 μm; Thread pitch diameter shrinks 4 × t | Deposits 100% uniformly inside blind bores; tap threads with oversized 6G/6e taps or mask threaded holes prior to chemical bath immersion. |
| 4. Chromate Conversion (Alodine / SurTec 650) | 0.2 – 0.8 μm | < 0.5 μm (True Zero-Growth Conversion) | Zero measurable shift on ±0.005 mm fits | Ideal for EMI/RFI electrical grounding lands and tight dowel/bearing bores where insulating anodized layers are prohibited. |
| 5. Chemical Passivation (ASTM A967) & Black Oxide | < 0.1 – 1.0 μm | Zero dimensional growth (0 μm shift) | Preserves exact CNC machined & ground tolerances | Requires zero masking; specify on 304/316L/17-4PH surgical stainless steel and 4140 alloy steel spline shafts. |
| 6. Electropolishing (ASTM B912) | –5 to –15 μm (Subtractive) | Removes 5–15 μm of surface peaks per side | OD shrinks –10–30 μm; Bore ID enlarges +10–30 μm | Micro-deburrs external thread crests and levels surface roughness down to Ra < 0.2 μm for cleanroom and UHV manifolds. |
| 7. Electrostatic Powder Coating | 60 – 120 μm | 100% additive thermoset film (+60–120 μm/side) | Adds 0.12–0.24 mm across mating sheet metal edges | Mask all PEM self-clinching nuts, studs, grounding pads, and sliding chassis rails with high-temp silicone caps and die-cut Kapton dots. |
| 8. PC Solvent Vapor Polishing vs. PMMA SPDT | 0 μm (Reflow / Lapping) | Ra drops to < 0.05 μm optical clarity | Preserves microfluidic channel geometry | PC/ABS requires mandatory 60–80 °C constant-temp oven annealing to prevent solvent stress crazing; PMMA must be mechanically diamond-milled/buffed (never solvent-fumed). |
4. Coating Metrology, Environmental Reliability Testing & Packaging
Every surface treatment batch is validated against rigorous international test standards in our quality inspection laboratory:
5. Production Turnaround Schedules & Logistics
Turnaround Terms: All schedules represent factory completion and quality inspection sign-off (Ex-Factory Production & Inspection Turnaround). International priority air express delivery (via DHL, FedEx, or UPS) requires an additional 3 – 5 Business Days depending on destination customs clearance.
6. Frequently Asked Questions (FAQ)
How do you mathematically account for coating thickness during CNC machining?
How is color consistency guaranteed across different anodizing production batches?
How do you protect critical internal threads and tight bores during hardcoating or plating?
What is the primary difference between Chemical Passivation and Electropolishing for stainless steel?
What is the realistic turnaround time for finished prototype and production parts?
Elevate Your Machined & Fabricated Parts with Production-Grade Finishes