Precision Grinding Services: CNC Surface & Cylindrical OD
Core Precision Grinding Capabilities & In-House Fleet
Our in-house grinding department utilizes thermally regulated synthetic coolant filtration alongside vitrified white alumina, Cubic Boron Nitride (CBN), and diamond-bonded abrasive wheels tailored to hardened tool steels, stainless alloys, and cemented carbides, maintaining consistent ±0.005 mm (±0.0002″) dimensional stability across prototype and batch runs.
1. Precision CNC Surface Grinding (Okamoto AR-618S)
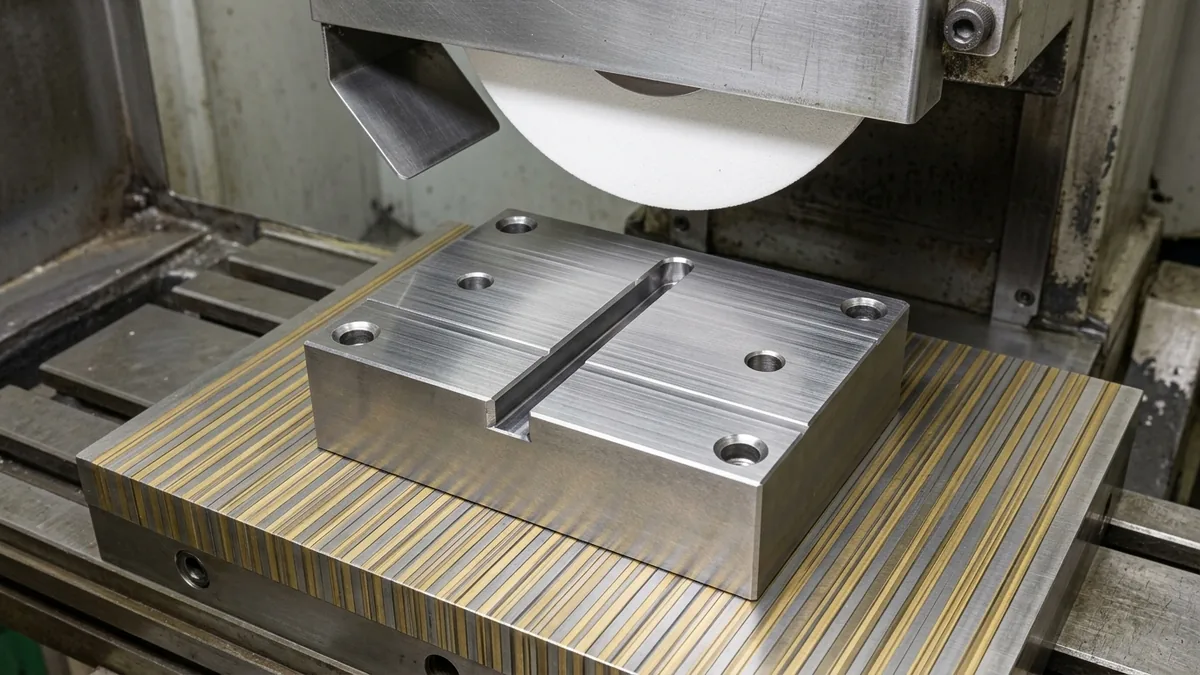
Precision Computer Numerical Control (CNC) surface grinding produces flat reference datums and coplanar guideways across hardened steel and carbide workpieces. Operating two in-house Okamoto AR-618S horizontal-spindle surface grinders with fine-pole electromagnetic chucks and 0.001 mm digital micro-downfeed resolution (as shown finishing the slotted D2 die block), we hold ±0.005 mm (±0.0002″) thickness tolerances.
- Primary Geometry: Hardened die blocks, linear guideways, mold core plates, shim spacers, and shear blades.
- In-House Envelope: Up to 600 × 300 × 250 mm (23.6″ × 11.8″ × 9.8″) across 2 Okamoto AR-618S units.
- Geometric Dimensioning and Tolerancing (GD&T): Flatness ≤ 0.005 mm / 100 mm; Parallelism ≤ 0.005 mm (0.0002″); Ra 0.1–0.4 μm (Ra 0.2 μm std).
2. External Diameter (OD) Cylindrical Grinding (Palmary ODC-3250)
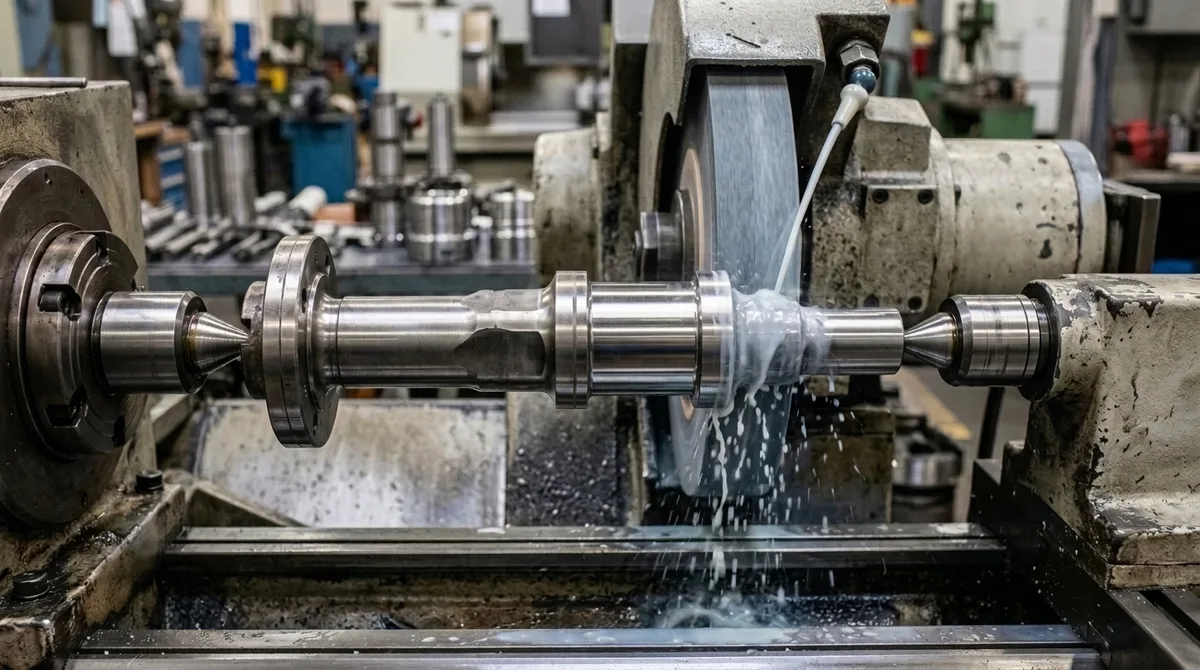
External diameter (OD) cylindrical grinding finishes rotational shafts, bearing seats, and hydraulic valve spools mounted between precision dead and live 60° centers or in collet chucks. Our in-house Palmary ODC-3250 cylindrical grinder eliminates post-quench bow and lobing (as shown on the multi-stepped transmission shaft), holding roundness and runout within 0.005 mm (0.0002″).
- Primary Geometry: Stepped motor shafts, bearing journals, hydraulic valve spools, pump rotors, and eccentric pins.
- In-House Envelope: Max diameter Ø320 mm (12.6″) × length 500 mm (19.7″) between centers (1 Palmary ODC-3250 unit).
- Key GD&T Controls: Roundness & Cylindricity ≤ 0.005 mm (0.0002″); Total Radial Runout ≤ 0.005 mm (0.0002″) TIR; Ra 0.1–0.2 μm.
3. Step, Shoulder Face & Wear-Plate Datum Grinding
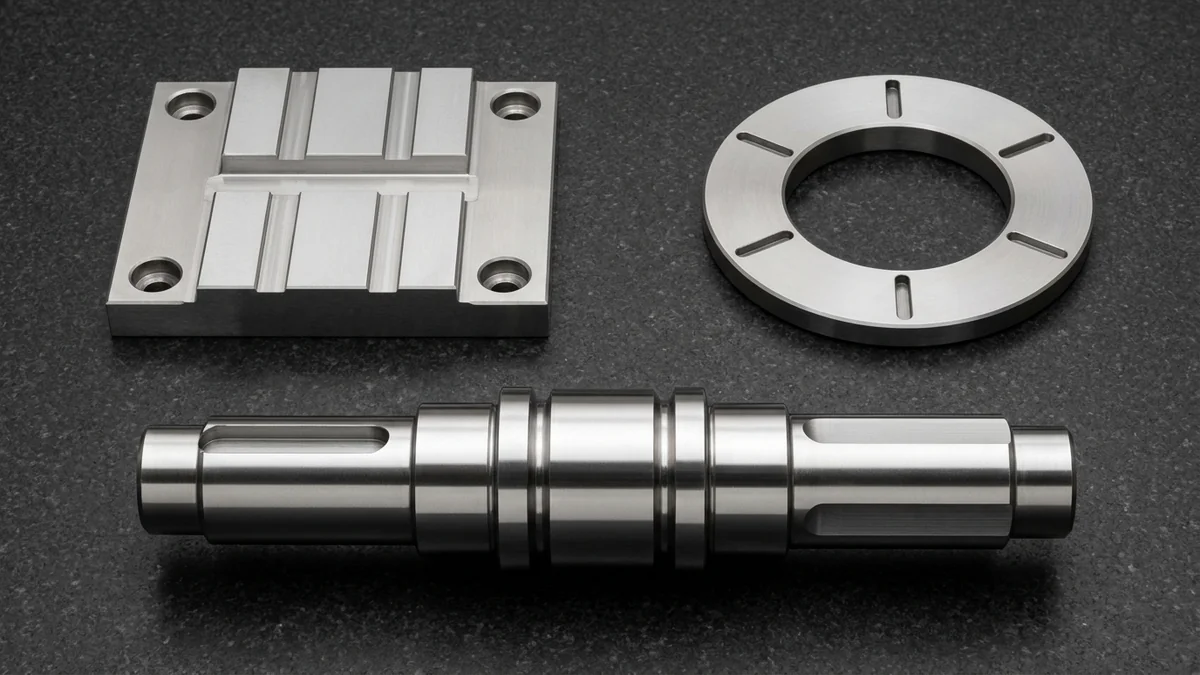
Step and shoulder-face grinding establishes perpendicular axial thrust faces, recessed guideway slots, and coplanar sealing lands on heat-treated components. Using dressed wheel profiles on our Okamoto and Palmary grinders, we finish stepped bearing journals, slotted wear plates, and radially grooved thrust rings (as shown in the ground 4140, 17-4PH, and D2 component set).
- Primary Geometry: 4140 stepped shafts with DIN 509 relief grooves, 17-4PH slotted wear plates, and D2 grooved thrust washers.
- Setup & Envelope: Planar steps within 600 × 300 × 250 mm; shouldered shafts within Ø320 × 500 mm.
- Key GD&T Controls: Shoulder perpendicularity ≤ 0.005 mm (0.0002″); step height ±0.005 mm (±0.0002″); Ra 0.1–0.2 μm (4–8 μin).
4. Hardened Internal Profiles via Sodick Wire EDM
Because peripheral and external OD wheels cannot enter small hardened openings, we finish internal through-bores, involute splines, keyways, and stamping die apertures (58–65 HRC) on three in-house Sodick ALN400Qs linear-motor wire Electrical Discharge Machining (EDM) units using 1 rough cut plus 3–4 skim cuts.
- Geometry: Hardened internal splines, keyways, punch retainer bores, and tight die openings (Rmin ≥ 0.07 mm).
- In-House Envelope: 400 × 300 × 250 mm (0.10–0.25 mm brass/tungsten wire, Qty 3).
- Accuracy & Surface Integrity: ±0.005 mm (±0.0002″); Ra 0.2 μm (8 μin) with recast white layer controlled to ≤ 1–2 μm.
5. Slender Pins & Micro-Shafts via STAR Swiss Turning
For precision dowel pins, surgical mandrels, and valve stems from Ø0.5 mm to Ø32.0 mm (0.020″–1.25″), six in-house STAR Micronics Swiss-type sliding-headstock lathes with tungsten carbide guide bushings hold ±0.005 mm (±0.0002″) diameters and 0.005 mm (0.0002″) TIR concentricity in a single setup.
- Geometry: High-aspect-ratio guide pins, miniature stepped shafts, sensor probes, and medical mandrels.
- Bar Capacity: Ø0.5 mm to Ø32.0 mm across STAR BS-12-H, SB-20R, and SR-32JM cells (Qty 6).
- Key GD&T: Concentricity ≤ 0.005 mm (0.0002″) TIR without center-hole or centerless rest fixtures.
Precision Grinding Tolerances & In-House Machine Specifications
| In-House Process & Fleet | Max Workpiece Envelope (mm) | Dimensional Tolerance (mm) | Geometric Tolerance (GD&T) | Surface Roughness (Ra μm) | Recommended Application / When to Choose |
|---|---|---|---|---|---|
| CNC Surface Grinding (Okamoto AR-618S × 2) | 600 × 300 × 250 mm (23.6″ × 11.8″ × 9.8″) | ±0.005 mm (±0.0002″) | Flatness & Parallelism ≤ 0.005 mm / 100 mm | Ra 0.1–0.4 μm (Ra 0.2 μm / 8 μin std) | Best for hardened D2/H13/S136 mold plates, linear guideways, shim spacers, and coplanar datum blocks |
| Cylindrical OD Grinding (Palmary ODC-3250 × 1) | Ø320 × 500 mm (Ø12.6″ × 19.7″) | ±0.005 mm (±0.0002″) | Roundness, Cylindricity & Runout ≤ 0.005 mm (0.0002″) | Ra 0.1–0.2 μm (4–8 μin) | Best for hardened 4140/440C motor shafts, hydraulic valve spools, bearing journals, and eccentric pins |
| Step, Shoulder Face & Thrust-Ring Grinding | 600 × 300 mm planar / Ø320 × 500 mm rotary | ±0.005 mm (±0.0002″) | Shoulder Perpendicularity ≤ 0.005 mm (0.0002″) | Ra 0.1–0.2 μm (4–8 μin) | Best for multi-stepped shafts with DIN 509 relief undercuts, slotted wear plates, and grooved thrust washers |
| Hardened Internal Profiles (Sodick ALN400Qs Wire EDM × 3) | 400 × 300 × 250 mm (15.7″ × 11.8″ × 9.8″) | ±0.005 mm (±0.0002″) | Profile & Hole Pitch ≤ 0.005 mm (Rmin ≥ 0.07 mm) | Ra 0.2–0.4 μm (1 rough + 3–4 skim cuts) | Best for hardened internal through-bores, involute splines, sharp keyways, and stamping die openings |
Materials & Hardness Spectrum: Tool Steels to Tungsten Carbide
Precision grinding excels where solid carbide end mills and turning inserts suffer rapid flank wear or edge chipping against high-hardness martensitic microstructures and abrasive ceramics. Our in-house grinding cell processes hardened tool steels, precipitation-hardened stainless steels, carbides, and plated wear surfaces:
Wheel Type: Vitrified CBN or high-purity white alumina with tangential synthetic coolant.
Applications: Valve spools, pump shafts, surgical tooling. Light downfeed prevents work hardening.
Wheel Type: Resin-bonded and metal-bonded diamond abrasive wheels with precision dressing.
Limitations: Soft, gummy 6061 aluminum and thermoplastics are excluded to prevent abrasive wheel loading.
Metrology & Quality Assurance: 20 °C ± 1 °C Verification Down to ±0.005 mm
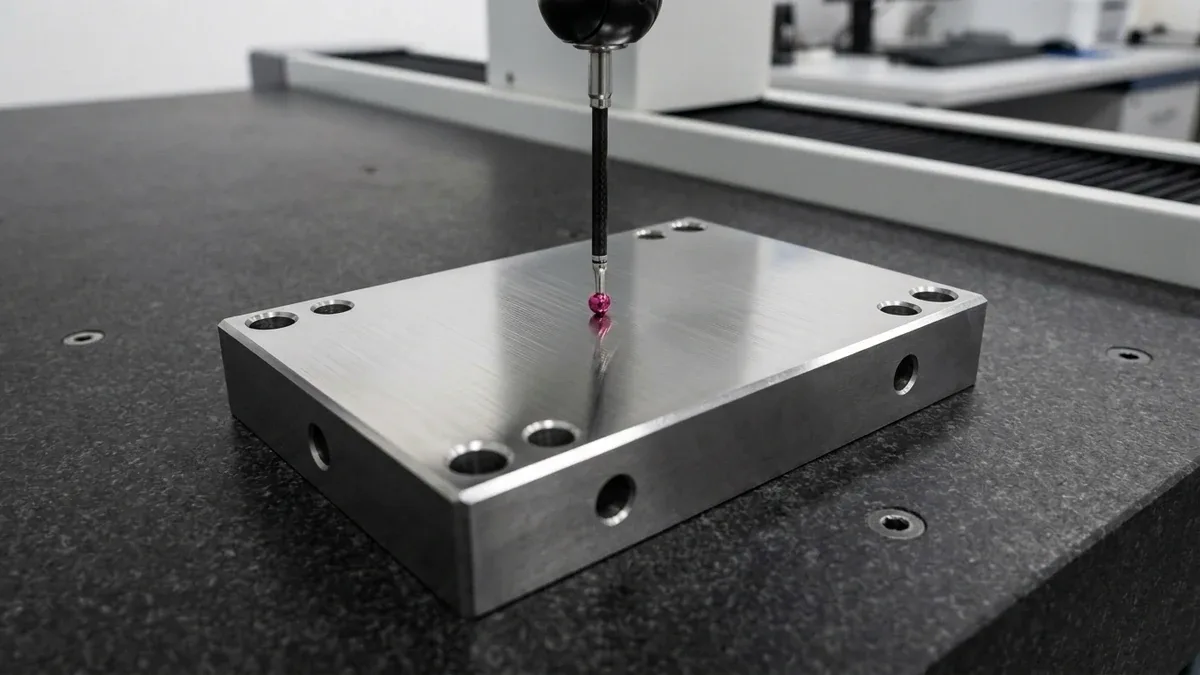
Tight-tolerance abrasive finishing requires thermally stabilized dimensional verification. Inside our dedicated 20 °C ± 1 °C (68 °F ± 1.8 °F) climate-controlled metrology laboratory, parts undergo ultrasonic cleaning and thermal soak before inspection with calibrated in-house metrology instruments (as shown probing the surface-ground datum plate):
- Zeiss Contura Bridge CMM (Available Upon Request): Multi-point ruby probing on our Zeiss CNC Coordinate Measuring Machine (CMM) (800 × 1,000 × 600 mm, MPEE = 1.5 + L/350 μm) verifies flatness, parallelism, cylindricity, and datum relationships.
- TESA Height Gauge & Between-Centers Runout Checks: A TESA Micro-Hite 700 glass-scale height gauge (±0.002 mm repeatability, 0.001 mm resolution), 0.001 mm micrometers, and lever dial test indicators verify step heights and radial runout (TIR).
- ISO 4287 Contact Stylus Roughness Profiling: Mitutoyo Surftest SJ-210 diamond-tip stylus profilometers (2 μm radius) quantify Ra, Rz, and Rq values down to Ra 0.1 μm (4 μin) on sealing journals.
- ASTM E18 Hardness & FAI Documentation: Digital Rockwell HRC hardness testing (±0.5 HRC), Mill Test Reports (MTR), and ballooned First Article Inspection (FAI) reports supplied upon request.
Engineering DFM Guidelines for Precision Grinding
Incorporating grinding-specific Design for Manufacturability (DFM) features into 3D CAD models and 2D tolerance drawings prevents wheel-corner binding, eliminates magnetic clamping springback on thin plates, and avoids costly secondary setups:
| Grinding DFM Feature | Recommended Drawing Specification | Abrasive Kinematics & Recommended Action |
|---|---|---|
| 1. Grinding Relief Undercuts (DIN 509) | Specify DIN 509 Form E (OD grinding only) or Form F (OD + perpendicular shoulder face) | Prevents the dressed wheel corner radius from binding against the shaft shoulder, ensuring 100% flush bearing seating. |
| 2. 60° Center Holes (DIN 332) | Include precision 60° lapped center holes on both shaft ends for between-centers OD grinding | Establishes a single common rotational datum across stepped journals, holding coaxiality and radial runout ≤ 0.005 mm. |
| 3. Pre-Grind Stock Allowance | Leave 0.10–0.20 mm per side (0.20–0.40 mm total on diameter or thickness) prior to heat treatment | Cleans up furnace decarburization scale and quench warpage without excessive CBN/alumina wheel loading or thermal burn. |
| 4. Thin Plate Stiffness (Surface Grind) | Keep ferromagnetic plate thickness ≥ 3.0 mm (0.118″) or allow shimmed flip-grinding spark-out cycles | Electromagnetic chucks pull thin warped sheets flat during cutting, causing elastic bow springback unless stress-relieved. |
| 5. Hardened Internal Bores & Splines | Design hardened internal profiles as through-features (≥ Ø2.0 mm start hole, corner R ≥ 0.07 mm) | Routes hardened bores and keyways to Sodick ALN400Qs wire EDM (1 rough + 3–4 skim cuts) without quill deflection or taper. |
| 6. Slender Shaft Aspect Ratio (L/D) | Maintain shaft L/D ≤ 8:1 for unsupported between-centers OD grinding; route Ø0.5–Ø32 mm slender pins to Swiss turning | Prevents radial grinding-wheel normal force from bowing slender shafts at mid-span and inducing barrel cylindricity error. |
| 7. Interrupted Journals & Non-Magnetic Parts | Mill keyways/cross-holes before final OD grinding; provide parallel blocking edges on non-magnetic 316L/carbide | Prevents wheel bounce across interrupted slots and secures non-ferromagnetic parts that cannot be held by bare magnets. |
| 8. Selective Fine-Grit Ra Callouts | Specify Ra 0.2–0.4 μm (8–16 μin) on standard ground fits; reserve Ra 0.1 μm (4 μin) for dynamic rotary seals | Fine-grit spark-out to Ra 0.1 μm requires frequent diamond wheel dressing and extended passes, doubling finishing time. |
When Should You Grind Instead of Hard Turning or Milling?
Precision grinding is an abrasive finishing process that holds hardened steel, cemented carbide, and ceramic parts to ≤ 0.005 mm (0.0002″) roundness, ≤ 0.005 mm / 100 mm flatness, and Ra 0.1–0.4 μm (4–16 μin) roughness. Select it when hard turning or milling reaches physical limits:
| Decision Factor (Unit) | Choose Precision Grinding (Recommended Use Case) | When Hard Turning / CNC Milling Is Preferred |
|---|---|---|
| Workpiece Hardness (HRC / HV) | 55–65 HRC quenched tool steels, cemented carbide (1,500+ HV), and technical ceramics | Annealed/pre-hardened alloys ≤ 45 HRC (or hard turning up to 52–55 HRC with PCBN tooling) |
| Roundness & Cylindricity (mm) | Roundness & cylindricity ≤ 0.005 mm (0.0002″) between dead/live 60° centers | Roundness ≤ 0.010–0.015 mm (0.0004″–0.0006″) on standard CNC chucker/turning centers |
| Surface Roughness (Ra μm) | Ra 0.1–0.4 μm (4–16 μin; Ra 0.2 μm std) free of periodic single-point feed cusps | Ra 0.4–1.6 μm (16–63 μin) as-milled or single-point turned |
| Flatness & Parallelism (mm) | ≤ 0.005 mm / 100 mm (0.0002″ / 4″) across hardened datum plates | ≥ 0.015–0.030 mm / 100 mm face-milled (uncalled features per ISO 2768-mK) |
| Applicable Part Geometry | Planar plates, guide rails, external OD shafts, stepped shoulders, and flat thrust rings | 3D freeform pockets, threads, undercuts, and gummy 6061/7075 aluminum or engineering plastics |
| Process Route Stage | Final datum and journal sizing after vacuum quenching and tempering (4–8d ex-factory prototypes) | Complete machining of unhardened alloys or pre-heat-treat roughing with 0.20–0.40 mm stock |
What Is the Best Process Route for Hardened Precision Parts?
Precision grinding serves as the final datum-locking stage in a hardened-part route: rough-machine soft stock with grinding allowance, heat-treat to target hardness, cut internal profiles via wire EDM, and finish-grind external datums. Consult our steel heat treatment guide and DFM engineering hub for pre-heat-treat planning.
Industry Solutions: Where High-Precision Grinding Is Essential
Frequently Asked Questions (FAQ)
What dimensional tolerances and surface finishes can AS Prototypes achieve with precision grinding?
When should I choose precision grinding over CNC hard milling or wire EDM?
Can you grind parts that have already undergone heat treatment?
What are your maximum workpiece dimensions for surface and cylindrical OD grinding?
How do you finish hardened internal bores, splines, and slender micro-pins?
How do you prevent grinding burn and micro-cracks in hardened steel?
How much stock should I leave for grinding after heat treatment?
How do I submit an RFQ for precision grinding, and what files are required?
What affects precision grinding cost and turnaround time?
Need High-Precision Surface or Cylindrical OD Grinding?
Upload your 3D CAD models (STEP, STP, or IGES) and 2D PDF engineering drawings specifying material grade, target HRC hardness, GD&T datums, and Ra surface finish. Our in-house engineering team reviews DIN 509 relief undercuts, pre-grind stock allowances, and Okamoto/Palmary fixture setups to deliver a custom production quotation.