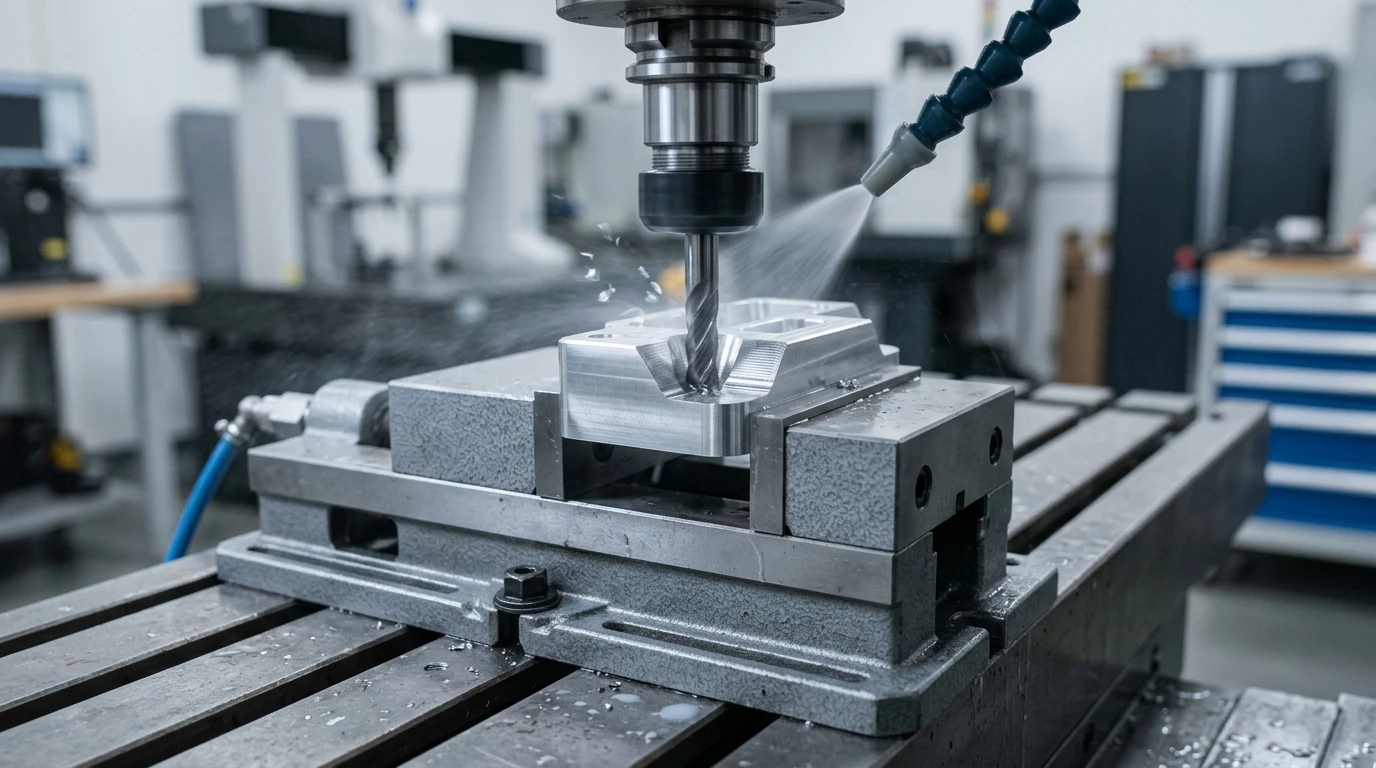
From precision-machined internal combustion engine (ICE) cylinder heads to high-voltage electric vehicle (EV) motor stator housings, CNC milling in automotive manufacturing is the core technological engine delivering vehicle reliability, acoustic comfort, and lightweight energy efficiency. As vehicle architectures shift toward high-RPM electric powertrains and integrated electronic chassis systems, the mechanical requirements placed on structural castings and billets have intensified. Thin-walled aluminum die castings with micro-channel liquid cooling passages, bearing seats spinning at 20,000 RPM, and lightweight 5-axis suspension uprights demand precision geometric dimensioning and tolerancing (GD&T), automated in-spindle metrology probing, and vibration-damped high-speed machining centers.
Core Automotive Subsystems Driven by Precision CNC Milling
Modern automotive component manufacturing leverages multi-axis CNC milling across diverse mechanical and thermal domains:
1. Electric Vehicle (EV) Powertrain & Battery Enclosures
Electric drivetrains integrate the motor, inverter, and reduction gearbox into compact “3-in-1” aluminum drive units. CNC milling machines post-process high-pressure die-cast (HPDC) aluminum cases to establish bearing journal concentricity within ±0.010 mm (±0.0004 in). Additionally, battery thermal management systems require extensive face milling across large liquid cold plates (up to 1,200 mm long) to achieve surface flatness within 0.03 mm, ensuring continuous thermal interface material (TIM) contact with pouch cells.
2. Engine Heads, Blocks & Forced-Induction Subsystems
High-efficiency combustion and hybrid engines rely on multi-axis CNC milling for complex intake/exhaust port profiling, multi-angle valve seat contouring, and deep-hole oil gallery gun-drilling. For turbochargers, 5-axis simultaneous CNC machining cuts aerodynamic titanium (Ti-6Al-4V) and aluminum compressor impellers from solid forged billets, generating continuous blade curvatures that withstand centrifugal forces at 150,000+ RPM.
3. Lightweight Chassis & Steering Knuckles
Unsprung weight directly governs vehicle handling dynamics and braking distance. Suspension uprights (knuckles), control arms, and high-performance multi-piston brake calipers are CNC milled from forged 6061-T6 or 7075-T6 aluminum. Deep weight-relieving pockets are milled while maintaining rigid bearing bores and ball-joint tapers.
Advanced Machining Strategies in Automotive CNC Milling
In our in-house automotive CNC milling facility, multi-axis machining centers are optimized for high-throughput and tight-tolerance consistency:
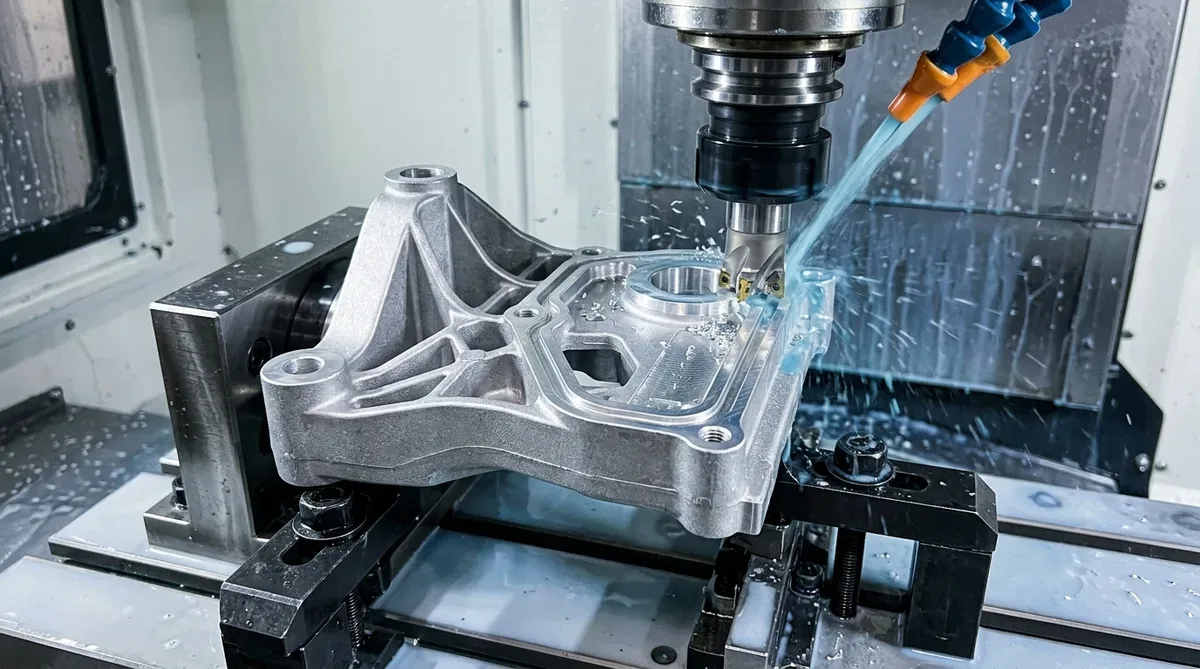
- High-Pressure Through-Spindle Coolant (70+ Bar): High-velocity coolant delivery blasts directly through micro-holes inside cutting tools, instantly evacuating chips from deep cross-drilled cooling ports and lubricating cutting edges to eliminate localized heat buildup and workpiece thermal distortion.
- Horizontal Machining Centers (HMC) with Tombstone Fixturing: Multi-sided cast iron tombstones mounted on dual-pallet changers allow operators to load 8 to 16 automotive components in one station while the machine cuts unattended inside the enclosure. Gravity-assisted chip fall prevents chip recutting.
- Automated Renishaw Touch Probing: In-spindle radio touch probes automatically locate raw casting datum bosses, establish dynamic work coordinate offsets (WCS), and perform in-process bore diameter checks before unclamping.
Automotive CNC Milling Subsystems & Tolerances Matrix
The table below summarizes primary automotive components, material specifications, machine configurations, and critical GD&T regimes:
| Automotive Component | Material Specification | Recommended Machine Type | Critical GD&T Tolerance Target |
|---|---|---|---|
| EV Motor Stator Housing | Cast Al A356 / A380 or Forged 6061 | 4-Axis HMC with Rotary Table | Bearing bore runout ≤ 0.008 mm, O-ring groove depth ±0.015 mm |
| Battery Liquid Cold Plate | Extruded Al 6063 / Sheet Al 3003 | High-Speed Large-Bed 3-Axis VMC | Flatness ≤ 0.03 mm across 800 mm mating face |
| Turbocharger Impeller (Blisk) | Forged Ti-6Al-4V / 2618 Aluminum | 5-Axis Continuous Simultaneous VMC | Blade profile tolerance within ±0.010 mm; dynamic balance |
| Suspension Steering Knuckle | Forged 7075-T6 / Ductile Iron QT500 | 4-Axis HMC with Dual Vises | Wheel bearing bore concentricity ±0.006 mm |
| Multi-Piston Brake Caliper | Forged 6061-T6 / Gray Cast Iron | 4-Axis VMC with Specialized Boring Bars | Piston bore cylindricity ≤ 0.008 mm; fluid port M10x1.0 threads |
Automotive Aluminum Alloy Selection: Cast vs. Forged
Understanding the mechanical and machinability trade-offs between raw material forms is critical for automotive engineering:
| Alloy Classification | Tensile Strength (MPa) | Machinability Index | Primary Automotive Application |
|---|---|---|---|
| Cast A356-T6 (Sand / Permanent Mold) | 230 – 260 MPa | Good (Silicon content requires PCD tooling) | Engine blocks, transmission cases, intake manifolds |
| Die-Cast A380 (HPDC) | 310 MPa | Moderate (High silicon, prone to tool wear) | High-volume gearbox covers, electronic housing lids |
| Forged / Billet 6061-T6 | 290 – 310 MPa | Excellent (100% benchmark, smooth chips) | EV subframes, prototype battery boxes, caliper bodies |
| Forged / Billet 7075-T6 | 540 – 570 MPa | Very Good (High hardness, crisp chip break) | Suspension control arms, racing uprights, driveshaft yokes |
Quality Control, CMM & Metrology Validation
Every automotive component machined in our automotive machining facility undergoes comprehensive metrology validation before final international packaging and release:
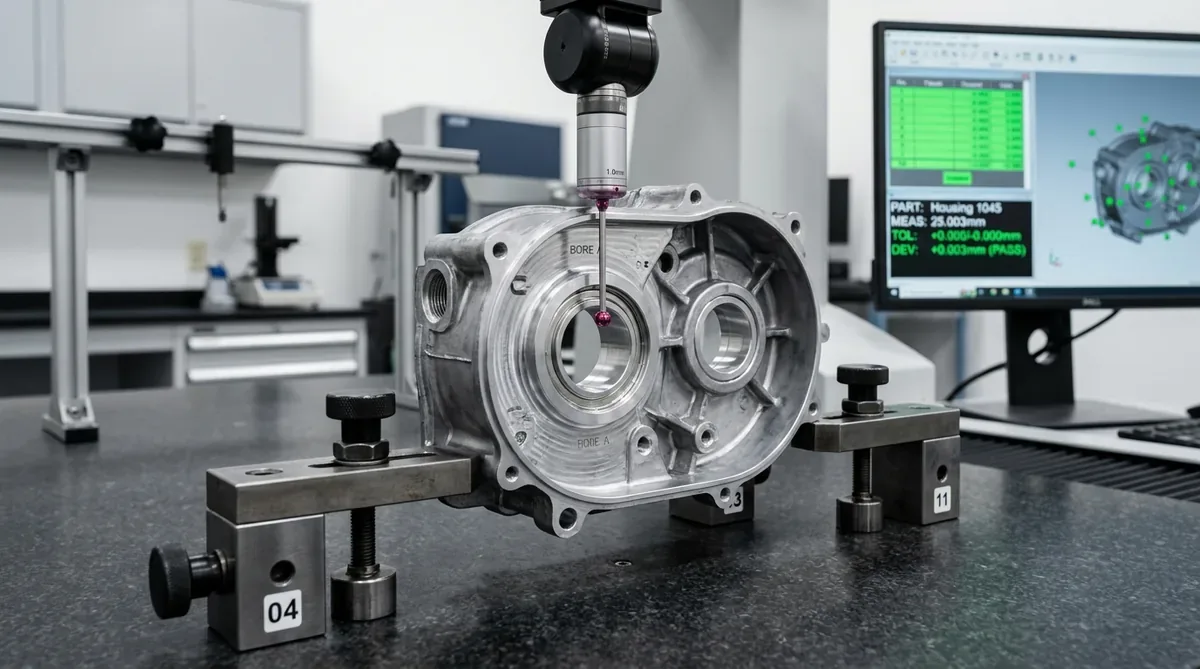
- Precision Coordinate Measuring Machine (CMM): Probing true position, parallelism, and multi-axis concentricity in a temperature-controlled metrology laboratory (20°C ± 0.5°C).
- Automated Helium Leak Testing: Checking EV battery cooling plates and fluid manifold weldments under vacuum to guarantee zero fluid porosity.
- Surface Roughness Profilometry: Confirming Ra 0.4 µm finishes across bearing journals and O-ring sealing gland channels.
EV drive unit casings combine internal helical gear shafts, stator coolant channels, and multi-angle electrical connection ports in a single housing. 4-axis HMC machining with a rotary table allows accessing multiple faces, deep bearing journals, and angled wire-harness ports in a single setup, eliminating positional tolerance stack-up and cutting fixturing costs.
Milling large, thin-walled aluminum plates releases internal residual stresses, causing bowing. We prevent warpage by utilizing pre-stretched stress-relieved plates (Al 6061-T651 or cast MIC-6 plate), deploying multi-pass balanced roughing routines on opposing faces, and utilizing vacuum chucks with high-feed cutter paths that minimize heat transfer into the workpiece.
Yes. Our CNC machine shop regularly machines raw die-cast, sand-cast, and investment-cast aluminum blanks. We design custom hydraulic clamping fixtures and utilize in-spindle Renishaw probing to establish datum alignment on cast reference pads, holding precision bearing and sealing tolerances.
Fixturing and Datum Strategy for Automotive Housings and Knuckles
Automotive housings and steering knuckles hold critical features to ±0.010 to ±0.020 mm only when one consistent datum scheme and rigid workholding carry from the first operation through final inspection.
- Shared datum scheme: Establish datums A, B and C on rough-machined faces in the first operation, then reuse the same dowel-pin locators in later operations so every feature is referenced to the same surfaces.
- Repeatable fixturing: Dedicated hydraulic or zero-point modular fixtures with hardened locating pins allow re-clamping with repeatability in the range of a few micrometers, which prevents stack-up between operations.
- Thin-wall deformation control: Clamp on stiff ribs and bosses with balanced force, then release and re-clamp lightly before a 0.2 to 0.3 mm finishing pass so clamping stress does not spring back after unclamping.
- In-process probing: A spindle touch probe verifies work offsets and bore positions after roughing, so any drift is corrected before finishing cuts commit the part.
Combining these four practices keeps multi-operation housings and knuckles within drawing tolerance without relying on operator judgment, and it creates the traceable measurement record that automotive programs expect when parts move from prototype to pilot builds.
Accelerate Your Automotive Production Programs with AS Prototypes
From rapid prototype EV motor casings and 5-axis impellers to series-production chassis components, AS Prototypes delivers precision multi-axis CNC milling, precision GD&T tolerances (per drawing), and robust DFM support for the world’s most demanding automotive engineers.