

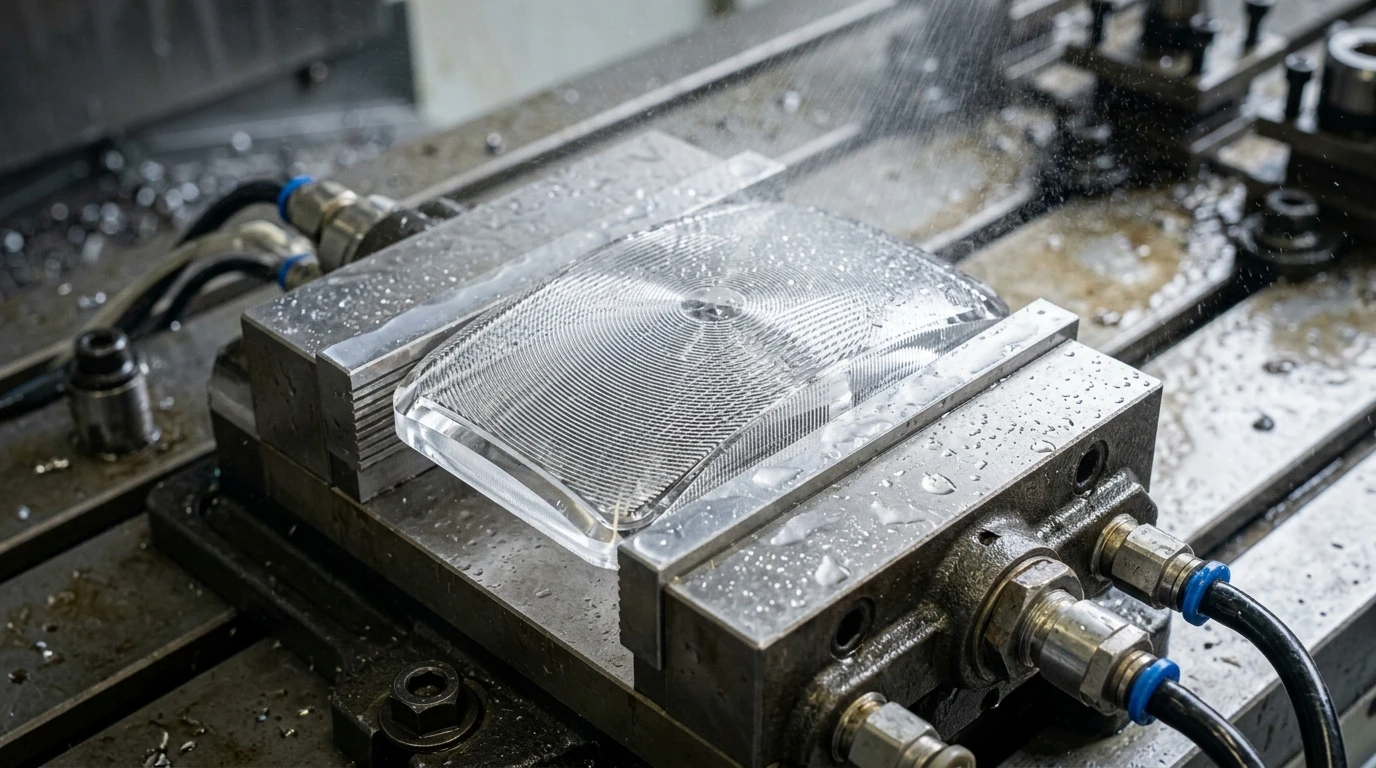
In contemporary automotive design, the rear lighting signature is the defining brand identifier of the vehicle at night. From continuous full-width coast-to-coast LED light blades and animated dynamic turn indicators to multi-depth 3D light tunnels, modern taillamps have evolved from basic signaling fixtures into complex mechatronic optical assemblies.
However, taking an aesthetic lighting concept from early sketch to series production requires navigating extreme regulatory compliance (ECE and SAE photometric distributions), environmental durability, and multi-material hermetic sealing. Implementing a structured automotive rear light development and multi-stage verification framework ensures that optical light guides, multi-shot injection moldings, and ultrasonic weld seams perform flawlessly under real-world vehicle operations.
Stage 1: Optical Architecture & Rapid Prototype Diamond Machining
The initial stage transforms 3D styling surfaces into functional optical light guides governed by Total Internal Reflection (TIR):
- Optical Light Guide Engineering: Thick-wall optical PMMA light pipes must distribute concentrated LED flux into a completely homogeneous, glare-free ribbon. Micro-optical extraction prisms (flutes or stepped facets) are calculated to progressively strip light out of the core at precise angles.
- Single-Point Diamond Milling (SPDM): In our machine shop, prototype light pipes and freeform reflector cavities are cut on ultra-precision 5-axis CNC machining centers. Monocrystalline diamond cutters with micro-stepovers achieve surface roughness below Ra 0.05 µm, eliminating post-machining distortion and enabling immediate goniophotometric validation before cutting production tooling.
- Vacuum Metallization (PVD Deposition): Inner reflector housings undergo high-vacuum physical vapor deposition of pure aluminum (80–120 nm) sealed with a silicon dioxide (SiO2) topcoat, achieving greater than 90% specular reflectivity.
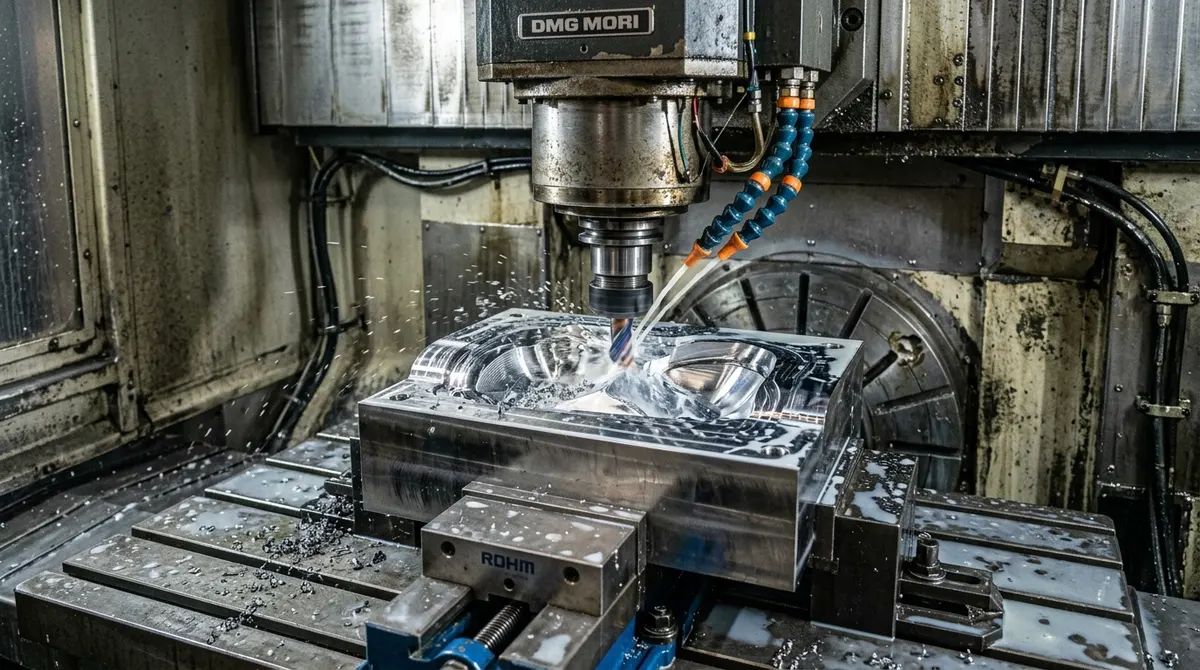
Stage 2: Multi-Shot Tooling (2K / 3K Injection Molding)
Modern rear lamps integrate multiple colors and structural plastics into a single unified lens to eliminate unsightly exterior seam lines:
- Rotary Platen & Core-Back Tooling: 2K and 3K injection molds utilize rotating platen or index-plate mechanisms to sequentially shoot clear PMMA (outer lens), transparent red PMMA (tail and stop functions), transparent amber PMMA (turn signals), and black ABS/PC (housing bezel).
- Differential Shrinkage Management: Different tinted polymer batches exhibit subtle shrinkage variances. Our tooling engineers utilize conformal cooling circuits and balanced hot runner gate locations to prevent internal stress birefringence (optical rainbowing) and joint delamination during cooling.
Stage 3: Lens-to-Housing Joining & Hermetic Sealing
The structural rear housing must be permanently joined to the transparent outer PMMA/PC lens without particulate contamination. Hot-plate and vibration welding are deployed when joining PMMA/PC lenses to matching polar ABS/PC housings; when mineral-filled polypropylene (PP-TD20) housings are specified, automated robotic dispensing of 1K/2K Polyurethane (PUR) structural adhesive is required to overcome polymer polarity incompatibility and ensure hermetic IP6K9K sealing:
- Hot-Plate Welding vs. Vibration Welding: For complex 3D curved perimeters, servo-driven hot-plate welding or linear vibration welding melts matching weld ribs under controlled displacement, creating an airtight, continuous joint with shear strength exceeding base resin limits.
- Breather Vent Integration: Automotive taillamps experience rapid internal pressure swings during rainstorms or vehicle washes. Micro-porous ePTFE membrane vents (Gore-Tex vents) are laser-welded over housing ports, equalizing air pressure while barring liquid water and fine dust particles (IP67/IP6K9K rating).
Multi-Stage Verification Roadmap
The table below summarizes the four milestone phases in automotive rear lamp engineering and verification:
| Development Stage | Key Engineering Activities | Primary Tooling / Manufacturing Route | Core Verification Milestone |
|---|---|---|---|
| Phase 1: Concept Optical Validation | Optical simulation (SPEOS), light pipe prism layout | 5-Axis Diamond CNC Milling & Optical Diamond Buffing | Goniophotometer luminous flux & homogeneity check |
| Phase 2: Design Verification (DVT) | Multi-material fit, LED PCB thermal routing, weld rib layout | Rapid Tooling (7075 Al / P20 Mold Base) | Thermal shock (-40°C to +85°C) & vibration endurance |
| Phase 3: Production Verification (PVT) | Multi-cavity 2K/3K hardened production mold trials | Class 101 Hardened S136 / H13 Steel Tooling | 100% ECE / SAE regulatory compliance & FAIR metrology |
| Phase 4: Serial Launch (SOP) | Automated robotic welding, in-line leak testing | Fully automated molding & ultrasonic assembly cells | Zero-defect delivery and CPK ≥ 1.67 process capability |
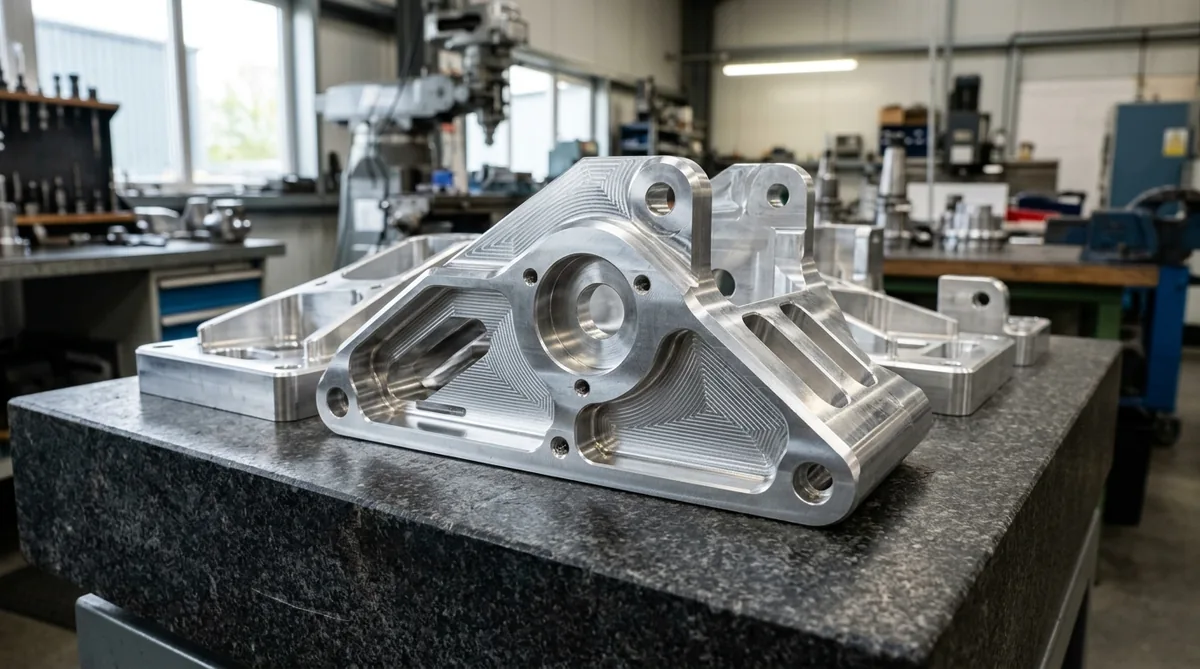
Material Selection for Rear Lighting Subsystems
Selecting appropriate resins across the automotive lighting prototyping assembly ensures long-term resistance to environmental weathering:
| Subsystem Component | Recommended Polymer Grade | Key Optical / Mechanical Attribute | Crucial Manufacturing Consideration |
|---|---|---|---|
| Outer Red / Clear Lens | Optical PMMA (Plexiglas / Altuglas) | 92% light transmittance, UV yellowing immunity | SPI-A1 mirror mold cavity polish, uniform wall thickness |
| High-Impact Outer Cover | Optical Polycarbonate (PC) | High impact ductility, resists stone chips | Requires UV-cured polysiloxane hardcoat against scratching |
| Inner Reflector Bezel | High-Heat PC or PEI | Thermal deflection >135°C, zero outgassing | PVD vacuum aluminizing with plasma SiO2 topcoat |
| Structural Rear Housing | ABS/PC Blend or PP-TD20 | High torsional stiffness, dimensional stability | Consistent weld rib geometry for vibration welding |
Stage 4: Photometric & Environmental Homologation
Before an automotive taillight enters commercial production, physical prototypes undergo rigorous homologation testing:
- Goniophotometric Photometry: Calibrated automated detector arms measure luminous intensity (candela) across horizontal and vertical angular test grids, confirming full compliance with ECE Regulations R7, R6, R23, and SAE J586/J588.
- Climatic Thermal Shock & Condensation Testing: Subjecting the complete sealed assembly to -40°C to +85°C thermal cycles at 95% relative humidity to prove that internal lens fogging dissipates within standard regulatory timeframes (typically under 15 minutes).
- High-Pressure Ingress Protection (IP6K9K): Exposing weld seams and cable harness grommets to 100-bar rotational hot water jets (80°C) to guarantee total moisture exclusion.
Optical PMMA (Acrylic) has superior inherent UV weatherability, retaining crystal clarity and rich red/amber coloration without yellowing over the entire 15-year lifespan of a vehicle. In contrast, standard Polycarbonate requires expensive anti-UV hardcoats to prevent solar degradation. PMMA also provides a higher light transmittance (92%) and exceptional surface gloss.
Homogeneous illumination is achieved by combining total internal reflection (TIR) light pipes with precision-calculated micro-optical extraction facets or diamond-milled diffusing flutes. The micro-prisms are graduated in spacing along the light guide length to release an equal amount of lumen flux at every point, avoiding localized bright spots or dark fade-outs.
Hot-plate welding and vibration welding are the industry standards for automotive rear lamps. Hot-plate welding provides a continuous, highly hermetic molten bead with minimal mechanical stress, while vibration welding offers fast 3-to-5 second cycle times with strong molecular interlocking along complex 3D perimeter contours.
Light Guide and Lens Surface Quality Requirements
Rear lamp light guides and lenses depend on optical-grade surface quality, because scratches, flow marks and haze scatter light and appear as visible hot spots when the lamp is illuminated.
- Tool surface finish: Optical features are cut or polished to mirror finishes in the SPI A-1 to A-2 range, since the molded surface reproduces every tool mark.
- Light guide geometry: Total internal reflection requires smooth sidewalls and generous bend radii, because tight bends and rough surfaces let light leak out of the guide before it reaches the emitting face.
- Material transmission: PMMA transmits roughly 92 percent of visible light and polycarbonate about 88 percent, which is one reason PMMA is favored for light guides and PC for impact-exposed outer lenses.
- Inspection under illumination: Inspect parts with the lamp energized in a dark room as well as under normal light, since weld lines, sink marks and gate vestige often appear only when the lamp is lit.
Checking these four items on early prototypes avoids discovering optical defects only after production tooling is complete, and it supports the multi-stage verification roadmap from diamond-machined samples to homologation testing.
Accelerate Your Automotive Lighting Programs with AS Prototypes
From single-point diamond milled light guides and rapid 2K tooling to complete ECE/SAE-compliant prototype rear lamp assemblies, AS Prototypes provides comprehensive optical engineering, fabrication, and verification support to bring your vehicle lighting designs to life.







