

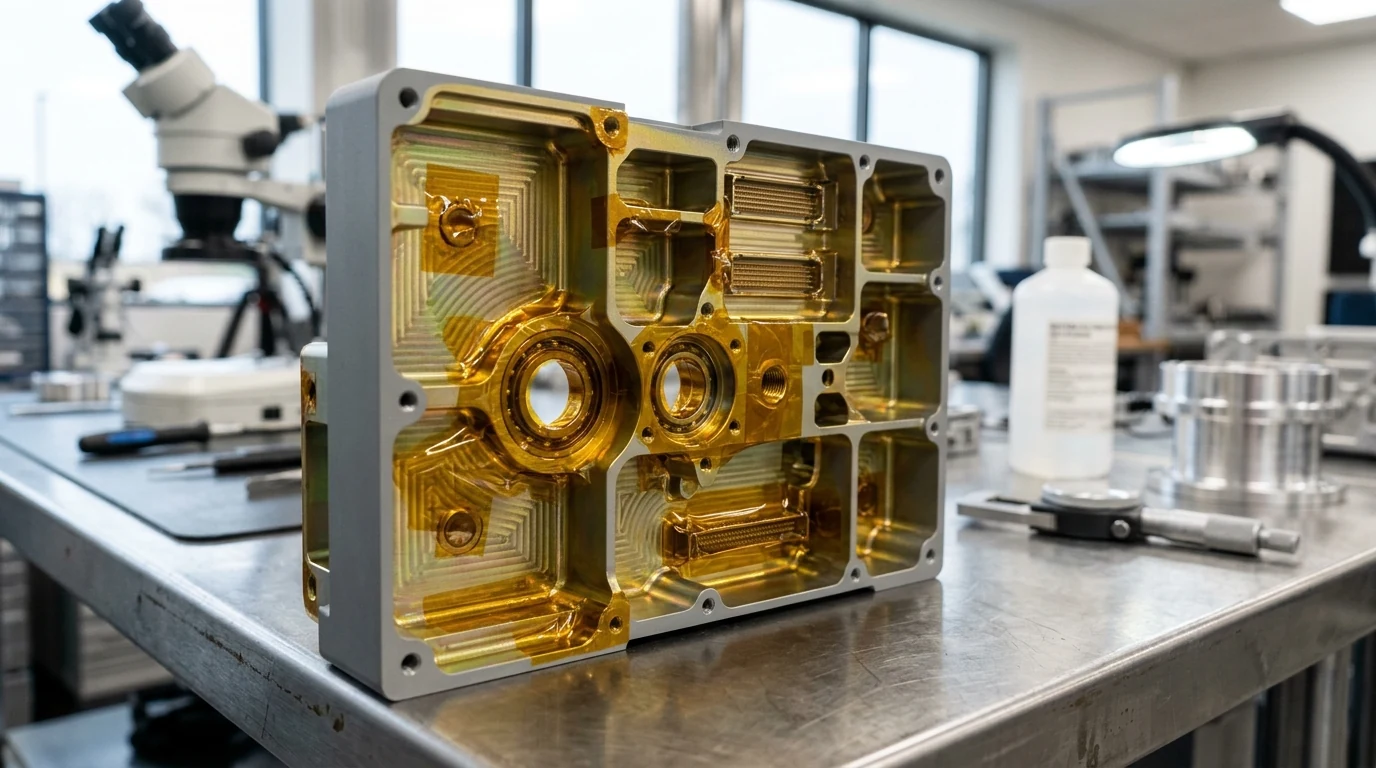
Aerospace prototype painting is a mission-critical finishing discipline designed to protect flight hardware against corrosive de-icing fluids, hydraulic Skydrol leakage, intense ultraviolet radiation, and extreme aerodynamic friction. Unlike commercial cosmetic coating, aerospace finishing requires exacting chemical pre-treatments, tightly controlled dry film thickness (DFT), and aerospace-grade primers and topcoats. In our specialized aerospace manufacturing and surface finishing facility, adhering to rigorous application parameters ensures structural and avionics prototypes endure harsh operational environments without coating delamination.
1. Multi-Layer Aerospace Coating Architecture
Modern aircraft component finishing relies on an engineered multi-tier coating system where each layer serves a specialized protective function:
- Tier 1: Chemical Pretreatment & Conversion Coating: Bare aluminum substrates (such as 2024, 6061, or 7075) undergo degreasing, acid deoxidization, and chemical conversion coating (Alodine / MIL-DTL-5541 Class 1A or Class 3). This microscopic passivation layer provides baseline corrosion protection and provides microscopic mechanical keying for subsequent primers.
- Tier 2: Corrosion-Inhibiting Epoxy Primers (MIL-PRF-23377): Strontium chromate or non-chromate zinc phosphate inhibited epoxy primers are applied at thicknesses of 15 µm to 25 µm. These primers form a cross-linked barrier against chemical permeation and actively passivate microscopic substrate scratches.
- Tier 3: Polyurethane Intermediate / Topcoats (MIL-PRF-85285): High-solids, aliphatic polyurethane topcoats provide flexibility, extreme UV degradation resistance, and chemical immunity to phosphate ester hydraulic fluids (Skydrol). Applied at 40 µm to 55 µm DFT in lusterless matte, semi-gloss, or high-gloss specifications.
| Coating System Layer | Standard Specification | Target Dry Film Thickness (DFT) | Cure Cycle / Drying | Primary Functional Role |
|---|---|---|---|---|
| Chemical Pretreatment | MIL-DTL-5541 Type II Class 1A | Molecular conversion (< 1 µm) | Ambient dry (15 – 30 min) | Corrosion passivation & paint adhesion base |
| Epoxy Primer | MIL-PRF-23377 Type I Class C2 | 15 – 23 µm (0.6 – 0.9 mil) | Touch: 2h / Recoat: 4h / Full: 7d | Chemical barrier & corrosion inhibition |
| Polyurethane Topcoat | MIL-PRF-85285 Type I Class H | 45 – 55 µm (1.8 – 2.2 mil) | Tack-free: 4h / Dry hard: 8h | Skydrol resistance, UV barrier, color/gloss |
| EMI Conductive Coating | MIL-DTL-83528 (Ni/Ag Acrylic) | 25 – 38 µm (1.0 – 1.5 mil) | Air dry (1h) / Oven cure: 65°C | Internal cavity RF/EMI attenuation (60-80 dB) |
2. Precision Masking Disciplines for Critical Interfaces
Aerospace prototypes feature intricate functional mating interfaces that must remain completely free of overspray. Excessive paint build-up inside bearing bores or on electrical bonding pads causes catastrophic assembly failures:
- Electrical Grounding & Bonding Pads: Radio frequency shielding and lightning dissipation require bare conductive surfaces (surface contact resistance < 2.5 mΩ). These areas are pre-treated with conductive Class 3 chromate conversion and masked with custom die-cut polyimide (Kapton) tapes before spray painting.
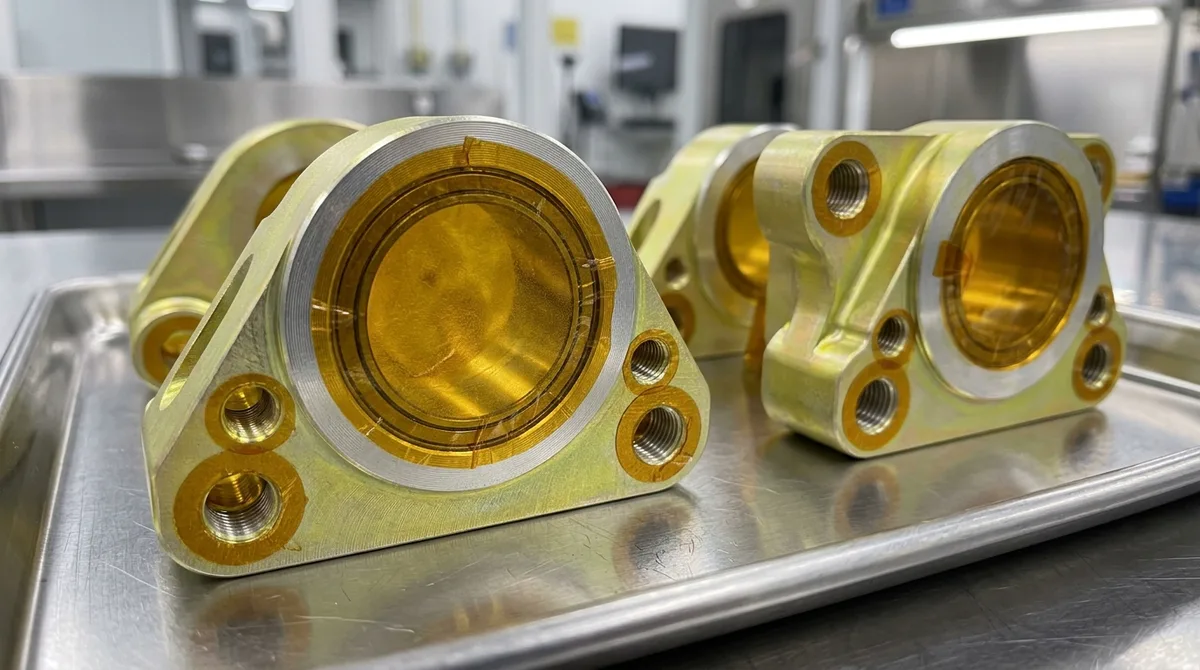
- Threaded Fastener Holes & Helicoil Inserts: All internal blind and through threads are sealed using high-temperature silicone rubber plugs or threaded vinyl caps. Coating ingress into threads alters bolt torquing friction coefficients and ruins clamping preloads.
- Precision Tolerance Mating Bosses: High-tolerance slip-fit bearing bores and dowel pin holes (tolerance ±0.008 mm) must be plugged with precision-turned Delrin or aluminum masking bungs to prevent micro-deflection during spray passes.
3. Cleanroom Environmental Control & Spray Kinematics
Aerospace coatings are notoriously sensitive to ambient humidity and particulate contamination during the flash-off and curing phases:
- Climate Control Parameters: Our spray booths operate within strict temperature boundaries of 20°C to 25°C with relative humidity controlled between 40% and 60%. Relative humidity exceeding 70% accelerates polyurethane polyisocyanate moisture curing, producing microscopic blisters and surface orange peel.
- HVLP & Electrostatic Atomization: Utilizing High-Volume Low-Pressure (HVLP) spray guns operating at 1.5 to 2.0 bar atomization pressure ensures transfer efficiencies greater than 65%, minimizing overspray turbulence on contoured flight surfaces.
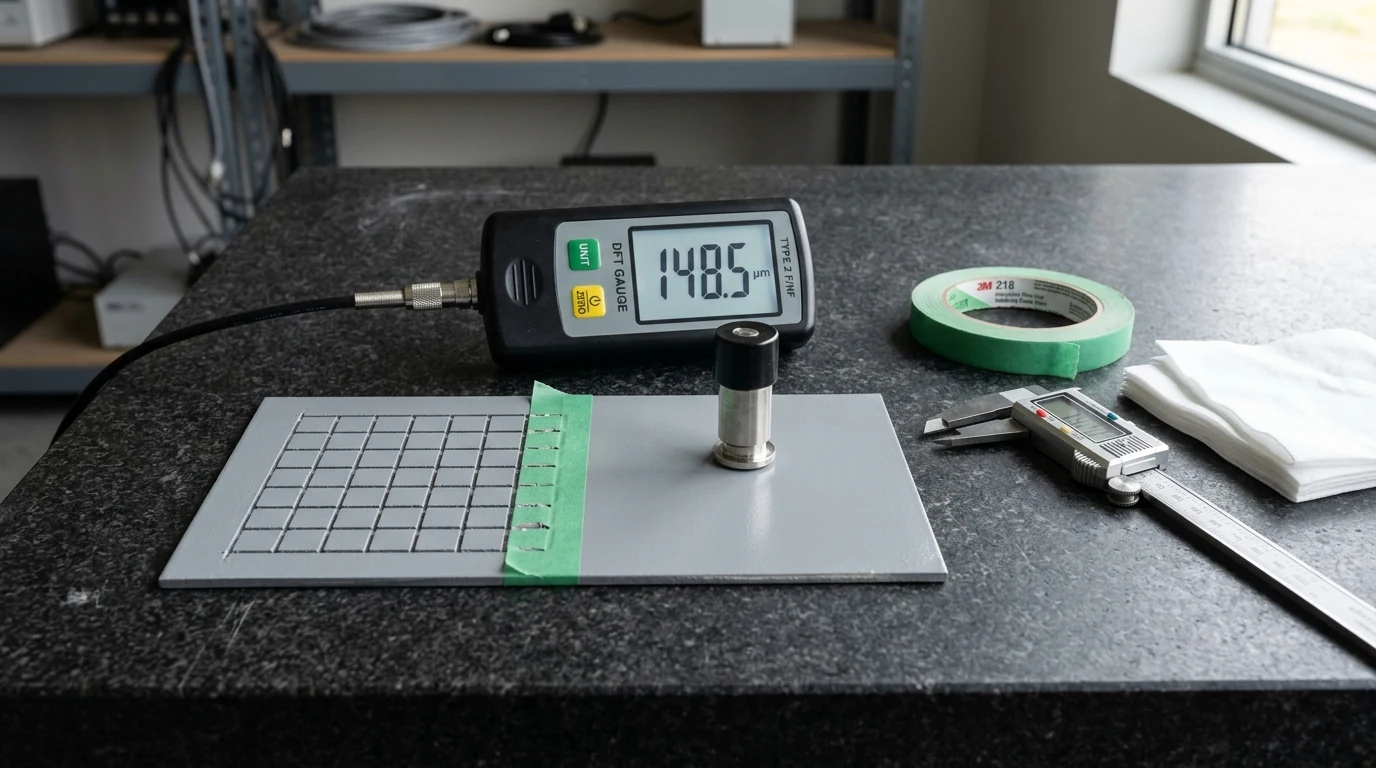
- Dry Film Thickness (DFT) Verification: Coating thicknesses are measured using non-destructive eddy-current and magnetic induction thickness gauges calibrated against NIST reference shims. Every critical feature undergoes a 5-point measurement protocol.
| Inspection Metric | Verification Method | Acceptance Criteria | Potential Failure Cause |
|---|---|---|---|
| Cross-Hatch Adhesion | ASTM D3359 Method B (Tape Test) | Class 4B / 5B (Zero flaking) | Improper surface deoxidation or oil contamination |
| Fluid Resistance | Skydrol LD-4 immersion (24h @ 23°C) | No blistering, softening, or loss of gloss | Incomplete polyurethane resin cross-linking |
| Film Hardness | Pencil Hardness (ASTM D3363) | ≥ 2H to 3H | Under-curing or off-ratio catalyst mixing |
| Electrical Conductivity | 4-Point Micro-ohmmeter probe | < 2.5 mΩ across bonding joints | Masking bleed or improper chromate conversion |
4. DFM Considerations for Aerospace Component Finishing
Effective aerospace painting starts during 3D CAD modeling. Integrating finishing DFM rules eliminates paint pooling and coating failure:
- Edge Radiusing (Breaking Sharp Corners): Surface tension causes liquid coatings to pull away from sharp 90° edges, resulting in dangerously thin paint build (edge pulling). All structural aerospace prototype edges should specify a minimum edge break of R 0.3 to 0.5 mm.
- Drainage Angles in Deep Cavities: Ensure deep milled pockets have drainage reliefs or generous internal corner radii (R ≥ 3.0 mm) to prevent paint puddling, which leads to solvent entrapment and long-term cracking.
- Hanging & Grounding Provision Points: Incorporate dedicated non-critical tooling holes or tapped locations to attach grounding wires and hanging jigs during electrostatic spraying and baking cycles.
Chemical conversion coating (Alodine / MIL-DTL-5541) forms a self-healing passivation layer that prevents aluminum oxidation. Without this pre-treatment, moisture penetrating the topcoat reacts with bare aluminum, forming galvanic blisters that cause catastrophic paint delamination.
Paint adds measurable thickness (typically 50 to 80 microns total DFT). For precision bores, dowel holes, and ground mating surfaces, our technicians install custom CNC-turned soft plugs, high-temp silicone caps, and laser-cut Kapton masks, keeping functional contact areas 100% paint-free.
Skydrol is an aggressive phosphate ester hydraulic fluid that acts as an aggressive chemical solvent against standard alkyd, acrylic, and poorly cross-linked epoxy coatings. Aerospace-grade aliphatic polyurethane topcoats (MIL-PRF-85285) provide a tightly cross-linked molecular matrix that resists hydraulic dissolution.
Coating Thickness and Adhesion Verification for Aerospace Finishes
Aerospace coating systems are verified by measured dry-film thickness and adhesion testing rather than by appearance, because primer and topcoat performance depends on thickness windows that are typically specified in tens of micrometers.
- Dry-film thickness: Measure each layer with an eddy-current or magnetic gauge following ASTM D7091 practice, taking multiple readings per surface, and record the minimum and maximum against the specified window.
- Adhesion testing: Cross-cut tape tests per ASTM D3359 and pull-off tests per ASTM D4541 quantify adhesion between primer and substrate and between primer and topcoat, and they are run on witness panels processed with the parts.
- Cure verification: A solvent double-rub test per ASTM D5402 confirms that the polyurethane or epoxy film has cured fully before parts are handled or shipped.
- Edge and corner coverage: Sharp edges tend to receive thinner film, so apply a stripe coat on edges and fastener holes and verify thickness there as well as on flat areas.
Retaining the readings with the part serial number gives design teams a coating record they can compare across builds, and it shows quickly whether a thickness or adhesion problem comes from surface preparation, spray technique or cure schedule.
Precision Aerospace Prototype Painting & Surface Finishing
Protect your aerospace flight prototypes with mil-spec surface treatments, high-adhesion primers, and durable polyurethane topcoats. Our finishing facility provides turnkey chemical conversion, precision masking, and non-destructive DFT inspection.
Upload your STEP, IGES, or 2D technical drawings for an expert finishing DFM review and instant quote:







