Drone Parts CNC Machining & Custom UAV Prototyping
AS Prototypes provides direct shop-floor precision machining, diamond PCD carbon fiber routing, and additive polymer manufacturing for advanced drone developers. From high-torque 7075-T6 motor mounts to precision optical gimbal brackets holding ±0.015 mm axis alignment, we deliver flight-ready hardware with precision-matched tolerances tailored to structural and dynamic fits.
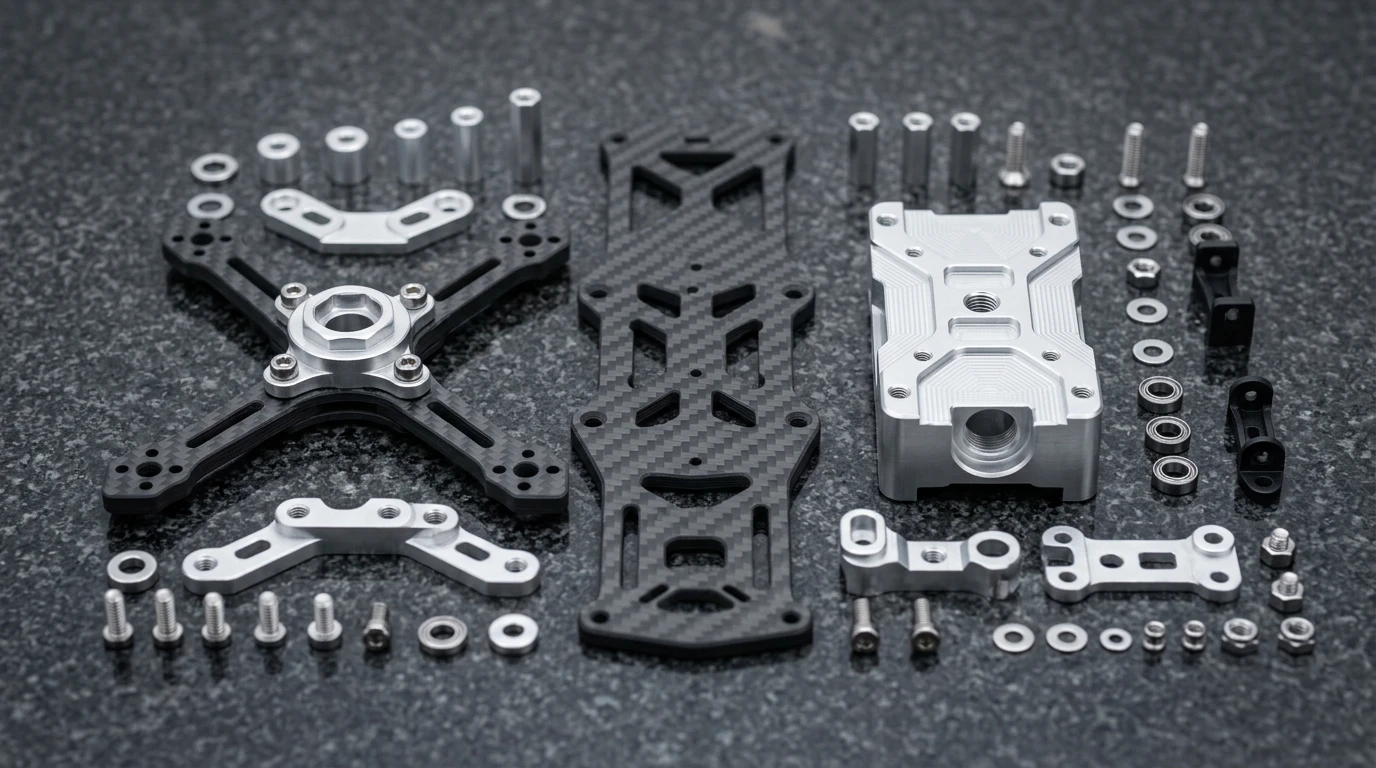
4-Stage UAV & eVTOL Hardware Prototyping Lifecycle
A disciplined, phase-gate manufacturing approach that eliminates aerodynamic deflection, prevents motor overheating, and guarantees mass repeatability.
DFM & Aerodynamic Simulation
Turnaround: 24 – 48 HoursFinite element stress clearance, thin-wall pocket evaluation, motor mount bolt circle validation, and DFM line-item costing.
- ✓ FEA deflection checks
- ✓ CAM tool clearance review
- ✓ Mass-optimization feedback
Alpha Airframe & Propulsion PoC
Turnaround: 4 – 8 Business DaysHigh-speed 3-axis CNC machining of motor mounts and PCD carbon routing for initial bench testing and vibration logging.
- ✓ 1 to 5 physical prototype units
- ✓ Zeiss CMM coordinate metrology
- ✓ Raw material test reports (MTR)
Beta Flight Hardware Freezing
Turnaround: 7 – 12 Business DaysLow-volume pre-flight test batches (10–50 units) with Type III hard anodizing, vapor-smoothed cowlings, and dynamic prop balancing.
- ✓ 10 to 50 pilot flight units
- ✓ Dynamic rotor runout verification
- ✓ Environmental heat-cycle testing
Series Production & Fleet Replication
Turnaround: 7 – 30 Business DaysScaled multi-axis manufacturing with frozen CAM programs, dedicated multi-station fixtures, and batch statistical process control.
- ✓ 50 to 1,000+ units on schedule
- ✓ Locked toolpaths & material heats
- ✓ Dedicated safety stock buffering
Precision UAV & Drone Component Showcase
Critical flight hardware matched to optimal shop-floor processes—balancing rapid iteration, flight-tested structural rigidity, and manufacturing cost-effectiveness.
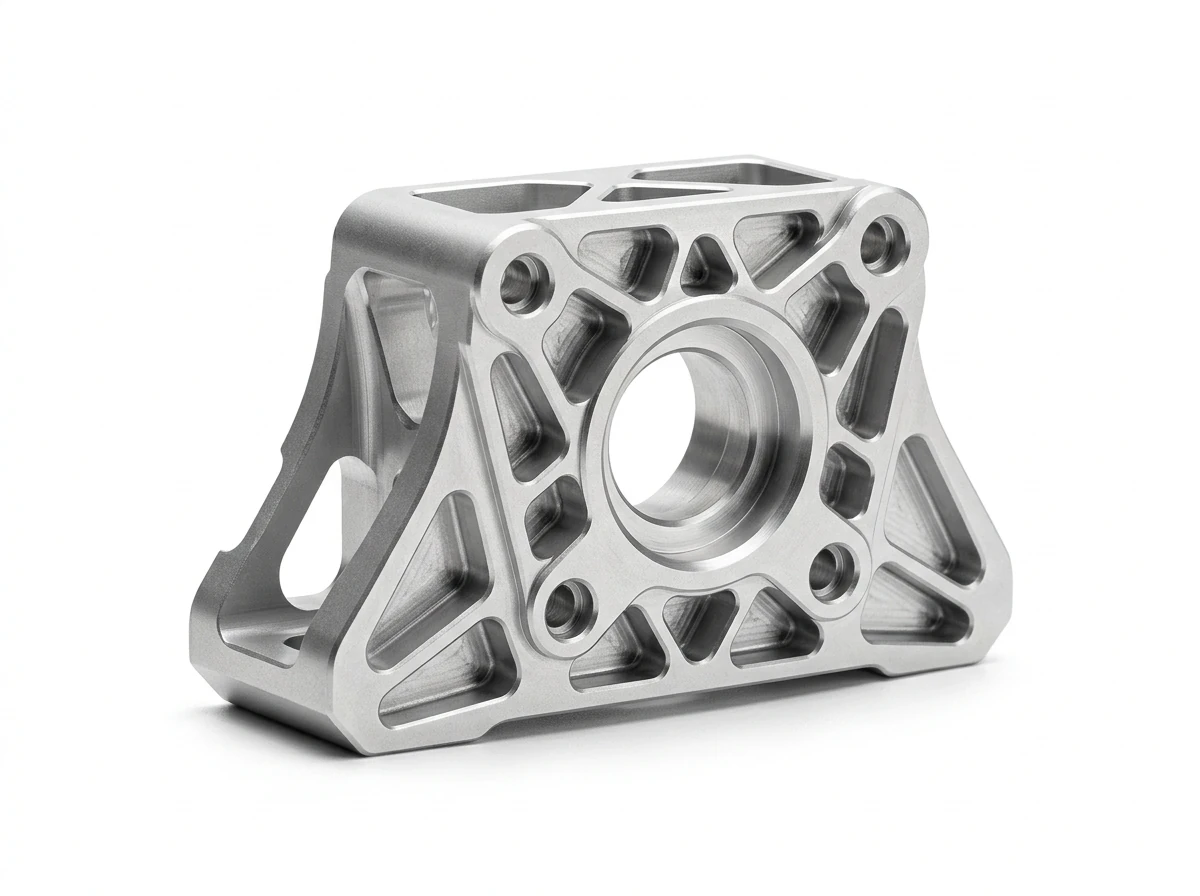
High-Torque Motor Mounts & Stators
Lightweight 7075-T6 motor brackets with 1.2mm isogrid walls. Machined on high-speed 3-axis machining centers to keep machine hourly rates economical ($25–$35/h) while mitigating thin-wall chatter and thermal deflection via balanced high-speed toolpaths.
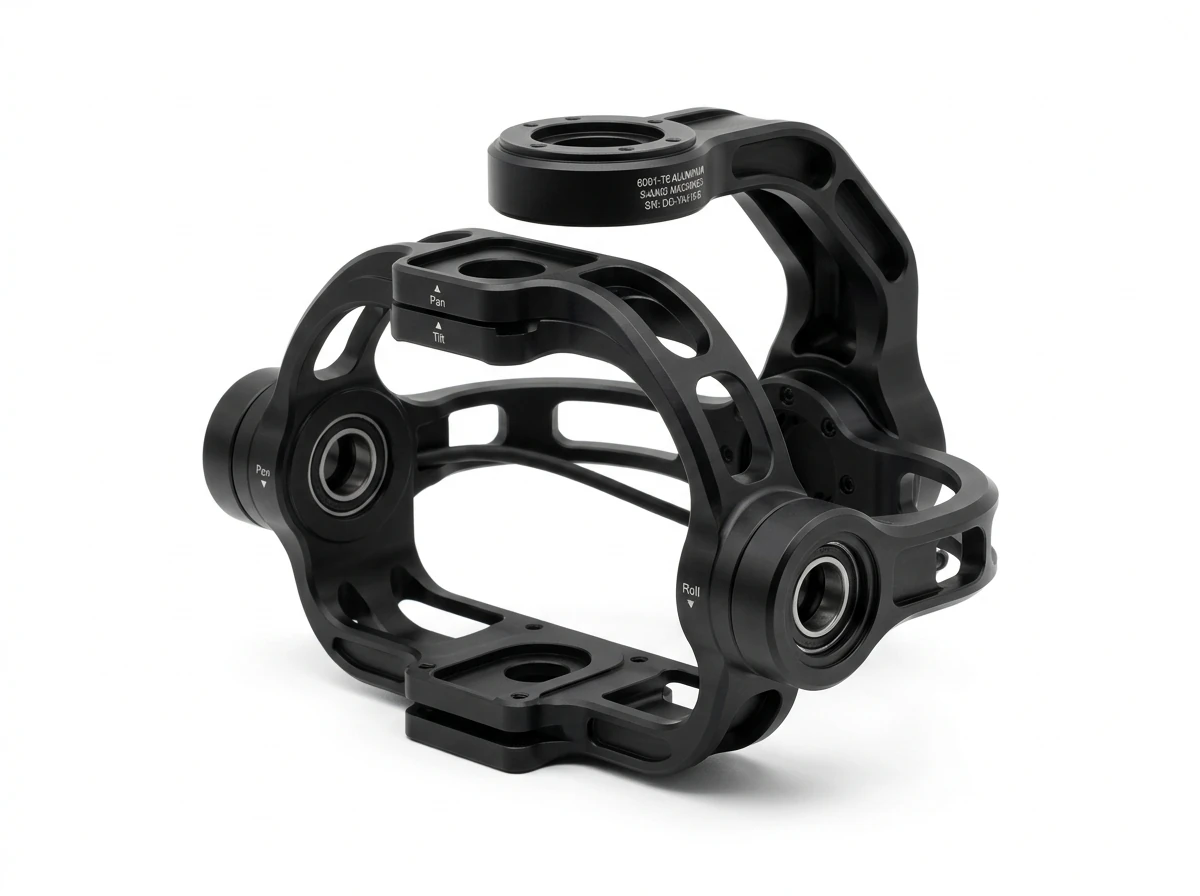
Multi-Axis Optical Gimbal Brackets
Sculpted aluminum and titanium yokes for LiDAR and thermal sensor gimbals. Simultaneous 5-axis continuous milling is deployed strictly where compound 3D undercuts require tool tilting without multi-setup error.
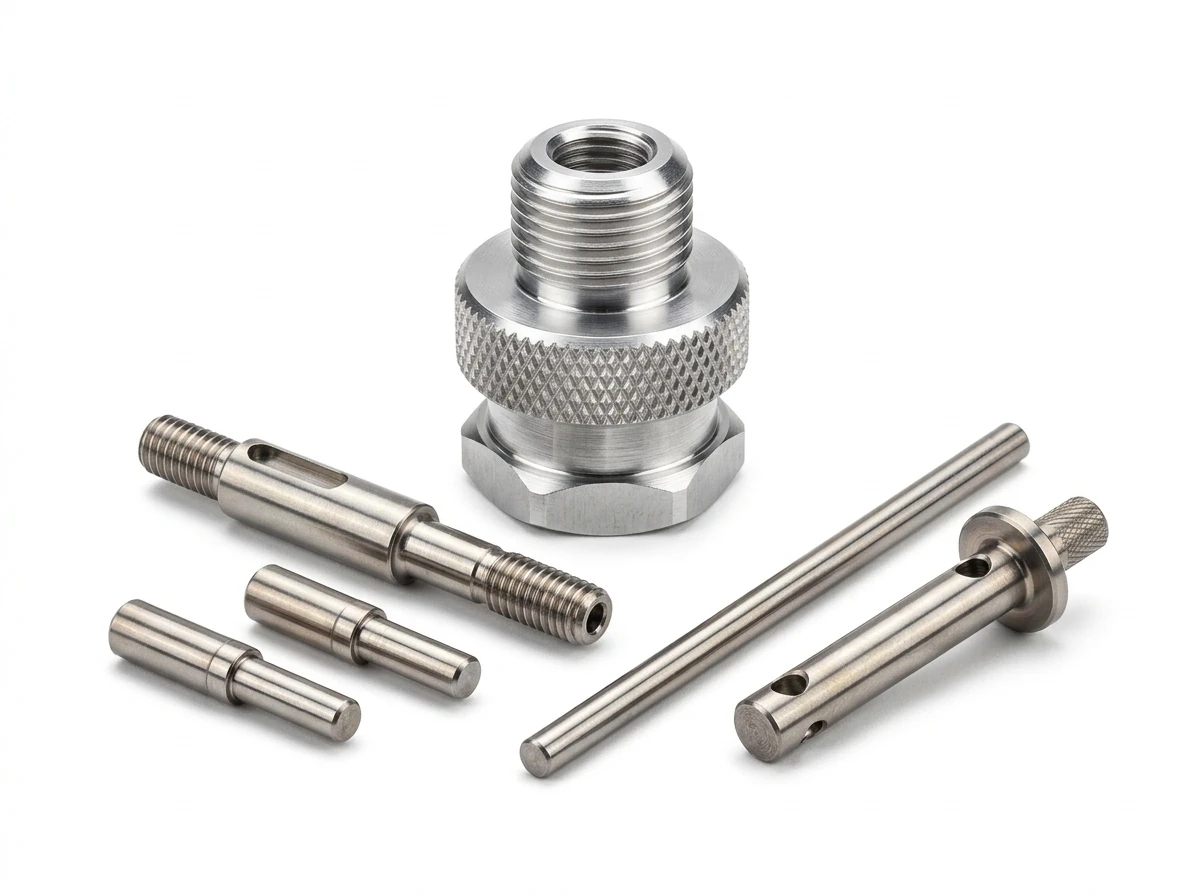
High-RPM Propeller Hubs & Motor Shafts
Precision-balanced self-tightening prop adapters, stepped titanium motor shafts, and standoffs. Automatic guide-bushing Swiss lathes turn long slender shafts in a single setup, eliminating unsupported tool deflection and maintaining cylindrical runout within 0.005 mm.
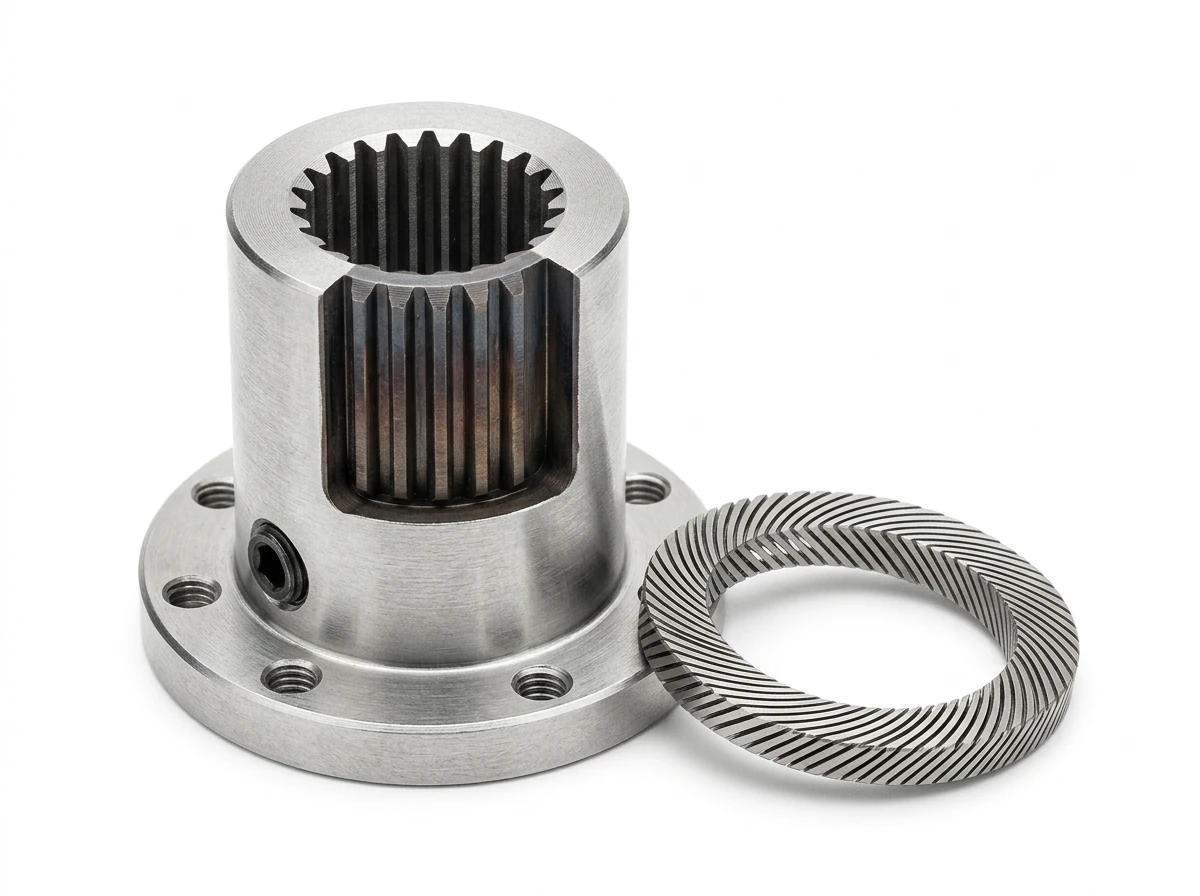
Motor Spline Couplings & Keyways
Internal involute splines, anti-rotation D-cuts, and micro-flexure slits in hardened alloys. Wire EDM electrical discharge eliminates tool radius limits, cutting internal sharp corners where standard end mills cannot reach.
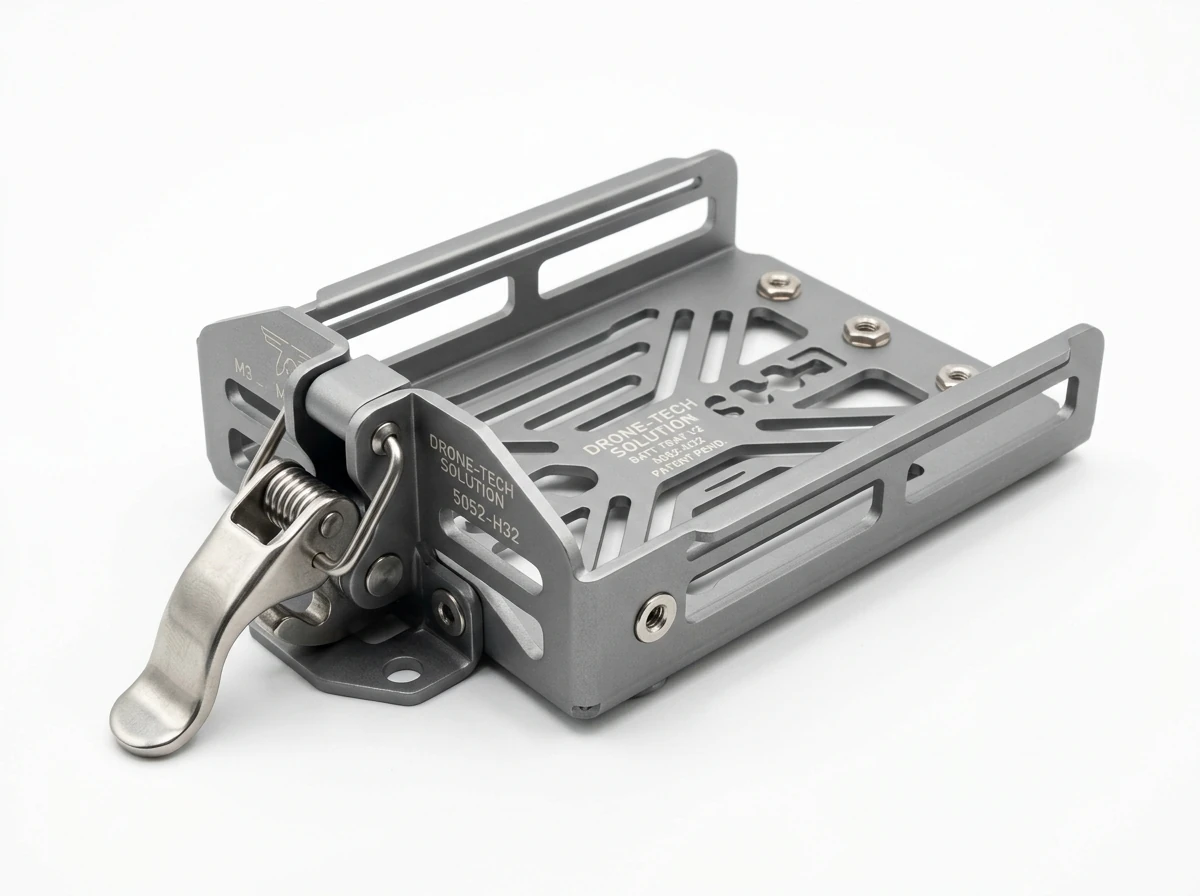
Quick-Release Battery Bays & Latches
High-strength 5052 aluminum sheet metal battery cradles, quick-release latch linkages, and avionics mounting plates. Laser cut and CNC bent at over 70% lower cost than hogging out solid billet blocks.
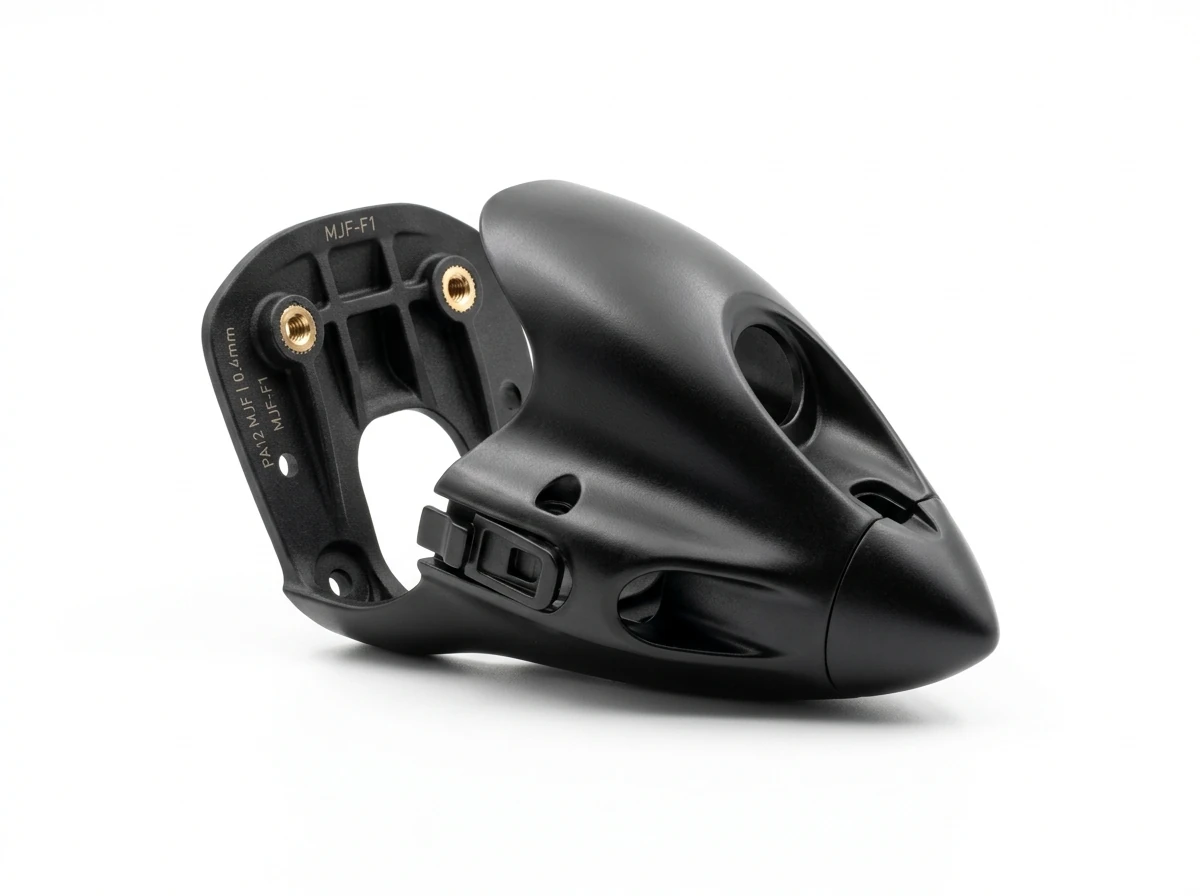
Aerodynamic HP MJF PA12 Cowlings
Thin-wall aerodynamic nose cones, motor shrouds, and sensor pods printed in durable PA12 nylon. Finished via automated chemical vapor smoothing for watertight, injection-mold quality without tooling costs.
Full-Spectrum UAV Manufacturing Process Ecosystem
Why combine three distinct manufacturing technologies under one roof? AS Prototypes unifies multi-axis metals, precision composites, and additive polymers to eliminate multi-vendor assembly stack-ups.
5-Axis Simultaneous CNC
Dedicated DMG MORI 5-axis spindles and Haas machining centers for monolithic 7075-T6 and Ti-6Al-4V airframe bulkheads, motor mounts, and sensor gimbals.
Precision H7/h6 Bores & ISO 2768-m ContoursDiamond PCD Carbon Routing
High-speed CNC routing using specialized polycrystalline diamond cutters, eliminating fiber fraying and structural delamination on 3K carbon plates.
Zero delamination on 1.5–4.0mm sheetHP MJF Nylon & Vapor Smoothing
Multi Jet Fusion additive manufacturing paired with automated chemical vapor smoothing for production-grade, airtight aerodynamic fairings.
Injection-molding level surface qualityDirect Manufacturer vs. Online Aggregator Platforms
Why drone and eVTOL hardware teams transition from online aggregator platforms (Xometry, Hubs) to our direct Shenzhen facility.
| Manufacturing Vector | Online Aggregator Platforms | AS Prototypes (In-House Direct Facility) |
|---|---|---|
| Manufacturing Model | Outsourced blind auction to disparate, unknown sub-tier job shops. | 100% In-House Spindles: Matched in-house machine fleet spanning 3-axis high-speed mills, Tsugami Swiss lathes, and DMG MORI 5-axis. |
| Multi-Material Airframe BOM | Split across 3+ subcontractors; high risk of mating tolerance mismatch. | Bundled Airframe BOM: 7075 aluminum, 3K carbon fiber, and MJF nylon fit-checked together before shipping. |
| Engineering DFM Review | Automated geometric mesh algorithms; misses thin-wall chatter and vibration modes. | Senior CAM Engineer Review: 24h evaluation of cutter deflection, resonance, and thread clearances. |
| Intellectual Property (IP) | CAD files uploaded to broad supplier networks across multiple regions. | Direct Bilateral Mutual NDA: Secure facility containment; files never leave our engineering network. |
| Surface Finish Integration | Standard commercial anodizing; often leads to seized threads on gimbal mounts. | Precision Thread Compensation: 4x build-up pre-tapping calculations for Mil-A-8625 Type III Hardcoat. |
| Commercial Pricing | 20% to 40% platform markup surcharge layered on subcontractor cost. | True Direct Factory Pricing: Zero platform markups; transparent machine-hour rates. |
UAV Material Selection & Precision Tolerances Matrix
Benchmarked mechanical properties, density factors, and achievable shop-floor tolerances across drone materials.
| Material Designation | Alloy Class / Spec | Tensile / Yield (MPa) | Density & Thermal Limits | In-House Tolerance | Key Drone Subsystem Applications |
|---|---|---|---|---|---|
| Aluminum 7075-T651 AMS 4045 Zinc Alloy | Aerospace High-Stress Billet | 570 / 503 MPa | ρ = 2.81 g/cm³, 120°C | ±0.008 mm | High-torque motor mounts, rotor arms, landing gear knuckles, propeller hubs. |
| Aluminum 6061-T6 AMS 4027 Structural Billet | High-Corrosion Resistance | 310 / 275 MPa | ρ = 2.70 g/cm³, 150°C | ±0.010 mm | Avionics enclosures, camera sensor gimbals, quick-release battery chassis. |
| Titanium Ti-6Al-4V Grade 5 / AMS 4928 | Alpha-Beta High Toughness | 950 / 880 MPa | ρ = 4.43 g/cm³, 400°C | ±0.015 mm | Precision optical gimbal yokes, high-stress rotor shafts, payload attachment hooks. |
| 3K Twill Carbon Fiber Quasi-Isotropic Composite | Autoclaved Prepreg Plate | Tensile: ≥ 600 MPa | ρ = 1.55 g/cm³, 130°C | ±0.050 mm | Main airframe center plates, boom arm tubes, sensor decks, folding arms. |
| HP MJF Nylon PA12 Vapor-Smoothed Additive | Multi Jet Fusion Thermoplastic | Tensile: 48 MPa | ρ = 1.01 g/cm³, 175°C | ±0.150 mm | Aerodynamic fairings, ESC cooling shrouds, antenna enclosures, custom wiring clips. |
Empirical Quality Verification & Flight-Critical Engineering
We eliminate speculative marketing claims with strict shop-floor physics, mathematical thread pre-compensation, and Zeiss coordinate metrology.
Zeiss CMM Coordinate Scanning
All flight-critical motor mounts and gimbal brackets undergo 3D probe scanning inside our climate-controlled lab (20.0°C ± 0.5°C) with volumetric accuracy E0 = 1.2 + L/350 μm.
- ✓ 100% ballooned FAIR reports
- ✓ True position true verification
- ✓ Opposing bearing bore coaxiality
Diamond PCD Compression Routing
To prevent interlaminar shear delamination and resin melting, our dedicated composite cell uses down-cut PCD routers and vacuum chucks under continuous fluid cooling.
- ✓ Zero ply delamination or peel
- ✓ Burr-free chamfered holes
- ✓ 40x optical microscope inspection
Mil Type III Thread Compensation
Hardcoat anodize adds ~25 μm outward surface growth (shifting 60° thread pitch by 0.100 mm). For threads under M8, we deploy precision silicone plug masking or post-anodize stainless steel wire inserts (Helicoil) to guarantee exact 6H fastener engagement.
- ✓ Guaranteed Go/No-Go gauge fit
- ✓ Matte black anti-glare blasting
- ✓ Zero thread stripping in flight
Traceable Heat-Lot Spectrometry
Every billet of 7075-T6, 6061-T6, and Ti-6Al-4V is logged with its original mill heat number. We perform incoming optical emission spectrometry to verify chemical composition.
- ✓ Traceable Mill Test Reports (MTR)
- ✓ 100% virgin alloy provenance
- ✓ High-altitude corona suppression
Frequently Asked Questions: Drone & UAV Machining
Direct answers from our manufacturing engineering team on tolerances, composite routing, lead times, and file security.
How does AS Prototypes prevent carbon fiber delamination during CNC routing?
We machine quasi-isotropic carbon fiber sheets using specialized polycrystalline diamond (PCD) compression router bits with opposing spiral flutes. The upper flute directs cutting forces downward while the lower flute pulls forces upward into the laminate core, completely neutralizing interlaminar shear stress. Combined with continuous fluid cooling and full-bed vacuum fixturing, our process delivers sharp, fray-free edges and structural composite integrity.
How do you ensure tight bearing tolerances on thin-wall aluminum motor mounts?
Motor mounts with thin isogrid walls (0.8mm to 1.2mm) are prone to cutter vibration and thermal deflection. We execute dynamic trochoidal toolpaths with high-pressure through-spindle coolant (70 bar) in a single clamping setup on our 5-axis machining centers. Bearing bores are finished with precision micro-boring heads to achieve ISO H6 tolerances (+0.008/-0.000 mm), ensuring true coaxial alignment between opposing bearing seats.
What are the calibrated production lead times for custom drone hardware?
Our lead times are strictly calibrated to physical shop-floor production: Comprehensive DFM engineering reviews are delivered within 24 hours. Rapid prototype airframes and machined motor mounts are produced in 4 to 8 business days. Parts requiring Mil-A-8625 Type III hard anodizing or chemical vapor smoothing ship in 7 to 12 business days. Scaled series production runs (50 to 1,000+ units) complete in 7 to 30 business days. International express air transit via DHL or FedEx requires an additional 3 to 5 business days.
Can AS Prototypes produce bundled multi-material drone BOMs under one roof?
Yes. Unlike online aggregator platforms that split purchase orders across separate machine shops, composite trimmers, and 3D printing vendors, AS Prototypes manufactures your complete airframe assembly in-house. We mill 7075-T6 aluminum brackets, route 3K carbon fiber plates, and 3D print vapor-smoothed HP MJF PA12 fairings in our facility, conducting physical slip-fit and bolt-circle verification before final packaging.
Ready to Prototype or Scale Your UAV Hardware?
Upload your 3D CAD models (STEP, IGES, or SolidWorks) and 2D GD&T drawings for a comprehensive DFM review within 24 hours. Directly collaborate with our senior CAM and composite tooling engineers.