DLP Red Wax 3D Printing Services: Micro Parts & Mold Masters
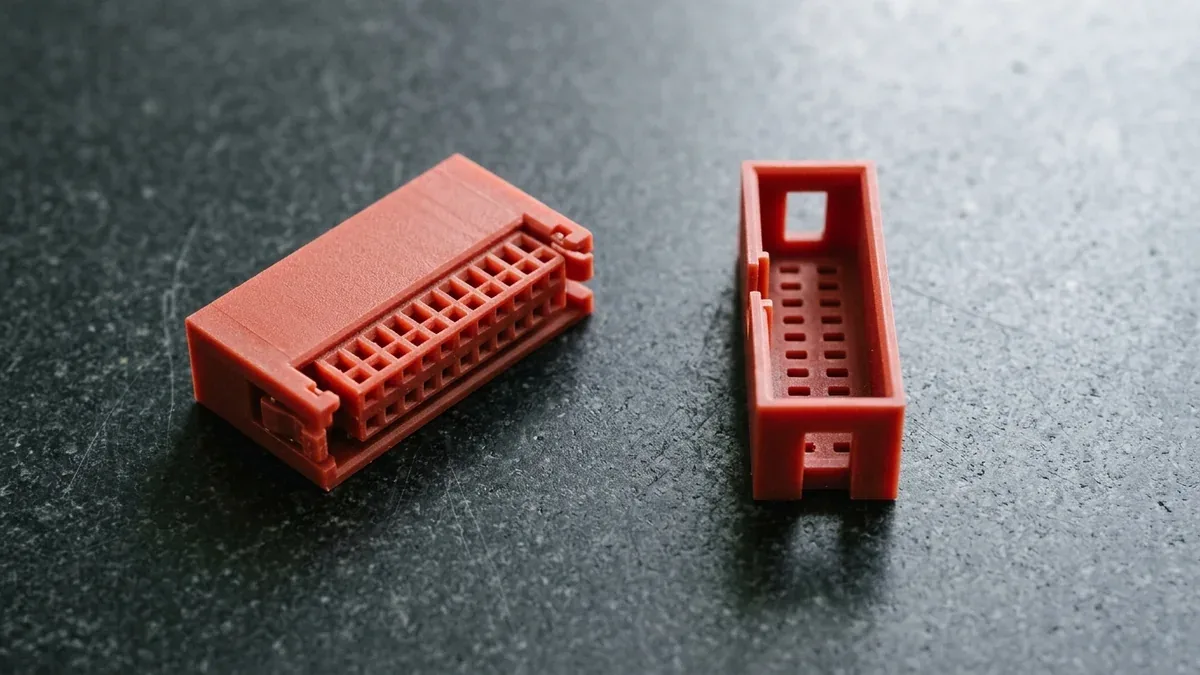
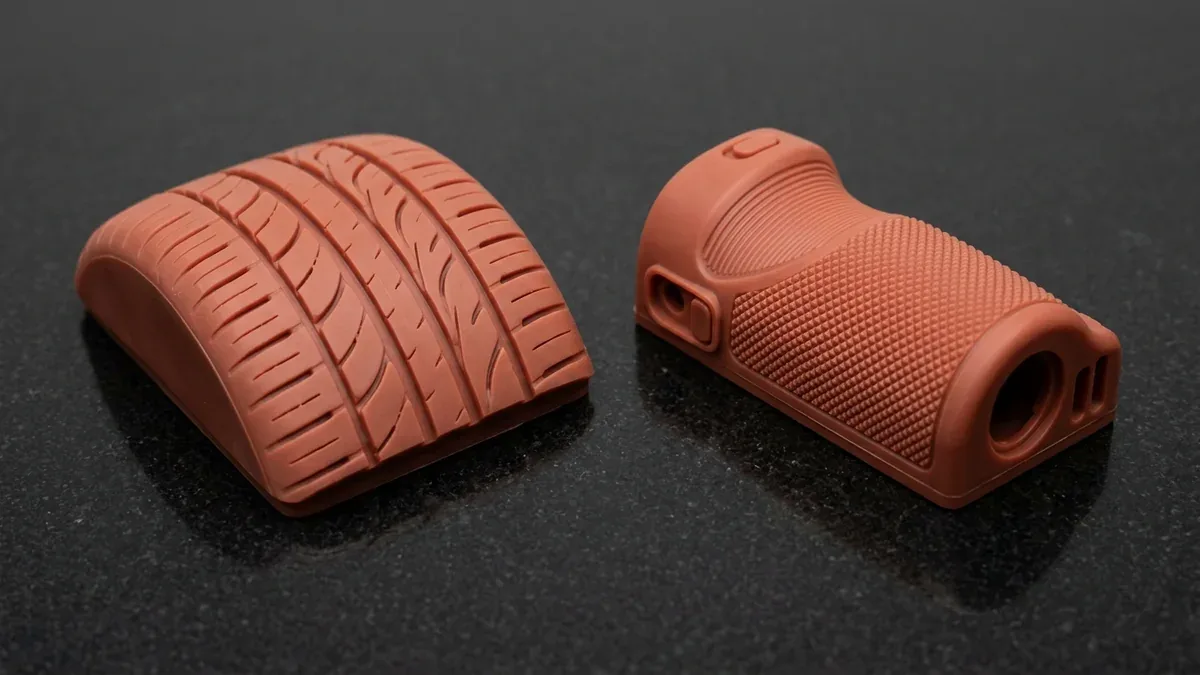
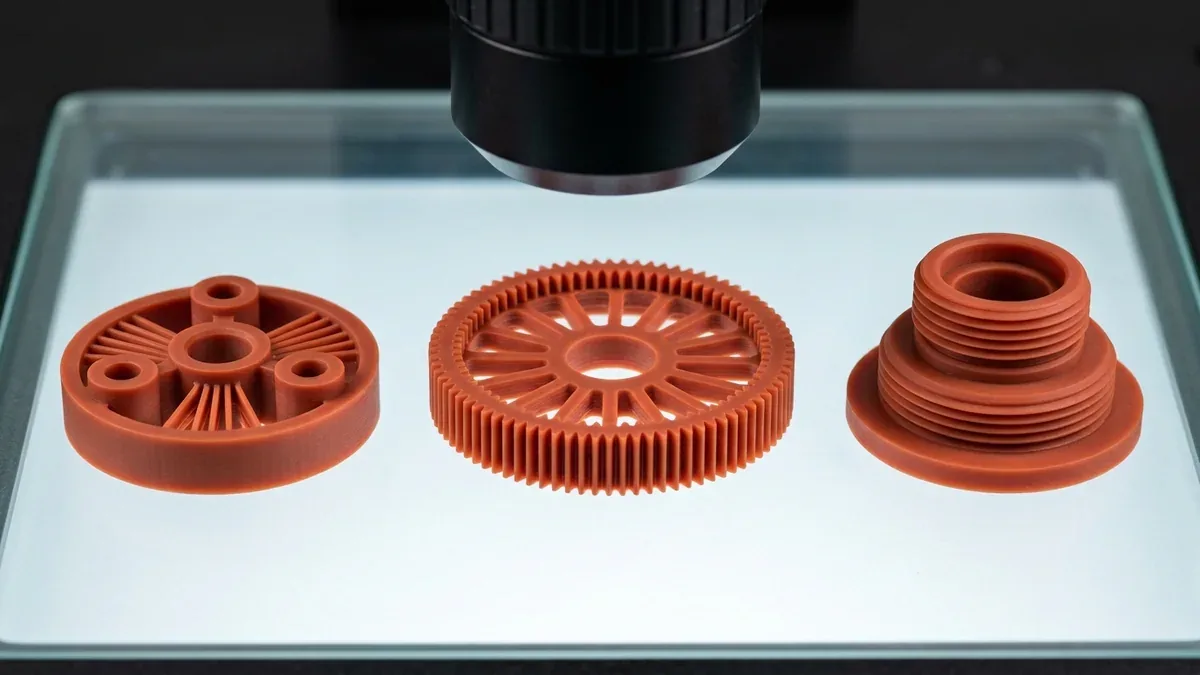
At AS Prototypes, our micro-additive workshop operates industrial Digital Light Processing (DLP) projectors running high-opacity ceramic/wax-filled terracotta-red and tan-brown photopolymers (commonly known in manufacturing as Red Wax / Brown Wax DLP, such as EnvisionTEC RCP30/R11 and tough matte red-wax resins). Because the dense terracotta pigment blocks lateral UV light bleed across each 15–25 µm (0.015–0.025 mm) layer, DLP red wax delivers razor-sharp 90° edges, zero visible stair-stepping (Ra 0.4–0.8 µm), and dimensional repeatability of ±0.02–0.05 mm (±0.0008–0.0020 in)—making it the premier choice for fine-pitch electronic connectors, RTV silicone mold master patterns, tire tread mold masters, micro-gears, and lost-wax casting patterns.
Engineering Takeaways: Why Specify DLP Red Wax Over Standard SLA?
- Zero UV Light-Bleed in Micro-Cavities: Standard white or clear SLA resins suffer from laser over-cure (“light bleed”) inside 0.3 mm connector slots and fine sipes. Opaque terracotta red wax absorbs stray 405 nm photons, preserving crisp square pinholes and razor-sharp relief textures.
- Unmatched Master Pattern for RTV Silicone Molding: High-wax red/tan DLP resins contain no unreacted sulfur compounds that inhibit platinum-cure RTV-2 silicone rubber, reproducing micro-knurling and tire-tread sipes directly into silicone molds without heavy hand-sanding.
- Micro-Part Envelope Focus: High-resolution DLP projectors focus millions of DMD pixels onto a compact build window (typically 90 × 50 × 100 mm to 192 × 108 × 200 mm). Parts larger than 150 mm should transition to industrial SLA 3D printing.
How DLP Red Wax 3D Printing Works: High-Opacity Micro-Projection
Unlike galvanometer laser SLA that traces vectors point by point, Digital Light Processing projects an entire cross-sectional slice simultaneously onto a vat of pigmented wax-filled photopolymer:
- 1. Digital Micro-Mirror (DMD) Optical Projection: An industrial 4K/1080p DMD chip modulates a 385 nm or 405 nm UV LED source through a telecentric lens, locking XY pixel pitch to 22–35 µm (0.0009–0.0014 in) across the entire build platform.
- 2. High-Opacity Terracotta & Tan Wax Pigmentation: Fine ceramic/wax fillers give the resin its signature velvety matte salmon-terracotta or sandstone-tan appearance, restricting UV cure depth strictly to each 15–25 µm layer and preventing roof sag over micro-channels.
- 3. Grayscale Sub-Pixel Anti-Aliasing: Boundary voxel light modulation smooths curved walls and helical gear flanks, eliminating pixel staircase artifacts and producing an injection-mold-like matte surface straight from the ultrasonic bath.
DLP Red Wax vs. Standard SLA vs. Swiss Micro-CNC Machining
Use this engineering comparison matrix to select the optimal process for miniature components, textured mold masters, and fine-pitch housings:
| Engineering Parameter | Micro-Nano DLP (Red / Tan Wax) | Standard Industrial SLA Resin | Swiss Precision CNC Turning |
|---|---|---|---|
| Layer Thickness (Z-Axis) | 15 – 25 µm (0.0006 – 0.0010 in) | 50 – 100 µm (0.0020 – 0.0040 in) | Continuous subtractive toolpath |
| Typical Dimensional Tolerance | ±0.02 – ±0.05 mm (±0.0008 – ±0.0020 in) | ±0.10 – ±0.20 mm per 100 mm | ISO 2768-mK (Key fits ±0.010 – ±0.020 mm) |
| As-Built Surface Roughness | Ra 0.4 – 0.8 µm (16 – 32 µin, matte) | Ra 0.8 – 1.6 µm (32 – 63 µin) | Ra 0.4 – 1.6 µm (16 – 63 µin) |
| Min. Wall / Partition Thickness | 0.20 – 0.30 mm (0.008 – 0.012 in) | 0.60 – 0.80 mm (0.024 – 0.031 in) | 0.30 – 0.50 mm (metal deflection limit) |
| Internal Corner Geometry | True 90° square micro-corners | Slight laser spot radius (R ≥ 0.08 mm) | Limited by end-mill radius (R ≥ 0.15 mm) |
| Primary Industrial Role | Fine-pitch connectors, RTV silicone mold masters, tire tread masters, micro-gears | Medium-to-large enclosures, clear optical housings, general form prototypes | Load-bearing metal shafts, surgical pins, high-pressure fluid valves |
DLP Red Wax & Brown Wax Material Grades & Datasheet Properties
We stock four specialized DLP red-wax and brown-wax photopolymer formulations matched to functional prototyping, RTV silicone molding, or lost-wax burnout:
| Material Grade & Color | Tensile Strength | Flexural Modulus | Elongation | HDT @ 0.45 MPa | Best Engineering Application |
|---|---|---|---|---|---|
| Imported Ceramic-Filled Red Wax (RCP30 / R11 Equivalent, Warm Terracotta) | 52 – 60 MPa (7.5 – 8.7 ksi) | 2,800 – 3,300 MPa | 3 – 5% | 65 – 75 °C (149 – 167 °F) | Master patterns for RTV silicone molding, tire tread blocks, fine-pitch connector housings, micro-gears |
| Tough Matte Red Wax (MD1500 ABS-Like Terracotta Resin) | 45 – 52 MPa (6.5 – 7.5 ksi) | 2,100 – 2,450 MPa | 10 – 15% | 62 °C (144 °F) | Snap-fit electronic housings, thin-wall terminal blocks, painted cosmetic display models, ergonomic grip prototypes |
| High-Detail Tan / Brown Wax (Sandstone-Clay Master Resin) | 55 – 64 MPa (8.0 – 9.3 ksi) | 2,900 – 3,400 MPa | 3 – 6% | 72 °C (162 °F) | Shoe-sole and automotive tire tread master molds, micro-relief industrial textures, high-contrast 3D optical scanning masters |
| Direct Castable Red / Purple Wax (High-Wax Investment Grade) | 22 – 30 MPa (3.2 – 4.4 ksi) | 900 – 1,300 MPa | 4 – 7% | 52 °C (126 °F) | Direct lost-wax investment casting in brass, bronze, silver, and stainless steel (< 0.01% ash residue) |
8-Point DFM Engineering Rules for DLP Red Wax Parts
Follow these 8 quantitative design rules when preparing CAD files for bottom-up micro-DLP red wax printing:
| Geometry Feature | Recommended Design Limit | Extreme Minimum Limit | Shop-Floor Engineering Guidance |
|---|---|---|---|
| 1. Supported Structural Walls | ≥ 0.35 mm (0.014 in) | 0.20 mm (0.008 in) | Connector partition walls connected on 3 sides print cleanly at 0.25 mm without warping during FEP film peel. |
| 2. Unsupported Cantilever Walls | ≥ 0.60 mm (0.024 in) | 0.40 mm (0.016 in) | Add 0.15 mm base fillets to freestanding fins or impeller blades to resist hydrodynamic resin peel forces. |
| 3. Micro Pinholes & Square Sockets | ≥ Ø0.35 mm (0.014 in) | Ø0.20 mm (0.008 in) | Through-holes flush easily during ultrasonic IPA/TPM washing; blind holes deeper than 3×D require side vent slots. |
| 4. Embossed Text & Surface Sipes | 0.15 mm width × 0.15 mm depth | 0.08 mm (0.003 in) | Opaque terracotta pigment gives exceptional shadow contrast on 0.15 mm recessed tire sipes and diamond knurling. |
| 5. Moving Assembly Clearance | 0.15 – 0.20 mm (0.006 – 0.008 in) | 0.10 mm (0.004 in) | Required radial air gap for pre-assembled micro-gears or sliding latches to prevent residual monomer bridging. |
| 6. Directly Printed Micro-Threads | M1.6 and larger (ISO metric) | M1.2 fine pitch | Apply 0.03–0.05 mm radial thread flank offset in CAD so printed male/female micro-threads assemble smoothly. |
| 7. Hollow Cavity Escape Ports | ≥ 2 holes × Ø1.5 mm (0.059 in) | Ø1.0 mm (0.039 in) | Closed hollow chambers act as suction cups against the FEP vat film; place vent holes at the lowest Z-elevation. |
| 8. Maximum Single-Piece Envelope | ≤ 120 × 70 × 100 mm | 190 × 108 × 200 mm | Keep parts compact to preserve 22–35 µm XY pixel resolution; larger housings should be routed to SLA. |
4-Level Post-Processing & Surface Finishing Tiers for Red Wax Parts
Specify the required surface finish tier on your RFQ based on whether the red wax print is a functional connector, a silicone molding master, or a painted display model:
| Finish Tier | Post-Processing Operations | Surface Roughness | Ex-Factory Lead Time | Recommended Use Case |
|---|---|---|---|---|
| Level 1: Standard Micro-Cleaned | Dual-stage ultrasonic IPA/TPM wash, micro-tip support removal, 405 nm + 60 °C thermal UV cure | Ra 0.4 – 0.8 µm (natural matte red/tan wax) | 4 – 6 Business Days | Board-to-board connectors, micro-gears, internal mechanisms, dimensional fit checks |
| Level 2: Silicone Master Grade | Level 1 + microscopic support-Witness blending under 20× stereo microscope, anti-inhibition UV bake | Ra 0.4 µm (zero support nibs on parting surfaces) | 5 – 8 Business Days | Master patterns for RTV-2 silicone vacuum casting & tire tread mold blocks |
| Level 3: Cosmetic Painted / Plated | Fine primer coat, custom Pantone / RAL spray painting, silk-screen legends, or vacuum metallization | Smooth matte, satin, or high-gloss coat | 7 – 12 Business Days | Exhibition appearance models, wearable electronics bezels, sculpted promotional masters |
| Level 4: Direct Castable Wax Pattern | Solvent mist cleaning, uncured monomer purge, zero-ash burnout conditioning (no primer/paint) | Ra 0.4 – 0.8 µm raw castable wax | 4 – 8 Business Days | Lost-wax investment casting into brass, bronze, sterling silver, or 316L stainless steel |
Core Industrial Applications of DLP Red Wax 3D Printing
Automotive tire tread segment masters, shoe-sole micro-textures, and knurled housing masters for platinum-cure polyurethane vacuum casting with zero silicone cure inhibition.
Board-to-board receptacle housings, IC burn-in test sockets, and micro-switch bobbins with 0.25 mm partition walls and crisp snap-fit locking tabs. Explore our electronics capabilities.
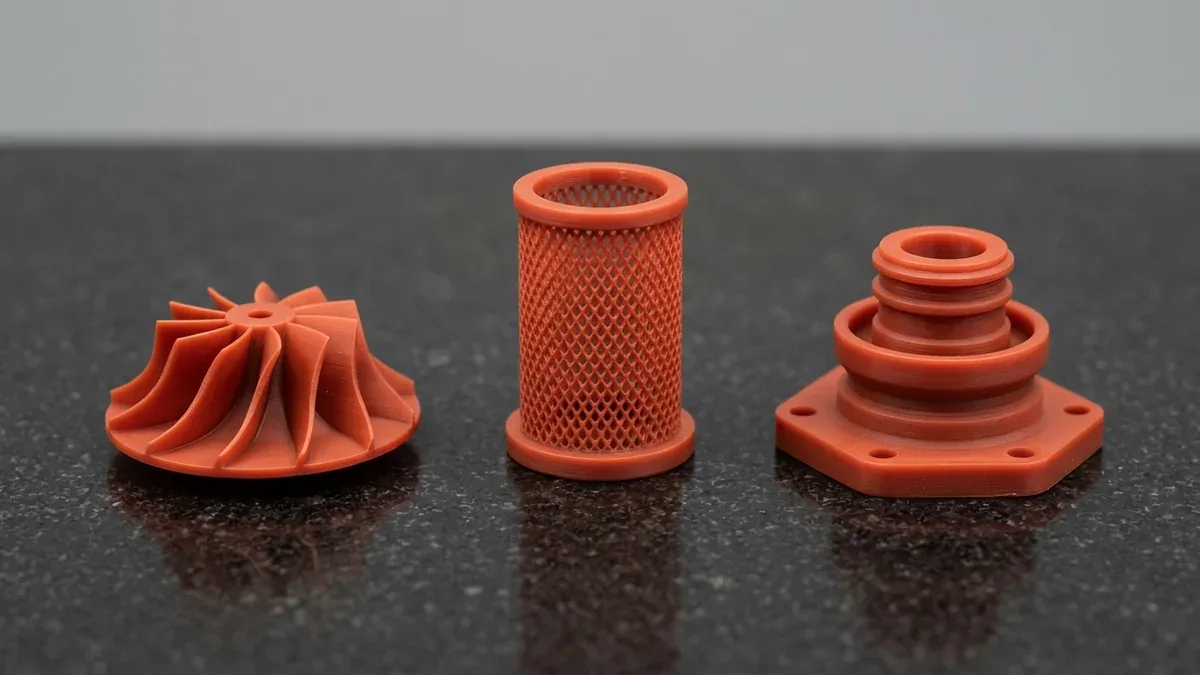
Miniature helical and planetary gears, 12-blade micro-impellers, diamond-mesh filter cages, and M1.2–M3.0 threaded optical barrels verified by non-contact optical vision metrology.
High-relief figurines, watchmaking bezels, filigree jewelry wax patterns, and intricate anatomical/industrial miniatures where 15–25 µm layers eliminate manual polishing.
Frequently Asked Questions: DLP Red Wax 3D Printing
Q1: Why is high-detail DLP resin opaque terracotta-red or tan-brown (“Red Wax”)?
Q2: Why do silicone mold makers prefer DLP Red Wax master patterns over standard SLA?
Q3: How do you inspect miniature DLP Red Wax parts without deforming thin 0.25 mm walls?
Q4: What is the ex-factory turnaround time for DLP Red Wax prototypes?
Ready to Build Micro-Precision Parts or Silicone Mold Masters in DLP Red Wax?
Upload your 3D CAD files (STEP, IGES, or high-mesh STL) for an engineer-led DFM check and custom quotation within 24 hours.