
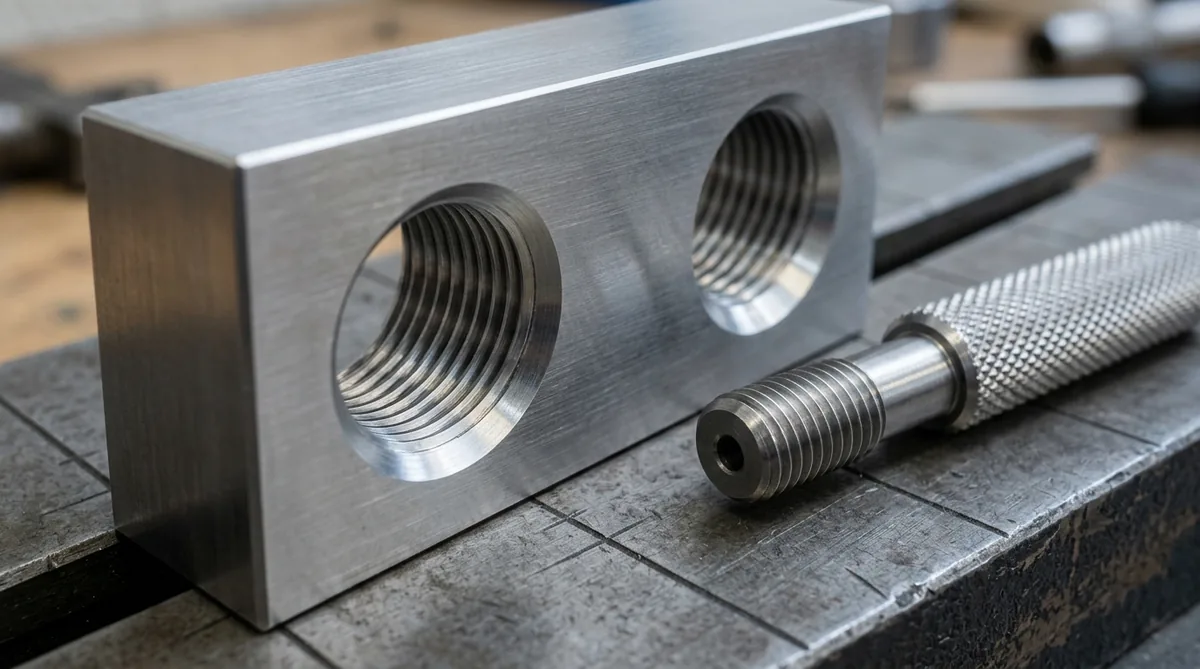
Fasteners join almost every mechanical assembly in the world today. Therefore, designing precise threaded holes is a vital skill for product engineers.
Threaded holes allow bolts and machine screws to mate with metal parts. They hold critical structural brackets, motor plates, and electronic cases tightly together.
However, tapping mistakes can easily ruin costly CNC machined parts. Broken taps, stripped lead threads, and shallow holes cause expensive scrap and shop delays.
At AS Prototypes, our machinists tap thousands of precision threads every month. In this practical guide, we explain the main types of threaded holes and key design rules for CNC machining.
Through Holes vs Blind Holes
Every threaded hole falls into one of two physical categories. Choosing the right style directly affects part strength and machining cost.
1. Through Holes
A through hole passes completely through the workpiece from one side to the other. It is the easiest type of threaded hole to machine.
First, chips pass freely out the bottom of the part. This clear chip path prevents binding and avoids broken taps.
Second, standard taps can pass all the way through the part. As a result, through holes guarantee full thread engagement across the entire thickness.
2. Blind Holes
A blind hole ends inside the workpiece without breaking through the opposite face. It is necessary when you need a smooth, sealed exterior wall.
However, blind holes present two distinct manufacturing hurdles. Chips cannot fall out the bottom, so they must exit upward through the flutes.
Furthermore, standard taps have tapered lead chamfers that do not cut full threads. Therefore, engineers must add extra pilot drill depth below the active thread zone.
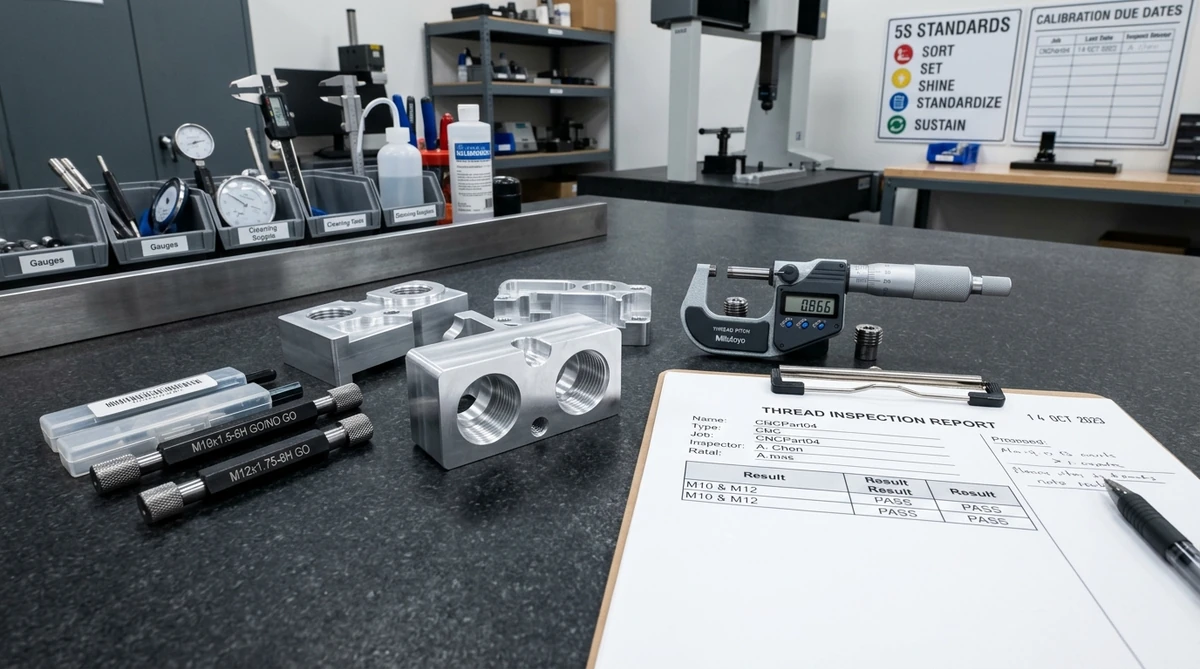
Core Methods for Machining Threaded Holes
Modern CNC machine shops use three distinct techniques to create internal screw threads. Each method offers unique technical perks.
1. Cut Tapping
Cut tapping uses a fluted tool with cutting teeth to carve metal away. As the tap turns, it slices helical chips out of the pre-drilled hole.
For through holes, machinists pick spiral point taps that push chips forward. For blind holes, they use spiral flute taps that pull chips upward like drill bits.
2. Roll Form Tapping
Form tapping does not cut chips at all. Instead, it cold-forms and displaces ductile metal under high radial pressure.
Consequently, form tapping creates zero chips inside the hole. This completely eliminates chip packing issues in deep blind holes.
In addition, cold-working smooths the grain structure of the metal. As a result, formed threads are up to 20 percent stronger than cut threads in aluminum.
3. CNC Thread Milling
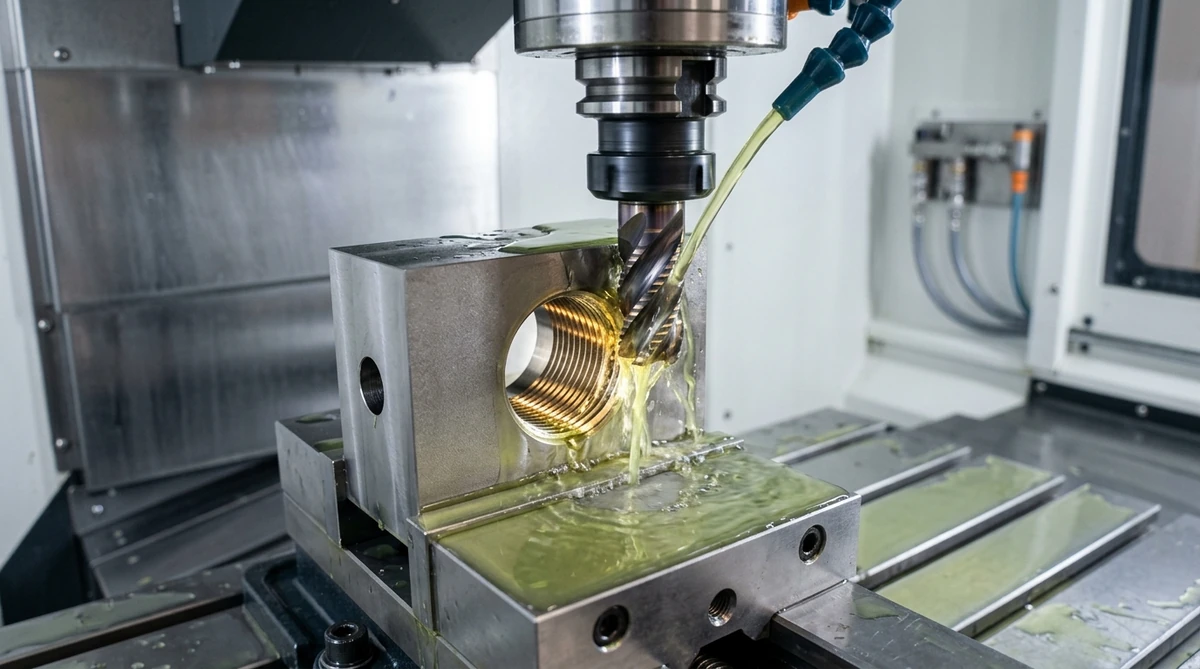
Thread milling uses a rotating carbide cutter driven in a helical interpolation path. It moves in a spiral circle while slowly rising out of the hole.
First, thread milling cuts full threads almost to the very bottom of a blind hole. Second, one single thread mill cutter can produce multiple hole diameters.
Finally, if a thread mill breaks, it does not jam in the hole. Machinists can easily remove the broken tool without scrapping the part. Our high-precision CNC milling centers use thread milling for costly titanium and aerospace parts.
Metric Thread Dimensions and Tap Drill Sizes
Selecting the correct pilot drill diameter is critical. A pilot hole that is too small snaps the tap. A hole that is too big strips the threads.
| Thread Size | Standard Pitch (mm) | Cut Tap Drill (mm) | Form Tap Drill (mm) | Min Engagement Depth |
|---|---|---|---|---|
| M3 | 0.50 mm | 2.50 mm | 2.80 mm | 4.5 mm (1.5x D) |
| M4 | 0.70 mm | 3.30 mm | 3.70 mm | 6.0 mm (1.5x D) |
| M5 | 0.80 mm | 4.20 mm | 4.65 mm | 7.5 mm (1.5x D) |
| M6 | 1.00 mm | 5.00 mm | 5.55 mm | 9.0 mm (1.5x D) |
| M8 | 1.25 mm | 6.80 mm | 7.40 mm | 12.0 mm (1.5x D) |
| M10 | 1.50 mm | 8.50 mm | 9.30 mm | 15.0 mm (1.5x D) |
Comparison of Thread Production Methods
Review the table below to select the optimal threading method for your custom parts.
| Threading Method | Chip Generation | Thread Strength | Blind Hole Capability | Best Use Case |
|---|---|---|---|---|
| Cut Tapping | Produces loose chips | Standard baseline | Needs extra drill depth | High-speed tapping in through holes and steels. |
| Form Tapping | Zero chips formed | Up to 20% stronger | Great for deep blind holes | Ductile aluminum, brass, and mild steels. |
| Thread Milling | Small, easily flushed chips | High precision finish | Cuts threads to very bottom | Hard metals, large diameters, and expensive parts. |
Essential Engineering Rules for Threaded Holes
Apply these four golden design rules to make your threaded parts stronger and cheaper to machine.
- Use 1.5x Diameter for Thread Engagement: In aluminum alloys, engaging threads 1.5 times the bolt diameter provides maximum pull-out strength.
- Always Add an Entry Chamfer: Include a 45-degree chamfer at the hole mouth. It guides bolts smoothly and stops burrs from rising.
- Provide Extra Drill Depth in Blind Holes: Always drill pilot holes at least 3 to 5 pitches deeper than the needed thread length.
- Use Helicoil Inserts for Soft Metals: For parts that face frequent disassembly, specify stainless steel Helicoil inserts to stop thread wear.
- Compensate for Plating Buildup (6GX/6HX Oversized Taps): Surface coatings like Type III hard anodizing or electroless nickel deposit on 60° thread flanks, shrinking the effective pitch diameter by 4× the single-side coating thickness (ΔD₂ = 4t). Always specify oversized taps (6GX/6HX) or CAM thread-milling pitch offsets prior to plating.
For aluminum and soft metals, design thread engagement between 1.5 and 2.0 times the bolt diameter. For steel and hard alloys, 1.0 to 1.5 times the diameter is sufficient.
Standard taps have lead chamfers that cannot cut full threads at the tip. Furthermore, extra drill depth leaves space for loose chips to pack without breaking the tap.
Roll forming is NOT recommended for austenitic stainless steels like 304 and 316. Severe work hardening rapidly spikes tapping torque, causing crest splitting and catastrophic tap seizure. CNC thread milling or spiral-flute cut tapping with high-pressure sulfurized fluid is the reliable shop standard.
Need Precision CNC Parts with Threaded Holes?
AS Prototypes machines tight-tolerance threaded holes across aluminum, titanium, stainless steel, and engineering plastics. Upload your 3D CAD files today for a fast DFM review and instant quote.
Request a CNC Machining Quote