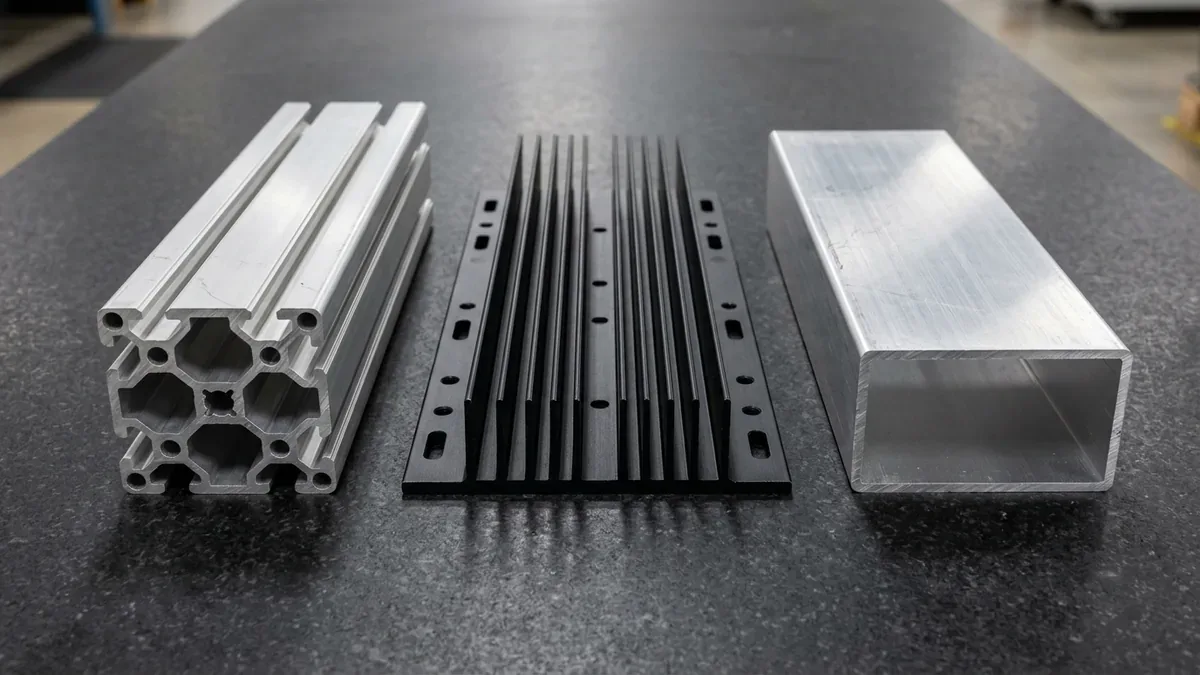
Understanding the aluminum extrusion process empowers engineers to design high-strength, lightweight structural frames and thermal enclosures efficiently. Consequently, industrial manufacturers utilize hot extrusion to produce complex cross-sections cost-effectively.
By forcing heated aluminum alloy billets through custom steel dies, fabricators create continuous profiles with exceptional surface finishes. Furthermore, combining extrusion with precision CNC machining delivers ready-to-assemble structural modules.
Selecting the optimal alloy and temper guarantees mechanical integrity across diverse applications. In addition, applying protective surface finishes enhances corrosion resistance and aesthetic appeal.
1. Direct Extrusion vs Indirect Extrusion
Extrusion facilities employ two distinct mechanical configurations to shape heated aluminum billets. Specifically, tooling engineers evaluate direct and indirect extrusion based on friction and profile complexity.
| Process Parameter | Direct (Forward) Extrusion | Indirect (Backward) Extrusion |
|---|---|---|
| Billet Movement | Billet moves relative to container walls | Billet remains stationary relative to container |
| Frictional Resistance | High friction along full container bore | Zero friction between billet and container walls |
| Ram Tonnage Requirement | 25% to 30% higher ram force needed | Significantly lower extrusion pressure needed |
| Grain Structure Uniformity | Moderate peripheral grain coarsening | Exceptional metallurgical grain uniformity |
| Geometric Profile Capability | Superior for complex multi-void hollows | Limited cross-sectional width by hollow ram |
2. The 10-Step Aluminum Extrusion Manufacturing Sequence
Transforming raw cylindrical logs into precision engineering profiles requires rigorous thermal and mechanical control. Specifically, ten consecutive steps govern modern extrusion production lines.
1. Extrusion Tool Steel Die Preparation
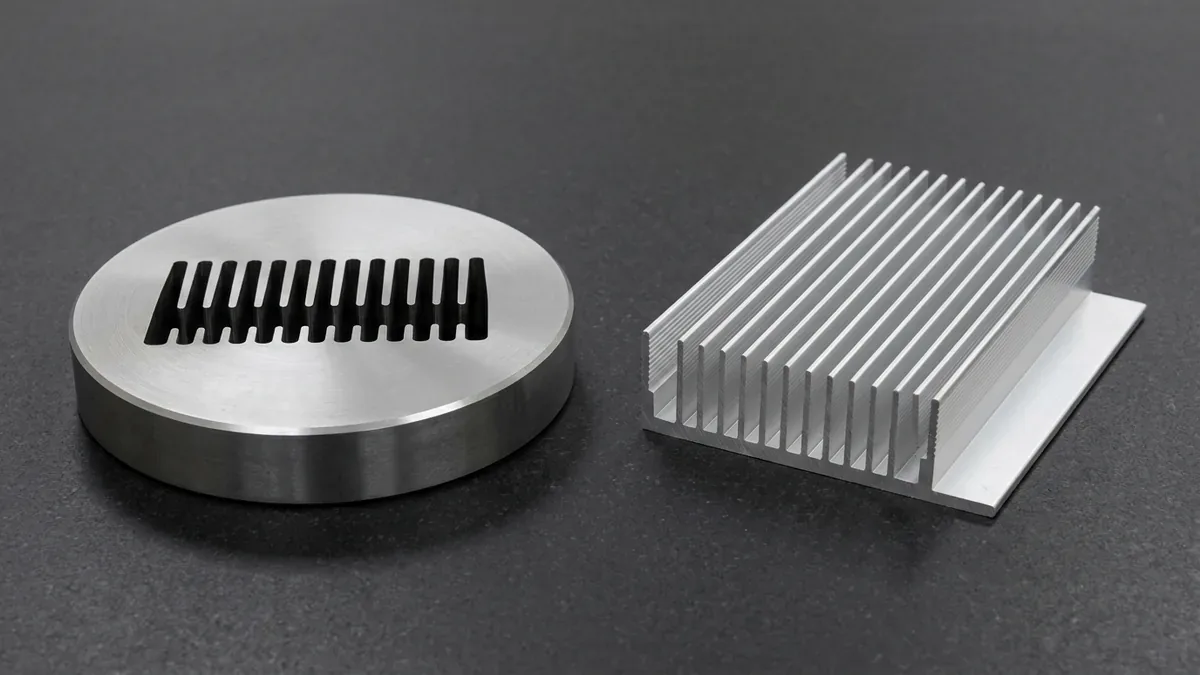
Machinists precision-machine circular extrusion dies from premium H13 tool steel. Furthermore, slow-feeding wire EDM carves complex internal aperture geometries with ±0.005 mm precision.
Before loading into the press, technicians preheat the die to 450 degrees Celsius. Consequently, preheating prevents thermal shock and ensures smooth metal flow.
2. Billet Log Induction Heating
First, technicians cut cylindrical billets from cast aluminum alloy logs. Next, electromagnetic induction furnaces heat the billets to 420 to 480 degrees Celsius.
This temperature softens the alloy into a malleable solid state. Crucially, the metal remains solid without entering a molten liquid phase.
3. Hydraulic Ram Pressure Application
A mechanical loader transfers the heated billet into the heavy extrusion press container. Then, an automated lubricator coats the dummy block to prevent adhesion.
The primary hydraulic ram exerts up to 15,000 tons of force. Consequently, the ductile alloy expands, filling the container walls completely.
4. Profile Emergence & Controlled Quenching
Continuous pressure forces the plasticized aluminum through the die orifices. As the custom profile emerges, mechanical pullers guide the leading end along runout tables.
Simultaneously, high-velocity air blowers or water spray curtains quench the hot extrusion rapidly. Therefore, rapid quenching freezes alloying elements in solid metallurgical solution.
5. Precision Tension Stretching & Straightening
As long extrusions cool, uneven thermal contraction induces natural longitudinal twists. Consequently, technicians transfer the cooled segments to mechanical stretching beds.
Hydraulic gripper jaws grasp opposing profile ends and pull under calibrated tension. Specifically, a 1% to 2% stretch straightens the profile and relieves residual stresses.
6. Precision Sawing & Artificial Aging (T5 / T6)
High-speed carbide circular saws cut stretched extrusions into standard handling lengths. Next, the batches enter large aging ovens heated to 180 degrees Celsius for several hours.
This artificial precipitation heat treatment hardens the metal to T5 or T6 tempers. Hence, the profiles achieve maximum tensile and yield strength.
3. Secondary CNC Machining and Surface Enhancement
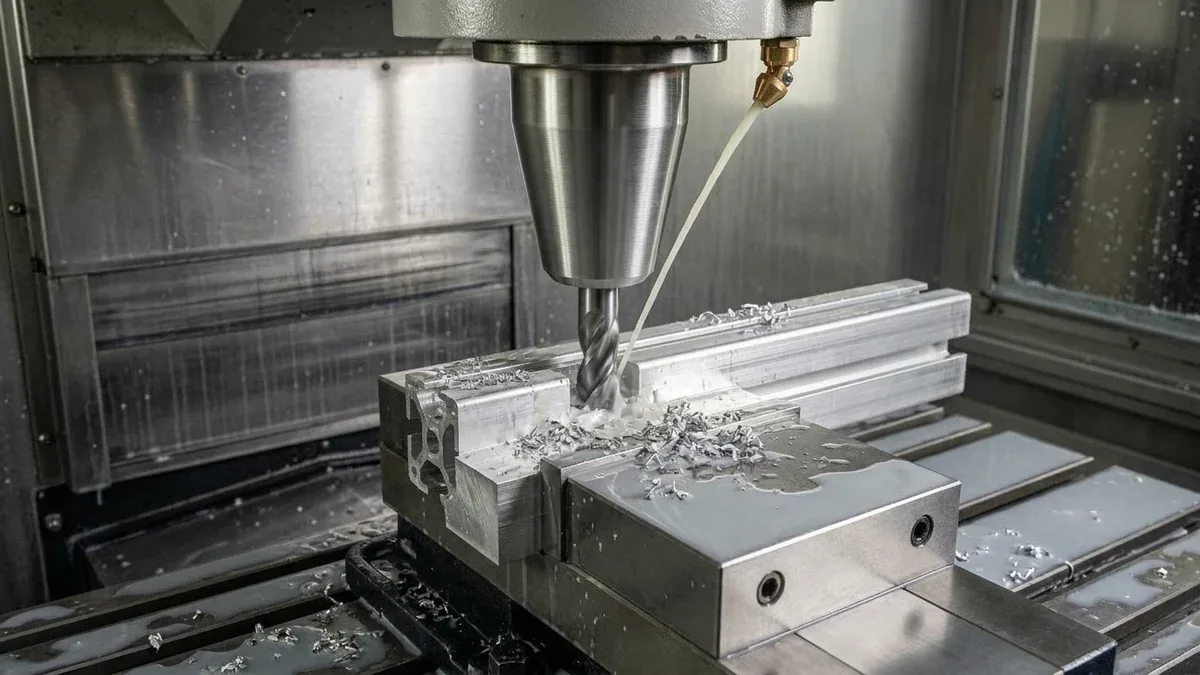
While extrusion forms uniform 2D cross-sections, functional assemblies require complex 3D features. Therefore, machine shops perform secondary operations on custom profiles.
High-speed machining centers drill cross-holes, mill mounting pockets, and tap threads rapidly. In addition, pneumatic multi-vise fixtures support long extrusions without vibrational chatter.
Following CNC machining, profiles receive protective surface finishes. Specifically, sulfuric acid anodizing produces a hard oxide barrier up to 25 microns thick.
Moreover, architectural powder coating provides vibrant exterior colors and weather resistance. Consequently, extruded components resist environmental corrosion for decades.
4. Common Extrusion Aluminum Alloys Selection Matrix
Choosing the correct aluminum alloy dictates extrudability, surface finish, and mechanical strength. To illustrate, review the primary extrusion alloys below:
| Alloy & Temper | Tensile Strength (MPa) | Yield Strength (MPa) | Extrudability Index | Primary Engineering Use Case |
|---|---|---|---|---|
| 6063-T6 | 240 MPa | 215 MPa | Exceptional (100%) | Architectural trim, intricate heatsinks, electronic cases |
| 6061-T6 | 310 MPa | 275 MPa | Good (60%) | Heavy structural framing, vehicle subframes, marine rails |
| 6005A-T6 | 270 MPa | 225 MPa | Very Good (80%) | Railway car bodies, bus structures, ladders |
| 7075-T6 | 570 MPa | 500 MPa | Challenging (15%) | High-stress aerospace spars, military armor extrusions |
5. Technical Engineering FAQ
Direct extrusion pushes the billet forward through a stationary die, creating high container friction. In contrast, indirect extrusion moves the die against a stationary billet. This eliminates container friction and saves 30% ram pressure.
Alloy 6063 exhibits superior extrudability and lower flow resistance than 6061. Consequently, it extrudes into complex thin-walled profiles and delivers a smoother surface finish that anodizes flawlessly.
Extrusion only forms continuous 2D cross-sections. In contrast, secondary multi-axis CNC machining cuts 3D mounting holes and locking tabs. Furthermore, it creates precision assembly datum surfaces.
Partner with Our Custom Extrusion & Precision CNC Machining Team
Optimize profile wall ratios, H13 extrusion die geometry, and secondary multi-axis CNC machining tolerances before production begins. Upload your 3D CAD files (STEP/IGES) and 2D GD&T drawings for a comprehensive shop-floor DFM review and custom quotation.
Upload 3D CAD for Extrusion & CNC DFM Review