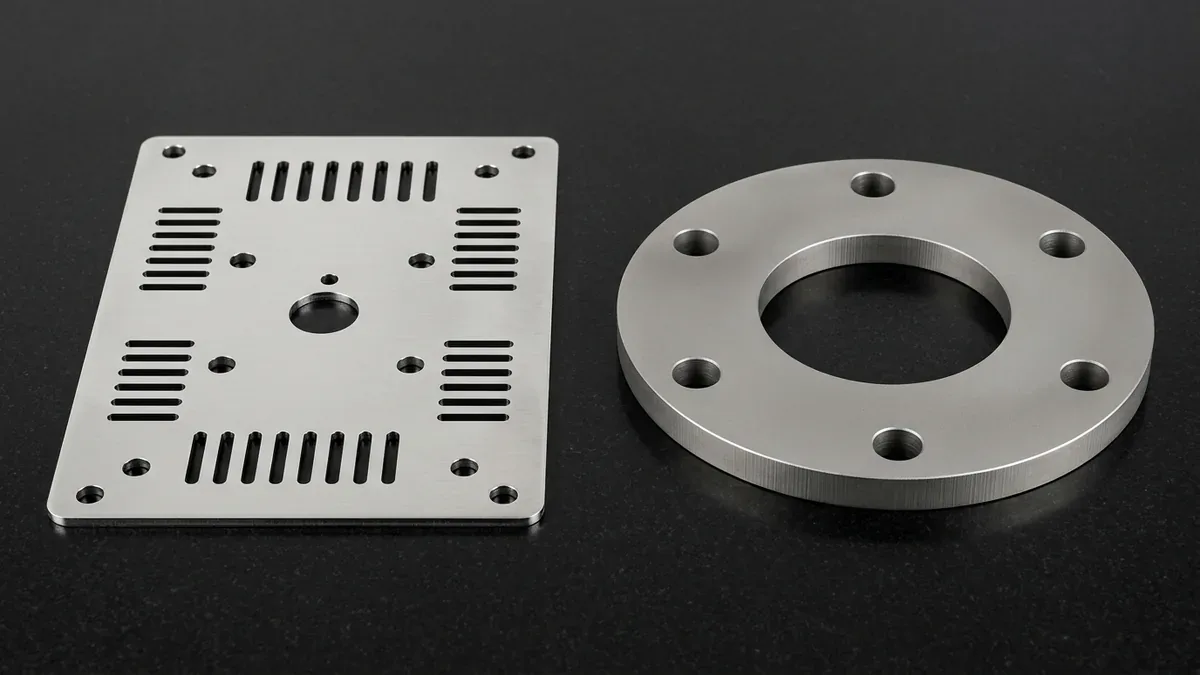
Precision profile blanking forms the structural foundation of modern mechanical enclosures and structural fabrications. Therefore, evaluating waterjet cutting vs laser cutting allows engineers to optimize dimensional accuracy, edge quality, and manufacturing economics. While both technologies utilize CNC gantry systems to follow complex CAD vector contours, their cutting physics differ fundamentally. Consequently, process selection directly impacts edge taper, thermal stress, and secondary post-processing requirements.
Abrasive waterjet cutting represents a cold erosion process utilizing ultra-high-pressure water infused with fine garnet particles. In contrast, industrial fiber laser cutting concentrates a coherent photon beam to vaporize material instantly. Each method presents distinct capabilities across raw plate thickness, material versatility, and cutting speed. In this engineering breakdown, we evaluate metallurgical impacts, kerf tolerances, and application boundaries.
1. Cutting Mechanics and Heat-Affected Zone (HAZ) Elimination
The absence or presence of thermal energy represents the most critical metallurgical difference between these processes. Fiber lasers deliver intense localized heat exceeding several thousand degrees Celsius. Consequently, laser cutting inevitably produces a heat-affected zone along the sliced perimeter. Within this narrow boundary, parent metal experiences localized metallurgical hardening, micro-structural recrystallization, and surface discoloration.
Conversely, abrasive waterjet cutting operates at near ambient room temperature. The continuous stream of water acts as an active coolant throughout the entire cutting path. As a result, waterjet cutting produces absolutely zero heat-affected zone and zero thermal warpage. This cold cutting characteristic proves invaluable when slicing heat-treated aerospace alloys, structural laminates, or work-hardening titanium grades.
2. Plate Thickness Envelopes and Kerf Width Dynamics
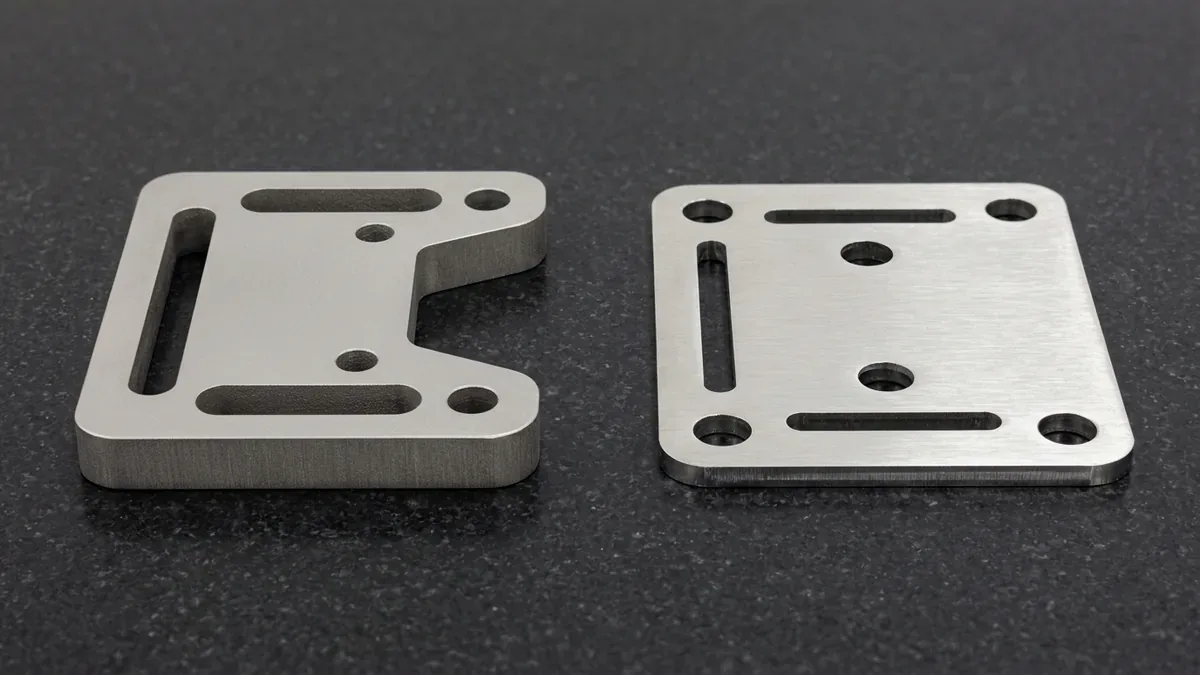
Material thickness capabilities establish a definitive operational boundary between these profiling technologies. Modern fiber laser cutters excel at processing thin-to-medium sheet metals with blistering traverse velocity. For stainless steel or aluminum under six millimeters, laser systems cut several times faster than waterjet tables. Furthermore, laser beam spot diameters measure only 0.1 mm, producing exceptionally narrow kerf slots.
However, when plate thickness exceeds twenty-five millimeters, fiber laser cutting efficiency deteriorates rapidly. In contrast, high-pressure waterjets powered by 60,000 PSI intensifier pumps slice through heavy armor plate effortlessly. Through our precision sheet metal fabrication services, engineers select laser cutting for thin chassis and waterjet for heavy billets. In addition, waterjet cutting handles reflective metals like brass and pure copper without back-reflection risks.
The comparative engineering parameters and process limitations are detailed in the table below.
| Operational Parameter | CNC Abrasive Waterjet Cutting | Industrial Fiber Laser Cutting |
|---|---|---|
| Thermal Impact | Zero Heat-Affected Zone (HAZ) | Localized HAZ (0.1 mm to 0.5 mm) |
| Typical Kerf Width | 0.75 mm to 1.20 mm | 0.10 mm to 0.30 mm |
| Maximum Practical Thickness | Up to 150 mm (metals & composites) | Up to 25 mm (mild steel / stainless) |
| Linear Cutting Accuracy | ±0.08 mm to ±0.15 mm | ±0.03 mm to ±0.05 mm |
| Edge Surface Roughness (Ra) | Ra 1.6 to 6.3 μm (matte satin) | Ra 0.8 to 3.2 μm (smooth, striations on thick) |
3. Edge Taper Management and Secondary Machining
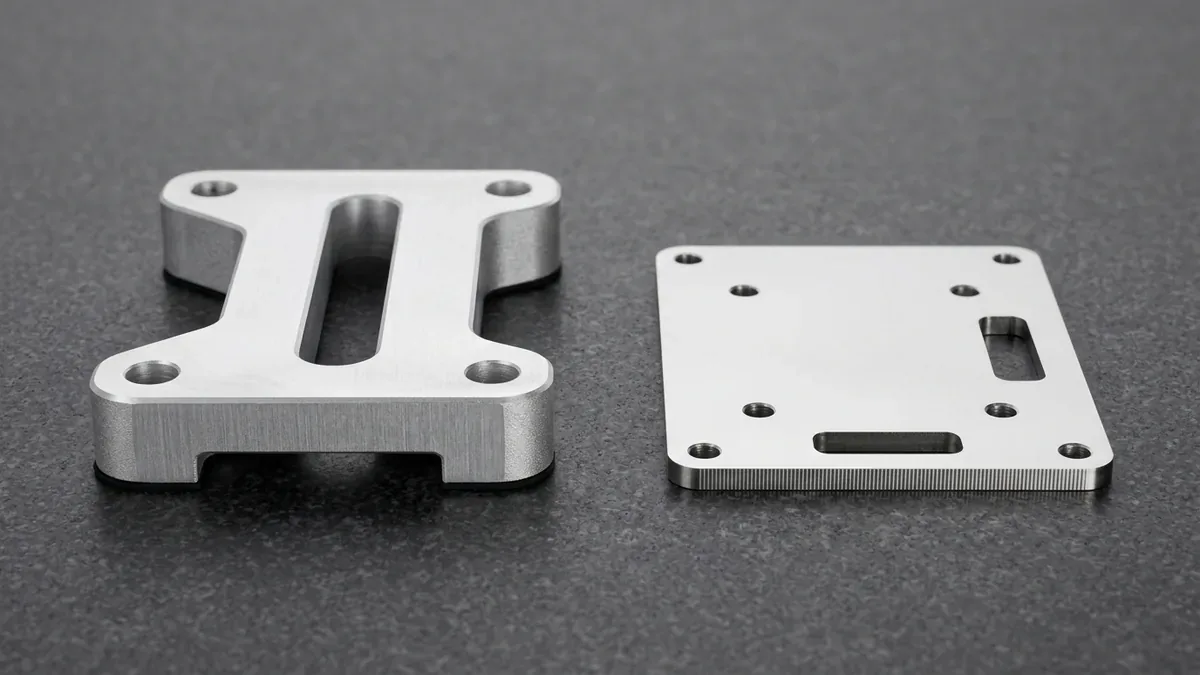
As abrasive waterjets penetrate deep into thick materials, the high-velocity jet stream gradually loses kinetic energy. Consequently, uncompensated waterjets can produce a noticeable edge taper across the vertical cut face. To eliminate this phenomenon, modern CNC waterjet tables utilize active five-axis tilting cutting heads. The articulated head tilts dynamically to counteract stream divergence, achieving perfectly square ninety-degree edges.
Laser cuts also exhibit minimal edge taper when cutting within optimal focal ranges. However, laser cutting can leave a slight oxidized scale along carbon steel cut edges. Therefore, parts slated for secondary robotic welding or powder coating require mechanical oxide removal. For parts demanding extreme precision, AS Prototypes integrates waterjet blanking with secondary machining. Specifically, precision CNC milling finishes critical mounting bores within ±0.010 mm (±0.0004″).
4. Material Compatibility and Production Economics
Material versatility represents one of abrasive waterjet cutting’s most formidable engineering strengths. Waterjets cut virtually any engineered material, including carbon fiber laminates, optical glass, ceramic tiles, and bulletproof armor. Because there is no thermal shock, composite laminates cut cleanly without resin delamination or fiber fraying.
Conversely, fiber lasers reign supreme for thin sheet metal production runs. Laser cutting requires no abrasive garnet consumables, lowering operational hourly costs significantly on thin materials. Moreover, laser cutting nested sheet metal nests run unattended overnight with automated pallet changers. AS Prototypes offers both technologies under one roof, providing unbiased engineering guidance for prototype and production volumes.
The application suitability across common engineering materials is summarized in the matrix below.
| Material Category | Waterjet Cutting Suitability | Fiber Laser Cutting Suitability |
|---|---|---|
| Thin Stainless Steel (<3 mm) | Good (slower than laser) | Optimal (fastest cycle, lowest unit cost) |
| Thick Aluminum Plate (>25 mm) | Optimal (clean cut, no dross) | Poor (excessive dross, thermal warping) |
| Highly Reflective Copper / Brass | Optimal (no back-reflection risk) | Moderate (requires specialized fiber laser) |
| Carbon Fiber Reinforced Polymers | Optimal (no melting or delamination) | Unsuitable (burns epoxy matrix) |
| Optical Glass & Engineering Ceramics | Optimal (with low-pressure pierce) | Unsuitable (thermal fracture failure) |
5. Technical Engineering FAQ
Waterjet cutting utilizes high-velocity water and abrasive garnet to erode material mechanically at room temperature. The continuous water flow absorbs all frictional heat, preventing thermal distortion or metallurgical microstructure changes.
Fiber laser cutting is significantly faster for thin sheet metals under six millimeters. Laser heads traverse at speeds up to several meters per minute, making laser cutting far more economical for high-volume blanking.
Yes. Modern CNC waterjet machines utilize dynamic 5-axis taper compensation. Consequently, they hold tolerances within plus or minus 0.08 mm, satisfying aerospace structural blanking specifications.
Engineer Precision Custom Sheet Metal Enclosures & Brackets
Eliminate bend springback, hole distortion, and assembly interference before cutting metal. Upload your 3D CAD files (STEP/IGES) and 2D flat-pattern drawings for a dedicated sheet metal DFM review and custom production quotation.
Upload CAD Files for Sheet Metal DFM & Quote