
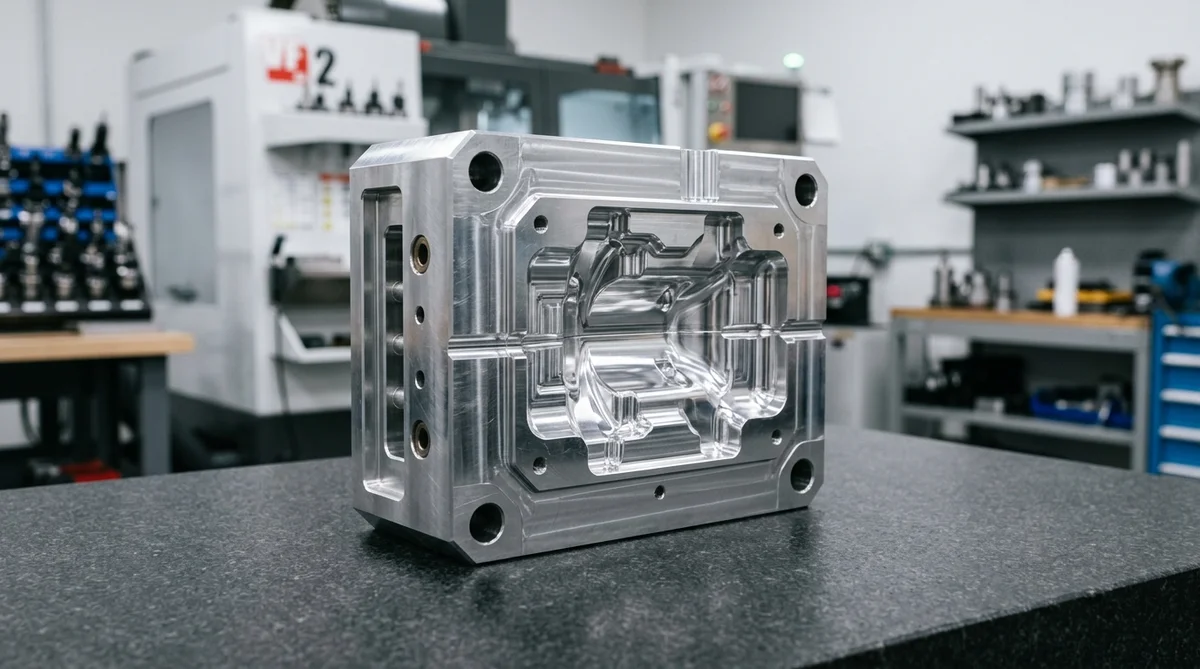
In hardware product realization, the transition between one-off functional prototyping and high-volume mass production has historically been an economic chasm. High-volume manufacturing demands substantial non-recurring engineering (NRE) expenditures—often tens or hundreds of thousands of dollars for hardened steel tooling—with production lead times spanning three to six months. Conversely, rapid prototyping workflows are optimized for single iterations rather than repeatable quality control, resulting in exorbitant per-unit costs when orders scale to dozens or thousands of pieces.
Short-run production—commonly referred to as High-Mix Low-Volume (HMLV) manufacturing—bridges this divide. Spanning batch volumes from 10 to 5,000 units, short-run manufacturing enables OEMs and hardware startups to execute pilot market launches, clinical trials, bridge-to-production runs, and bespoke aerospace assemblies without paralyzing capital investments. Among structural engineering materials, aluminum alloys (predominantly 6061-T6, 7075-T651, 5083, and A380/ADC12) serve as the cornerstone of agile manufacturing. This guide explores the engineering methodologies, rapid tooling dynamics, and digital manufacturing workflows that make low-volume aluminum production commercially viable and technically rigorous.
1. The Economics of High-Mix Low-Volume (HMLV) Manufacturing
The total unit cost in mechanical manufacturing is governed by the classic cost amortization curve:
Unit Cost = (Tooling CapEx + NRE Setup) / Batch Quantity + Material Cost + Machine Cycle Cost + Finishing Overhead
In massive production runs (100,000+ units), fixed tooling and setup costs approach zero on a per-unit basis, making raw cycle time the sole cost driver. In short-run manufacturing, however, setup time, machine changeover, fixturing design, and CAM programming constitute up to 60% of the total project expenditure. Achieving cost efficiency requires decoupling batch economics from traditional tooling constraints through agile engineering.
Why Aluminum Dominates Agile Short-Run Programs
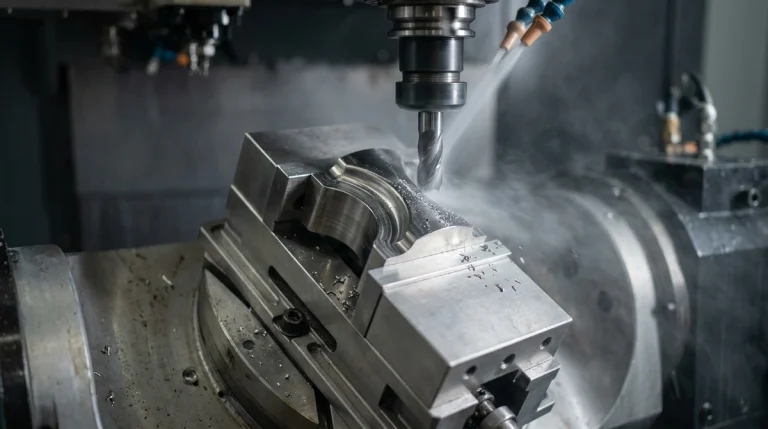
- Exceptional Machinability Index: Aluminum alloys such as 6061-T6 and 7075-T6 exhibit high shear angles and low cutting forces. Modern high-speed machining (HSM) centers can operate at surface speeds exceeding 1,200 m/min with aggressive chip loads, reducing cutting cycle times by 65% compared to stainless steel or titanium.
- Minimal Tool Wear: Low abrasive wear on micro-grain carbide cutters eliminates mid-run tool offsets, allowing unbroken unattended batch execution.
- Thermal Stability and Recyclability: High thermal dissipation prevents part warping during aggressive roughing, while clean chips retain premium metallurgical salvage value, mitigating raw material expense.
- Versatile Post-Processing Compatibility: Aluminum supports an expansive spectrum of functional finishes—from conductive chromate conversion (Alodine) to Type III hardcoat anodizing and powder coating—without requiring corrosive pre-plating baths.
2. Agile CNC Machining: Eliminating Setup Bottlenecks
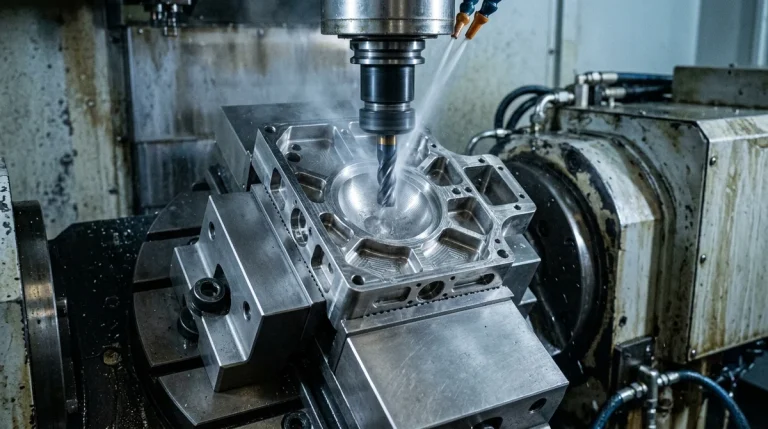
The principal barrier to affordable short-run CNC machining is setup changeover latency. When a setup machinist spends three hours setting up vices, dialing in work coordinate systems (G54-G59), and setting tool height offsets to machine a batch of twenty parts, setup cost dwarfs actual cutting cost. At AS Prototypes, our shop floor implements SMED (Single-Minute Exchange of Die) principles to compress changeover time to minutes.
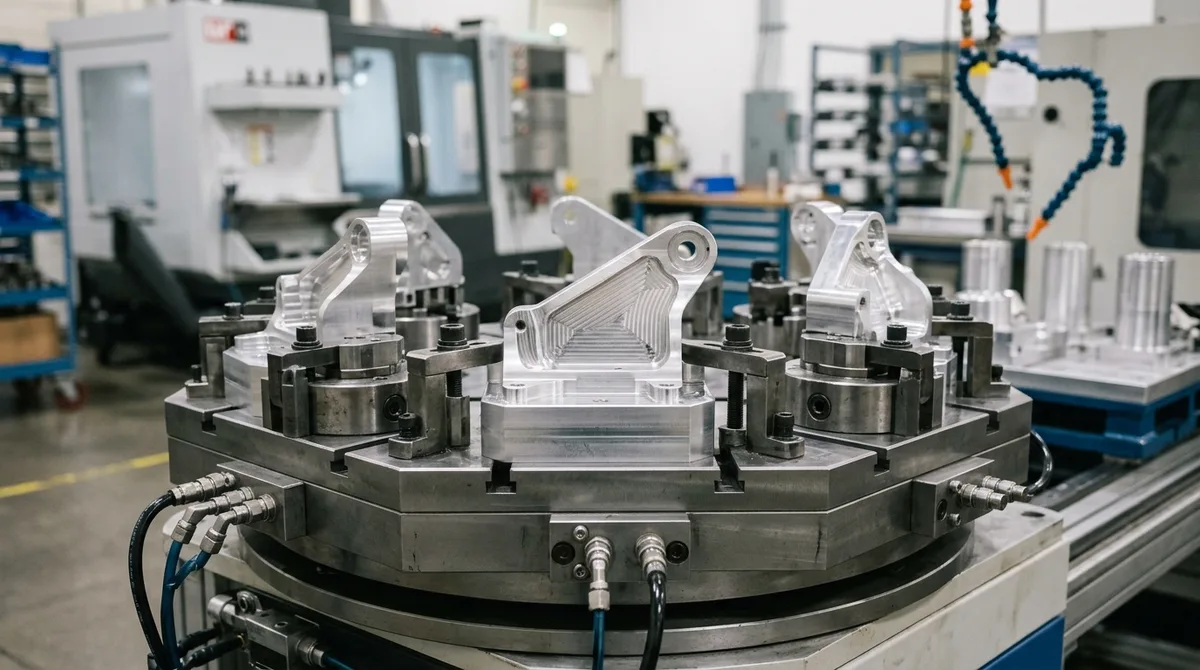
Core Machining Tactics for Short Runs
- Standardized Zero-Point Clamping Systems: Using pneumatic or mechanical zero-point base plates (e.g., Lang, Schunk, 5th Axis), multi-axis fixtures can be swapped with sub-5-micron repeatability in less than 60 seconds without re-probing workpiece datum points.
- Multi-Pallet Dual-Table Automation: Pallet-changing vertical and horizontal machining centers (HMCs) permit operators to load raw aluminum billets and unload finished components on pallet A while the spindle continuously cuts on pallet B, achieving near 90% spindle utilization.
- Master Tool Library Standardization: Rather than tearing down tooling carousels between different customer jobs, machines are outfitted with standard 30- to 60-tool master libraries. Core roughers, finishing end mills, chamfer cutters, spot drills, and high-performance thread mills remain permanently loaded and pre-calibrated via laser tool setters.
- Parametric CAM Templates: Standardized feature-based machining macros automatically apply proven high-speed trochoidal roughing toolpaths and constant-cusp 3D finishing passes directly to imported STEP/IGES models, collapsing CAM programming cycles from hours to minutes.
3. Rapid Tooling: Soft Aluminum Tooling vs. Hardened Steel
For short-run plastic injection molding (50 to 5,000 parts) or sheet metal forming, traditional hardened tool steels (such as H13, S136, or P20 hardened to 48–54 HRC) represent unnecessary financial overkill. Fabricating hardened steel molds involves lengthy roughing, furnace heat treatment, thermal stress relief, EDM spark erosion, and tedious manual benching—taking 6 to 12 weeks.
Aluminum Rapid Tooling replaces tool steel with aerospace-grade wrought aluminum plate (such as QC-10, Alumec 89, or stress-relieved 7075-T651):
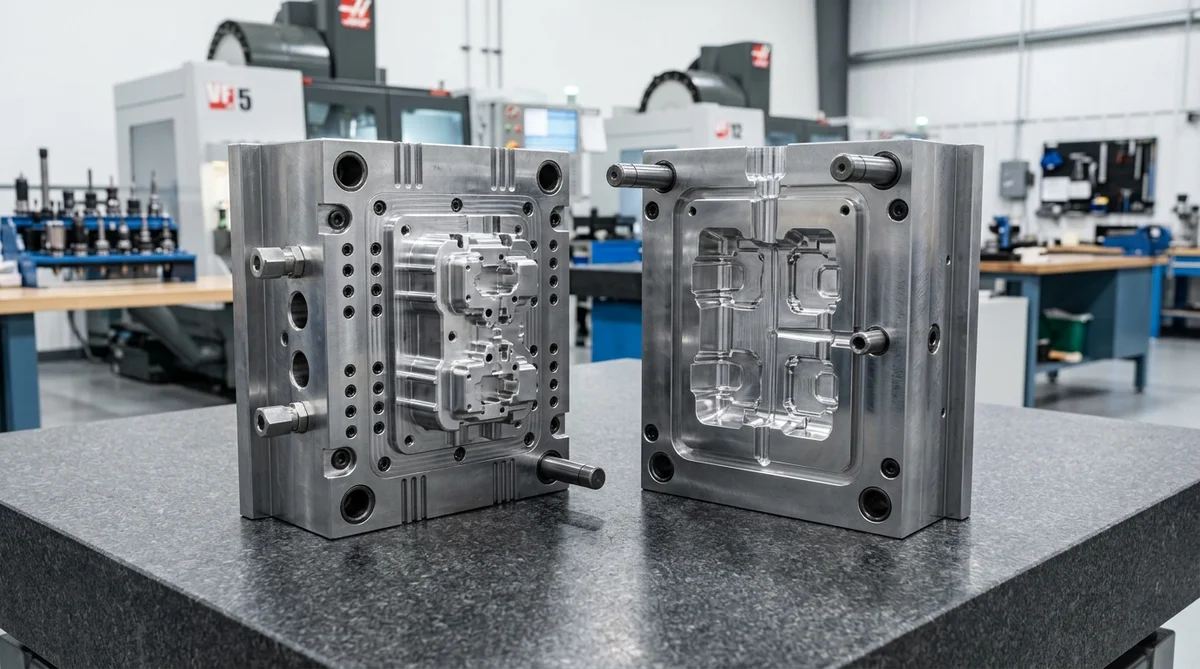
Technical Merits of Aluminum Soft Tooling
- 80% Reduction in Machining Time: 7075-T651 aluminum exhibits a Brinell hardness of ~150 HB and can be milled at five times the feed rates of steel. Deep cavity pockets, cooling water lines, and runner systems are machined in days rather than weeks.
- Thermal Conductivity Advantage: Aluminum conducts thermal energy at 130 to 160 W/m·K—roughly 4 to 5 times faster than standard mold steels (κ ≈ 30 W/m·K). Faster heat extraction directly reduces injection molding cooling cycle times by 30% to 50%, dramatically improving part throughput.
- Tool Life Longevity: When molding non-abrasive engineering polymers (such as polypropylene, ABS, polycarbonate, or POM), a precision 7075 aluminum mold comfortably delivers 5,000 to 25,000 defect-free parts with minimal parting-line degradation.
- Rapid Engineering Change Orders (ECO): If a design modification is required after pilot testing, aluminum core and cavity inserts can be welded, re-machined, or re-sparked via EDM with negligible downtime.
4. Rapid Sand & Investment Casting via 3D Printed Patterns
Foundry casting has long been the gold standard for producing complex, thin-walled, or organically curved aluminum components (such as automotive suspension knuckles, intake manifolds, and pump housings). However, conventional sand and investment casting require expensive physical master patterns machined from hardwood, urethane tooling board, or cast iron.
Digital Patternless Foundry Workflows
Modern agile foundries bypass physical pattern machining using digital additive manufacturing:
- Binder Jetting Sand Molds: Industrial 3D sand printers deposit a liquid binder over fine silica or ceramic sand layers (150 μm layer thickness) to print complex sand molds and intricate internal cores directly from CAD data. Cores featuring re-entrant angles and complex undercut cooling jackets—impossible to pull with rigid tooling—are cast with zero tooling investment.
- QuickCast SLA / 3D-Printed Wax Patterns: For precision investment casting (A356-T6 or A380 aluminum), stereolithography (SLA) prints hollow, lightweight resin master patterns with internal honeycomb ribs. During autoclave burnout, the resin pattern collapses inward and vaporizes without ash residue, preventing ceramic shell cracking. Lead times collapse from 12 weeks to under 15 business days.
5. Wire EDM Stack-Cutting: Low-Cost 2D Profiling
When short-run components feature intricate internal apertures, narrow slots (down to 0.15 mm), square internal corners, or high aspect-ratio keyways, conventional CNC milling struggles due to tool deflection and minimum inside-corner radius constraints. Custom broaching tools or specialty stamping dies cost thousands of dollars.
Wire Electrical Discharge Machining (Wire EDM) provides an agile solution through stack-cutting:
- Simultaneous Batch Processing: Multiple sheet metal blanks, extruded aluminum plates, or laser-cut blanks are clamped tightly into a single stack (up to 150–200 mm tall).
- High-Precision Wire EDM: A traveling brass or zinc-coated wire (0.20 to 0.25 mm diameter) cuts through the entire clamped stack in a single programmed CNC path. Tens or hundreds of identical components are produced in one continuous cycle with positional tolerances tighter than ±0.005 mm and zero burrs.
- Zero Tool Wear Compensation: Because the electrical spark does not exert mechanical cutting pressure, ultra-thin webs and delicate flexure features will not distort or work-harden.
6. Engineering Comparison: Short-Run Production Technologies
The following engineering comparison summarizes the cost structure, lead times, and optimal volume thresholds for modern short-run manufacturing technologies:
| Technology | Optimal Batch Range | Tooling / NRE Investment | First-Article Lead Time | Achievable Tolerances | Unit Cost Profile | Ideal Component Geometries |
|---|---|---|---|---|---|---|
| Multi-Axis CNC Machining | 10 – 1,000 parts | Very Low (Soft jaws & CAM setup) | 4 – 8 business days | ±0.010 mm (±0.0004 in) | Moderate to Low | Prismatic housings, brackets, heat sinks, complex 5-axis aerospace fittings |
| Aluminum Rapid Tooling (Molding) | 250 – 10,000 parts | Moderate ($3k – $15k) | 18 – 35 business days | ±0.050 mm (±0.002 in) | Very Low per part | Plastic bezels, consumer electronics shells, medical device enclosures |
| 3D Printed Sand / Wax Casting | 10 – 250 parts | Low (Zero hard pattern cost) | 2 – 4 weeks | ±0.25 mm (±0.010 in) | Moderate | Organic engine blocks, fluid pump manifolds, lightweight hollow brackets |
| Wire EDM Stack-Cutting | 50 – 2,000 parts | Minimal (Stack clamping fixture) | 4 – 8 business days | ±0.005 mm (±0.0002 in) | Low to Very Low | Flat plates, gears, internal splines, flexures, micro-slotted shims |
| DMLS / SLM Metal 3D Printing | 1 – 25 parts | Zero tooling investment | 4 – 8 business days | ±0.10 mm (±0.004 in) | High (Powder & machine cost) | Lattice structures, conformal cooling channels, topology-optimized aerospace nodes |
7. Supply Chain Integration & Quality Assurance in Short Runs
Executing successful low-volume production requires more than machine tools; it demands a resilient supply chain and tight metrological feedback loops:
- Strategic Raw Material Buffering: Delays in procuring verified aluminum billets (such as AMS-QQ-A-250/11 for 6061-T6 or AMS 4045 for 7075-T651) halt short-run momentum. AS Prototypes maintains extensive inventory caches of domestic and aerospace-prime-grade bar stock with traceable MTR, plate, and custom extrusions to initiate CNC cutting immediately upon PO release.
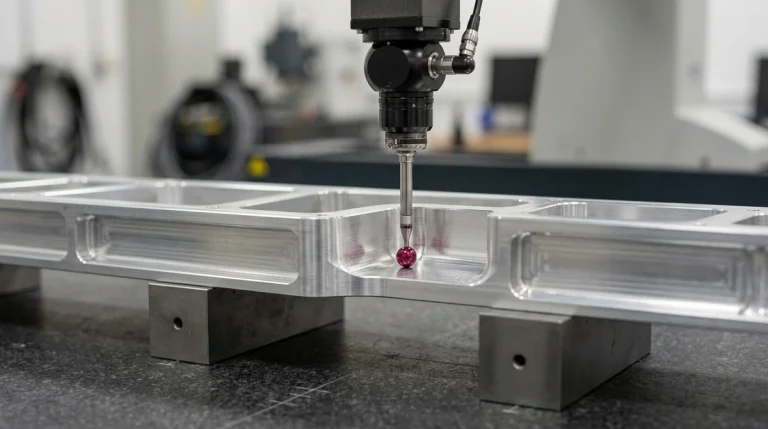
- First Article Inspection (FAI) & CMM Verification: Before batch release, the first machined part undergoes full geometric verification on coordinate measuring machines (CMM) and high-resolution optical vision systems. Full dimensional inspection reports (AS9102 format) are generated to validate toolpath offsets.
- Statistical Process Control (SPC): For batch runs between 100 and 5,000 units, periodic sampling tracks critical-to-function dimensions to ensure capability indices (Cpk > 1.33), preventing tool wear creep and maintaining zero-defect delivery.
Quality 7075-T651 aluminum molds routinely produce 5,000 to 25,000 shots of unfilled polymers like ABS, PP, and PC. For abrasive glass-filled resins, aluminum tool life ranges between 2,000 and 5,000 shots before wear manifests on parting lines.
The economic crossover point typically occurs between 50 and 200 units. Below 50 units, 5-axis CNC machining avoids upfront NRE mold costs. Above 200 units, the cycle-time advantage of aluminum tooling delivers significant per-part cost reductions.
For CNC-machined batches (10–300 parts), standard turnaround is 7 to 12 business days. For aluminum rapid injection tooling and T1 molded samples, standard turnaround is 18 to 35 business days including full CMM dimensional inspection.
Accelerate Your Low-Volume Production with AS Prototypes
Whether you require 20 precision CNC milled aluminum enclosures for clinical hardware trials, 500 rapid-tooled injection molded housings, or 2,000 stack-cut wire EDM shims, AS Prototypes delivers rapid turnaround, tight tolerances, and predictable batch economics under one roof.
Our senior engineering team reviews every CAD model for DFM optimization, tool clearance, and cost reduction prior to spindle start.