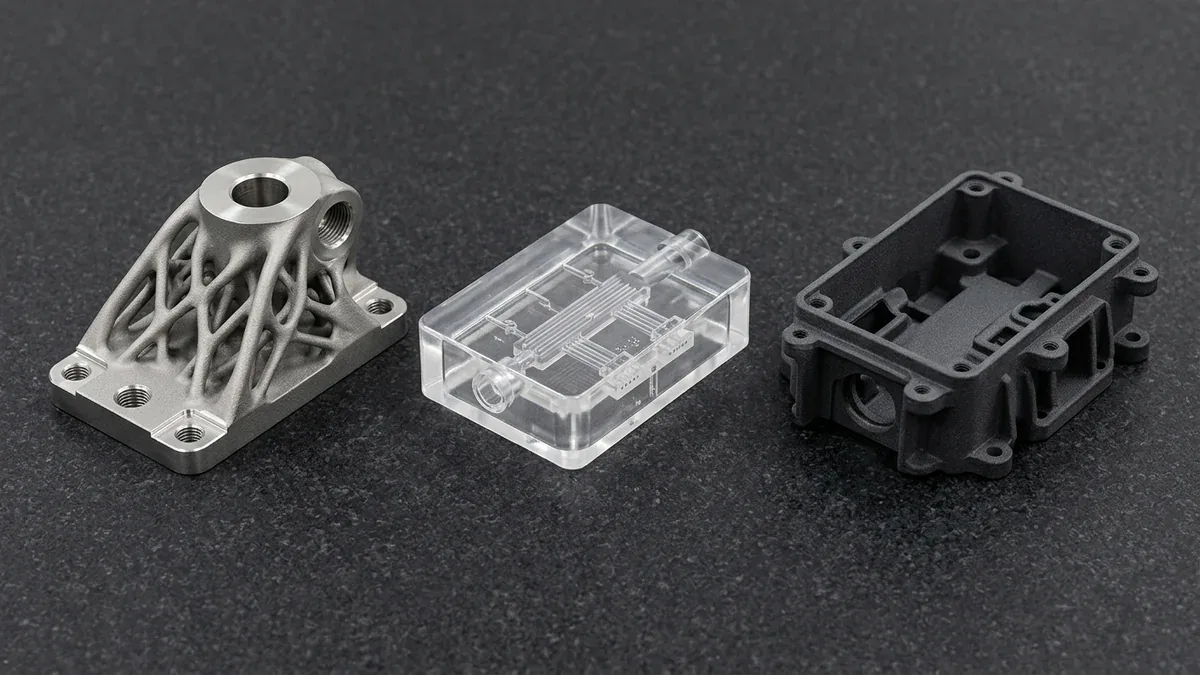
Selecting the right additive manufacturing technology determines the mechanical strength, surface finish, thermal performance, and unit cost of your prototype. Today, design engineers can leverage seven primary 3D printing types to turn complex digital CAD designs into high-performance components. Each technology relies on distinct physical states of matter—fine atomized metal powders, liquid photopolymer resins, molten thermoplastic filaments, and composite sheets—activated by focused fiber lasers, UV projection engines, or thermal extrusion nozzles.
According to the international ISO/ASTM 52900 standard, additive manufacturing divides into seven distinct categories. Below, we examine each technology family in detail, detailing key material selections, dimensional tolerances, and engineering trade-offs to help you choose the right process for functional testing and bridge production.
- 1. Powder Bed Fusion (PBF: DMLS, SLM, SLS)
- 2. Vat Photopolymerization (SLA, DLP, LCD)
- 3. Material Extrusion (FDM / FFF)
- 4. Material Jetting (PolyJet / Multi-Jet)
- 5. Binder Jetting (Metal & Sand BJ)
- 6. Directed Energy Deposition (DED)
- 7. Sheet Lamination (SL)
- 8. Design for Additive Manufacturing (DFAM) Guidelines
- 9. Comprehensive Engineering Comparison: The 7 AM Technologies
- 10. Metal AM vs. Polymer AM: Process Selection Matrix
- 11. Technical Engineering FAQ
1. Powder Bed Fusion (PBF: DMLS, SLM, SLS)
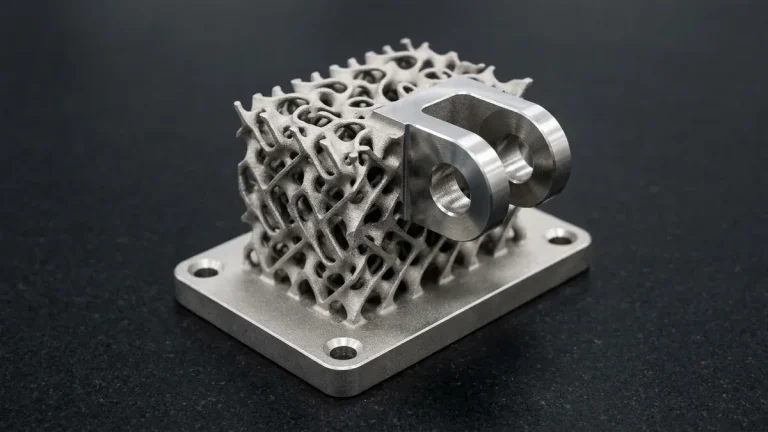
Powder Bed Fusion represents the gold standard for high-strength functional prototypes, lightweight structural brackets, and end-use industrial hardware. In this process, a precision recoater blade spreads a micro-thin layer of fine atomized powder (typically 20 to 60 μm) across a heated build platform. Subsequently, a high-power thermal source—such as an ytterbium fiber laser or electron beam—selectively scans and fuses the cross-sectional geometry.
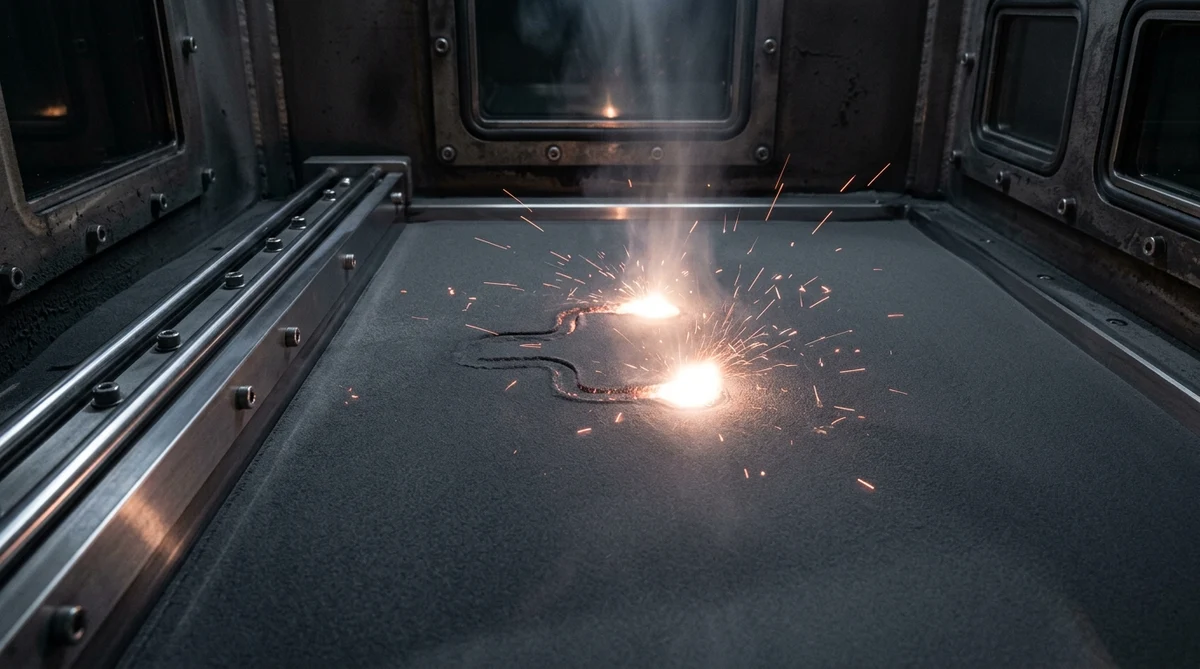
For metallic alloys, Direct Metal Laser Sintering (DMLS) and Selective Laser Melting (SLM) utilize focused fiber lasers inside a strictly controlled inert argon or nitrogen chamber. These systems achieve full metallurgical bonding with relative densities exceeding 99.7%. Common aerospace and medical alloys include Titanium Ti-6Al-4V Grade 5, Inconel 718, 316L stainless steel, and AlSi10Mg aluminum. When your project demands flight-critical mechanical integrity, our specialized metal 3D printing capabilities provide rapid turnarounds with tight dimensional control.
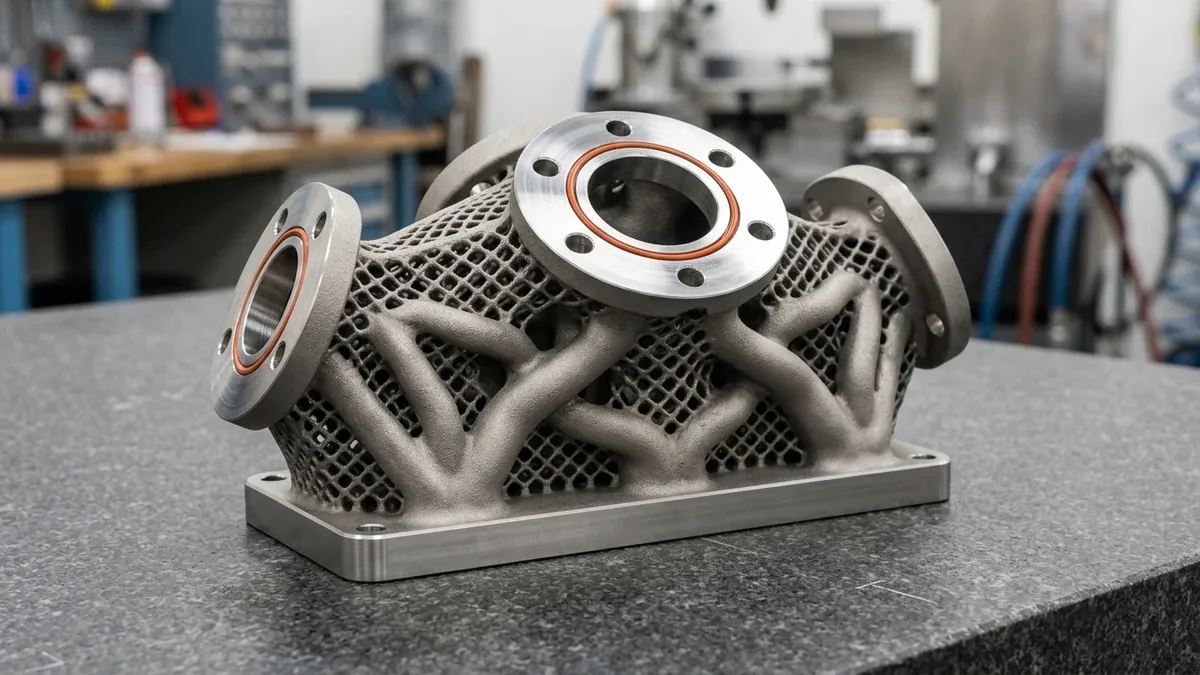
In polymer applications, Selective Laser Sintering (SLS) fuses thermoplastic powders such as Polyamide 12 (Nylon PA12) and PA11 without requiring dedicated sacrificial support structures. Because the surrounding unsintered powder bed continuously supports overhanging geometry, SLS empowers engineers to print highly complex internal channels, nested mechanical assemblies, and organic ducting impossible to machine with traditional cutting tools.
2. Vat Photopolymerization (SLA, DLP, LCD)
Vat Photopolymerization processes convert liquid photocurable resin into solid cross-linked polymers through localized ultraviolet (UV) light exposure. In Stereolithography (SLA), a galvanometer-guided UV laser traces cross-sections point-by-point, whereas Digital Light Processing (DLP) flashes an entire cross-sectional layer simultaneously using a digital micromirror device (DMD). Liquid Crystal Display (LCD) masking utilizes an LED array masked by an LCD panel to expose full layers with remarkable cost efficiency.
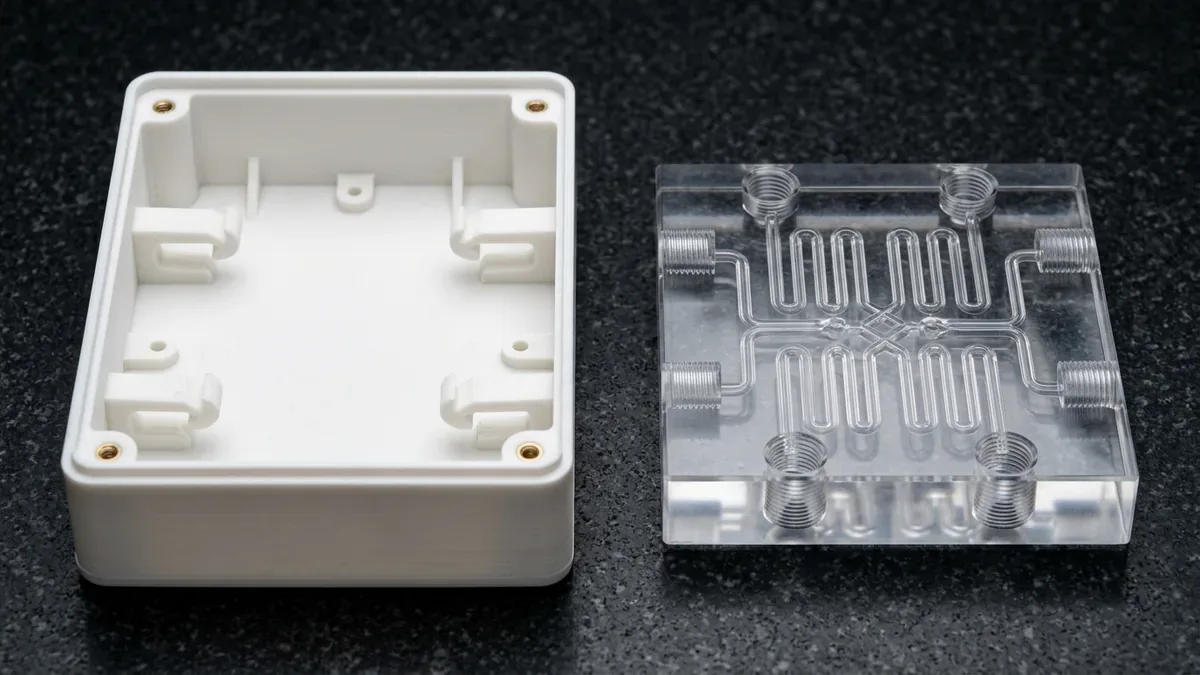
Vat photopolymerization achieves the highest feature resolution and smoothest surface finishes of any polymer additive technology:
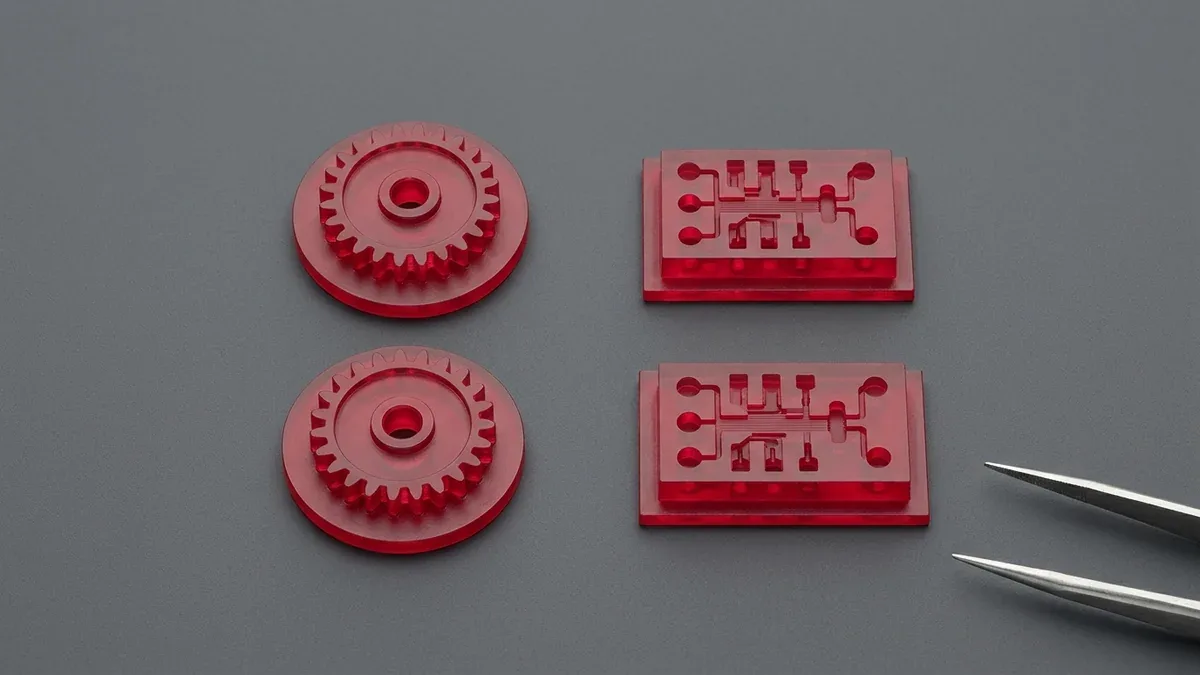
- Layer Heights & Resolution: Capable of printing at ultra-fine 25 to 100 μm layer thicknesses with minimum feature details down to 0.1 mm and surface roughness as low as Ra 0.8 μm after post-curing.
- Engineering Resins: Formulations range from Tough ABS-like and polypropylene-like resins for functional snap-fit housings to Water-Clear acrylic resins for optical lenses and fluidic sight glasses, as well as ceramic-filled resins with heat deflection temperatures exceeding 250°C.
- Ideal Applications: Master patterns for polyurethane vacuum casting, dental surgical guides, aesthetic consumer electronics appearance models, and microfluidic lab-on-a-chip prototypes.
3. Material Extrusion (FDM / FFF)
Material Extrusion, commonly known as Fused Deposition Modeling (FDM) or Fused Filament Fabrication (FFF), is the most ubiquitous additive manufacturing method across industrial workshops. A continuous thermoplastic filament is drawn into a heated extrusion head, melted into a semi-liquid state, and precisely deposited layer-by-layer along computer-controlled CNC toolpaths.
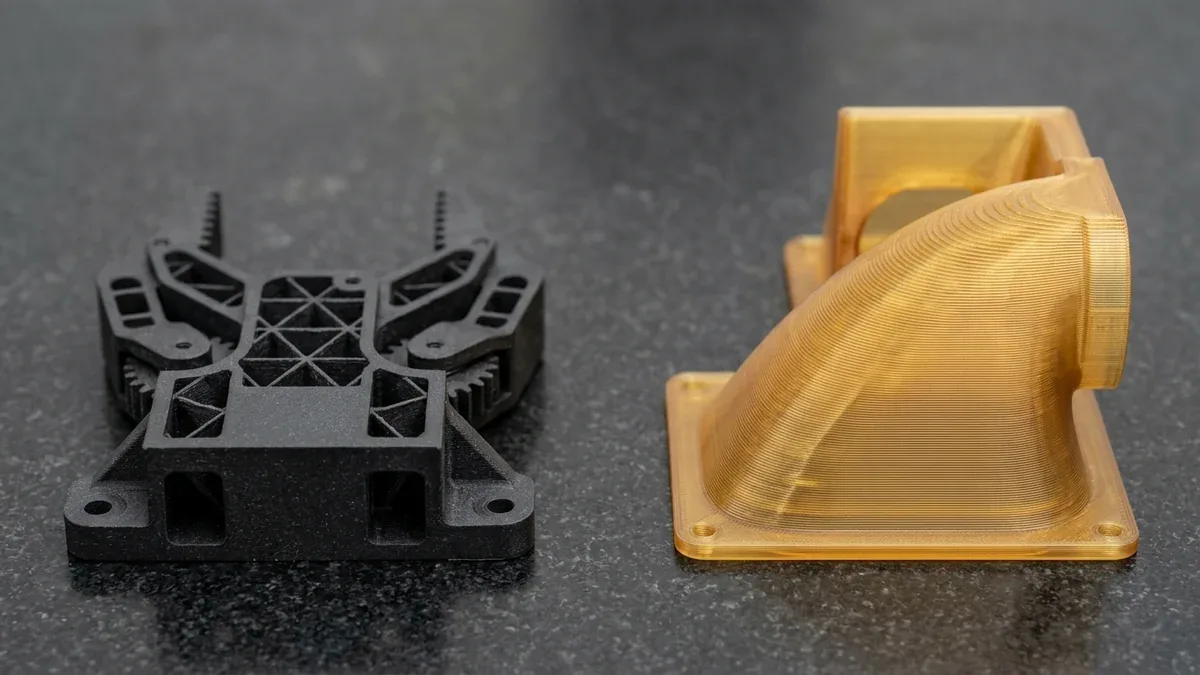
Industrial-grade FDM systems deliver unmatched engineering material versatility:
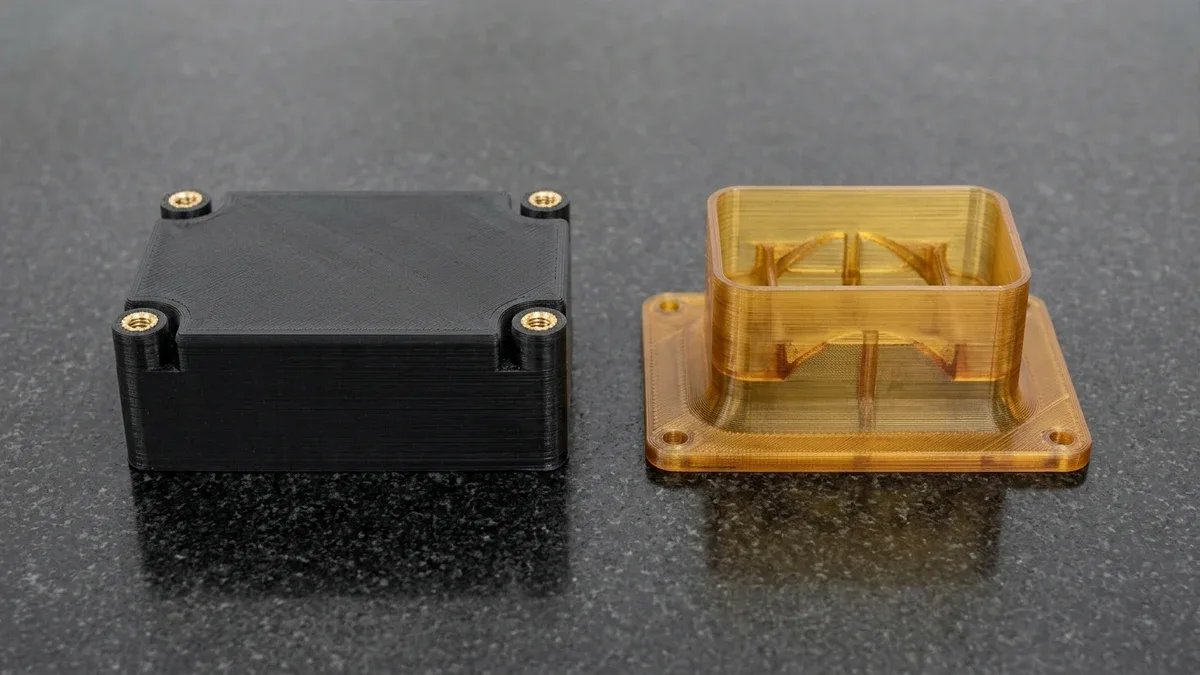
- Engineering Thermoplastics: Direct extrusion occurs with genuine production polymers, including ABS-M30, Polycarbonate (PC), high-temperature aerospace PEI (Ultem 9085 / 1010), and PEEK for harsh chemical and thermal environments.
- Composite Materials: Carbon-fiber-reinforced polyamides (PA-CF) provide exceptional stiffness-to-weight ratios, rivaling cast aluminum in rigidity while reducing component weight by up to 40%.
- Mechanical Anisotropy: Parts exhibit high mechanical strength within the horizontal XY printing plane, while interlaminar Z-axis tensile strength is typically 20% to 35% lower due to thermal weld lines. Consequently, strategic build orientation is vital when producing rugged robotics brackets, check fixtures, and assembly jigs.
4. Material Jetting (PolyJet / Multi-Jet)
Material Jetting operates similarly to high-resolution inkjet 2D printing. Hundreds of piezoelectric printheads deposit micro-droplets of photopolymer resins onto a build platform, where an integrated UV curing lamp instantly solidifies each layer.
Material Jetting stands apart for its multi-material and multi-durometer printing capabilities:
- Digital Materials: By blending rigid Vero materials with flexible rubber-like Agilus30 elastomers on the fly, engineers can produce gradient parts with variable Shore A durometers (from Shore 30A to 95A) in a single uninterrupted print.
- Overmolding Simulation: Enables rapid prototyping of soft-touch ergonomic tool grips over rigid substrates, integrated fluidic gaskets, and complex multi-color CMF (Color, Material, Finish) validation samples.
- Surface Quality: Delivers injection-molded-quality smooth surfaces without visible layer stair-stepping (Ra ≈ 0.8 μm).
5. Binder Jetting (Metal & Sand BJ)
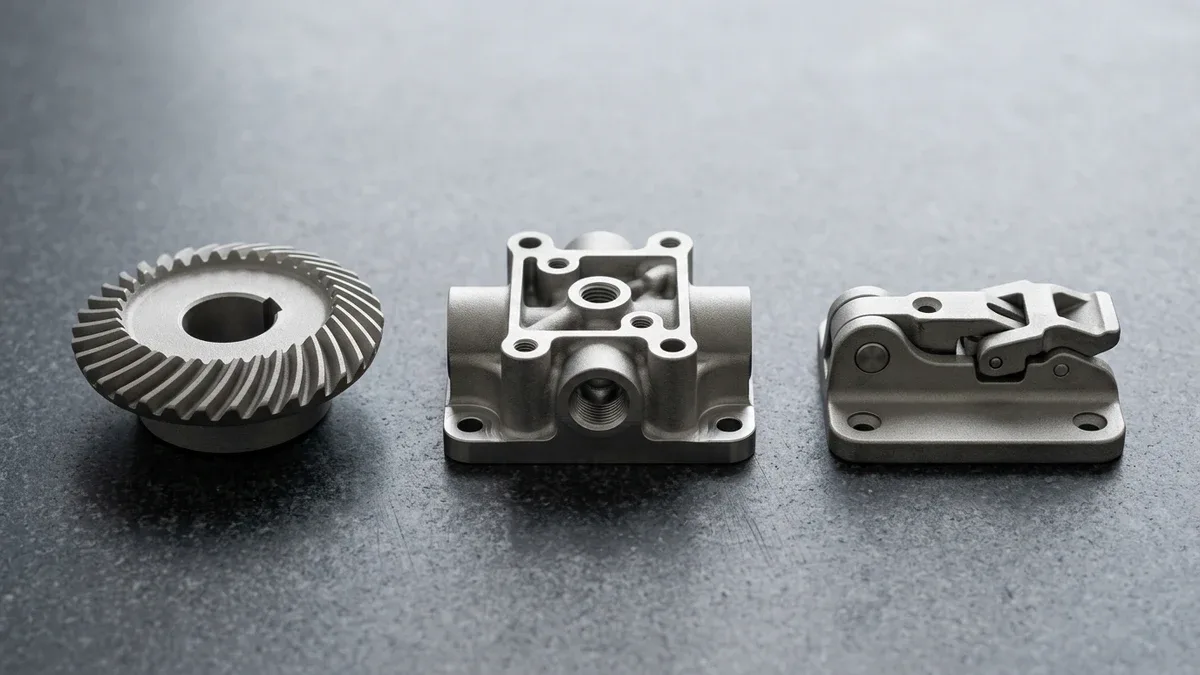
Binder Jetting utilizes a multi-channel printhead to selectively deposit a liquid binding adhesive onto a spread layer of powdered metal, ceramic, or foundry sand. Unlike PBF, Binder Jetting is an ambient-temperature process that introduces zero thermal residual stresses or distortion during the print cycle.
The process operates across two primary industrial domains:
- Metal Binder Jetting (MBJ): The printed “green part” undergoes solvent debinding followed by high-temperature vacuum furnace sintering, achieving relative densities exceeding 97% in 316L and 17-4PH stainless steel, or bronze infiltration. It provides high volumetric throughput for small, intricate metal components without requiring laser support anchors.
- Sand Binder Jetting: Large-format sand systems print complex foundry sand molds and cores directly from 3D CAD files within hours, eliminating the need for expensive wood or aluminum tooling patterns in rapid casting.
6. Directed Energy Deposition (DED)
Directed Energy Deposition focuses thermal energy—such as an industrial laser, plasma arc, or electron beam—directly at the deposition zone while simultaneously feeding metal wire or blown powder through a multi-axis coaxial nozzle. The focused heat source melts the feedstock as it contacts the substrate, creating metallurgically bonded clad tracks.
DED achieves massive deposition rates (up to several kilograms per hour) compared to powder bed systems. Therefore, manufacturers deploy DED primarily for large aerospace structural repairs, adding features onto existing forgings, and creating multi-axis hybrid machine tools that combine additive cladding with high-speed CNC finish milling.
7. Sheet Lamination (SL)
Sheet Lamination bonds thin sheets of material together using adhesive, heat, or ultrasonic welding, followed by laser or CNC contour cutting. Ultrasonic Additive Manufacturing (UAM) utilizes ultrasonic energy to bond metal foils at room temperature, enabling engineers to embed delicate electronic sensors, thermocouples, and fiber optics directly inside solid metal matrices without thermal degradation.
8. Design for Additive Manufacturing (DFAM) Guidelines
Regardless of which 3D printing type you select, designing with additive principles in mind minimizes build failures, optimizes surface quality, and reduces unnecessary post-processing costs. Key geometric rules include:
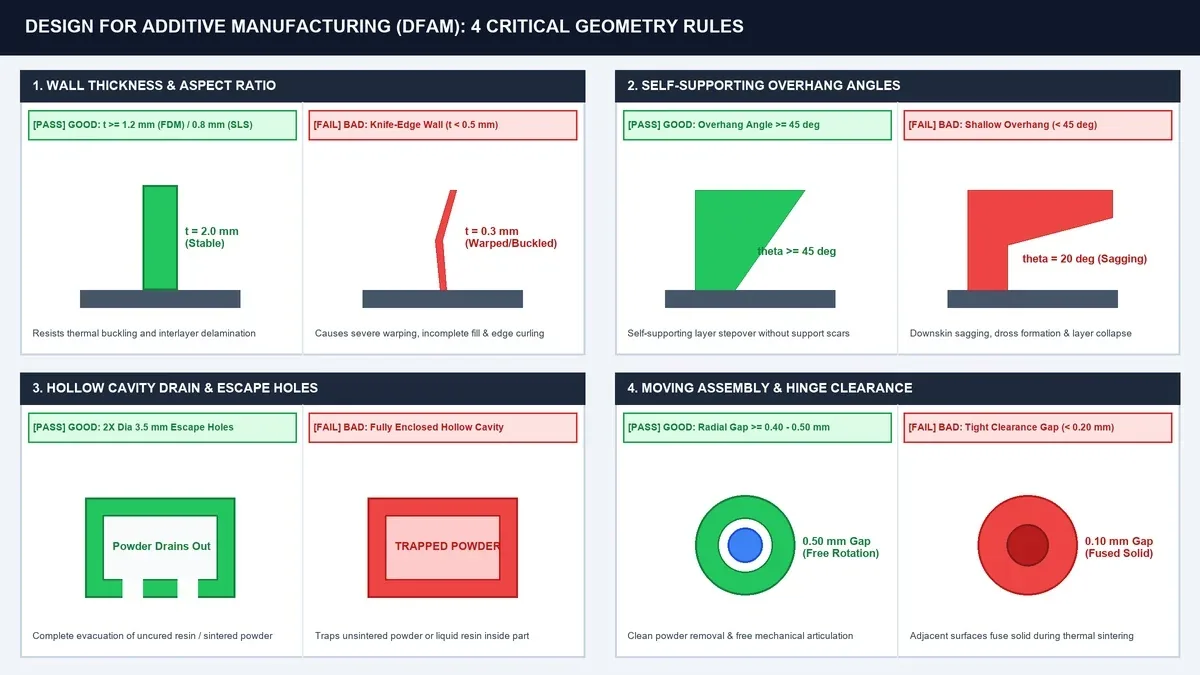
- Self-Supporting Overhangs: Keep overhang angles greater than 45° relative to the build plate. Features steeper than 45° print cleanly without supports in FDM and SLA; angles under 45° require sacrificial support structures that leave witness marks.
- Wall Thickness Standards: Maintain minimum wall thicknesses of 1.0 to 1.5 mm for structural durability. For large unsupported polymer panels, design ribs with 2.0 mm+ thickness to prevent post-cure thermal warping.
- Evacuation & Drain Ports: Hollow geometries in SLS, MJF, SLA, and DMLS must include at least two escape holes (∅ 3.0 mm minimum) to allow uncured liquid photopolymer or un-sintered loose powder to drain freely during post-processing.
- Assembly & Clearance Gaps: For print-in-place moving assemblies (such as hinges or ball joints), provide a minimum radial clearance gap of 0.4 mm to 0.5 mm to prevent neighboring feature fusing.
9. Comprehensive Engineering Comparison: The 7 AM Technologies
To help engineering teams select the optimal manufacturing method, the table below contrasts the technical capabilities of all seven ISO/ASTM 52900 process categories:
| Process Category | Common Technologies | Primary Materials | Min Layer Thickness | Standard Tolerance | Best Industrial Application |
|---|---|---|---|---|---|
| Powder Bed Fusion (PBF) | DMLS, SLM, SLS, EBM | Titanium, Inconel, 316L, Nylon PA12 | 20 – 50 μm | ±0.1 mm to ±0.2 mm | Aerospace brackets, functional snap-fits |
| Vat Photopolymerization | SLA, DLP, LCD, CLIP | Standard, Tough, Castable & Clear Resins | 25 – 100 μm | ±0.05 mm to ±0.1 mm | Optical prototypes, dental, master patterns |
| Material Extrusion | FDM, FFF, CFR | ABS, PC, PEEK, Carbon-Nylon | 100 – 300 μm | ±0.2 mm | Jigs, fixtures, rugged concept models |
| Material Jetting | PolyJet, NPJ | Rigid & Flexible Photopolymers | 16 – 32 μm | ±0.1 mm | Multi-color, multi-durometer models |
| Binder Jetting | Metal BJ, Sand BJ | Stainless Steel, Sand, Infiltration bronze | 50 – 100 μm | ±0.2 mm to ±0.5 mm | Sand molds, batch production of steel parts |
| Directed Energy Deposition | LMD, WAAM, Cold Spray | Titanium, Stainless Steel, Nickel alloys | 500 – 2000 μm | ±0.5 mm to ±1.5 mm | Turbine blade repair, huge aerospace shells |
| Sheet Lamination | LOM, UAM | Paper, Aluminum foil, Copper sheets | 100 – 150 μm | ±0.2 mm to ±0.3 mm | Embedded smart sensors, non-critical molds |
10. Metal AM vs. Polymer AM: Process Selection Matrix
When selecting among different 3D printing types, engineers must evaluate whether a polymer prototype suffices for fit checks or if end-use metallic properties are required. The comparison below illustrates performance metrics across our primary production lines:
| Manufacturing Process | Representative Material | Tensile Strength (MPa) | As-Built Surface Finish (Ra) | Ex-Factory Turnaround (As-Built / Finished) |
|---|---|---|---|---|
| DMLS / SLM | Titanium Ti-6Al-4V | 1050 – 1150 | 6.3 – 10 μm | 4 – 8 Business Days / 7 – 12 Business Days |
| SLS Nylon | Polyamide 12 (PA12) | 45 – 50 | 8.0 – 12.5 μm | 4 – 8 Business Days / 7 – 12 Business Days |
| SLA Photopolymer | Tough ABS-Like Resin | 40 – 65 | 0.8 – 2.5 μm | 4 – 8 Business Days / 7 – 12 Business Days |
| Industrial FDM | Polycarbonate (PC) | 55 – 70 | 12.5 – 25 μm | 4 – 8 Business Days / 7 – 12 Business Days |
11. Technical Engineering FAQ
Stereolithography (SLA) and Material Jetting provide the tightest tolerances among polymer systems, achieving ±0.10 mm to ±0.20 mm per 100 mm. In metal additive manufacturing, Direct Metal Laser Sintering (DMLS) holds tolerances of ±0.1 mm to ±0.2 mm. Furthermore, post-print CNC milling can refine critical datum faces down to ±0.010 mm.
Yes. Fully dense components produced via DMLS or SLM undergo post-build stress relief and hot isostatic pressing (HIP). As a result, their yield strength and tensile properties match or exceed traditional wrought alloys. Consequently, aerospace and medical device manufacturers routinely qualify DMLS parts for mission-critical applications.
3D printing delivers unmatched cost efficiency for low volumes, complex topological structures, and rapid design iterations. However, when batch quantities exceed several hundred units, or when pristine surface roughness (Ra below 0.8 micrometers) is required across simple geometric profiles, CNC machining or rapid tooling injection molding becomes more economical.
Accelerate Hardware Validation with Industrial 3D Printing & Hybrid CNC
Bridge additive design freedom with precision CNC datum finishing and polyurethane vacuum casting. Upload your 3D CAD assemblies (STEP/IGES/STL) to evaluate material selection, functional tolerances, and batch unit economics.
Request an Additive & Prototyping DFM Analysis