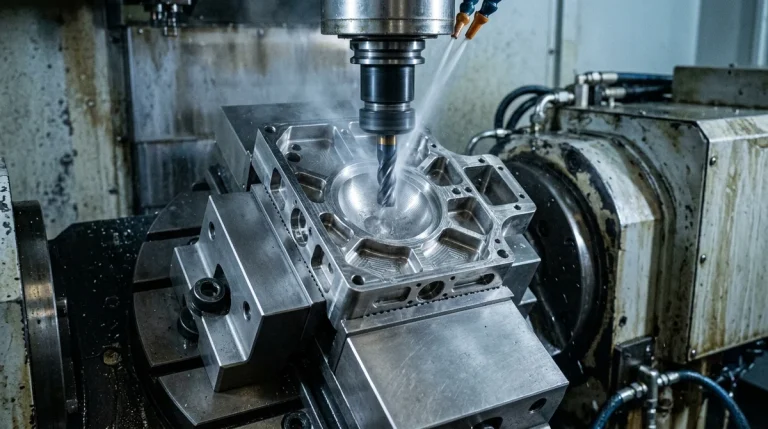

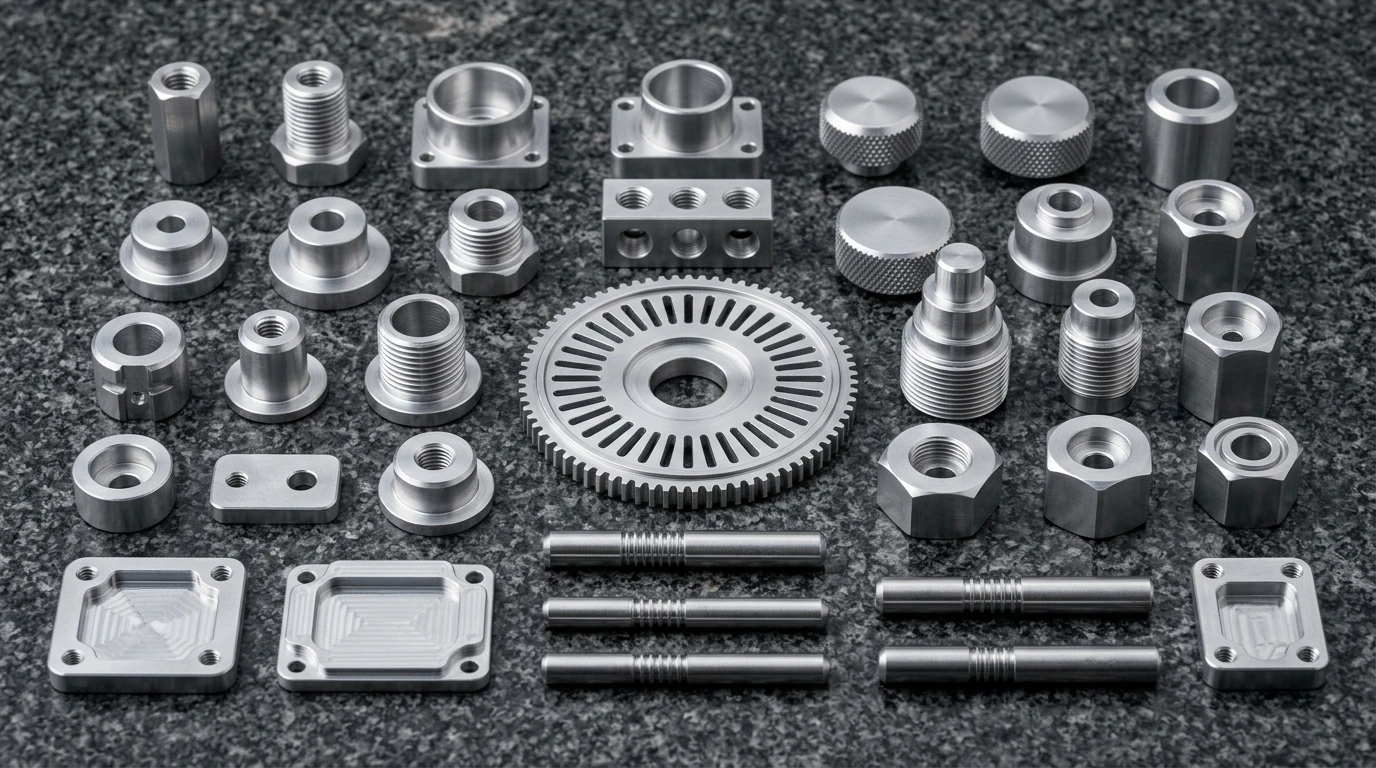
Aluminum is one of the most popular metals for CNC machining today. Engineers prize it for its low weight, high strength, and great thermal traits.
However, the machinability of aluminum changes a lot between different grades. Pure aluminum is gummy and sticks to cutters. In contrast, heat-treated alloys cut crisp and clean at high speeds.
Therefore, knowing how to boost aluminum machinability is vital. It cuts your cycle times, saves tool life, and yields mirror-like surface finishes.
At AS Prototypes, we mill and turn complex aluminum parts every day. In this guide, we share proven shop tips to optimize your CNC machining results.
What Defines the Machinability of Aluminum?
Machinability measures how easily a metal cuts without damaging the tool. For aluminum, four key factors decide this score.
First, cutting force plays a major role. Alloys that need low cutting force save spindle power and reduce tool wear.
Second, chip formation is critical. Clean chips curl up and snap off with ease. In contrast, long gummy chips wrap around spinning cutters and scratch parts.
Third, built-up edge (BUE) affects finish quality. Soft aluminum tends to weld onto hot tool tips. This creates rough burrs on fine edges.
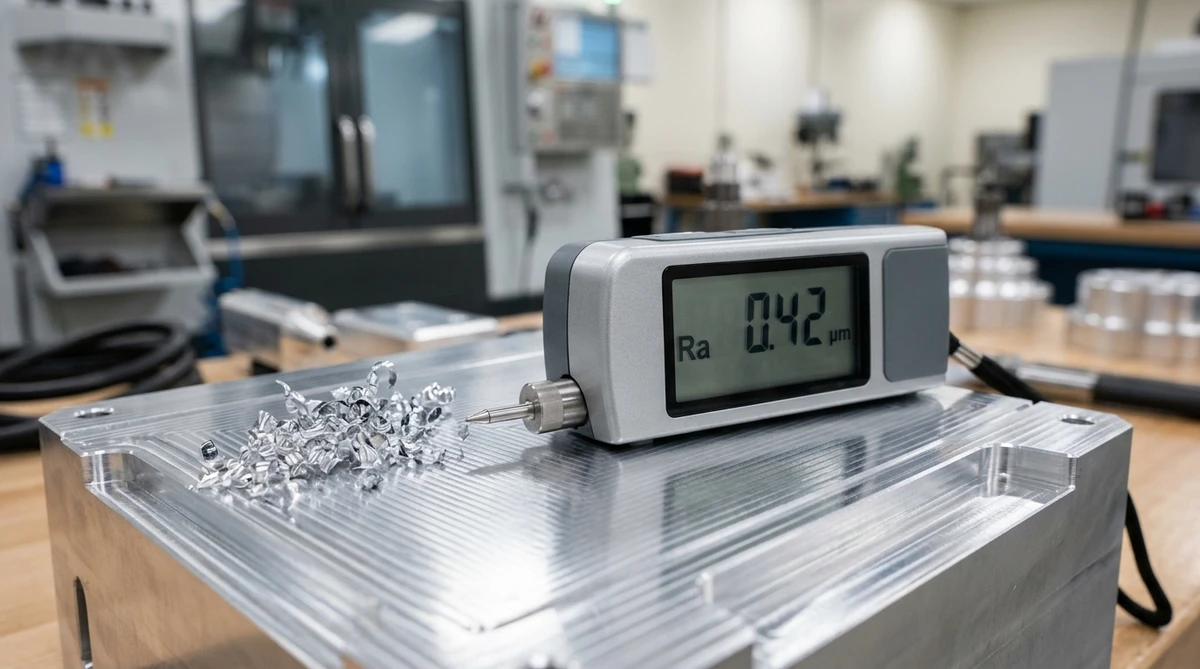
Finally, surface finish and tool life complete the test. Good machinability lets shops hit ISO 2768-mK tolerances with minimal tool changes.
Best Aluminum Alloys for CNC Machining
Not all aluminum cuts the same way. The alloy series sets the mechanical properties and cutting behavior.
1. 6061-T6 Aluminum
6061-T6 is the workhorse of CNC machine shops. It blends silicon and magnesium for balanced strength and corrosion resistance.
In addition, it chips cleanly and takes anodizing very well. It is the best all-around pick for brackets, heat sinks, and custom housings.
2. 7075-T6 Aluminum
7075-T6 uses zinc as its primary alloy element. It delivers yield strength comparable to many structural steels.
Because it is hard and stiff, it machines with short, brittle chips. This makes it ideal for deep pockets and thin walls. Aerospace and robotics rely on it heavily.
3. 2024-T3 Aluminum
2024-T3 features copper as its main alloying metal. It offers extreme fatigue strength for aircraft fittings and tension members.
However, it has lower corrosion resistance than 6061. Therefore, it usually requires hard anodizing or protective primer coats after milling.
4. MIC-6 Cast Tooling Plate
MIC-6 is a continuous cast aluminum plate known for extreme dimensional stability. It is stress-relieved to stop warpage during heavy face milling.
Consequently, fixture makers pick MIC-6 for large vacuum plates, robot bases, and metrology nests.
Machinability Comparison of Common Aluminum Grades
To help you pick the right grade, compare the mechanical traits and machinability ratings in the table below.
| Aluminum Alloy | Temper State | Machinability Index (%) | Yield Strength (MPa) | Best Shop Application |
|---|---|---|---|---|
| 6061 | T6 | 90% | 276 MPa | General CNC parts, frames, and colored anodized brackets. |
| 7075 | T6 | 95% | 503 MPa | Aerospace frames, race car hubs, and high-stress gears. |
| 2024 | T3 / T4 | 85% | 324 MPa | Aircraft wing ribs, tension links, and structural shear pins. |
| 5052 | H32 | 60% | 193 MPa | Sheet metal bending, marine panels, and fuel tanks. |
| MIC-6 | Cast / Aged | 90% | 105 MPa | Ultra-flat tooling plates and precision CMM fixture nests. |
How to Optimize Cutting Tools and Coolant
Tool choice makes a massive impact on your cutting speeds and surface quality.
1. Use Sharp Polished Flutes
Always pick 2-flute or 3-flute end mills with polished chip gullets. The mirror polish prevents hot aluminum chips from welding to the cutter flutes.
Furthermore, large flute gaps clear chips rapidly out of deep pockets. This prevents recutting chips, which dulls tool edges and ruins finishes.
2. Apply Advanced DLC Tool Coatings
Uncoated carbide works well, but diamond-like carbon (DLC) coatings work even better. DLC coatings provide a slick surface with an ultra-low friction coefficient.
As a result, chips slide right off without sticking. This doubles tool life and enables dry high-speed machining when needed.
3. Maintain Flood Coolant Pressure
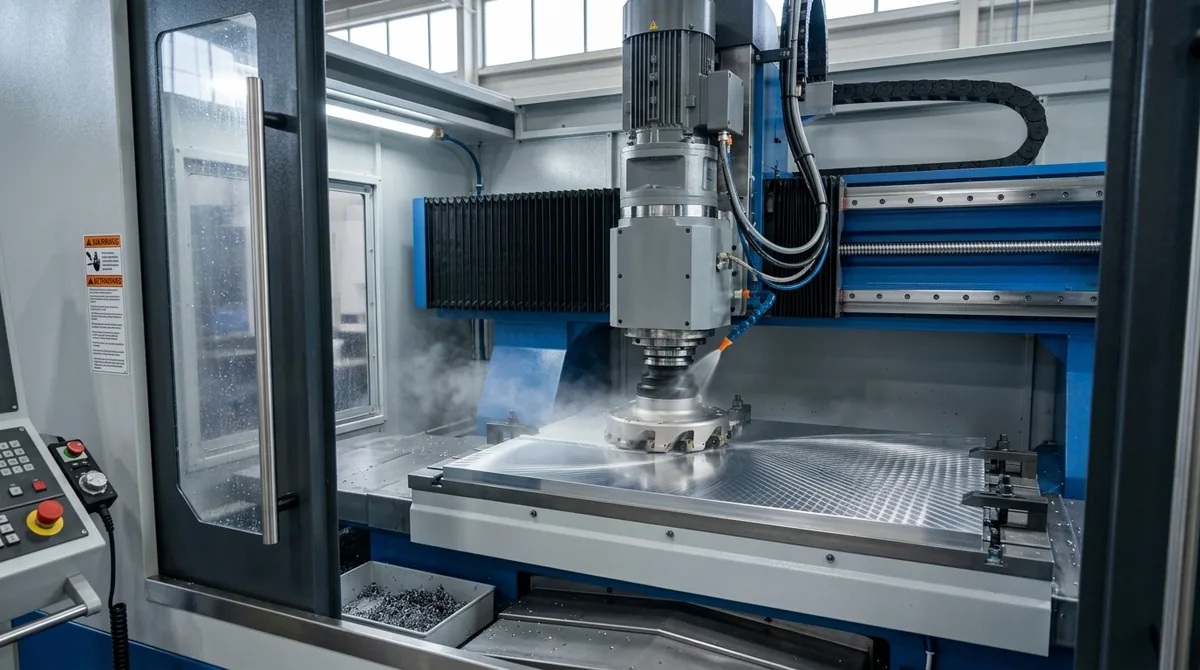
Flood coolant serves two vital roles. First, it cools the cutting zone and lubricates the shear plane.
Second, high-pressure coolant flushes chips away from the tool path. Without good coolant flow, heat builds up fast and causes aluminum to smear. For complex aerospace bulkheads, our multi-axis centers also use 5-axis tool orientation to guarantee clean chip escape.
Speed and Feed Guidelines for High-Speed Milling
To maximize material removal rates, reference our shop cutting parameters below.
| Operation Type | Tooling Style | Cutting Speed Vc (m/min) | Feed per Tooth fz (mm) | Coolant Method |
|---|---|---|---|---|
| Rough Pocketing | 3-Flute Carbide Rougher | 400 – 800 m/min | 0.10 – 0.25 mm | High-pressure flood coolant (20 bar). |
| Profile Finishing | 3-Flute Polished End Mill | 600 – 1,200 m/min | 0.04 – 0.08 mm | Flood coolant or mist lubrication. |
| Face Milling | Indexable Face Mill (PCD Inserts) | 1,000 – 2,500 m/min | 0.12 – 0.20 mm | Dry with air blast or light mist. |
| Deep Hole Drilling | Through-Coolant Carbide Drill | 150 – 300 m/min | 0.08 – 0.18 mm | Through-spindle coolant (40 bar). |
Practical Design Tips to Boost Machinability
Product designers can cut machining costs by adopting these smart design rules.
- Use Generous Internal Radii: Keep corner radii at least one-third of the pocket depth to avoid tool chatter.
- Limit Pocket Depth Ratios: Keep deep pockets under 4 times the tool diameter for fast roughing passes.
- Standardize Hole Diameters: Use common drill sizes to reduce tool changes during multi-axis operations.
- Maintain Uniform Wall Thickness: Design stiff ribs to prevent vibration when cutting thin structural walls.
7075-T6 and 6061-T6 offer the best machinability. Their high temper hardness forms short, brittle chips that clear cutters quickly without gummy buildup.
Pure or soft aluminum has low yield strength and high ductility. Heat from cutting causes the soft metal to weld onto tool tips, creating a rough built-up edge.
Sharp carbide end mills run best at 400 to 800 meters per minute on 6061-T6. Always use steady flood coolant to clear chips.
Get Precision CNC Machined Aluminum Parts Fast
AS Prototypes delivers high-speed CNC milling and turning for prototypes and full production batches. Upload your 3D CAD files today for an instant DFM review and fast quote.