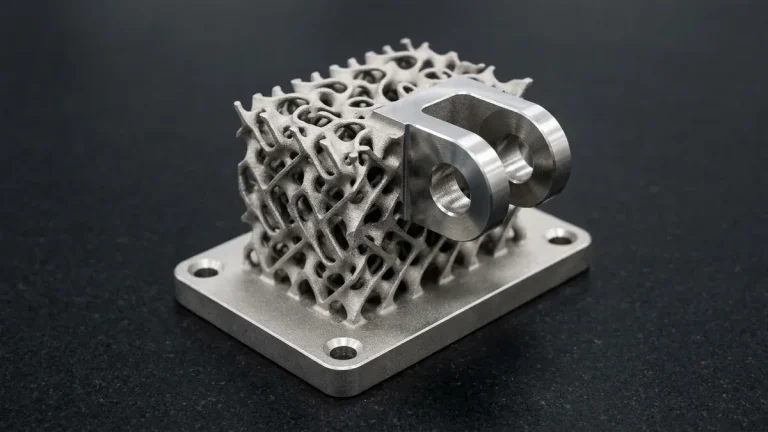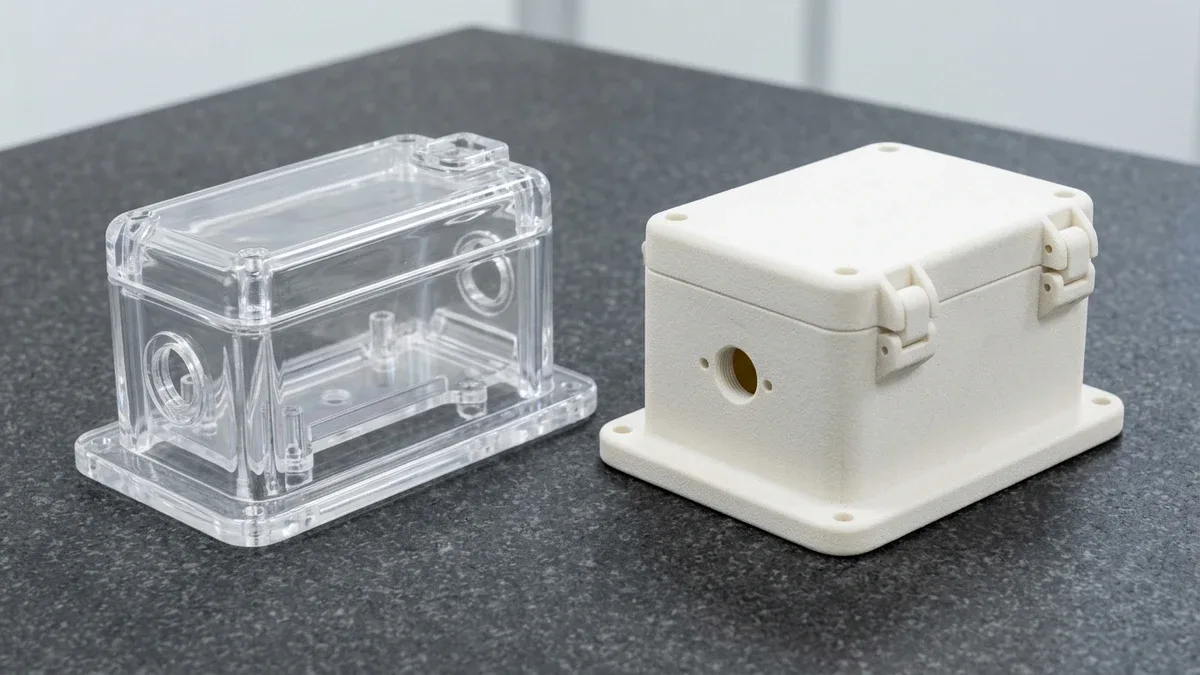
Additive manufacturing has revolutionized product development workflows, compressing design cycles from months into days. However, selecting the incorrect 3D printing technology during the prototyping phase introduces severe validation risks: functional snap-arms snapping unexpectedly, optical light guides clouding under heat, or thin walls warping during environmental testing.
Among polymer additive systems, Stereolithography (SLA) and Selective Laser Sintering (SLS) stand as the two dominant industrial standards. While both build parts additively layer-by-layer using focused laser energy, their underlying polymer chemistry, laser physics, mechanical load capacities, and post-processing requirements are completely distinct.
At AS Prototypes, our industrial additive manufacturing facility operates large-scale SLA resin vats alongside high-capacity SLS nylon powder beds, backed by automated post-curing ovens, chemical vapor smoothing chambers, and precision CNC finishing centers. In this comprehensive technical guide, we evaluate photopolymerization kinetics against laser sintering thermodynamics, compare mechanical and thermal properties across genuine engineering materials, analyze 3D nesting economics, and provide clear engineering rules to select the ideal process for your project.
- 1. Physical Principles: Photopolymerization vs Powder Sintering
- 2. Comprehensive Technical Specifications: SLA vs SLS
- 3. Mechanical Ductility and Environmental Aging Mechanics
- 4. Support Structure Mechanics vs Support-Free Powder Bed Nesting
- 5. Material Selection Guide: SLA Resins vs SLS Powders
- 6. Post-Processing Workflows and Surface Refinement
- 7. Design for Additive Manufacturing (DFAM) Selection Rules
- 8. Technical Engineering FAQ
1. Physical Principles: Photopolymerization vs Powder Sintering
Understanding the molecular mechanisms of each process explains their divergent mechanical and cosmetic characteristics.
1.1 Stereolithography (SLA): Jacobs Photopolymerization Kinetics
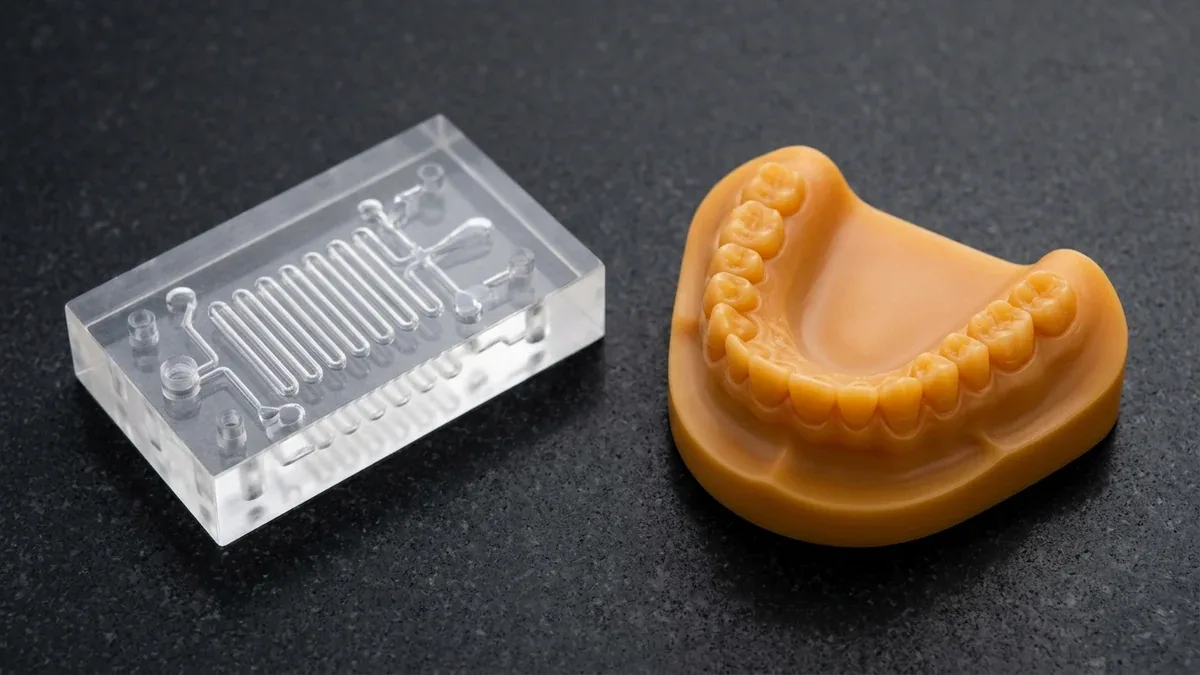
Stereolithography builds parts by selectively curing liquid photocurable monomer resins inside a vat using a solid-state ultraviolet laser (λ = 355 nm). The laser beam traces cross-sections across the resin surface, exciting photoinitiators that trigger free-radical or cationic chain polymerization, crosslinking liquid oligomers into a rigid solid thermoset polymer.
The cure depth (Cd) of the photopolymerized layer is modeled by the classic Jacobs Working Curve Equation:
Where Dp is the resin penetration depth at the 355 nm wavelength (typically 0.10 to 0.15 mm), Emax is the peak laser exposure energy delivered to the resin surface (mJ/cm2), and Ec is the critical gel-point exposure energy required for liquid-to-solid phase transition. Because laser spot size can be focused down to 0.075 mm (75 μm), SLA achieves unmatched micro-feature precision and surface smoothness.
1.2 Selective Laser Sintering (SLS): Thermal Powder Coalescence
Selective Laser Sintering operates in a powder-bed format without liquid resin. Fine, semi-crystalline thermoplastic powder particles (typically 45 to 60 μm diameter) are preheated inside an inert nitrogen chamber to just below their melting temperature (Tmelt, approx. 175°C for Nylon PA12). A high-power CO2 or fiber laser scans the powder bed, adding just enough localized thermal energy to melt and coalesce particles together into solid geometry.
The energy delivered to the powder bed is quantified by the Andrew Laser Energy Density equation (ED):
And volumetric energy density (Evolumetric):
Where Plaser is laser beam power (W), vscan is beam scanning velocity (mm/s), hhatch is hatch line spacing (mm), and tlayer is layer thickness (typically 0.10 to 0.12 mm). Maintaining tight closed-loop control over Evolumetric ensures complete inter-particle fusion without inducing polymer chain thermal degradation or smoking.
1.3 Laser Beam Gaussian Optics and Energy Distribution
In stereolithography, the ultraviolet laser beam operates in the fundamental transverse electromagnetic mode (TEM00), producing a Gaussian spatial intensity distribution across the resin surface:
Where I0 is peak optical intensity at the beam centerline, r is radial distance from the optical axis (mm), and w0 is laser waist radius (typically 35 to 50 μm). As dual-axis galvanometer mirrors sweep the beam at linear velocities up to 10 m/s, the cured photopolymer profile forms a parabolic cross-sectional “cure bullet”. Controlling beam overlap and galvanometer jump delays eliminates internal un-cured liquid traps and guarantees uniform isotropic green-state density.
2. Comprehensive Technical Specifications: SLA vs SLS
The table below provides a side-by-side engineering comparison of dimensional tolerances, mechanical limits, surface characteristics, and operational parameters.
| Technical Parameter | Stereolithography (SLA) | Selective Laser Sintering (SLS) |
|---|---|---|
| Raw Material State | Liquid photocurable thermoset resin | Fine dry thermoplastic powder (PA12 / PA11) |
| Standard Dimensional Tolerance | ±0.10 mm or ±0.15% (Tight fit) | ±0.20 mm or ±0.25% (Thermal shrink) |
| Minimum Wall Thickness | 0.6 mm (Supported) / 0.8 mm (Free) | 1.0 mm (Supported) / 1.5 mm (Free) |
| Minimum Feature Size | 0.15 mm (Micro-text, fine ribs) | 0.60 mm (Embossed text / pins) |
| As-Printed Surface Roughness | Ra 0.4 to 0.8 μm (Near injection smooth) | Ra 4.0 to 8.0 μm (Granular matte texture) |
| Tensile Strength (UTS) | 35 to 55 MPa (Standard) / Up to 80 MPa (Ceramic) | 45 to 52 MPa (Genuine Nylon 12) |
| Elongation at Break | 6% to 15% (Brittle thermoset behavior) | 18% to 25% (Ductile thermoplastic behavior) |
| Heat Deflection Temp (HDT @ 0.45 MPa) | 45°C to 65°C (Standard) / 230°C (Ceramic Resin) | 160°C to 175°C (PA12 & PA12-GF) |
| Support Structures Required | Yes (Lattice supports on overhangs < 45°) | No (100% self-supporting powder bed) |
| 3D Volumetric Nesting | Limited (Parts must anchor to build plate) | Full 3D stacking across X, Y, and Z axes |
| Ex-Factory Turnaround | 4 to 8 Business Days (As-Printed) / 7 to 12 Days (Finished) | 4 to 8 Business Days (As-Printed) / 7 to 12 Days (Finished) |
3. Mechanical Ductility and Environmental Aging Mechanics
The physical divergence between thermoset resins and true thermoplastics governs how parts perform under dynamic mechanical stress and long-term environmental exposure.
3.1 Elongation at Break and Impact Dynamics
SLA materials, being photopolymerized thermosets, feature highly crosslinked molecular networks. While this creates exceptional surface hardness and compressive rigidity, it results in brittle tensile failure under dynamic shock loads. Typical standard SLA resins exhibit elongation at break values below 12%. Subjecting an SLA cantilever snap-fit arm or living hinge to repeated deflection causes rapid micro-crack propagation and catastrophic brittle fracture.
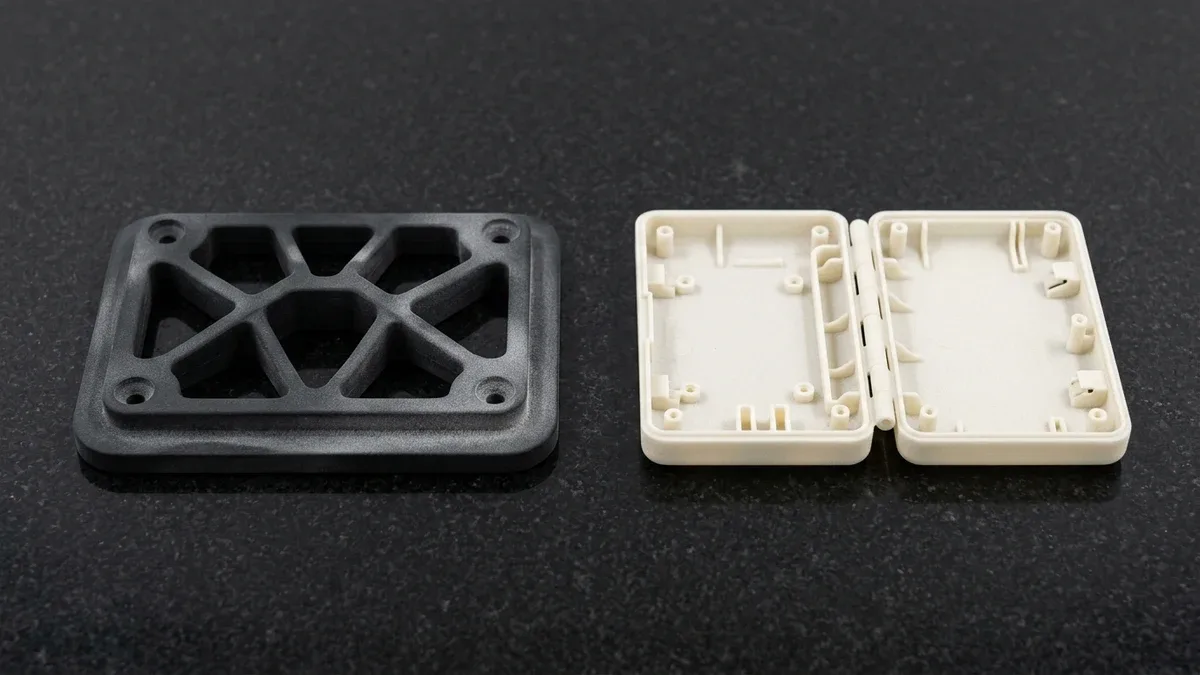
In contrast, SLS uses authentic semi-crystalline engineering polymers—primarily Polyamide 12 (Nylon 12). SLS PA12 features long entangled polymer chains that yield plastically under stress, achieving an elongation at break between 18% and 25% and high Izod notched impact toughness (4.5 to 6.0 kJ/m2). SLS snap-fits, living hinges, threaded inserts, and press-fit pins can be cycled hundreds of times without mechanical fatigue failure.
3.2 Outdoor UV Stability and Hydrothermal Aging
When selecting a process for outdoor enclosures or automotive under-hood components, environmental degradation mechanisms must be considered:
- SLA UV Sensitivity: Photopolymers contain residual photoinitiators. When exposed to outdoor sunlight (UV radiation), the material undergoes continuous post-polymerization crosslinking. Over weeks of UV exposure, unpainted SLA components become increasingly brittle, darken in color, and shift dimensionally. SLA parts intended for outdoor use require UV-blocking polyurethane clear-coats or opaque automotive-grade paint.
- SLS Chemical and Thermal Endurance: Sintered PA12 nylon is chemically inert to automotive fuels, greases, synthetic hydraulic oils, and alkalis. It withstands continuous service temperatures of 160°C (up to 175°C for glass-filled PA12-GF). When sealed via automated chemical vapor smoothing, SLS nylon parts provide years of weather-proof outdoor service without mechanical embrittlement.
4. Support Structure Mechanics vs Support-Free Powder Bed Nesting
One of the most consequential engineering distinctions between SLA and SLS is the requirement for sacrificial support structures.
4.1 SLA Support Structure Management
Because SLA builds components inside a liquid resin vat, gravity and viscous peel forces during platform repositioning require physical support structures. Overhanging geometry with an angle below 45 degrees relative to the horizontal build plane must be reinforced with fine scaffolding lattice structures.
While software automatically generates these supports, removing them introduces labor-intensive post-processing. Technicians must manually clip supports using flush cutters and hand-sand support contact points (“witness marks”) with 400 to 800 grit abrasive paper. If supports are placed on high-tolerance mating faces, cosmetic texture variations or dimensional dips can occur.
4.2 SLS Support-Free Powder Bed Advantage
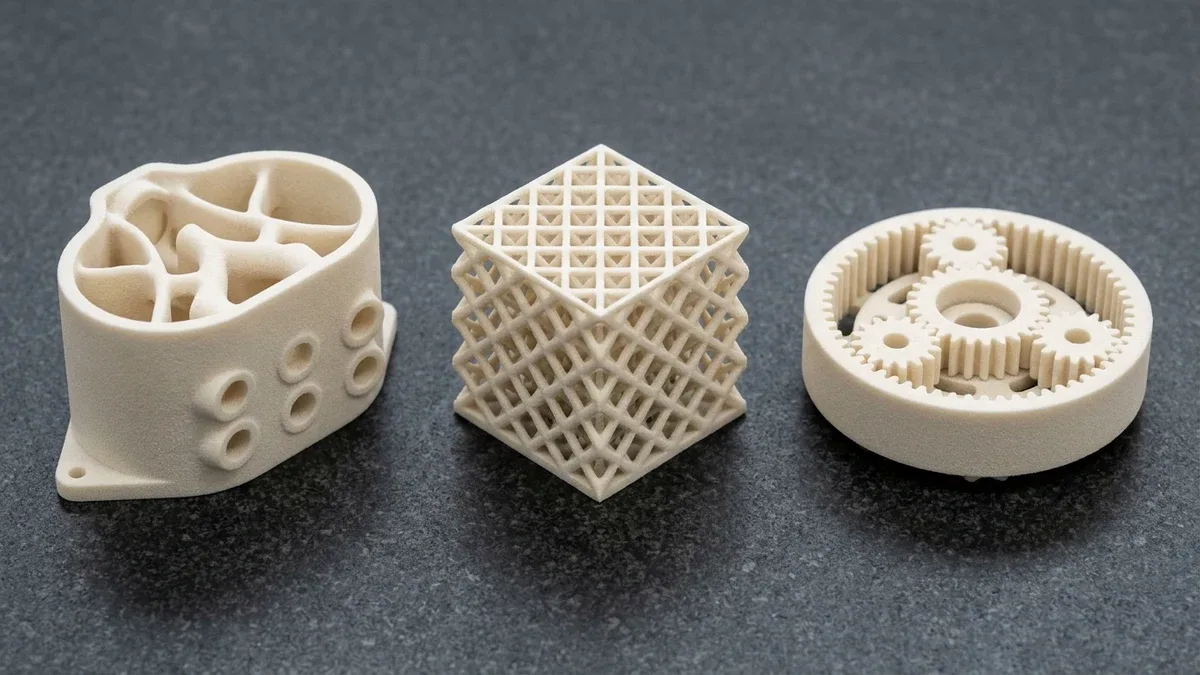
Selective Laser Sintering requires zero mechanical support structures. The unsintered polymer powder packed around the parts provides 100% natural, continuous geometric support throughout the entire build cycle. This physical freedom unlocks three transformative engineering advantages:
- Organic Conformal Channels: SLS can manufacture curved internal fluid channels, gyroid heat exchanger lattices, and hollow weight-reduction chambers that are impossible to clean or support in SLA or CNC milling.
- Print-in-Place Interlocking Mechanisms: Fully assembled ball joints, multi-link hinges, and planetary gear sets can be printed pre-assembled in a single build cycle, ready to function immediately once unfused powder is blown out.
- 3D Volumetric Chamber Nesting: Parts can be stacked across all three spatial dimensions throughout the 300 × 300 × 600 mm build chamber. Stacking 50 to 500 parts per run drives down unit machine amortization costs dramatically.
5. Material Selection Guide: SLA Resins vs SLS Powders
Selecting the right formulation ensures the printed component fulfills its intended mechanical and thermal role.
| Material Grade | Polymer Family | Tensile Modulus | Heat Deflection (HDT) | Ideal Engineering Application |
|---|---|---|---|---|
| SLA Standard White / Gray | Methacrylate Photopolymer | 2.5 to 2.8 GPa | 55°C | Cosmetic show models, visual fit checks |
| SLA Optical Clear Resin | Acrylic Photopolymer | 2.4 to 2.7 GPa | 50°C | Light pipes, fluid diagnostic sight glasses |
| SLA High-Temp Ceramic | Ceramic-Filled Composite | 8.0 to 10.0 GPa | > 230°C | Wind tunnel testing, rapid injection mold inserts |
| SLS Nylon PA12 | Polyamide 12 Thermoplastic | 1.7 to 1.9 GPa | 160°C | Functional snap-fit enclosures, drone brackets |
| SLS Glass-Filled PA12-GF | 30% Glass Bead Reinforced PA12 | 3.2 to 3.8 GPa | 175°C | High-stiffness jigs, automotive intake manifolds |
| SLS Flexible TPU | Thermoplastic Polyurethane | Shore 88A to 92A | 80°C | Gaskets, protective bumpers, flexible footwear |
6. Post-Processing Workflows and Surface Refinement
The post-processing sequence determines whether an additive component looks like a raw 3D print or a production-grade injection molded part.
6.1 SLA Post-Processing Sequence
- Solvent Washing: Parts are submerged in automated isopropyl alcohol (IPA) or tripropylene glycol monomethyl ether (TPM) ultrasonic agitation tanks to dissolve uncured liquid resin from crevices.
- Support Detachment: Hand technicians clip support struts and sand witness nodes smooth with fine-grit silicon carbide paper.
- UV & Thermal Post-Curing: Components enter calibrated UV curing chambers (operating at 405 nm and 60°C) for 30 to 60 minutes. This final exposure completes polymer crosslinking, elevating tensile strength and heat deflection temperature to maximum datasheet values.
- Optical Wet Sanding & Clear Coating: For transparent parts, technicians execute progressive wet-sanding from 800 to 2000 grit, followed by an acrylic clear-coat spray to yield water-clear optical transparency.
6.2 SLS Post-Processing Sequence
- Automated De-Caking: Sintered build cakes cool inside the chamber before moving to breakout stations where high-pressure oscillating air knives blow away loose unfused powder.
- Media Bead Blasting: Components undergo fine glass bead or aluminum oxide blasting to remove surface-adhering powder grains, establishing a clean, uniform satin texture.
- Chemical Vapor Smoothing: In automated vapor chambers, vaporized solvent condenses onto the PA12 surfaces, liquifying the microscopic outer 10-micron skin. Surface tension pulls micro-peaks into valleys before the solvent is fully extracted. This slashes surface roughness from Ra 6.0 μm down to Ra ≤ 1.0 μm, seals surface porosity for complete water-tightness, and boosts elongation at break.
- High-Temperature Black Dyeing: Parts are immersed in pressurized dye tanks to achieve deep, scratch-resistant matte black coloration.
6.3 Metallic Electroplating and Secondary Finishing on SLA
While SLA parts are intrinsically polymer thermosets, their glass-smooth surface finish makes them prime candidates for functional metallic electroplating. By applying an electroless nickel strike followed by acid copper leveling and final decorative chrome or hard nickel deposition (20 to 50 μm thickness), engineers transform lightweight resin components into metallized prototypes with high surface conductivity, electromagnetic interference (EMI) shielding, and enhanced flexural stiffness.
7. Design for Additive Manufacturing (DFAM) Selection Rules
When finalizing CAD designs, adhere to the following core engineering guidelines:
Rule 1: Choose SLA for Polyurethane Vacuum Casting Masters
If your project calls for 20 to 100 prototype units in authentic production elastomers or flame-retardant resins via vacuum casting services, always print master patterns in SLA. The glass-smooth surface (Ra ≤ 0.4 μm) transfers directly into silicone RTV molds, eliminating days of labor-intensive mold cavity polishing.
Rule 2: Choose SLS for Functional Snap-Fits and Living Hinges
Never rely on standard SLA resins for functional snap-fit clips. Sintered PA12 nylon provides the requisite 20% elongation at break needed to deflect cantilever arms without yielding or cracking.
Rule 3: Design Generous Drain Ports for Hollow SLS Geometry
To reduce part weight and powder consumption in SLS, hollow out thick bosses. However, you must incorporate at least two drain holes (≥ 3.5 mm diameter) at opposite ends of the cavity to allow trapped powder to escape during automated air blasting.
Rule 4: Avoid Large Flat Horizontal Planes in SLA
Large flat planes oriented parallel to the SLA vat surface experience massive suction peel forces when separating from the vat film. Re-orient flat planes at a 30 to 45 degree tilt angle on build supports to minimize cross-sectional peel area and prevent layer separation.
8. Technical Engineering FAQ
SLS is significantly more durable and functional for mechanical applications. While high-temperature ceramic SLA resins achieve higher tensile modulus, SLS PA12 nylon delivers authentic thermoplastic ductility (18% to 25% elongation at break), high impact toughness, and resistance to repeated fatigue cycling.
SLA uses focused UV lasers and liquid resins to produce exceptionally smooth surfaces (Ra 0.4 to 0.8 microns) with invisible layer lines. It can be wet-sanded and clear-coated to achieve optical transparency, and serves as the industry standard master pattern for silicone vacuum casting molds.
No. SLS is completely self-supporting because parts are suspended within the compacted, un-sintered powder bed during printing. This allows complex geometries, internal fluid channels, print-in-place moving hinges, and 3D volumetric stacking throughout the chamber.
Chemical vapor smoothing uses vaporized solvent in a vacuum chamber to melt and reflow the outer 10-micron surface of SLS PA12 parts. It reduces surface roughness from Ra 6.0 down to Ra 1.0 micron, seals surface porosity for water-tightness, and increases impact strength.
Engineering DFM reviews and quotes are completed within 24 hours. Standard as-printed SLA and SLS prototypes achieve ex-factory release in 4 to 8 business days, while parts requiring optical clear-coating, chemical vapor smoothing, or custom painting/plating require 7 to 12 business days ex-factory (excluding 3 to 5 days international air freight).
Accelerate Hardware Validation with Industrial 3D Printing & Hybrid CNC
Bridge additive design freedom with precision CNC datum finishing and polyurethane vacuum casting. Upload your 3D CAD assemblies (STEP/IGES/STL) to evaluate material selection, functional tolerances, and batch unit economics.
Request an Additive & Prototyping DFM Analysis