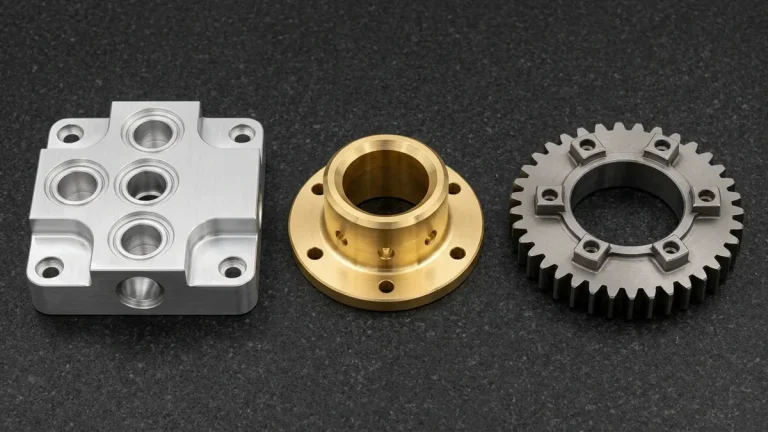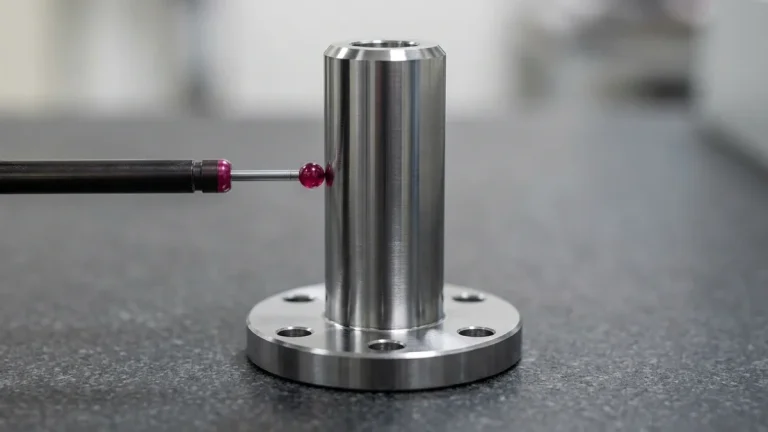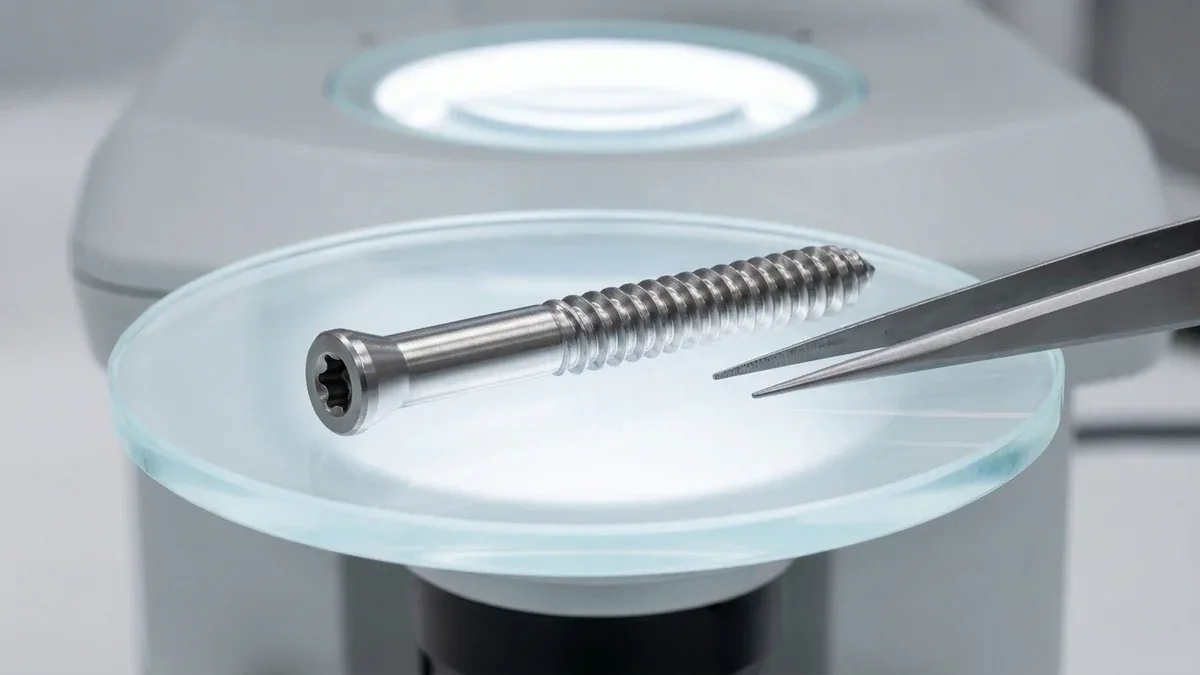
In the medical device and surgical instrumentation sector, precision manufacturing is inseparable from patient safety, clinical efficacy, and regulatory approval. Whether machining class III implantable orthopedic reconstruction plates, complex cardiovascular catheters, endoscopic articulation joints, or diagnostic fluidic manifolds, medical components demand uncompromising dimensional tolerances (±0.010 mm on milled housings and ±0.005 mm on Swiss-turned pins or Wire EDM slots), verified biocompatible metallurgy, mirror-polished micro-finishes, and full lot traceability. In precision manufacturing, mastering custom machining medical parts ensures repeatable dimensional stability and predictable production scaling.
At AS Prototypes, with more than a decade of precision micro-machining, Swiss turning, and rapid prototyping leadership, we partner with medical device OEMs, surgical robotics pioneers, and biotech research institutions worldwide. Guided by strict quality control methodologies, this engineering guide examines the core principles of custom machining medical parts—from biocompatible alloy selection and multi-axis Swiss turning to multi-stage ultrasonic cleaning, ASTM A967 passivation, and climate-controlled metrology.
- 1. Why Custom CNC Machining is Essential in Medical Device Development
- 2. Biocompatible Materials Matrix for Medical CNC Machining
- 3. Advanced CNC Machining Processes for Medical Components
- 4. Critical Post-Processing, Ultrasonic Cleaning & Metrology Validation
- 5. AS Prototypes Medical Prototyping Capabilities
- 6. Technical Engineering FAQ
1. Why Custom CNC Machining is Essential in Medical Device Development
While mass-market consumer electronics rely heavily on high-volume plastic injection molding or casting, medical product development depends fundamentally on custom CNC machining for several vital reasons:
- Patient-Specific Customization & Anatomical Fit: Orthopedic reconstruction, cranial implants, and spinal fusion devices increasingly demand custom contours tailored to individual patient anatomy derived from CT/MRI DICOM datasets. CNC machining carves these complex, non-standard shapes directly from solid titanium or PEEK blocks without custom tooling delays.
- Accelerated FDA 510(k) & CE-MDR Clinical Validation: Bringing a medical device to market requires exhaustive bench testing, cadaver lab evaluations, and clinical trials. CNC prototyping delivers low-volume functional runs (10 to 500 units) crafted from identical implant-grade alloys, allowing teams to complete biocompatibility, tensile fatigue, and sterilization validation months before investing in production molds.
- Complex Monolithic Functional Integration: Medical engineers can consolidate multi-piece assemblies into single, leak-proof, monolithic components featuring internal fluidic micro-channels, reducing potential bacterial entrapment seams and assembly labor.
- Zero-Defect Micro-Scale Precision: Minimally invasive surgical (MIS) tools and endoscopic instruments feature micro-machined gears, trocars, and hinges requiring dimensional tolerances down to ±0.005 mm (±0.0002 in.) with 100% burr-free edge radii under 50× optical magnification.
2. Biocompatible Materials Matrix for Medical CNC Machining
Selecting the appropriate verified material is essential for clinical safety. The table below details the primary medical-grade metals and engineering polymers machined at AS Prototypes:
| Material Grade | Specification Standard | Tensile Strength [MPa] | Sterilization Compatibility | Biocompatibility Classification | Key Medical Applications |
|---|---|---|---|---|---|
| Ti-6Al-4V ELI (Grade 23) | ASTM F136 / ISO 5832-3 | 860 – 930 | Autoclave, EtO, Gamma, E-Beam | Permanent Implant (ISO 10993) | Orthopedic bone plates, pedicle screws, dental implants, trauma fixation |
| 316L VM (Vacuum Melt) | ASTM F138 / ISO 5832-1 | 580 – 800 | Autoclave, EtO, Chemical Vapor | Temporary Implant / Surgical Contact | Surgical scalpels, laparoscopic graspers, orthopedic drill bits, cannula tubing |
| PEEK-OPTIMA (Natural) | ASTM F2026 / ISO 10993 | 100 – 130 | Autoclave (reusable), EtO, Gamma | Permanent Implant (Radiolucent) | Spinal fusion cages, craniomaxillofacial implants, pacemakers, heart valve trials |
| Cobalt-Chromium (CoCrMo) | ASTM F1537 / ISO 5832-12 | 1170 – 1450 | Autoclave, Gamma, Plasma | Permanent High-Wear Implant | Artificial knee femoral components, hip joint balls, spinal rods, dental bridges |
| 6061-T6 (Medical Grade) | ASTM B221 (RoHS/REACH) | 310 | EtO, Chemical Disinfectants | Non-Implantable Device Structural | Ventilator manifolds, MRI mobile carts, ultrasound chassis, surgical robotic arms |
3. Advanced CNC Machining Processes for Medical Components
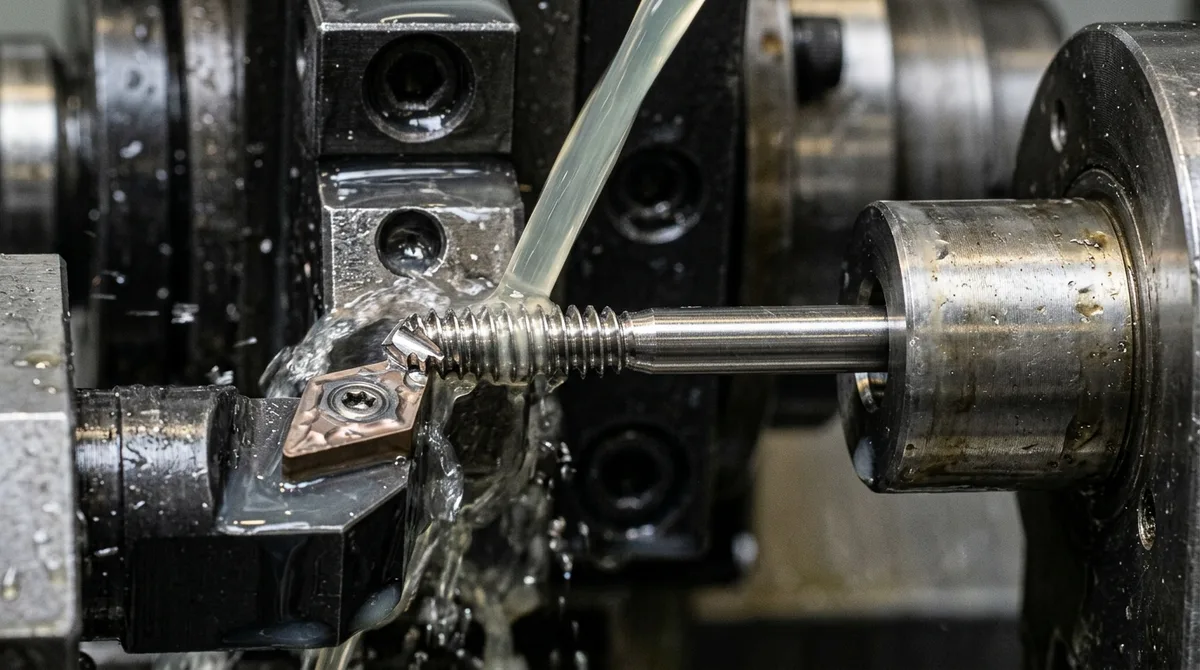
Fabricating micro-scale medical hardware requires specialized multi-axis machine configurations designed to mitigate cutting deflection and eliminate secondary operations:
1. Swiss-Type CNC Turning (Sliding Headstock)
For long, slender parts such as bone screws, guide wires, and dental implant posts with length-to-diameter ratios exceeding 10:1, conventional CNC lathes cause substantial part deflection. Swiss-type CNC lathes feed bar stock through a precision guide bushing directly adjacent to the cutting tool. This zero-deflection setup maintains exceptional concentricity down to ±0.005 mm (±0.0002 in) and enables single-pass thread whirling of specialized dual-lead cortical bone threads.
2. 5-Axis Micro-Milling
Intricate anatomical bone plates and polyaxial screw heads require complex 3D contouring and compound-angle fastener holes. Simultaneous 5-axis machining allows the cutter to access all five sides in a single setup, guaranteeing precise datum relationships between the screw lock threads and the contoured plate surface.
3. Wire EDM for Micro-Features
Electrical Discharge Machining (EDM) is vital for cutting ultra-narrow surgical scalpel slots, micro-fluidic channels, and biopsy jaw serrations in hardened stainless steels and superalloys without imparting mechanical cutting stresses or micro-burrs.
4. Critical Post-Processing, Ultrasonic Cleaning & Metrology Validation
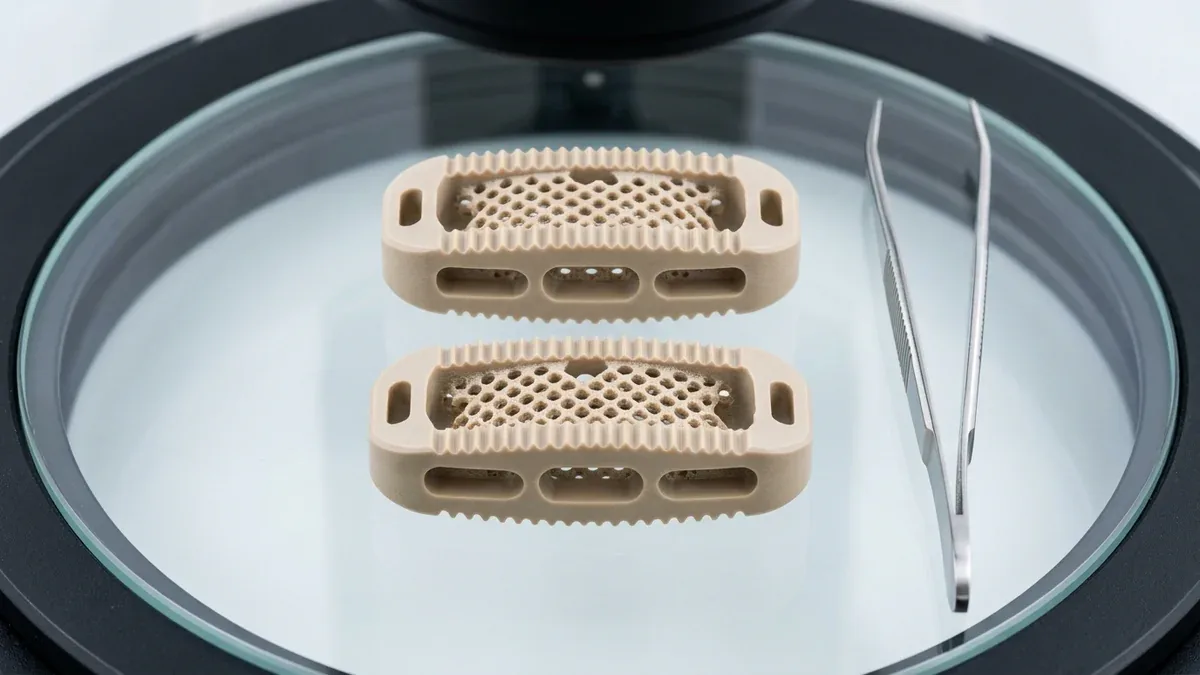
Machining is only half of the medical manufacturing process. Post-machining treatments dictate whether a part is clinically safe and biocompatible:
- Chemical Passivation (ASTM A967): Machined stainless steel components are treated in warm citric or nitric acid baths to dissolve free iron contaminants embedded from cutting tools, building an inert, corrosion-resistant chromium oxide passive film.
- Electropolishing & Micro-Deburring: Electropolishing removes micro-peaks from surgical surfaces, achieving a mirror surface roughness (Ra < 0.1 μm) that prevents bacterial colonization and blood clot formation during clinical procedures.
- Multi-Stage Ultrasonic Bio-Cleaning: Parts undergo multi-chamber ultrasonic degreasing using medical-grade biodegradable detergents, followed by repeated rinses in high-resistivity deionized (DI) water to eradicate all trace machining lubricants.
- FDA Unique Device Identification (UDI) Laser Marking: High-precision non-thermal fiber laser annealing permanently engraves 2D Data Matrix codes, lot numbers, and part identifiers without penetrating the corrosion-resistant passive layer.
5. AS Prototypes Medical Prototyping Capabilities
At AS Prototypes, we bridge the gap between creative medical engineering and commercial clinical viability:
- Full Lot Traceability: Verified Mill Test Reports (MTR) provided with every titanium, stainless steel, and PEEK batch.
- 20°C ± 1°C Climate-Controlled Metrology Lab: Non-contact 2.5D optical vision measuring systems (VMS), calibrated Go/No-Go gauges, and on-demand Zeiss bridge CMM coordinate verification.
- Rapid Prototyping Turnaround: Functional surgical instrument prototypes completed ex-factory in 4 to 8 business days (7 to 12 business days with passivation, electropolishing, or anodizing) for time-sensitive clinical evaluations.
6. Technical Engineering FAQ
Ti-6Al-4V ELI (Grade 23) is the gold standard for permanent bone plates and spinal cages due to its biocompatibility, high fatigue strength, and low interstitial oxygen content that resists in-vivo stress corrosion.
PEEK has low thermal conductivity (k ≈ 0.25 W/m·K) and softens under tool friction. We employ razor-sharp polished diamond-like carbon (DLC) tooling, high-pressure filtered deionized water or cold air blast, and post-machining annealing.
High-precision Swiss-type turning centers equipped with guide bushings, synchronized sub-spindles, and high-frequency live tooling turn, thread, and cross-drill micro-screws (Ø1.0–3.5 mm) in single setups with ±0.005 mm tolerances.
Partner with Our Precision CNC Machining & Engineering Team
Eliminate tool deflection, residual stress distortion, and tolerance stack-up risks before production begins. Upload your 3D CAD files (STEP/IGES) and 2D GD&T drawings for a comprehensive shop-floor DFM review and custom quotation.
Upload 3D CAD for Engineering DFM & RFQ