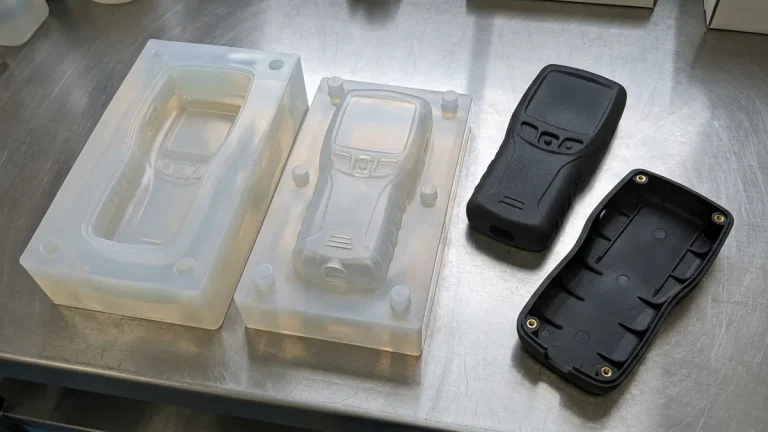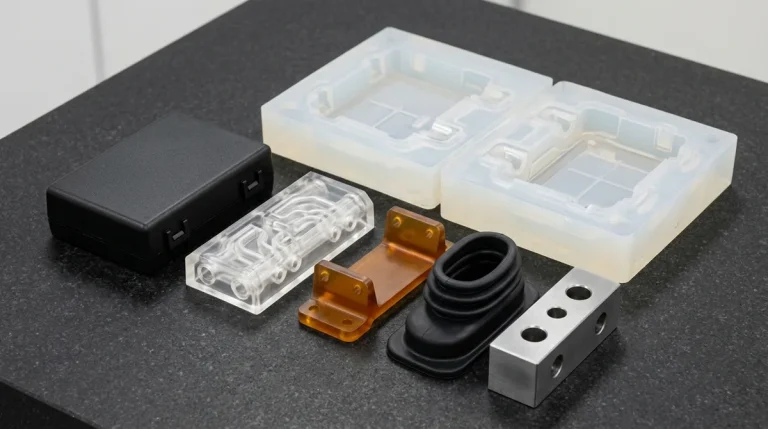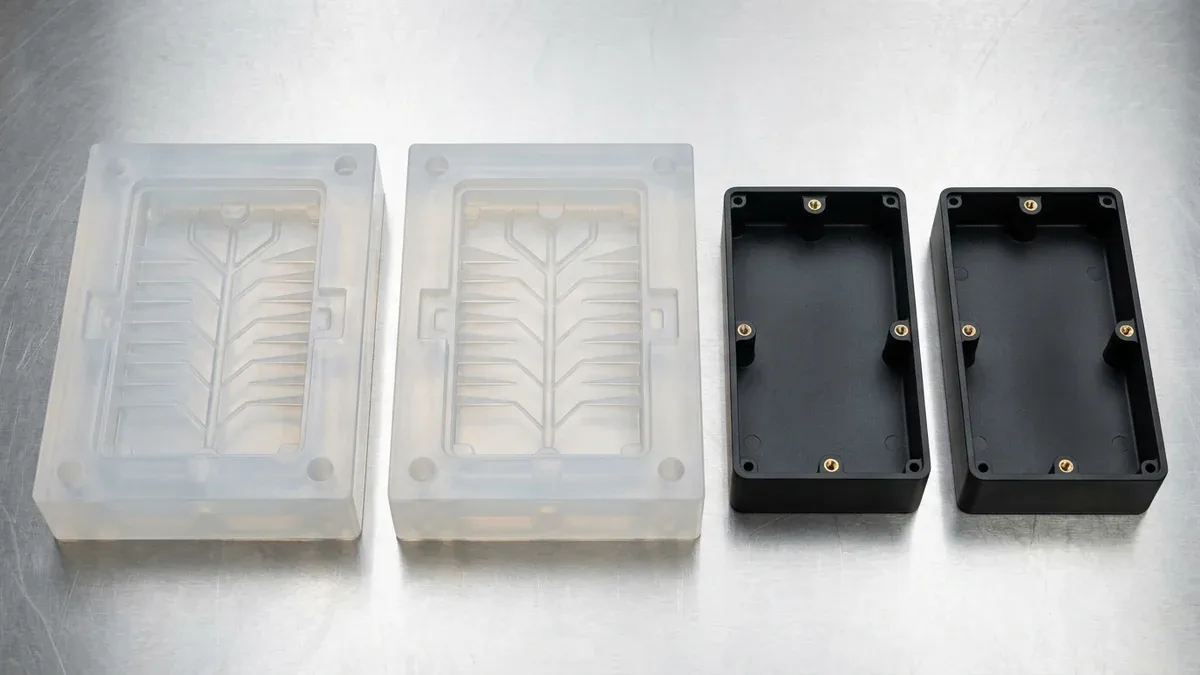
Silicone rubber molds represent the cornerstone of rapid low-volume prototyping and bridge manufacturing, enabling product development teams to replicate production-grade plastic components without committing to costly steel injection tooling. By leveraging room-temperature vulcanizing (RTV) silicone chemistry combined with polyurethane vacuum casting, hardware engineers can produce functional prototypes with injection-molded surface quality, precise geometric fidelity, and diverse mechanical properties. In our dedicated polyurethane vacuum casting and prototyping facility, mastering the chemical, thermal, and mechanical nuances of silicone tooling bridges the critical gap between initial precision CNC machining and high-volume series production.
- 1. Master Pattern Precision and Surface Quality Transfer
- 2. Platinum-Cured vs. Tin-Cured RTV Silicone Formulations
- 3. Parting Line Architecture, Gating, and Vacuum Degassing
- 4. Mold Life Expectancy and Chemical Degradation Mechanisms
- 5. Engineering Polyurethane Resin Selection Guide
- 6. Handling, Storage and Demolding Practices That Extend Silicone Mold Life
- 7. Technical Engineering FAQ
1. Master Pattern Precision and Surface Quality Transfer
A fundamental physical law of silicone tooling is that silicone rubber molds replicate the exact surface texture and micro-geometry of the master pattern with atomic fidelity. Every micro-scratch, machine toolpath mark, or polishing reflection present on the master will faithfully reproduce onto every cast part:
- Master Pattern Fabrication: Master patterns are typically produced via high-resolution SLA 3D printing (using micro-layer photopolymers) or 3-axis or 4-axis CNC machining in aluminum (6061-T6) or engineering plastics (POM-C / ABS).
- Surface Finishing Protocols: The master must undergo meticulous post-processing to achieve the intended final aesthetic. This includes manual wet-sanding from 400 to 2000 grit, bead blasting for uniform matte textures (VDI 24 to VDI 33), or optical diamond polishing for Class-A high-gloss and optically transparent components.
- Thermal Shrinkage Compensation: Engineers must account for dual-stage volumetric shrinkage during pattern preparation: the linear shrinkage of the silicone mold itself (typically 0.1% to 0.2% for addition-cure silicones) plus the volumetric shrinkage of the specific polyurethane casting resin (ranging from 0.15% to 0.4% depending on resin viscosity and cure temperature). CAD models are scaled accordingly before cutting the master.
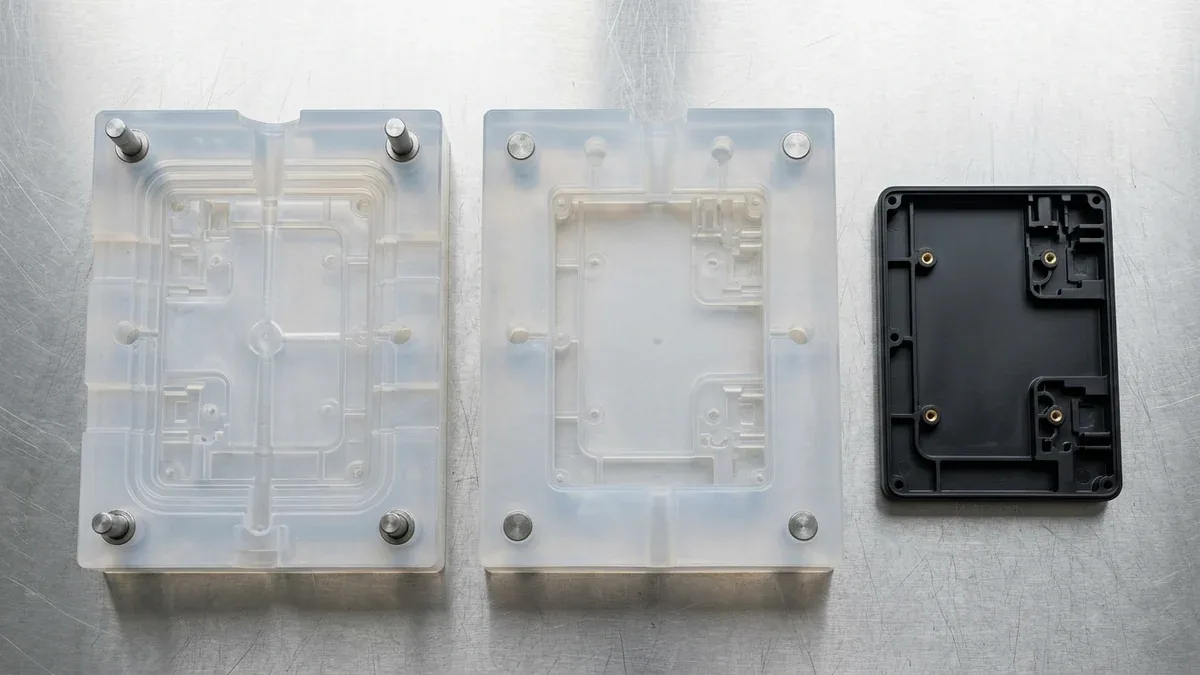
2. Platinum-Cured vs. Tin-Cured RTV Silicone Formulations
Selecting the optimal silicone chemistry determines dimensional stability, tear resistance, and overall tool longevity. Two primary Room Temperature Vulcanizing (RTV) silicone types dominate precision prototyping:
- Addition-Cure (Platinum-Catalyzed) Silicones: The industry gold standard for engineering vacuum casting. Platinum-cure silicones exhibit virtually zero post-cure linear shrinkage (< 0.1%), exceptional tear strength (up to 30 N/mm), and outstanding resistance to aggressive polyurethane isocyanates. However, they are sensitive to cure inhibition caused by sulfur compounds, amine hardeners, and certain condensation-cure materials.
- Condensation-Cure (Tin-Catalyzed) Silicones: Economical formulations suitable for simple geometric configurations or plaster/wax casting. However, tin-cure systems release alcohol byproducts during polymerization, resulting in continuous long-term shrinkage (0.4% to 1.0%) and lower dimensional stability over repetitive casting cycles.
| Engineering Property | Platinum-Cured (Addition) RTV Silicone | Tin-Cured (Condensation) RTV Silicone | Significance in Precision Prototyping |
|---|---|---|---|
| Linear Mold Shrinkage | < 0.10% (Ultra-stable) | 0.40% – 1.00% (Continuous drift) | Directly impacts dimensional tolerance repeatability |
| Tear Strength (ASTM D624) | 25 – 32 N/mm | 15 – 22 N/mm | Prevents mold tearing along deep ribs and undercut features |
| Hardness (Shore A) | Shore 38A – 42A | Shore 25A – 30A | Maintains structural wall stiffness during heavy resin fills |
| Polyurethane Chemical Resistance | Excellent (Minimal swelling) | Moderate (Prone to plasticizer leaching) | Governs total usable parts before cavity degradation occurs |
3. Parting Line Architecture, Gating, and Vacuum Degassing
The structural layout of the silicone mold is engineered manually by experienced master toolmakers to ensure laminar resin flow and bubble-free castings:
- Parting Line Creation: Using specialized scalpel techniques, the cured silicone block is cut along the component parting line following geometric feature edges. Interlocking registration keys (V-grooves or conical lugs) are carved into the perimeter to guarantee positive mechanical alignment between upper and lower mold halves.
- Gating and Venting Dynamics: Feeding sprues are attached to thick-walled sections of the part to prevent premature starvation, while micro-risers and vacuum overflow vents are located at the highest geometric summits. This prevents air pocket entrapment during resin intake.
- Vacuum Degassing Protocols: Both silicone prepolymer mixing and final polyurethane casting take place under a deep vacuum chamber (-0.098 to -0.10 MPa). Under vacuum, trapped air bubbles expand rapidly, surface, and collapse, yielding porosity-free molds and defect-free cast components.
4. Mold Life Expectancy and Chemical Degradation Mechanisms
Unlike steel tooling designed for millions of cycles, silicone rubber molds are temporary tooling with finite lifespans. The primary wear mechanism is not abrasive friction, but chemical degradation and exothermic breakdown:
- Polyurethane Chemical Attack: Polyurethane casting systems rely on polyol and isocyanate crosslinking. Over repeated cycles, aggressive isocyanate monomers penetrate the porous silicone polymer chains, extracting plasticizers and gradually hardening the cavity surface.
- Exothermic Thermal Degradation: During the exothermic crosslinking reaction in a 70°C curing oven, peak localized internal temperatures can exceed 110°C in thick sections, accelerating silicone embrittlement.
- Expected Shot Life: For standard engineering polyurethanes (ABS-like or PP-like), a premium platinum silicone mold reliably yields 15 to 25 defect-free parts. When casting highly aggressive transparent urethanes or high-temperature resins, mold life typically moderates to 10 to 15 parts before micro-tearing or surface haze appears.
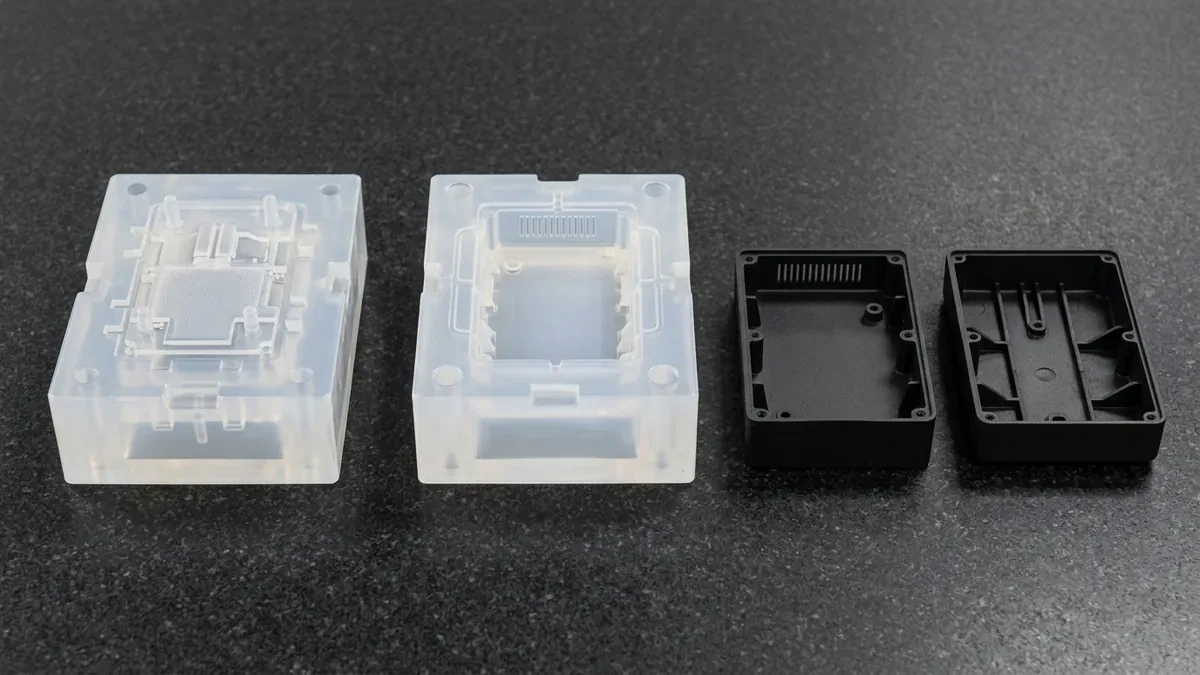
5. Engineering Polyurethane Resin Selection Guide
Polyurethane vacuum casting simulates nearly the entire spectrum of commercial injection-molded engineering plastics:
| PU Resin Grade | Simulated Thermoplastic | Tensile Modulus (MPa) | Heat Deflection Temp (HDT) | Primary Prototype Applications |
|---|---|---|---|---|
| Rigid Impact PU (Heilong / Axson) | ABS / High-Impact Polystyrene | 1,800 – 2,200 | 80°C – 95°C | Electronic enclosures, handheld instrument bezels, automotive trim |
| Flexible Polyolefin PU | Polypropylene (PP) / HDPE | 900 – 1,200 | 65°C – 75°C | Snap-fit assemblies, living hinges, fluid reservoirs |
| Optical Clear Urethane | PMMA (Acrylic) / PC | 2,000 – 2,400 | 85°C – 100°C | Automotive headlamp lenses, light pipes, medical sight glasses |
| High-Temperature Resistant PU | Glass-Filled Nylon / PBT | 2,500 – 3,200 | 120°C – 140°C | Under-the-hood automotive brackets, thermal testing fixtures |
| Elastomeric Cast Urethane | Rubber / TPE / EPDM | N/A (Shore 30A – 90A hardness) | N/A (Elastic elongation > 350%) | Overmolded grips, waterproof gaskets, vibration dampeners |
6. Handling, Storage and Demolding Practices That Extend Silicone Mold Life
Silicone mold life depends as much on handling as on chemistry, and storing molds flat, cleaning them with suitable solvents and demolding parts gently typically preserves surface detail across more shots.
- Release agent discipline: Use release agent sparingly and consistently, since an excess builds up in fine texture and transfers to the cast part, while too little causes tearing at thin edges.
- Storage: Store cured molds flat in a cool, dry place away from direct sunlight and from contact with oils, because distortion and chemical contamination shorten life.
- Demolding technique: Peel the mold away from the part progressively rather than pulling straight, and open the parting line along its full length to avoid tearing at sharp corners.
- Mold preheating: Warm molds to about 60 to 70°C before pouring polyurethane to improve flow and cure, which reduces bubbles and improves surface finish on each cast.
Following these routines lets each silicone mold produce its full expected quantity of consistent parts, and it supports repeat batches where the first and last castings need to match in dimension, texture and cosmetic quality.
7. Technical Engineering FAQ
A high-grade platinum-cured silicone mold typically produces 15 to 25 functional parts when casting standard ABS-like or PP-like polyurethanes. For aggressive optical-clear urethanes or high-temperature formulations, mold life generally ranges between 10 to 15 shots before localized surface degradation or micro-tears necessitate a new silicone tool.
Typical tolerances for vacuum casting parts range within ±0.15 mm for features up to 100 mm, and ±0.2% of nominal dimension for larger geometry. Achieving this precision requires accurate calibration of master pattern scale factors to compensate for both silicone mold shrinkage (0.1%) and resin shrinkage (0.15% to 0.4%).
Yes. Because RTV silicone captures surface micro-topography down to the sub-micron level, a master pattern with diamond optical polishing will produce silicone molds that replicate perfectly transparent, water-clear polyurethane lenses and high-gloss Class-A automotive bezels without secondary post-polishing.
Transition Seamlessly from Rapid Silicone Tooling to Precision Vacuum Casting
Optimize silicone mold life, parting line architecture, and polyurethane resin selection with our in-house vacuum casting and tooling engineering team. Upload your 3D CAD models (STEP/IGES) for a comprehensive DFM manufacturability assessment.
Upload 3D CAD for Vacuum Casting & Tooling DFM Review