

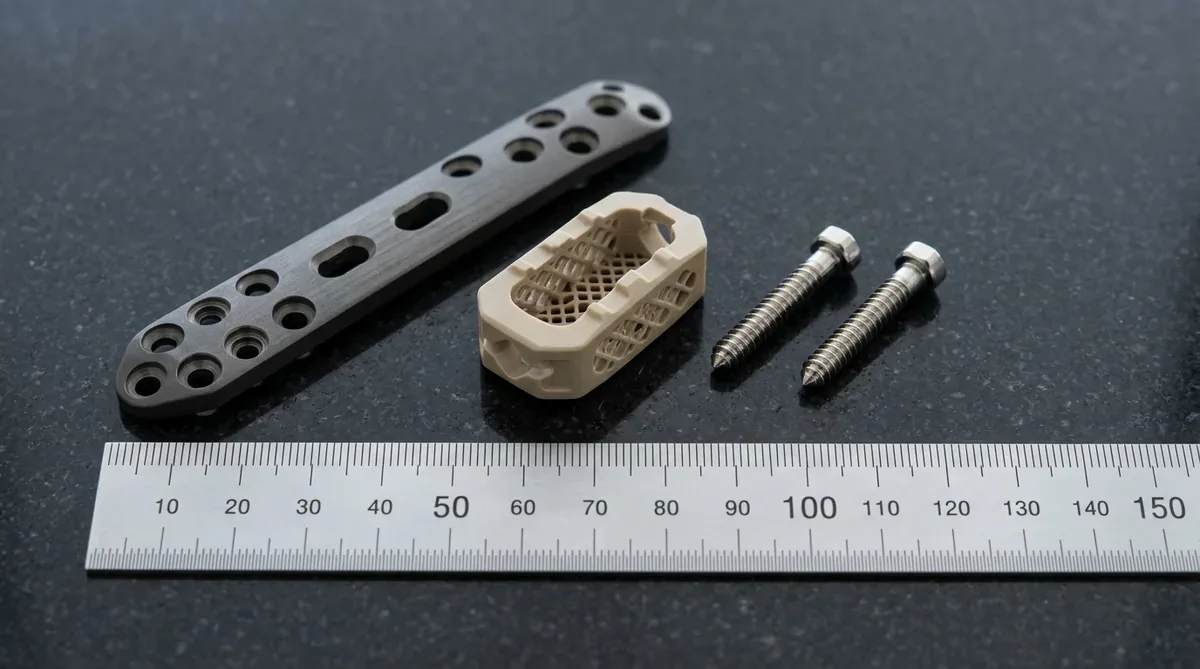
⚙ Quick Engineering Takeaways (BLUF)
- Precision Machining Spectrum: Swiss-type sliding headstock turning (live tooling, 10,000 to 15,000 RPM) machines micro-cannulas and bone screws down to 0.5 mm diameter; high-speed 3/4-axis VMCs produce complex fluidic blocks and monitor enclosures; simultaneous 5-axis machining delivers complex anatomical orthopedic implants.
- Bridge Tooling Economics: Rapid aluminum bridge molds (7075-T651 / QC-10) bridge the critical 10-to-16-week steel tool bottleneck, yielding 500 to 50,000+ injection molded parts in verified medical resins within 18 to 35 business days.
- Material Integrity & Biocompatibility: Full material traceability (MTR / EN 10204 3.1) covering medical titanium (ASTM F136 Ti-6Al-4V ELI), vacuum-melted surgical stainless steel (ASTM F138 316LVM), implantable PEEK-OPTIMA, optical-grade COC/COP, and biocompatible Liquid Silicone Rubber (LSR).
- Surface Finishing & Bio-Burden Elimination: Validated chemical passivation per ASTM A967 (citric/nitric) builds a protective Cr2O3 chromium oxide barrier (Cr/Fe > 2.0); electropolishing per ASTM B912 achieves specular Ra ≤ 0.2 μm roughness to resist bacterial biofilm colonization.
- Metrology & Cleanroom Inspection: Climate-controlled CMM with ruby continuous scanning probes and non-contact multisensor video measuring machines (VMM) inspect critical lumen concentricity, true position, and delicate microfluidic channels down to ±0.010 mm without physical deflection.
The medical technology landscape operates under severe, non-negotiable constraints: accelerating regulatory validation cycles, zero-defect mechanical reliability, stringent biocompatibility mandates, and an imperative for resilient supply chains. When medical device OEMs develop life-sustaining respiratory equipment, point-of-care microfluidic diagnostics, orthopedic surgical trials, or minimally invasive endoscopic instruments, standard prototyping lead times measuring several months introduce fatal commercial risk. Transforming complex healthcare concepts into validated physical devices demands agile medical device prototyping, rapid bridge tooling, and high-precision CNC multi-axis manufacturing.
At AS Prototypes, we support biomedical engineers, medical device startups, and multinational healthcare innovators across every phase of product maturation—from early proof-of-concept (PoC) iterations to pilot clinical trial validation runs. Operating under rigorous in-house quality management protocols aligned with healthcare manufacturing standards, our machine shop delivers micro-machined surgical titanium components, optical-grade medical polymers, and rapid bridge injection molding with precision tolerances down to ±0.010 mm.
1. Prototyping Phases & Regulatory Reality in Medical Device Manufacturing
Unlike commercial consumer electronics, medical device manufacturing operates under strict regulatory scrutiny where a single dimensional defect or chemical contaminant can compromise patient safety. Prototyping in this sector is not merely an aesthetic exercise; it serves as empirical validation for mechanical integrity, fluid dynamics, tissue response, and automated assembly tolerances.
A structured medical device development roadmap progresses through three distinct manufacturing tiers:
- Phase 1: Proof of Concept (PoC) & Ergonomic Architecture: Rapidly testing form, fit, and tactile ergonomics for surgical handles, patient monitors, and fluidic interfaces. High-speed 3-axis CNC machining and high-resolution stereolithography allow engineering teams to evaluate geometric clearance and hand-feel within 4 to 8 business days.
- Phase 2: Design Verification Testing (DVT) & Pre-Clinical Trials: Physical hardware undergoes mechanical fatigue stress testing, thermal cycling, drop testing, and preliminary cadaveric/bench trials. Components must be fabricated from end-use biocompatible substrates—such as titanium Ti-6Al-4V ELI, surgical stainless steel 316LVM, or implantable PEEK—using production-intent Swiss turning and 5-axis CNC milling to replicate actual mechanical shear and tensile performance.
- Phase 3: Pilot Clinical Batches & Regulatory Submissions: Producing 500 to 10,000 clinical trial units for human pilot studies and regulatory submissions. Rapid aluminum bridge tooling enables the injection molding of verified medical resins (such as USP Class VI polycarbonate, polypropylene, and cyclic olefin copolymers) weeks ahead of permanent production steel tooling.
A common pitfall encountered by healthcare startups is relying on general commercial machine shops that lack cleanroom wash lines or material isolation controls. Cross-contamination from brass lead particles, residual cutting oil sulfur, or unverified metal heats can cause cytotoxicity failures during biological safety evaluations. AS Prototypes isolates medical production cells, utilizing dedicated synthetic water-soluble coolants, full positive material identification (PMI), and automated multi-stage ultrasonic degreasing to safeguard biocompatibility from the first cut.
2. Precision Swiss CNC & Multi-Axis Machining for Miniature Surgical Hardware
Miniature medical hardware—including endoscopic articulating wrists, trocar cannulas, bone anchors, dental abutments, and micro-fluidic valve bodies—demands extraordinary dimensional precision and flawless surface integrity. Standard milling setups struggle with long, slender parts due to tool pressure deflection, where cantilever bending follows the structural relationship δ = (F · L³) / (3 · E · I). When the length-to-diameter ratio (L/D) exceeds 4:1, conventional workpiece clamping introduces catastrophic runout and chatter.
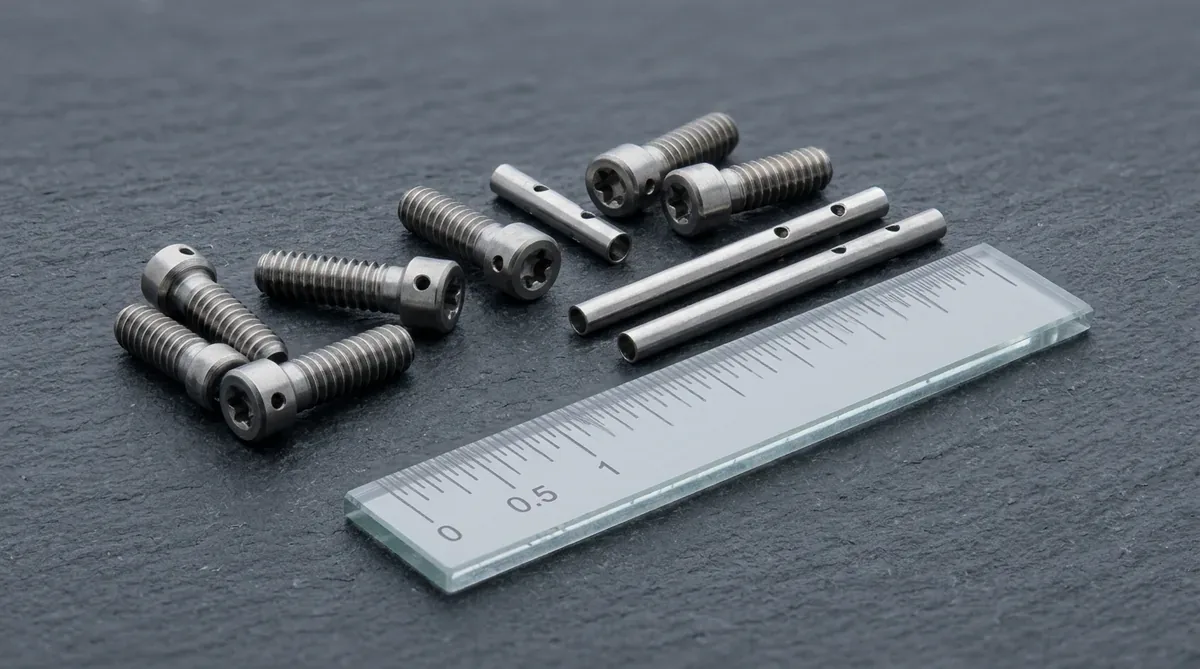
To overcome these mechanical limitations, our in-house facility deploys high-precision Swiss-type sliding headstock lathes equipped with dual spindles and synchronized live tooling:
- Guide Bushing Support: In a Swiss lathe, the bar stock is continuously advanced through a carbide guide bushing, with cutting tools engaging mere millimeters from the support point. This virtually eliminates workpiece deflection, enabling seamless machining of micro-cannulas and bone pins with L/D ratios exceeding 25:1 while holding outer diameter tolerances within ±0.010 mm.
- Simultaneous Live Tooling & Sub-Spindle Handoff: High-speed live milling spindles operating at 10,000 to 15,000 RPM perform cross-drilling, hexalobular (Torx) drive milling, helical thread whirling, and flat profiling. The secondary pick-off spindle grips the turned workpiece for back-working operations—including internal cannulation drilling and deburring—completing intricate surgical implants in a single setup without cumulative fixture transfer errors.
- Burr-Free Micro-Cannulation & High-Pressure Coolant: Cannulated medical bone screws require deep central axial fluid conduits (lumen diameters down to 0.8 mm). We utilize micro-gun drills paired with 70 to 100 bar high-pressure through-spindle coolant delivery. This intense fluidic velocity fractures chips instantly, preventing internal wall galling and clearing microscopic swarf that could otherwise lodge in bone marrow during surgical implantation.
For larger medical assemblies—such as diagnostic spectrophotometer optical chassis, robotic arm positioning linkages, and dialysis pump manifold blocks—our high-speed 3-axis and 4-axis vertical machining centers (VMCs) serve as the primary production workhorses. By deploying rigid Kurt hydraulic vises, custom-machined aluminum soft jaws, and 4th-axis rotary indexers, we achieve rapid multi-sided prismatic machining with true positional tolerances within ±0.010 mm. When anatomical contours or complex spatial port geometries require freeform 3D surfacing, our continuous 5-axis machining centers engage high-precision ball-nose cutters with optimized tool tilt angles, avoiding ball-tip zero-surface-speed dead zones to achieve uniform finishes across multi-curved surfaces.
For micro-scale channel networks and diagnostic flow cells, our specialized micro-milling capabilities deploy ultra-high-speed air-bearing spindles operating up to 60,000 RPM. Utilizing micro-endmills with cutting diameters down to 0.05 mm, we achieve channel depth uniformity within ±0.010 mm in optical polymers and pure copper heat spreaders.
3. Agile Bridge Manufacturing: Rapid Aluminum Tooling vs. Traditional Steel Molds
In medical device commercialization, the longest lead-time bottleneck is production injection molding tooling fabrication. Standard multi-cavity hardened tool-steel molds (P20, H13, or S136 stainless) demand 10 to 16 weeks of tooling and EDM cycles. When immediate clinical trial hardware or sudden market demand emerges, waiting four months introduces crippling project delays.
Rapid aluminum bridge tooling eliminates this bottleneck by utilizing forged aerospace-grade 7075-T651 or QC-10 high-strength aluminum mold inserts fitted into standardized Master Unit Die (MUD) bases:
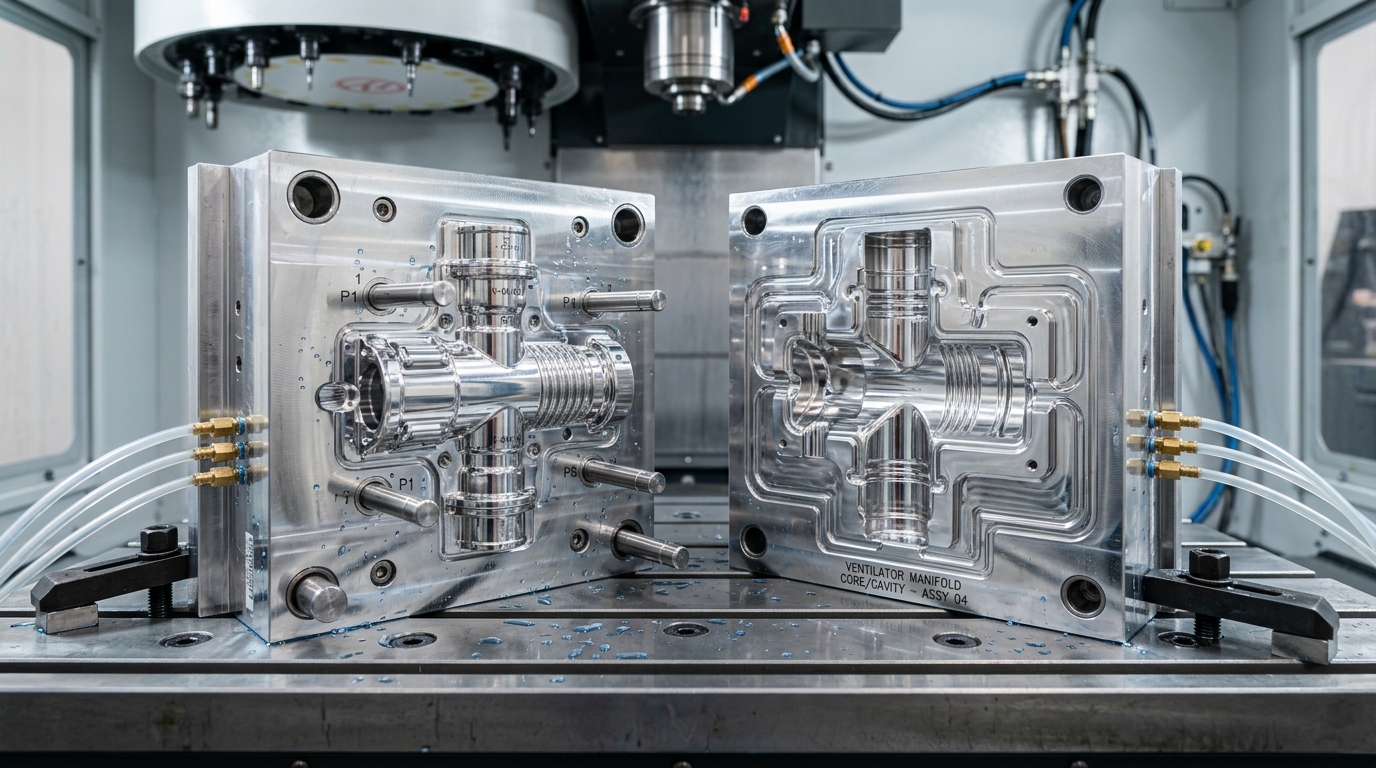
The engineering advantages of rapid aluminum tooling for healthcare manufacturing include:
- Drastic Turnaround Compression (18 to 35 Business Days): Forged 7075 aluminum exhibits a thermal conductivity of approximately 130 W/m·K—more than four times higher than P20 tool steel (29 W/m·K). This enables aggressive high-speed machining with spindle speeds of 18,000 RPM or higher and rapid heat dissipation, compressing mold fabrication from months into weeks.
- Direct Production-Grade Medical Resin Molding: While additive manufacturing (3D printing) can generate visual prototypes, printed polymers frequently fail chemical solvent wipe tests, lipid resistance, autoclave steam sterilization, or ISO 10993 cytotoxicity evaluations. Rapid aluminum tooling processes end-use medical-grade production pellets: Polycarbonate (Makrolon 2858), Medical Polypropylene (USP Class VI), Cyclic Olefin Copolymer (COC/COP), and biocompatible Liquid Silicone Rubber (LSR).
- Shortened Injection Cycle Times & Reduced Sink: The rapid heat extraction of aluminum mold walls cools thick polymer sections—such as ventilator port ribs and fluidic valve manifolds—up to 30% faster than steel tooling. This minimizes internal thermal stress, helps reduce sink marks, and accelerates pilot production runs of 500 to 50,000 parts.
- Hand-Loaded Inserts (Pick-Outs) for Complex Geometry: To avoid the massive expense and lead time of hydraulic side-action cams, our mold design engineers incorporate precision hand-loaded aluminum or beryllium-copper inserts. These inserts are manually loaded during each molding cycle to form intricate side-ports, luer locks, and internal undercuts, drastically lowering upfront tooling investment.
| Manufacturing Process | Typical Batch Size | Achievable Tolerance | Ex-Factory Turnaround | Primary Medical Applications |
|---|---|---|---|---|
| Precision Swiss Turning | 1 to 5,000+ pcs | ±0.010 mm to ±0.020 mm | 4 to 8 Business Days | Cannulated bone screws, trocar needles, dental implant abutments, endoscopic shafts |
| High-Speed 3/4-Axis VMC | 1 to 500 pcs | ±0.010 mm to ±0.020 mm | 4 to 8 Business Days | Diagnostic fluidic blocks, dialysis pump plates, surgical robot housings, monitor chassis |
| Simultaneous 5-Axis Milling | 1 to 200 pcs | ±0.010 mm to ±0.015 mm | 5 to 10 Business Days | Complex cranial fixation meshes, anatomical knee trials, multi-axial pedicle spinal heads |
| Rapid Aluminum Bridge Tooling | 500 to 50,000 pcs | ±0.025 mm to ±0.050 mm | 18 to 35 Business Days | Ventilator manifolds, IV pump chambers, disposable syringe barrels, cartridge shells |
| Liquid Silicone Rubber (LSR) Tooling | 100 to 10,000 pcs | ±0.050 mm (flash-free) | 18 to 35 Business Days | Respiratory patient masks, one-way duckbill check valves, peristaltic tubing cuffs |
4. Engineering Material Matrix for Medical Prototyping
Selecting the correct material substrate for medical prototypes involves balancing structural yield strength, chemical resistance against aggressive enzymatic cleansers, sterilization cycle compatibility, and ISO 10993 biological safety. Substrates must maintain dimensional stability during autoclave steam cycles (121°C to 134°C) or gamma irradiation while presenting zero cytotoxic leaching.
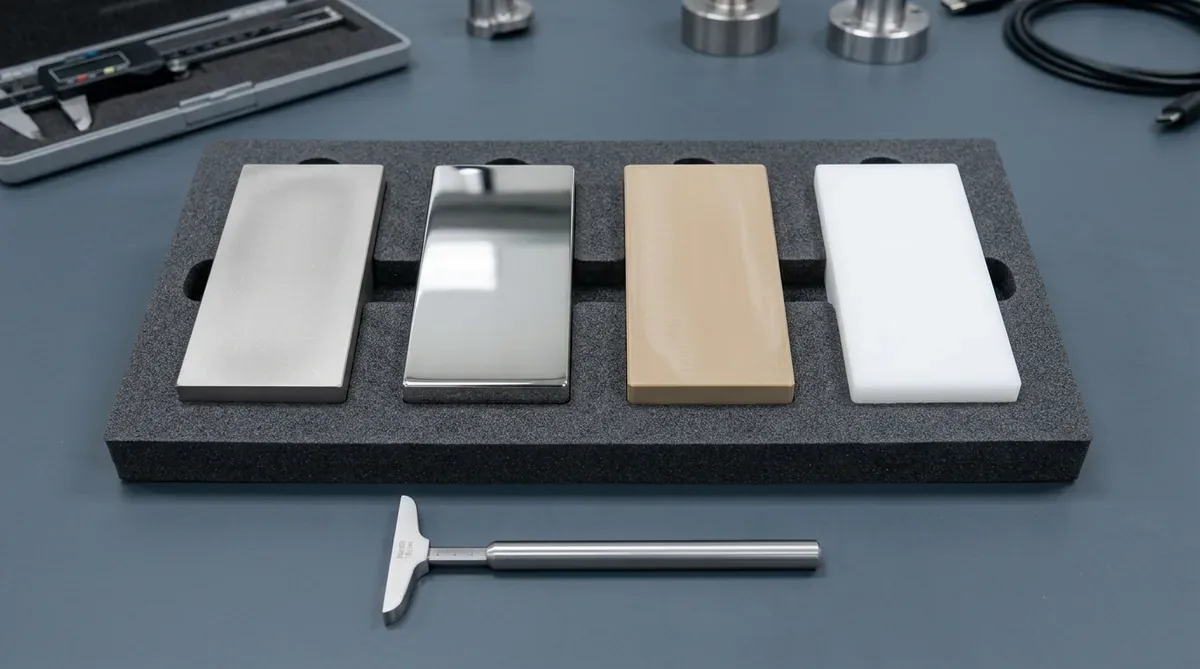
Our in-house facility maintains dedicated stock of fully traceable, verified medical-grade metals and engineering polymers:
Biocompatible Metals & Alloys
- Titanium Ti-6Al-4V ELI (Grade 23, ASTM F136): The premier standard for surgical implants. ELI (Extra Low Interstitial) specifies ultra-tight limits on interstitial elements (oxygen ≤ 0.13%, iron ≤ 0.25%, carbon ≤ 0.08%), imparting superior fracture toughness and fatigue resistance compared to standard Grade 5. With its low thermal conductivity (k ≈ 6.7 W/m·K), machining demands rigid setups, sharp PVD AlTiN-coated carbide inserts, and high-pressure flood cooling to prevent thermal work-hardening.
- 316LVM Surgical Stainless Steel (ASTM F138): Vacuum Arc Remelted (VAR) to eliminate microscopic non-metallic inclusions and gas porosity. 316LVM exhibits an ultra-clean austenitic crystal matrix with exceptional resistance to pitting and crevice corrosion in physiological saline fluids. Essential for surgical forceps, endoscopic trocar sheaths, and orthopedic pins.
- Cobalt-Chromium Alloy (CoCrMo, ASTM F75 / ASTM F1537): Exhibits extraordinary wear resistance and biocompatibility, making it the benchmark for high-load articulating surfaces in artificial hip stems and knee joint trials. CoCr work-hardens instantly, requiring rigid machine tools, low cutting speeds (Vc ≈ 25 to 45 m/min), and heavy chip loads.
High-Performance Medical Polymers
- PEEK-OPTIMA (Implantable Grade / USP Class VI): Polyetheretherketone offers an elastic modulus (3.6 GPa) much closer to human cortical bone (~18 GPa) than titanium (~110 GPa), drastically reducing stress shielding in spinal fusion cages and orthopedic trauma hardware. It is radiolucent under X-ray and CT scans, allowing clear postoperative bone growth monitoring. PEEK requires pre-machining stress-relief annealing (200°C) and intermediate thermal cycles during heavy roughing to prevent internal stress-induced warping.
- Cyclic Olefin Copolymer (COC / COP – Topas & Zeonor): A glass-like amorphous polymer exhibiting >92% light transmission, near-zero autofluorescence, and virtually zero moisture absorption (<0.01%). These optical and chemical characteristics make it the gold standard for in-vitro diagnostic (IVD) disposable cartridges, PCR reaction wells, and microfluidic lab-on-a-chip assemblies.
- Medical Polycarbonate (Makrolon 2858 / Lexan HP): Impact-resistant, dimensionally stable, and crystal clear. Widely molded and CNC machined for respiratory ventilator enclosures, dialyzer housings, and blood oxygenator shells. Resistant to ethylene oxide (EtO) and gamma irradiation sterilization.
- Medical Acetal (POM-C Medical Grade): Delivers low coefficient of friction, high dimensional stability, and exceptional machinability for surgical drill guides, sliding instrument mechanisms, and insulin pen gears.
- Liquid Silicone Rubber (LSR – Platinum Cured): Hypoallergenic, skin-contact compliant elastomer capable of withstanding extreme thermal cycling (-50°C to +200°C). Molds with micro-venting and tight parting-line fits (≤ 5 μm) ensure flash-free seals for patient ventilation masks and IV valves.
| Material Substrate | Material Standard | Density (g/cm³) | Tensile Strength (MPa) | Sterilization Compatibility | Key Medical Applications |
|---|---|---|---|---|---|
| Ti-6Al-4V ELI (Gr 23) | ASTM F136 / ISO 5832-3 | 4.43 | 860 – 965 | Autoclave, Gamma, EtO, E-beam | Spinal rods, bone plates, dental abutments, surgical instruments |
| 316LVM Stainless | ASTM F138 / ISO 5832-1 | 7.95 | 580 – 860 | Autoclave, Steam, EtO, Plasma | Surgical forceps, endoscopic trocars, vascular clip appliers |
| CoCrMo Alloy | ASTM F75 / ASTM F1537 | 8.30 | 950 – 1,200 | Autoclave, Gamma, EtO | Knee condyle trials, hip femoral heads, high-wear surgical guides |
| PEEK-OPTIMA | ASTM F2026 / USP Class VI | 1.30 | 95 – 110 | >1,500 Steam Autoclave cycles, EtO | Interbody spinal fusion cages, radiolucent retractors, heart valve parts |
| COC / COP (Topas) | USP Class VI / ISO 10993 | 1.02 | 55 – 65 | EtO, Gamma (<50 kGy) | Microfluidic flow cells, IVD cartridges, optical cuvettes, prefillable syringes |
| Makrolon 2858 (PC) | USP Class VI / ISO 10993-1 | 1.20 | 65 – 75 | EtO, E-beam, Gamma | Dialyzer caps, oxygenator housings, fluid filter bodies, surgical lighting lenses |
| Medical LSR | USP Class VI / ISO 10993-10 | 1.12 | 7 – 11 | Autoclave, Steam, EtO, Gamma | Respiratory ventilator cushions, check valves, catheter cuffs, fluidic septums |
5. Cleanroom Finishing, Chemical Passivation & Surface Engineering
Surface roughness and microscopic topography profoundly dictate cell attachment, thrombogenicity, and bio-burden retention in clinical hardware. Subsurface micro-fissures, abrasive burrs, or embedded ferrous free-iron particles from tooling friction can compromise patient safety. AS Prototypes operates dedicated surface finishing and cleanroom post-processing lines to meet strict healthcare standards:
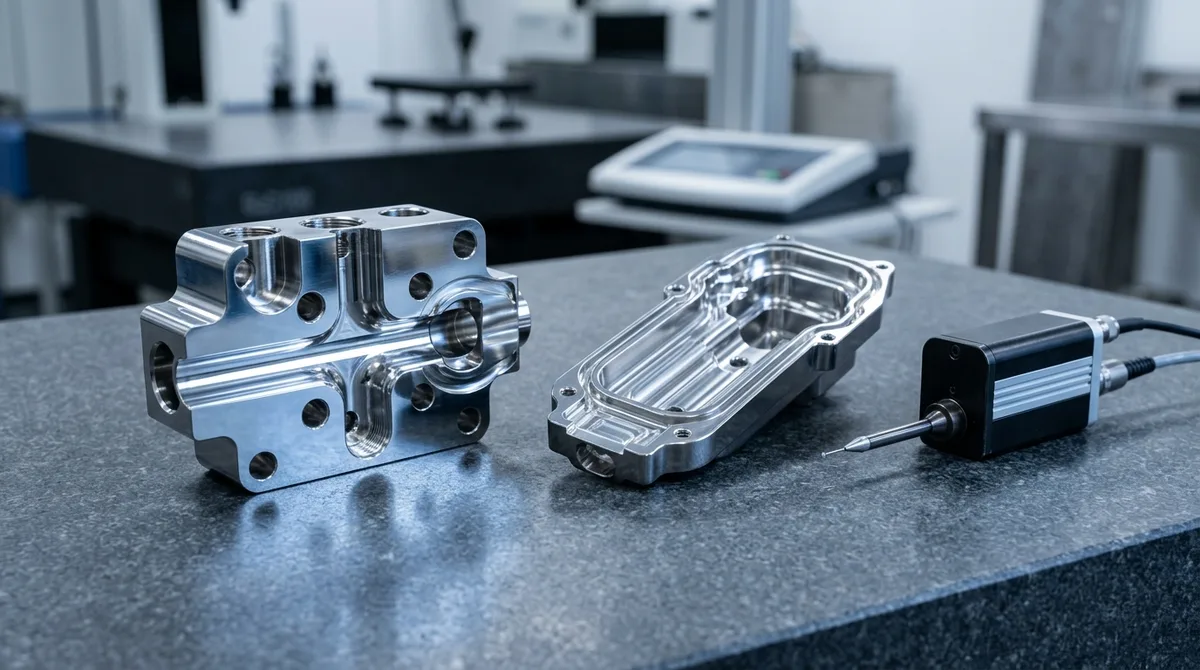
Chemical Passivation per ASTM A967
During machining, carbide and tool steel cutters inevitably transfer microscopic free-iron particles onto the stainless steel or titanium component surface. If left untreated, these particles oxidize into localized corrosion pits when exposed to saline body fluids or harsh hospital cleansers. We perform chemical passivation in accordance with ASTM A967:
- Citric Acid Passivation (Citric 2 / Citric 4): An environmentally benign, highly targeted organic acid bath (4% to 10% citric acid at 50°C to 65°C). Citric acid selectively chelates and dissolves surface iron ions without attacking alloying nickel or chromium. This elevates the surface chromium-to-iron (Cr/Fe) ratio above 2.0, establishing a robust, self-healing chromium oxide (Cr2O3) passive barrier.
- Nitric Acid Passivation (Nitric 2 / Nitric 4 with Sodium Dichromate): Reserved for high-carbon martensitic surgical steels (such as 420 or 440C scalpels and shears) requiring simultaneous heavy oxidation to purge free iron while preserving blade edge hardness.
- Verification Testing: Passivation efficacy is validated via ASTM A967 practice testing, including 24-hour water immersion testing, high-humidity exposure, and copper sulfate swab tests to ensure no free-iron reaction.
Electropolishing per ASTM B912
For blood-contacting lumens, surgical implant plates, and fluidic manifolds, mechanical polishing alone can fold over microscopic burrs and create micro-crevices where bacteria can form biofilms. Electropolishing per ASTM B912 is an electrochemical dissolution process in which the part acts as an anode in a temperature-controlled phosphoric/sulfuric acid electrolyte bath. Electric current concentrates on microscopic peaks, stripping away 5 μm to 15 μm of surface material:
- Eliminates microscopic tearing, tool marks, and burrs, achieving a specular mirror polish with surface roughness down to Ra ≤ 0.15 μm to 0.20 μm.
- Relieves micro-machining residual stresses on thin-walled tubular implants.
- Significantly reduces protein adhesion and blood clot formation in cardiovascular and endoscopic flow valves.
Multi-Stage Ultrasonic Degreasing & Bio-Burden Scrubbing
Machined components undergo a strict four-stage automated ultrasonic cleaning sequence: (1) Ultrasonic immersion in a heated alkaline biocompatible detergent bath to dissolve cutting oils and particulates; (2) Dual-stage cascading rinses in high-purity 18 MΩ·cm deionized (DI) water; (3) Alcohol dehydration rinse; and (4) HEPA-filtered hot-air drying inside a cleanroom enclosure. Every batch is immediately vacuum-sealed in double medical-grade polyethylene bags to maintain bio-burden control during transit.
| Finishing Process | Governing Standard | Target Roughness (Ra) | Dimensional Impact | Core Healthcare Benefit |
|---|---|---|---|---|
| Citric Acid Passivation | ASTM A967 (Citric 2/4) | Unchanged from machining | < 0.001 mm (negligible) | Chelates free iron; prevents pitting in autoclaves and physiological saline |
| Electropolishing | ASTM B912 / ISO 15730 | Ra ≤ 0.15 – 0.20 μm | -0.005 mm to -0.012 mm / surface | Eliminates micro-cracks and burrs; minimizes bacterial biofilm colonization |
| Titanium Anodizing (Type II) | AMS 2488 / ASTM F86 | Ra 0.4 – 0.8 μm | < 0.002 mm (thin conversion) | Anti-galling on surgical screw threads; color coding for surgical drill sizes |
| Vapor Polishing (PC / PMMA) | Internal Cleanroom SOP | Ra ≤ 0.05 μm (Optical) | 0.005 – 0.020 mm (surface reflow) | Restores total optical clarity to machined microfluidic channels and sight glasses |
| Ultrasonic DI Water Washing | ISO 14644-1 Cleanroom Protocols | Unchanged | 0 mm | Purges cutting fluids, particulate residues, and bio-burden prior to clean-bagging |
6. Cleanroom Metrology & Quality Verification Protocols
Unlike consumer parts, medical prototypes directly interface with biological tissue, drug delivery channels, and precision physiological sensors. Dimensional drift or hidden internal burrs can lead to catastrophic clinical failure. AS Prototypes integrates inspection directly into the manufacturing workflow within a temperature-controlled metrology laboratory (20.0 ± 0.5°C):
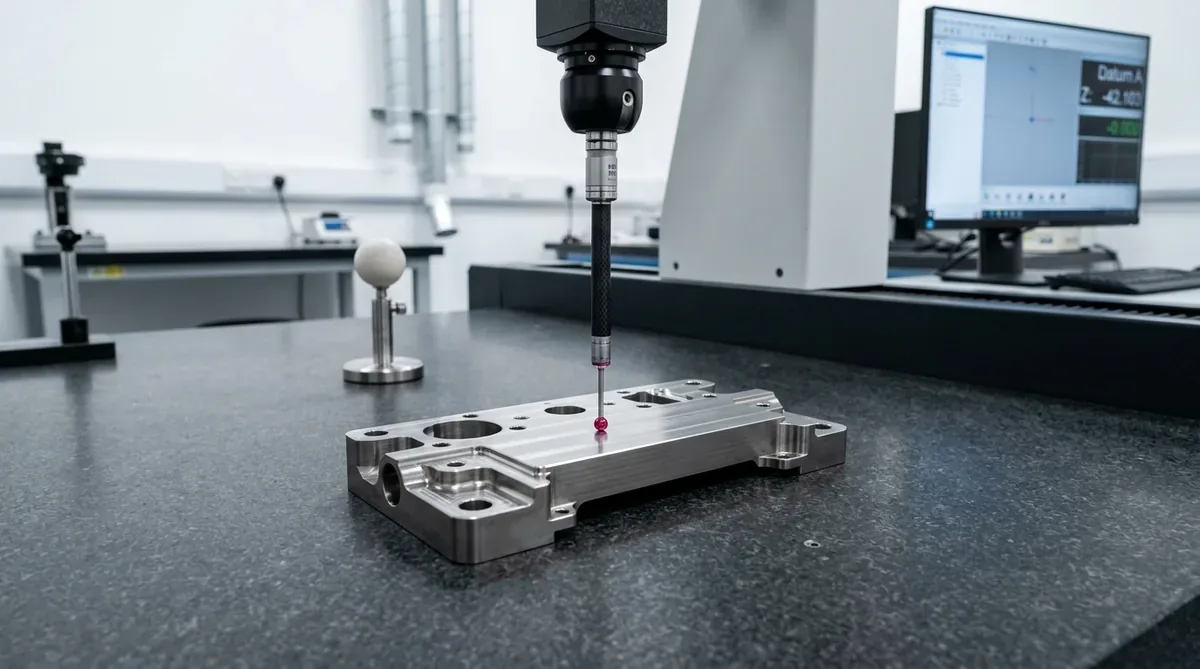
Non-Contact Multisensor Optical VMM Metrology
Microfluidic lab-on-a-chip cartridges, transparent polycarbonate optical manifolds, and flexible elastomeric seals deform under physical contact measurement probes. We deploy automated Video Measuring Machines (VMM) featuring sub-pixel edge-detection cameras, programmable multi-angle ring lighting, and integrated laser displacement sensors:
- Inspects micro-channel depths, wall draft angles, and channel widths down to 50 μm without exerting physical contact pressure.
- Measures delicate O-ring gland profiles and needle trocar tip taper angles with optical resolution down to 0.5 μm.
Zeiss CMM High-Precision Scanning
Prismatic orthopedic implant trials, titanium bone plates, and surgical robot housings are verified on our Zeiss Coordinate Measuring Machine (CMM) utilizing continuous scanning probe heads. Equipped with synthetic ruby and silicon nitride styli, the CMM performs full Geometric Dimensioning & Tolerancing (GD&T per ASME Y14.5-2018):
- Evaluates primary Datum A planar flatness, hole-to-hole true position within Ø0.010 mm, and perpendicularity across multi-axis milled faces.
- Executes automated point-cloud surface deviation comparisons against native 3D CAD models (STEP/IGES) to verify complex anatomical freeform curves.
Material Traceability & Regulatory Quality Documentation
Every medical prototyping and bridge manufacturing batch is delivered with complete quality documentation to support regulatory submission dossiers:
- Raw Material Mill Test Reports (MTR / EN 10204 3.1): Providing complete heat number traceability, chemical elemental breakdown, and tensile/yield mechanical property verification. Positive Material Identification (PMI) via handheld X-ray fluorescence (XRF) is conducted upon raw stock intake.
- First Article Inspection (FAI) & CMM Verification (Upon Request): Comprehensive dimensional inspection (available upon request) recording every ballooned drawing characteristic, measured value, tolerance band, and gauging methodology.
- Reports of Conformance (CoC): Documenting compliance with purchase order requirements, applied surface finishing specifications (ASTM A967 / ASTM B912), and bio-burden washing protocols.
7. Design for Manufacturability (DFM) Guidelines for Medical Prototypes
Optimizing part geometry during early CAD drafting prevents tooling redesigns, shortens manufacturing cycle times, and lowers unit costs. Our engineering team conducts thorough DFM reviews on all medical CAD files (STEP/IGES) within 24 hours. The following best practices reflect practical shop-floor realities:
- Internal Intersecting Lumens & Deburring: Medical fluidic manifolds frequently incorporate intersecting deep cross-holes for reagent routing. When drilling perpendicular bores, burrs form at the breakout intersection. Design intersecting holes with matching diameters, or introduce a 120° chamfer at the junction. For micro-lumens where mechanical deburring tools cannot reach, specify electrochemical deburring (ECD) or abrasive flow machining (AFM).
- Wall Thickness Uniformity in Medical Molding: When designing housings for rapid aluminum bridge tooling, maintain uniform wall thickness (ideally 1.5 mm to 2.5 mm for PC/ABS; 1.0 mm to 2.0 mm for PP). Where wall transitions are unavoidable, utilize gradual 3:1 tapered fillets. This prevents differential volumetric shrinkage, which causes sink marks and internal void cavitation that compromise pressure retention.
- Draft Angles for Optical Clear Polymers: Transparent polymers (such as Makrolon PC or Zeonor COP) scratch easily during mold ejection. Ensure minimum draft angles of 1.0° to 2.0° on all internal and external vertical walls. Optical sight windows should feature a 3.0° draft and SPI A-1 diamond mirror polish on mold cavities to ensure streak-free visual inspection of reagent fluid levels.
- Thread Integrity in Soft Polymers & Titanium: Cut threads in surgical PEEK or small medical polymers can strip under clinical tightening torque. Incorporate press-fit or ultrasonic threaded inserts (stainless steel or titanium). When machining threads directly into titanium Ti-6Al-4V ELI, use planetary thread milling rather than cut taps to prevent tap fracture, while providing a generous bottom thread relief of at least 1.5× pitch.
- Stress-Relief Annealing for Engineered Thermoplastics: Semi-crystalline and amorphous medical polymers (PEEK, POM-C, Ultem PEI) harbor significant residual stresses from extrusion. Heavy roughing cuts release these stresses, resulting in severe post-machining warpage. Specify rough machining followed by stress-relief annealing (e.g., PEEK at 200°C for 4 hours) prior to final finish passes to lock in critical ±0.010 mm tolerances.
| Part Feature / Characteristic | Standard Machining | Precision Swiss / EDM | Rapid Aluminum Molding | Recommended DFM Practice |
|---|---|---|---|---|
| Lumen / Hole Diameter | ±0.025 mm | ±0.005 mm | ±0.035 mm | Maintain depth-to-diameter ratio ≤ 8:1 for standard drills; Swiss gun-drilling for > 15:1 |
| Minimum Wall Thickness | 0.80 mm (Metals) | 0.25 mm (Titanium) | 1.20 mm (PC / PP) | Thinner walls invite vibration during milling; provide structural ribbing to maintain stiffness |
| Internal Corner Radii | R ≥ 0.25 × Cavity Depth | R ≥ 0.05 mm (Wire EDM) | R ≥ 0.50 mm | Avoid sharp internal corners to reduce tool wear, eliminate notch stress, and ease flow |
| True Position / Coaxiality | Ø0.030 mm | Ø0.010 mm | Ø0.050 mm | Design single-setup datum references; avoid multi-fixture datum shifts across critical ports |
| Surface Roughness (Ra) | Ra 0.8 – 1.6 μm | Ra 0.2 – 0.4 μm | SPI A-2 (Ra 0.05 μm) | Specify electropolishing (ASTM B912) for blood-contact lumens; bead blast for ergonomic handles |
8. Engineering FAQ: Medical Device Prototyping & Rapid Tooling
For high-precision Swiss CNC turning and 3/4-axis milling in medical titanium or surgical stainless steel, our standard ex-factory turnaround is 4 to 8 business days following DFM approval. For rapid aluminum bridge tooling, mold fabrication requires 18 to 35 business days, with initial T1 molded parts shipped via expedited air courier within 3 to 5 business days after trial sign-off.
Every medical order includes complete Mill Test Reports (MTR / EN 10204 3.1) tracing raw metal billet heat numbers back to the original melt mill, accompanied by Positive Material Identification (PMI) spectral analysis. For injection molded polymers, we provide raw resin manufacturer compliance records verifying USP Class VI and ISO 10993 testing, RoHS/REACH declarations, and detailed Reports of Conformance (CoC).
We employ a multi-step protocol: (1) High-pressure through-spindle coolant (70 to 100 bar) during micro-machining prevents burr formation at intersecting cross-holes; (2) Micro-abrasive flow machining or electrochemical deburring purges microscopic edge burrs; and (3) Automated multi-stage ultrasonic degreasing using heated biocompatible detergent, high-purity 18 MΩ·cm deionized water rinses, and cleanroom vacuum-packing eliminates all hydrocarbon residues.
Yes. Unlike 3D printed polymers that often fail biocompatibility, outgassing, or autoclave sterilization tests, our 7075-T651 aluminum rapid bridge molds process genuine medical-grade production resins, including Makrolon 2858 Polycarbonate, medical polypropylene, Cyclic Olefin Copolymers (COC/COP), and Liquid Silicone Rubber (LSR). These bridge molds typically yield 500 to 50,000+ parts for pilot clinical trials and pre-market validation.
On our high-precision Tsugami Swiss-type lathes, guide bushing continuous support enables us to hold outer diameter tolerances within ±0.005 mm to ±0.010 mm on titanium bone pins, trocar needles, and dental abutments. High-speed live milling spindles achieve true positional hole locations within ±0.010 mm, with central cannulation runout strictly controlled within 0.015 mm over long length-to-diameter aspect ratios.
Accelerate Your Medical Device Innovation to Clinical Reality
From high-precision Swiss-turned titanium surgical implants and PEEK spinal trials to rapid aluminum bridge tooling for clinical trial molding, AS Prototypes delivers the engineering agility, cleanroom precision, and regulatory traceability your healthcare project demands.
Request a Medical Prototyping RFQ






