Elastomeric components play an essential role in mechanical sealing, vibration isolation, and fluid management. Selecting the most effective rubber molding processes ensures dimensional accuracy and prolonged operational life. Consequently, manufacturing engineers must evaluate process kinematics against production volumes.
Rubber molding differs fundamentally from thermoplastic processing. Because uncured elastomers require thermal vulcanization, chemical cross-linking occurs inside heated mold cavities. Therefore, cycle times and tool venting demand meticulous temperature control.
At AS Prototypes, our injection molding division provides advanced elastomeric tooling solutions. Furthermore, for low-volume rubber prototyping, our vacuum casting department casts durable silicone and polyurethane elastomers rapidly.
1. The Three Primary Rubber Molding Methods
Industrial rubber processors rely primarily on compression, transfer, and injection techniques.
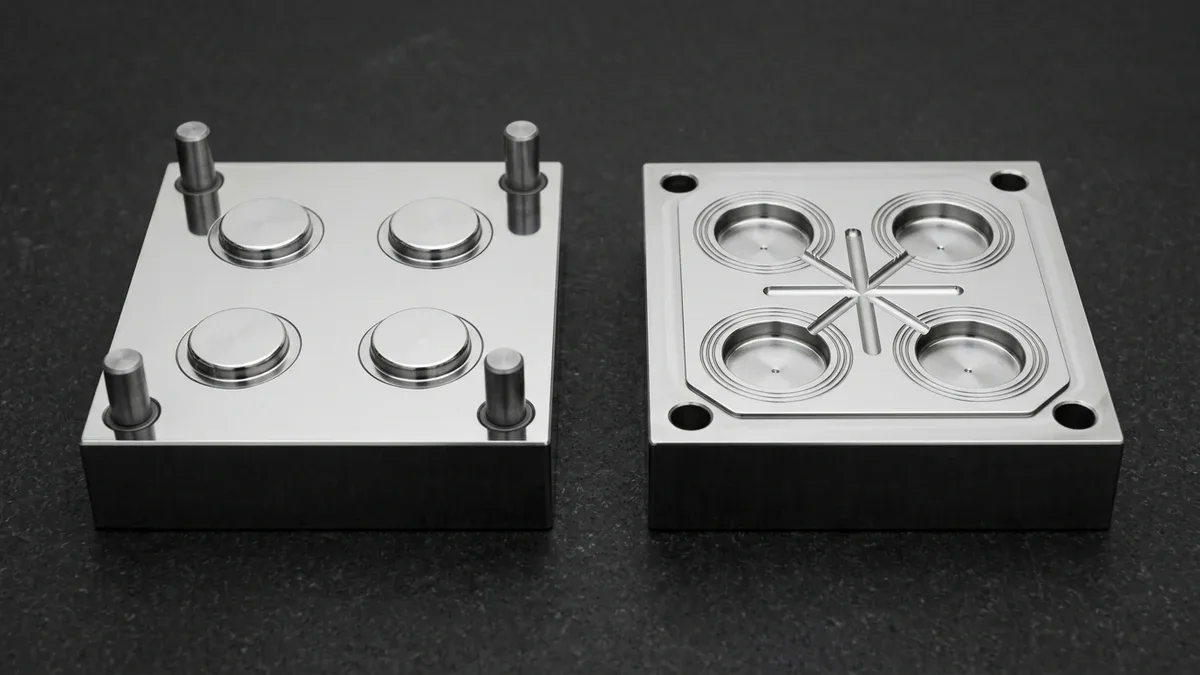
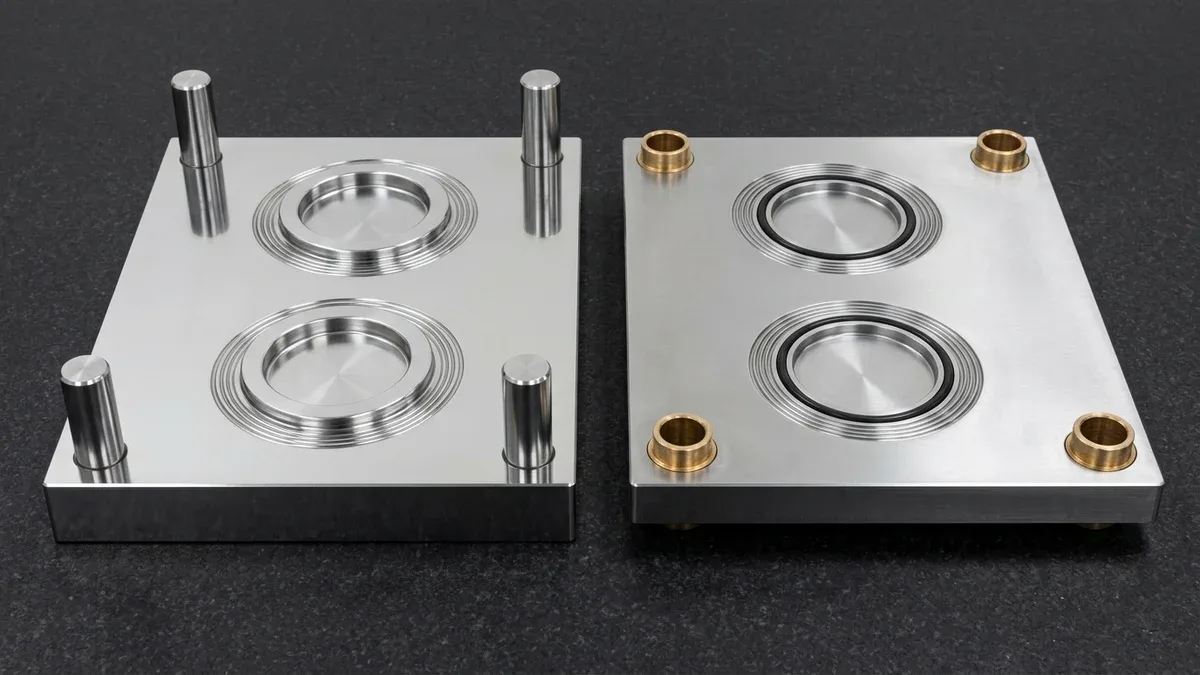
First, compression molding remains the most traditional approach. Technicians place a pre-weighed rubber blank directly into an open, heated mold cavity. Subsequently, hydraulic platens close under intense clamping tonnage. While compression molding features low tooling expense, flash trimming adds manual labor.
Second, transfer molding incorporates an intermediate pot and plunger. Specifically, the heated plunger forces softened rubber through distribution sprues into closed cavities. Consequently, transfer molding supports delicate metal inserts and tighter flash tolerances.
Third, injection molding represents the pinnacle of automated production. A reciprocating screw meters and injects heated elastomer into chilled or heated runners. As a result, cycle times drop significantly while maintaining exceptional dimensional consistency.
| Process Parameter | Compression Molding | Transfer Molding | Rubber Injection Molding |
|---|---|---|---|
| Tooling Investment | Lowest upfront tooling cost | Moderate tooling cost | Highest upfront tooling investment |
| Cycle Time | Slow (5 – 15 minutes / cycle) | Moderate (3 – 8 minutes) | Fastest (30 – 120 seconds) |
| Material Waste | Moderate flash overflow | High pot pad scrap residue | Minimal (cold runner systems) |
| Dimensional Tolerance | ISO 3302-1 Class M3 (±0.2 mm) | ISO 3302-1 Class M2 (±0.1 mm) | ISO 3302-1 Class M1 (±0.05 mm) |
| Economic Batch Volume | 50 – 1,000 units | 500 – 5,000 units | > 5,000 units mass production |
2. Engineering Elastomer Selection Guide
Specifying the right polymer compound dictates resistance to heat, ozone, and aggressive hydraulic fluids.
| Elastomer Type | Hardness Range | Operating Temperature | Primary Resistance Highlights |
|---|---|---|---|
| Silicone (VMQ / LSR) | 10 – 80 Shore A | -60°C to +230°C | Biocompatible, FDA food compliant, extreme thermal stability. |
| Fluorocarbon (Viton / FKM) | 60 – 90 Shore A | -20°C to +200°C | Outstanding resistance to aviation fuels, oils, and aggressive acids. |
| EPDM | 30 – 90 Shore A | -45°C to +150°C | Superior outdoor UV, ozone, steam, and brake fluid resistance. |
| Nitrile (NBR / Buna-N) | 40 – 90 Shore A | -40°C to +120°C | Standard workhorse for petroleum oils, lubricants, and hydraulic seals. |
| Neoprene (CR) | 40 – 80 Shore A | -35°C to +100°C | Balanced resistance to weather, moderate oils, and mechanical abrasion. |
3. DFM Rules for Elastomeric Tooling Design
To ensure repeatable mold releases and minimize flash formation, follow these practical guidelines:
First, specify generous draft angles. Incorporate one to two degrees of draft on deep sidewalls to facilitate smooth part ejection.
Second, account for volumetric curing shrinkage. Different elastomers shrink between 1.5% and 4.0% during vulcanization. Therefore, CAD core tooling must scale proportionally.
Third, place parting lines along natural part edges. Thoughtful parting line placement simplifies deflashing and protects critical sealing surfaces.
4. Technical Engineering FAQ
Compression molding places pre-weighed uncured rubber preforms directly into open heated cavities, offering low upfront tooling cost for 50 to 1,000 parts with ISO 3302-1 Class M3 (±0.20 mm) tolerances. Rubber injection molding automatically meters and injects elastomer into closed, temperature-controlled cavities, achieving 30 to 120 second cycle times, minimal flash, and tight ISO 3302-1 Class M1 (±0.05 mm) tolerances for high-volume runs.
Elastomers undergo volumetric thermal contraction as they cool from vulcanization temperatures (150°C to 200°C) to ambient room temperature (20°C), combined with chemical cross-linking densification. Linear shrinkage typically ranges from 1.5% to 4.0% depending on polymer base (NBR, EPDM, FKM, or Silicone) and Shore A filler loading, which our tooling engineers pre-compensate when CNC machining the P20, H13, or S136 mold cavity.
Yes. For 10 to 50 functional prototype units, polyurethane vacuum casting using room-temperature vulcanizing (RTV) silicone molds produces flexible elastomeric parts in 20 to 80 Shore A hardness within 7 to 12 business days ex-factory, verified via non-contact 2.5D optical vision metrology (VMS) and Shore A durometer testing.
Transition Seamlessly from Rapid Tooling to High-Precision Molding
Optimize cavity life, gate geometry, and part unit economics with our in-house tooling and injection molding engineering team. Upload your 3D CAD models (STEP/IGES) for a comprehensive Moldflow and DFM manufacturability assessment.
Upload 3D CAD for Tooling & Molding DFM Review