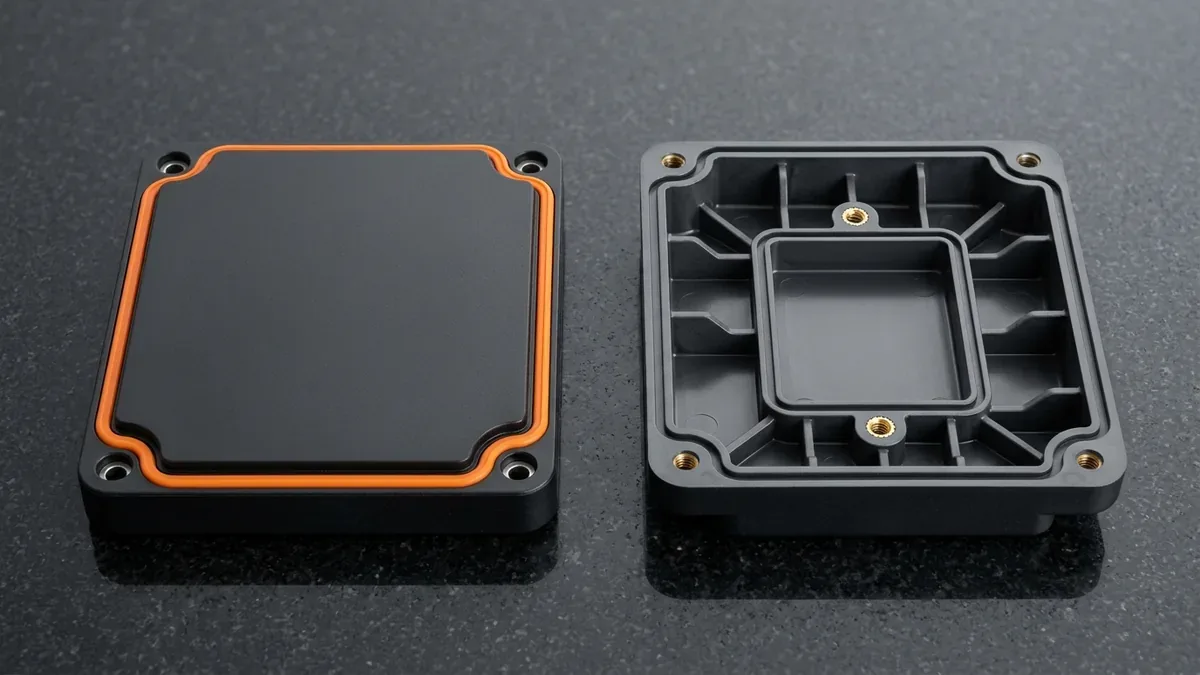
Evaluating overmolding material compatibility represents a vital engineering prerequisite for multi-material injection molding. Consequently, product designers combine rigid structural plastics with soft elastomeric grips to enhance ergonomics and sealing performance.
Successful overmolding relies on achieving high bond strength between dissimilar polymers. Furthermore, deploying advanced injection molding processes eliminates secondary assembly adhesives and mechanical fasteners.
For early-stage design validation, engineers often utilize polyurethane vacuum casting. However, scaling to series manufacturing mandates strict adherence to polymer chemistry and thermal shrinkage rules.
1. Chemical Bonding vs Mechanical Interlocking
Multi-material assemblies achieve joint retention through chemical adhesion, mechanical features, or a hybrid combination. Specifically, understanding these two bonding mechanisms dictates mold tooling complexity.
Chemical bonding occurs when molten elastomer melts into the surface molecules of a compatible rigid substrate. Therefore, compatible polymer chains interlock at the molecular interface during cooling.
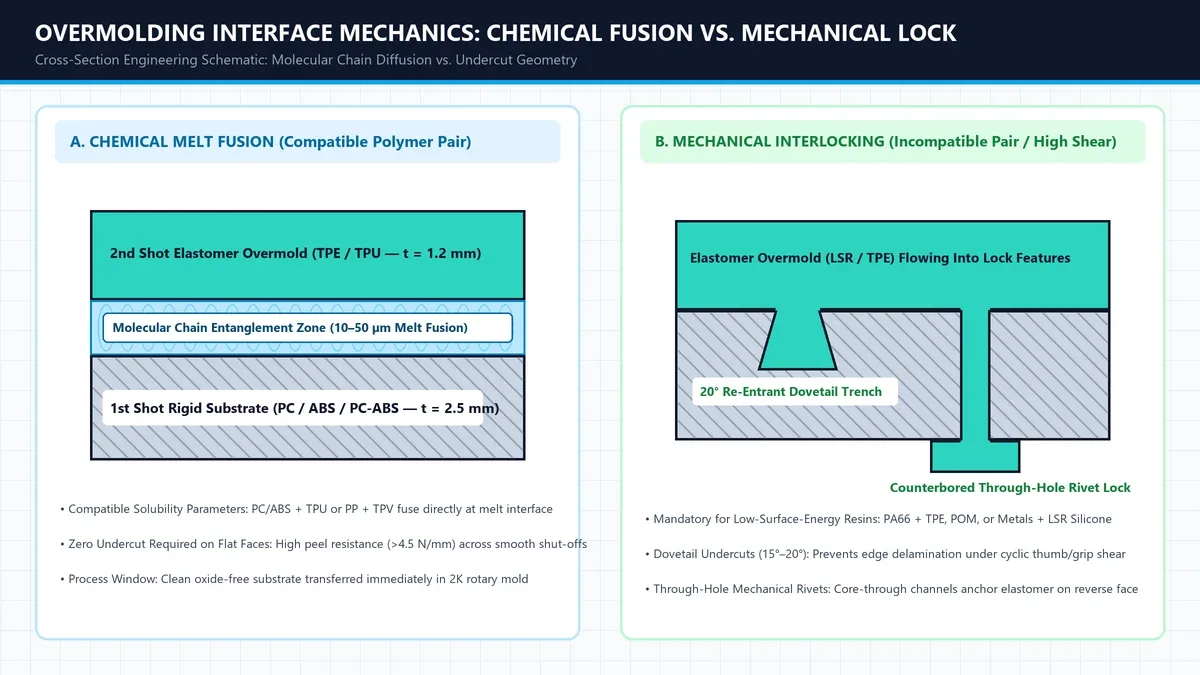
In contrast, incompatible resin pairings cannot form molecular chemical bonds. Consequently, tooling designers must integrate mechanical interlocks, such as through-holes, dovetail undercuts, and knurled grooves.
These geometric undercuts physically entrap the overmolded elastomer as it solidifies. Thus, the soft layer cannot peel away under heavy twisting loads.
2. Overmolding Material Bonding Matrix
Polymer compatibility depends on chemical polarity, melt temperature alignment, and surface energy. To illustrate, review the comprehensive compatibility matrix below:
| Rigid Substrate Resin | TPE (Styrenic) | TPU (Polyurethane) | TPV (Vulcanizate) | LSR (Silicone) |
|---|---|---|---|---|
| ABS | Excellent Chemical Bond | Superior Chemical Bond | Mechanical Interlock Only | Requires Primer / Interlock |
| Polycarbonate (PC) | Excellent Chemical Bond | Superior Chemical Bond | Moderate Chemical Bond | Requires Primer / Interlock |
| Nylon 6 / 66 (PA) | Special Modified TPE Only | Good Chemical Bond | Mechanical Interlock Only | Special Self-Bonding LSR |
| Polypropylene (PP) | Superior Chemical Bond | Not Compatible (Interlock Only) | Superior Chemical Bond | Not Compatible (Interlock Only) |
| PBT / PET Polyester | Good with Modified TPE | Excellent Chemical Bond | Moderate Chemical Bond | Requires Primer / Interlock |
3. Core Engineering Factors for Overmold Success
Achieving defect-free multi-material parts requires careful thermal management during production. Specifically, four processing parameters govern overmold adhesion.
1. Substrate Preheating & Surface Energy
Cold substrate inserts cause incoming molten elastomer to solidify prematurely before molecular diffusion occurs. Consequently, bond strength drops significantly on unheated parts.
Toolmakers maintain mold core temperatures between 60 and 90 degrees Celsius. Therefore, warm contact surfaces facilitate complete chemical interdiffusion.
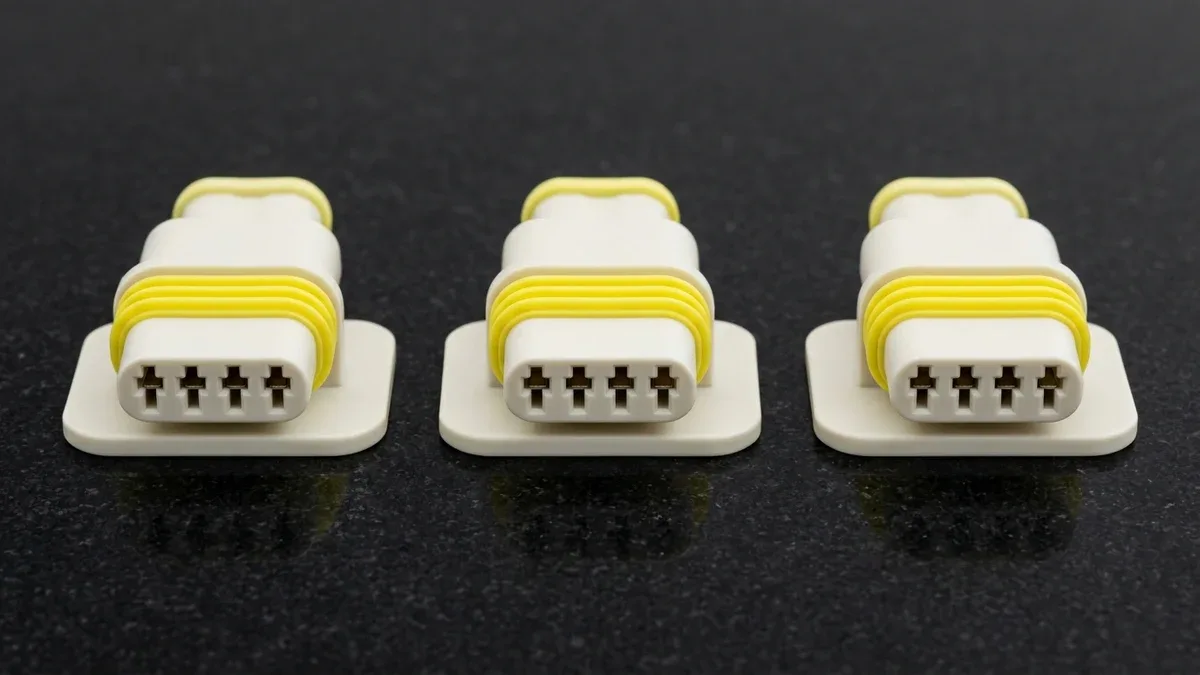
2. Differential Volumetric Shrinkage
Elastomers typically exhibit higher volumetric shrinkage rates than rigid engineering substrates. For example, soft TPE can shrink up to 2.5% during crystallization.
Conversely, glass-filled nylon substrates shrink less than 0.5%. Hence, excessive elastomer thickness creates peel stresses that delaminate edges over time.
3. Shut-Off Land Design
Molten soft resins possess low viscosity under high injection pressures. Consequently, poor tool clamping causes elastomer flash across cosmetic substrate faces.
Engineers design sharp steel shut-off lands with a slight negative crush ridge. Specifically, a 0.05 mm crush ensures clean, crisp cosmetic transition borders.
4. Overmold Elastomer Properties Comparison
Engineers select overmolding elastomers based on hardness, oil resistance, and tactile touch. To illustrate, review the primary overmold materials below:
| Elastomer Category | Hardness Range | Tensile Strength | Melt Processing Temp | Best Application |
|---|---|---|---|---|
| Thermoplastic Elastomer (TPE) | 20 Shore A to 90 Shore A | 5 to 15 MPa | 180 to 210 °C | Consumer electronics, soft toothbrush grips |
| Thermoplastic Polyurethane (TPU) | 60 Shore A to 70 Shore D | 25 to 50 MPa | 190 to 230 °C | Rugged tool bumpers, abrasive industrial wheels |
| Thermoplastic Vulcanizate (TPV) | 35 Shore A to 50 Shore D | 7 to 18 MPa | 190 to 220 °C | Automotive under-hood grommets, weather seals |
| Liquid Silicone Rubber (LSR) | 10 Shore A to 80 Shore A | 8 to 12 MPa | Room temp pump, 160 °C mold | Medical respiratory masks, waterproof gaskets |
5. Technical Engineering FAQ
Chemical bonding relies on molecular polymer chain diffusion between compatible molten resins. In contrast, mechanical interlocking utilizes undercuts, through-holes, and grooves to physically trap incompatible materials together.
Polypropylene possesses very low surface energy and a non-polar molecular structure. Consequently, standard polar TPU materials cannot adhere to it. Instead, engineers must select specialized olefin-based TPE or TPV grades or design mechanical through-hole interlocks across the PP substrate.
Higher substrate mold temperatures slow the cooling of the overmolded resin. Therefore, molten polymer chains have more time to diffuse and form a permanent molecular bond before crystallization occurs, especially when core temperatures are maintained between 60°C and 90°C.
Transition Seamlessly from Rapid Tooling to High-Precision Molding
Optimize cavity life, gate geometry, and part unit economics with our in-house tooling and injection molding engineering team. Upload your 3D CAD models (STEP/IGES) for a comprehensive Moldflow and DFM manufacturability assessment.
Upload 3D CAD for Tooling & Molding DFM Review