Auditing a prospective professional mold supplier represents a vital strategic decision for OEM engineering and procurement teams. Consequently, selecting an unqualified tooling shop creates chronic part flashing, costly tool modifications, and missed commercial launch deadlines.
Production injection molding requires substantial upfront capital investment in hardened steel tooling. Furthermore, choosing a world-class injection molding manufacturer ensures seamless transition from initial DFM through high-volume production.
Before issuing tooling purchase orders, procurement managers must verify physical shop floor capabilities. Specifically, reviewing verified manufacturing machines on the factory equipment list confirms in-house CNC and EDM capabilities.
1. 5 Critical Engineering Questions for Mold Supplier Audits
Thorough supplier due diligence uncovers hidden manufacturing risks before steel machining commences. For example, asking five specific technical questions reveals true toolmaker competence.
Question 1: What Tool Steel Grade and Heat Treatment Documentation Do You Provide?
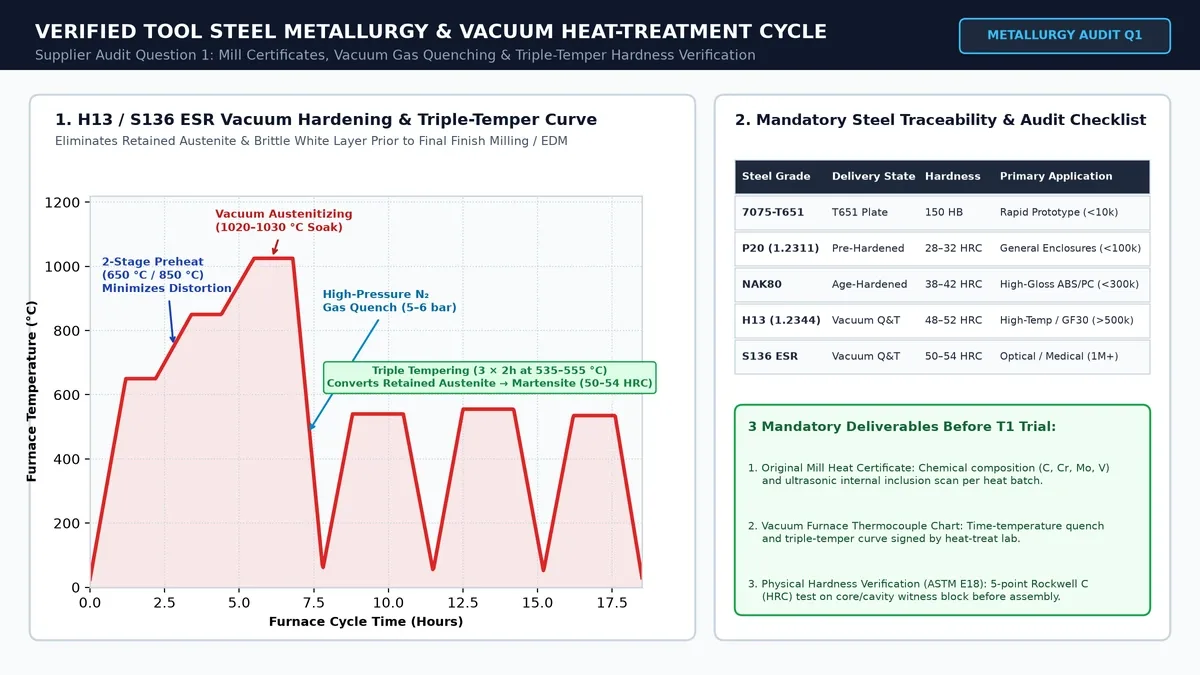
Unqualified low-cost tooling shops often substitute soft pre-hardened steel like P20 for high-volume production programs. However, abrasive glass-filled resins rapidly erode soft cavity shutoffs.
A professional mold supplier guarantees genuine verified tool steel such as H13, NAK80, or S136 stainless steel. Additionally, they provide raw material Mill Test Reports (MTR) and furnace vacuum heat treatment hardness logs.
Question 2: Do You Provide In-House Moldflow Simulation and Comprehensive DFM Reports?
Tool design without upfront flow simulation leads to unpredicted air traps, weld lines, and severe warpage. Consequently, tooling modifications after steel hardening cause expensive schedule delays.
Reputable toolmakers perform full Moldflow finite element simulation prior to steel cutting. Therefore, engineers resolve gate locations, wall thickness transitions, and cooling loops during initial engineering reviews.
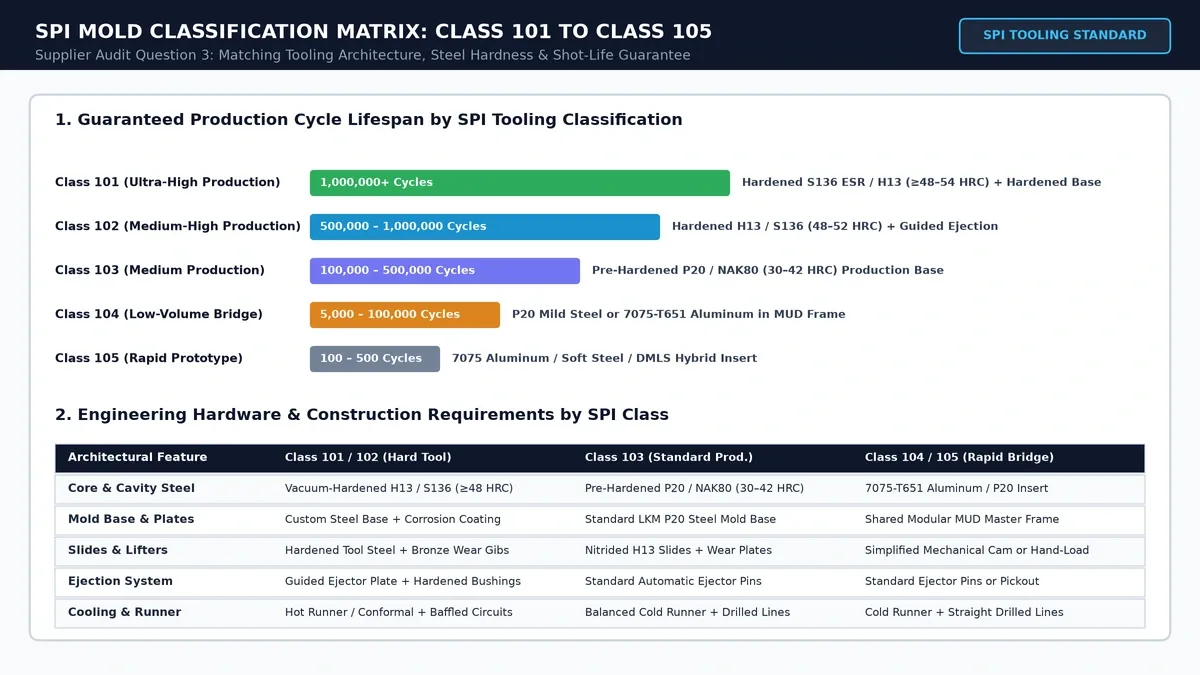
Question 3: What SPI Tool Class Will You Build, and What Is the Shot Life Guarantee?
The Society of the Plastics Industry (SPI) defines rigid tooling classifications based on production volume. To illustrate, review the SPI mold classification matrix below:
| SPI Mold Class | Production Cycle Life | Minimum Steel Hardness | Cooling Channel Standards | Target Production Volume |
|---|---|---|---|---|
| Class 101 | 1,000,000+ Cycles | ≥ 48 HRC (H13 / S136 Hardened) | Conformal / Plated Rust-Free Channels | High-volume consumer & automotive |
| Class 102 | Up to 1,000,000 Cycles | ≥ 42 HRC (420SS / 718H) | Direct Milled Core & Cavity Channels | Medium-to-high volume industrial |
| Class 103 | Up to 500,000 Cycles | ≥ 30 HRC (P20 Pre-hardened) | Standard Internal Drilled Circuits | Medium volume assemblies |
| Class 104 | Up to 100,000 Cycles | P20 or Mild Steel | Basic Water Bridges | Low-volume pilot runs |
| Class 105 | Under 1,000 Cycles | 7075-T6 Aluminum / Epoxy | No Cooling or External Chillers | Rapid prototyping validation |
Question 4: What Dimensional Inspection Reports and First Article Protocols Do You Follow?
Receiving sample parts without detailed coordinate measuring data leaves buyers blind to out-of-spec dimensions. In contrast, professional suppliers generate complete First Article Inspection (FAI) reports.
Specifically, 2.5D optical vision metrology and CMM touch probes measure critical GD&T callouts across multiple cavities. Thus, buyers receive proven dimensional compliance conforming to ISO 2768-mK before mold signoff.
Question 5: Who Owns the Mold Tooling, and What Preventive Maintenance Is Included?
Unscrupulous tooling vendors occasionally hold mold ownership hostage or charge exorbitant storage fees. Therefore, engineering contracts must explicitly confirm 100% customer ownership of tooling assets.
Furthermore, premier suppliers provide complimentary lifetime preventive maintenance for molds retained in-house. Specifically, regular ultrasonic cleaning, lubrication, and pin replacements preserve tool life.
2. Injection Mold Tooling Steel Comparison Matrix
Tooling longevity depends directly on selecting appropriate core and cavity steel alloys. To illustrate, review the steel comparison below:
| Mold Steel Alloy | Hardness (HRC) | Polishability & Clarity | Corrosion Resistance | Optimal Resin & Application |
|---|---|---|---|---|
| P20 Pre-hardened | 28 to 32 HRC | Standard SPI B2 / B3 | Low (Requires anti-rust oil) | PP, ABS, PE non-abrasive general parts |
| 718H Pre-hardened | 33 to 38 HRC | Good SPI B1 / B2 | Moderate | Large automotive panels, structural housings |
| NAK80 Age-hardened | 37 to 43 HRC | Excellent SPI A2 Diamond Polish | Moderate | Transparent lenses, cosmetic consumer electronic cases |
| H13 Through-hardened | 48 to 54 HRC | High SPI A3 / B1 | Moderate Thermal Fatigue Resistant | Glass-filled nylon (PA+GF), abrasive polymers |
| S136 Stainless ESR | 50 to 54 HRC | Superior SPI A1 Optical Mirror | Outstanding Acid & Rust Resistant | Corrosive PVC/POM, optical lenses, medical parts |
3. Technical Engineering FAQ
Professional mold suppliers own their in-house high-speed CNC machines, sinker EDM systems, and metrology labs. In contrast, intermediaries outsource manufacturing, resulting in poor communication, unverified steel, and uncontrollable quality.
SPI classifications align expected production lifespan with appropriate steel hardness and cooling designs. Consequently, specifying SPI classes prevents suppliers from substituting cheap aluminum or soft steels on long-term production contracts.
Buyers should demand official Mill Test Reports (MTR) along with ultrasonic flaw test reports. Furthermore, requesting post-heat-treatment Rockwell hardness test reports ensures cavities achieve specified wear resistance.
Transition Seamlessly from Rapid Tooling to High-Precision Molding
Optimize cavity life, gate geometry, and part unit economics with our in-house tooling and injection molding engineering team. Upload your 3D CAD models (STEP/IGES) for a comprehensive Moldflow and DFM manufacturability assessment.
Upload 3D CAD for Tooling & Molding DFM Review