

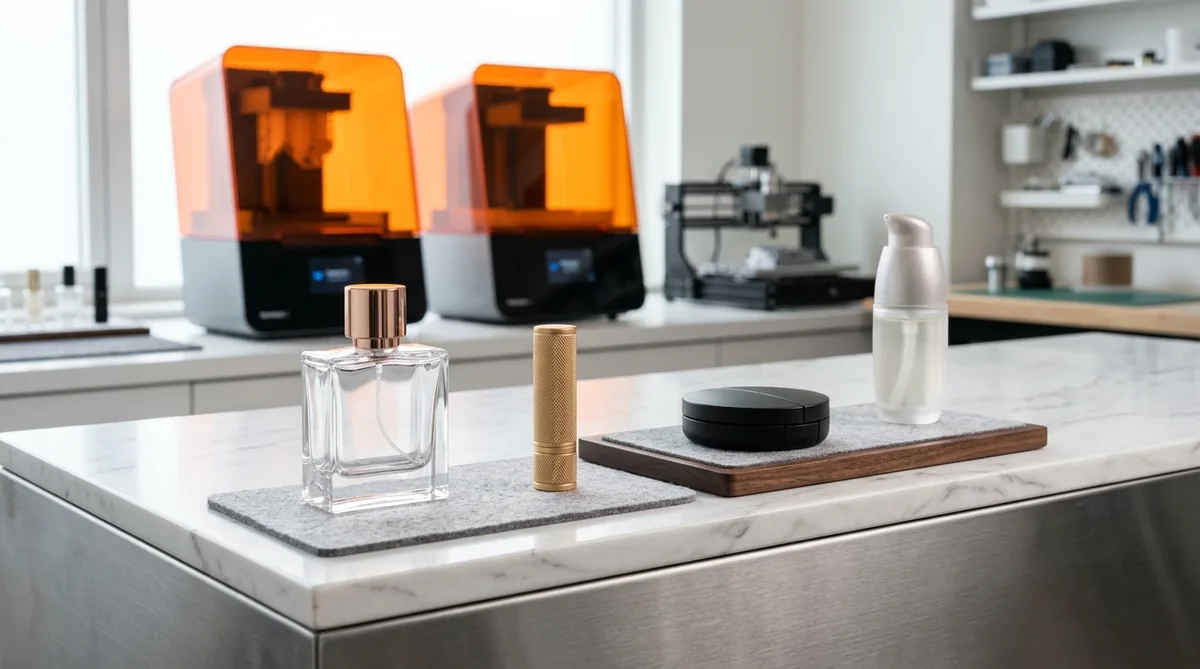
In the beauty, fragrance, and premium skincare sectors, packaging is far more than a protective vessel—it is the tangible embodiment of brand prestige, tactile luxury, and consumer emotional connection. However, commercializing innovative packaging concepts—from heavy-base perfume flacons and magnetic-closure cushion compacts to intricate swivel lipstick mechanisms—demands balancing delicate aesthetics with mass-production feasibility. Rapid prototyping in the cosmetic industry bridges this design-to-manufacturing divide. By integrating high-resolution stereolithography (SLA), polyurethane vacuum casting, precision CNC metal machining, and luxury PVD finishing, packaging engineers can validate ergonomics, seal hermeticity, and shelf-appeal in days rather than waiting months for steel molds.
Key Packaging Challenges Addressed by Rapid Prototyping
Cosmetic packaging development involves unique mechanical and sensory challenges that digital 3D renderings cannot evaluate:
- Weight & Haptic Perception: High-end consumers equate physical heft with luxury. Prototyping allows designers to test internal metal ballast weights (zamak or stainless steel cores) embedded inside injection-molded acrylic caps to achieve the exact target center-of-gravity.
- Tactile Snap & Sound Acoustics: The acoustic pitch and tactile resistance of a compact case latch or a magnetic lipstick cap closing must communicate high quality. Prototyping allows fine-tuning of neodymium magnet air gaps and interference snaps before mold release.
- Tolerance Stack-Up in Multi-Part Mechanisms: A modern lipstick tube contains an inner elevator spiral, guide sleeve, outer shell, and decorative base. Small-batch prototyping validates clearance fit down to ±0.02 mm, preventing sticky binding or loose rattling during twisting.
Core Prototyping Technologies for Cosmetic Components
In our in-house rapid manufacturing workshop, cosmetic packaging concepts are realized through complementary digital production streams:
1. High-Resolution SLA & Optical Polyurethane Casting
Replicating thick-wall glass and crystal-clear Surlyn or PMMA perfume bottles requires high optical clarity. We utilize high-resolution Stereolithography (SLA) followed by automated solvent clearing and UV curing to create master patterns. When 10 to 50 functional samples are required for consumer focus groups, polyurethane vacuum casting in optical clear PU resins reproduces glass-like transparency, zero air bubbles, and true heavy-bottom walls without expensive mold NRE.
2. Multi-Axis CNC Machining for Metal Caps & Sleeves
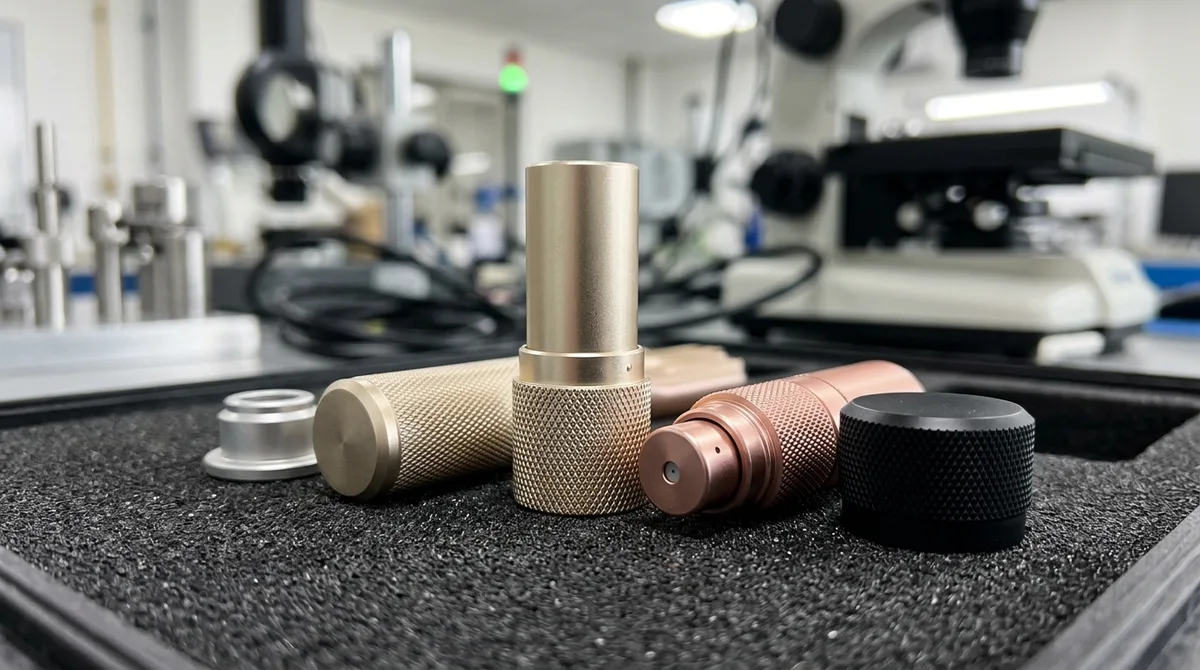
Luxury cosmetic caps, lipstick casings, and mascara shells frequently specify metal shells for cold-to-the-touch tactile feel. Utilizing precision multi-spindle CNC turning and 3/4-axis milling, we machine aerospace-grade 6061-T6 aluminum, brass, and stainless steel billets. We produce diamond-knurled grip bands, fine-pitch threads, and razor-sharp chamfers that showcase impeccable machining craft.
3. Rapid Tooling & Bridge Injection Molding
When entering pilot market launches or clinical consumer trials (500 to 20,000 units), prototyping shifts to rapid aluminum (Al 7075) or pre-hardened steel (P20/NAK80) tooling. This produces end-use components in genuine production resins—including Surlyn, PET, Polypropylene (PP), and post-consumer recycled (PCR) plastics—with turnaround times of 18 to 35 business days.
Prototyping Process Selection Matrix
The table below summarizes manufacturing processes, achievable finishes, and volume suitability across cosmetic packaging applications:
| Prototyping Method | Representative Resins / Alloys | Surface Finish Capability | Optimal Volume | Typical Cosmetic Application |
|---|---|---|---|---|
| SLA 3D Printing | Water-clear acrylic resin, Tough ABS-like resin | Optical clear polish, soft-touch matte spray | 1 – 10 units | Form and fit validation, preliminary photo mockups |
| Polyurethane Vacuum Casting | Optical PU (PMMA-like), Tough ABS-like, Elastomeric PU | Molded-in texture, translucent tint, high gloss | 10 – 50 units | Consumer focus groups, ergonomic marketing samples |
| Multi-Axis CNC Machining | Aluminum 6061, Brass C3604, Zamak-3, Delrin (POM) | Diamond knurling, satin bead blast, anodized colors | 1 – 500 units | Heavyweight luxury caps, lipstick shells, compact frames |
| Rapid Tooling Injection Molding | Surlyn, PETG, PP, ABS, PCTG, PCR resins | SPI-A1 mirror polish, chemical etch textures | 500 – 20,000 units | Pilot commercial runs, retail shelf-life verification |
Luxury Surface Finishing & Metallization
A cosmetic prototype must look and feel indistinguishable from a final department-store product. Our specialized in-house surface finishing capabilities include:
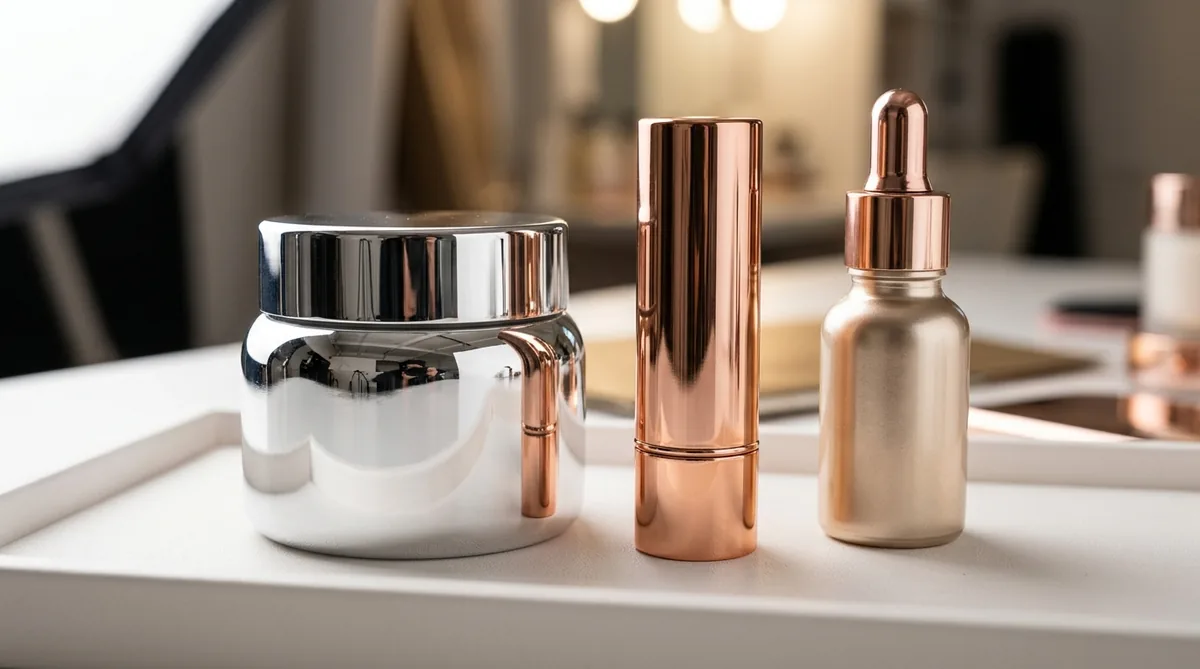
- Vacuum Metallization (PVD Deposition): Applying ultra-thin layers of evaporated aluminum followed by tinted protective lacquers to produce brilliant mirror chrome, rose gold, rich champagne, and metallic gunmetal finishes on plastic or metal substrates.
- Satin Anodizing & Chemical Brightening: Producing deep, scratch-resistant metallic colors across CNC aluminum lipstick shells and compact bezels, with controlled Ra roughness from ultra-matte to liquid gloss.
- Soft-Touch Tactile Coatings: Spraying two-component polyurethane soft-touch elastomeric coatings that impart a velvety, rubberized grip on skincare pump dispensers and foundation compacts.
- Precision Laser Etching & Hot Foil Stamping: Crisp application of logos, micro-lettering, and metallic foil branding across curved container contours.
Finishing Aesthetic & Durability Matrix
The following engineering guide details key decorative treatments and their performance characteristics:
| Decorative Treatment | Visual / Haptic Effect | Abrasion Resistance | Chemical Resistance (Alcohol/Oils) | Target Packaging Substrate |
|---|---|---|---|---|
| PVD Mirror Chrome / Gold | High specular reflectivity, luxury jewel aesthetic | High (With UV topcoat) | High (Resists perfume fragrance oils) | ABS, Zamak, Aluminum |
| Satin Color Anodizing | Deep metallic luster, fine brushed or bead-blast texture | Maximum (Hard anodic layer) | Maximum (Impervious to solvents) | Machined 6061 Aluminum |
| Velvet Soft-Touch PU | Warm, matte rubberized tactile sensation | Moderate | Good (Resists creams and lotions) | ABS, Polycarbonate, PP |
| Optical Vapor Polishing | Crystal-clear glass-like clarity | Moderate | Subject to base resin traits | Polycarbonate (PC) (with post-vapor 60–80°C annealing; PMMA polished via diamond flycutting & rotary buffing) |
Functional Testing & Compatibility Validation
Before launching high-volume production, functional prototypes undergo critical validation routines:
- Formula Compatibility & Stress Cracking: Immersing prototype polymers in actual cosmetic formulas (containing essential oils, alcohol, and active chemical emulsions) at 45°C for 48 hours to ensure zero environmental stress cracking (ESC) or chemical leaching.
- Drop Testing & Impact Durability: Verifying that weighted compacts and perfume caps survive 1.5-meter concrete drops without hinge breakage or glass chipping.
- Vacuum Hermetic Leak Testing: Testing threaded closures and pump dispenser gaskets inside vacuum decay chambers to guarantee zero leakage during air cargo transport.
We achieve luxury weight and haptic feel in prototypes by utilizing high-density vacuum-cast polyurethane resins or machining solid thick-wall acrylic (PMMA), often paired with precision-machined brass or zamak ballast weights concealed within the bottle base or metal cap assembly.
Yes. Our rapid tooling department uses pre-hardened tool steel (P20 or NAK80) molds with balanced heating systems specifically engineered to process high-clarity Surlyn resin, holding tight shrinkage tolerances and achieving optical SPI-A1 cavity polishes.
We recommend submitting 3D models in STEP (.stp) or Parasolid (.x_t) format, along with 2D drawings in PDF format indicating critical thread tolerances, seal surfaces, acceptable parting lines, and cosmetic finish specifications (such as Pantone color codes and SPI texture standards).
Formulation Compatibility Testing for Cosmetic Packaging
Cosmetic packaging prototypes must be tested with the actual formulation, because fragrance alcohols, essential oils and emollients cause stress cracking, swelling or discoloration in many clear plastics.
- Stress cracking: Polycarbonate and some acrylics crack when molded-in stress meets ethanol or fragrance oils, so use stress-relieved parts or select more chemically resistant resins such as PETG for cosmetic contact.
- Closure and leak testing: Verify thread fit, closure torque and liner compression with filled samples, and check leakage after temperature cycling and transport vibration.
- Decoration durability: Run tape adhesion and rub tests on metallized, painted and printed surfaces after exposure to the formulation, since solvent in fragrance can soften coatings.
- Dimensional verification: Measure neck finish, thread pitch and seal diameters on prototypes, because small deviations affect closure fit more than visual appearance.
Testing with real formulations before tooling avoids expensive redesigns after launch, and it gives packaging teams data to choose between materials, decorations and closures while changes to the prototype remain quick and simple.
Elevate Your Cosmetic Packaging from Concept to Reality
From crystal-clear optical bottles and custom CNC metal closures to bridge-production rapid tooling with luxury PVD finishes, AS Prototypes delivers fast, flawless packaging prototypes that captivate consumers and accelerate retail launches.







